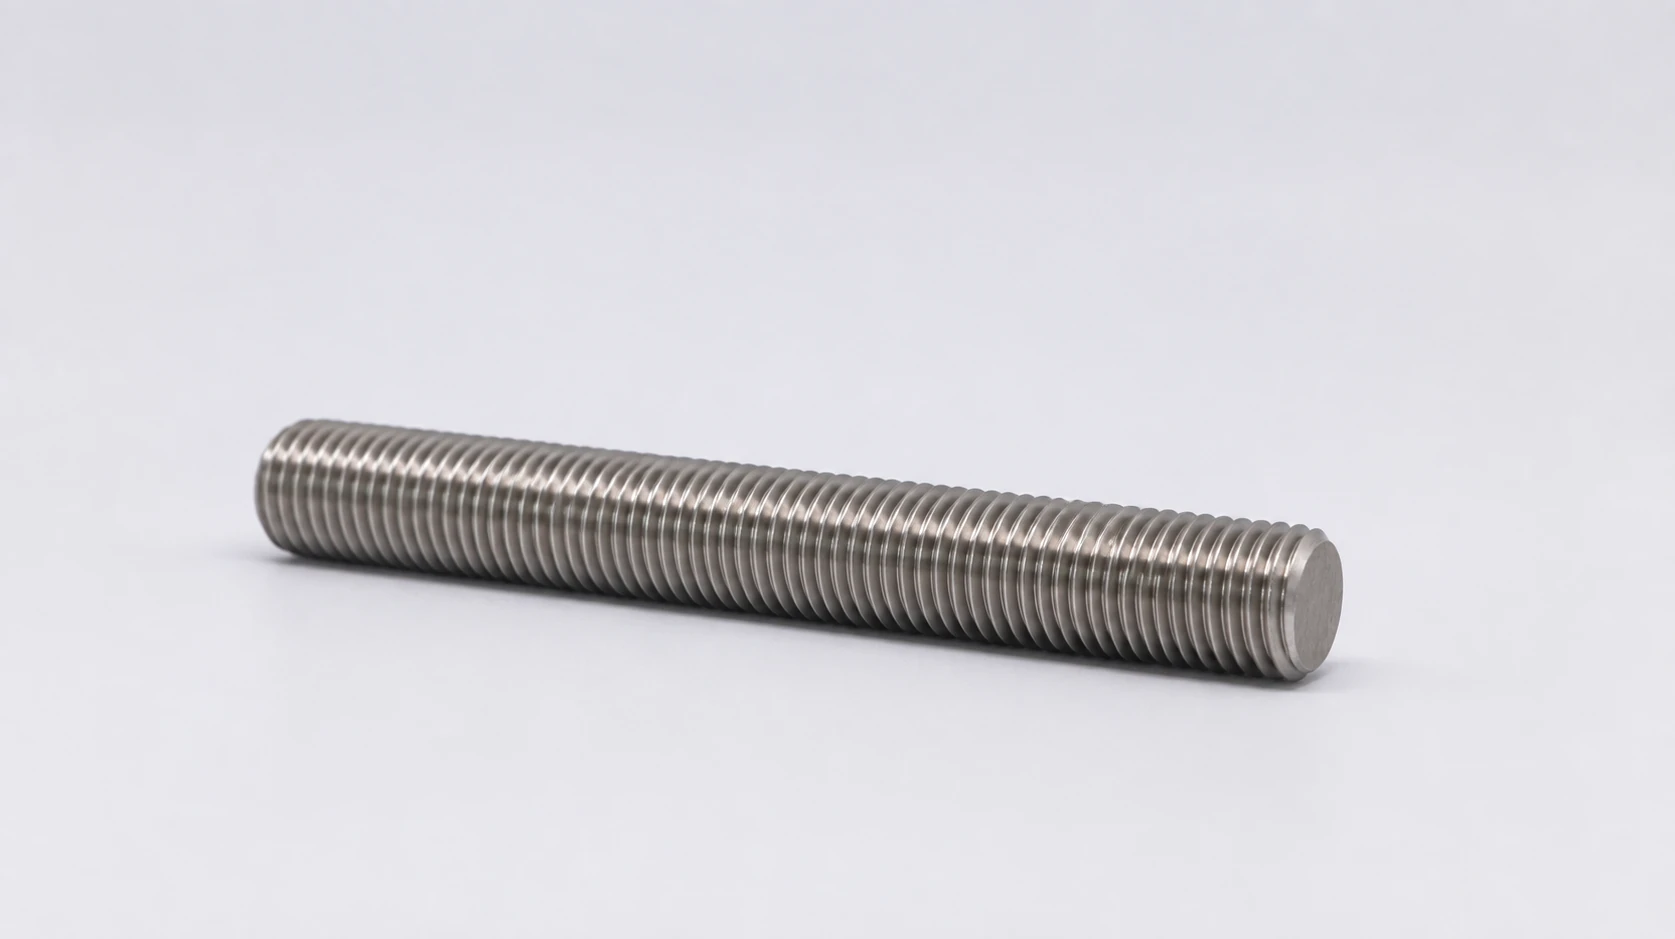
Inconel X-750 Stud Bolts
ASME B18.31.2ASTM B637
Inconel X-750 stud bolts pair a precipitation-hardened nickel-chromium alloy with double-ended closure for turbine casing, steam bonnet, and rotor tie-bolt joints under sustained heat and cyclic load. The alloy resists relaxation and creep.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated and agedSolution treatment prepares the alloy for controlled precipitation aging, which develops the strength of the ordered condition.
What we can make in Alloy X-750
Fully threaded
Two nuts clamp the flange or cover; usable thread length spans the assembled grip.
Double-end
A plain centre spans the grip, with a threaded portion at each end for the nuts.
Tap-end
One end engages a tapped casing; the exposed end accepts the cover nut.
- Threads
- Metric · UNC · UNF · 8UN · UNJ
- Forms
- Continuous thread · Double-end · Tap-end
- Final condition
- Solution treated and aged
- Inspection
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
Manufacturing route
CNC machining suits samples and special end forms. Repeat lots use cut-to-length stock with rolling or cutting selected for the ordered thread and material condition.
Heat treatment & final condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
End lengths, runout and effective thread engagement are checked separately from overall length; tap ends are gauged to their own fit requirement.
Where X-750 fits — and what matters
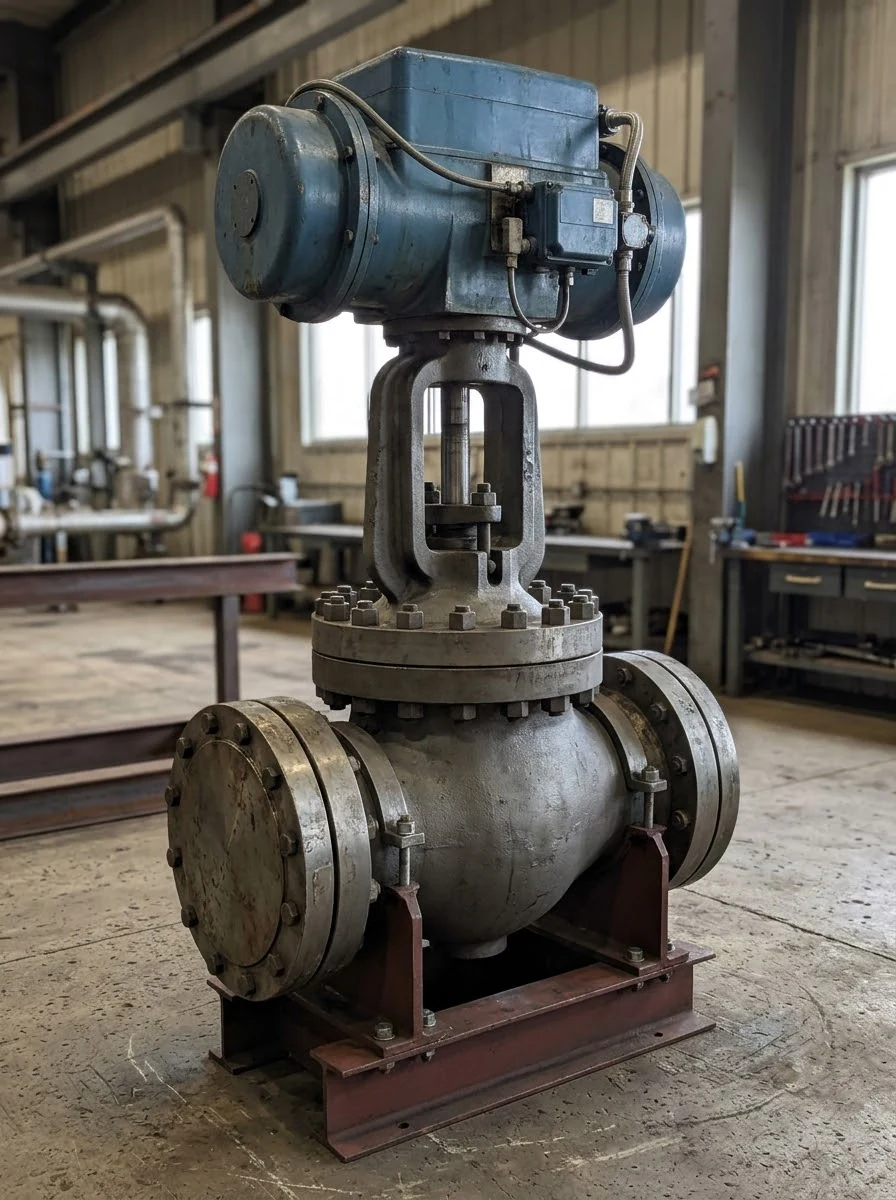
High-pressure steam valve bonnets
Inconel X-750 Stud BoltsInconel X-750 studs clamp hot steam-valve bonnets through accessible nuts. Their precipitation treatment is chosen for the temperature and duration of loading, so the stud's hot strength matches the operating duty. On tapped-stud bonnets, the cover lifts off after the nuts are removed while the studs remain in the valve body.
Connection requirements
- Bonnet joint thickness, gasket type, and required preload
- Stud diameter, overall length, and nut engagement at each end
- Temperature range, cycling duty, and heat-number certification
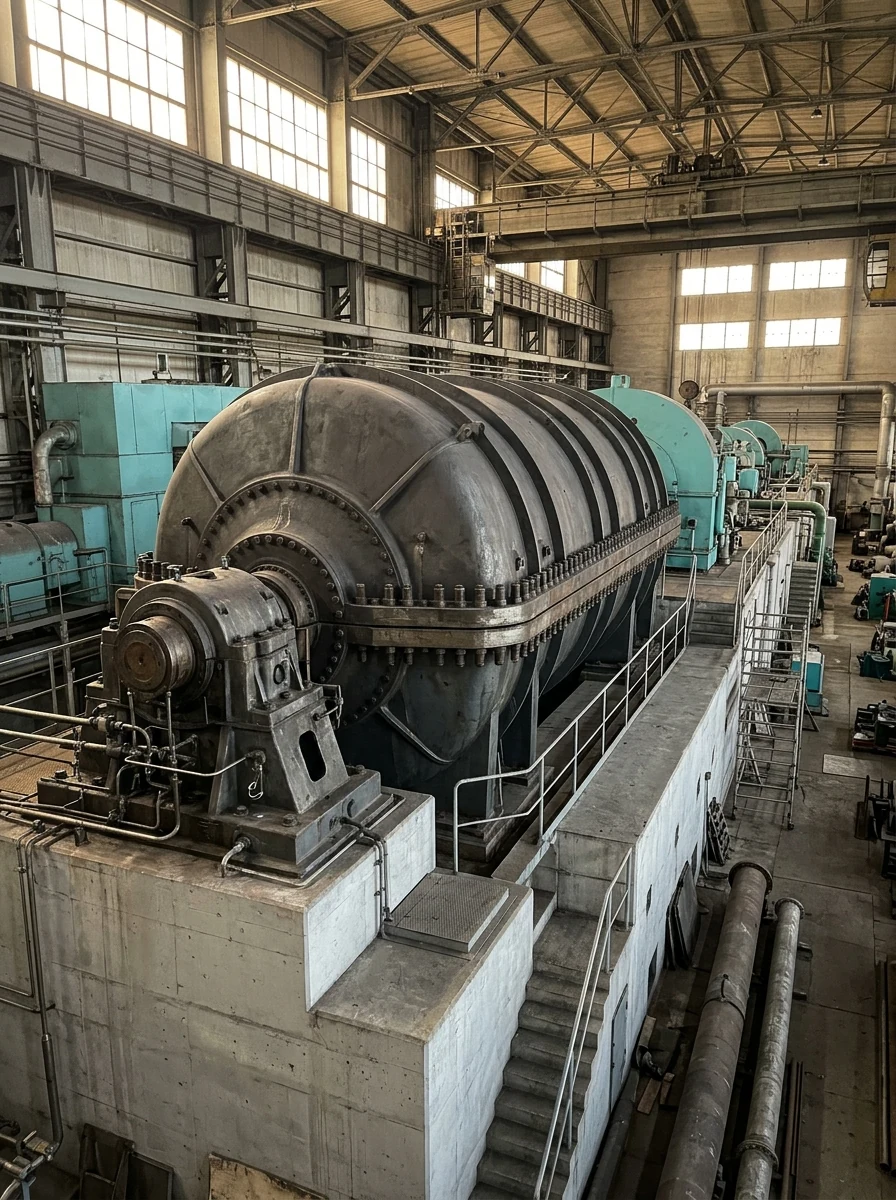
Gas & steam turbine casing joints
Inconel X-750 Stud BoltsA turbine casing stud must carry tension over long hot operating periods and still permit casing access at overhaul. X-750 combines the stud arrangement with precipitation-hardened elevated-temperature properties. Its treatment condition is selected around the actual temperature and load duration of the bolted joint.
Connection requirements
- Casing joint thickness, gasket type, and required preload
- Stud diameter, overall length, and nut engagement at each end
- Temperature range, cycling duty, and heat-number certification
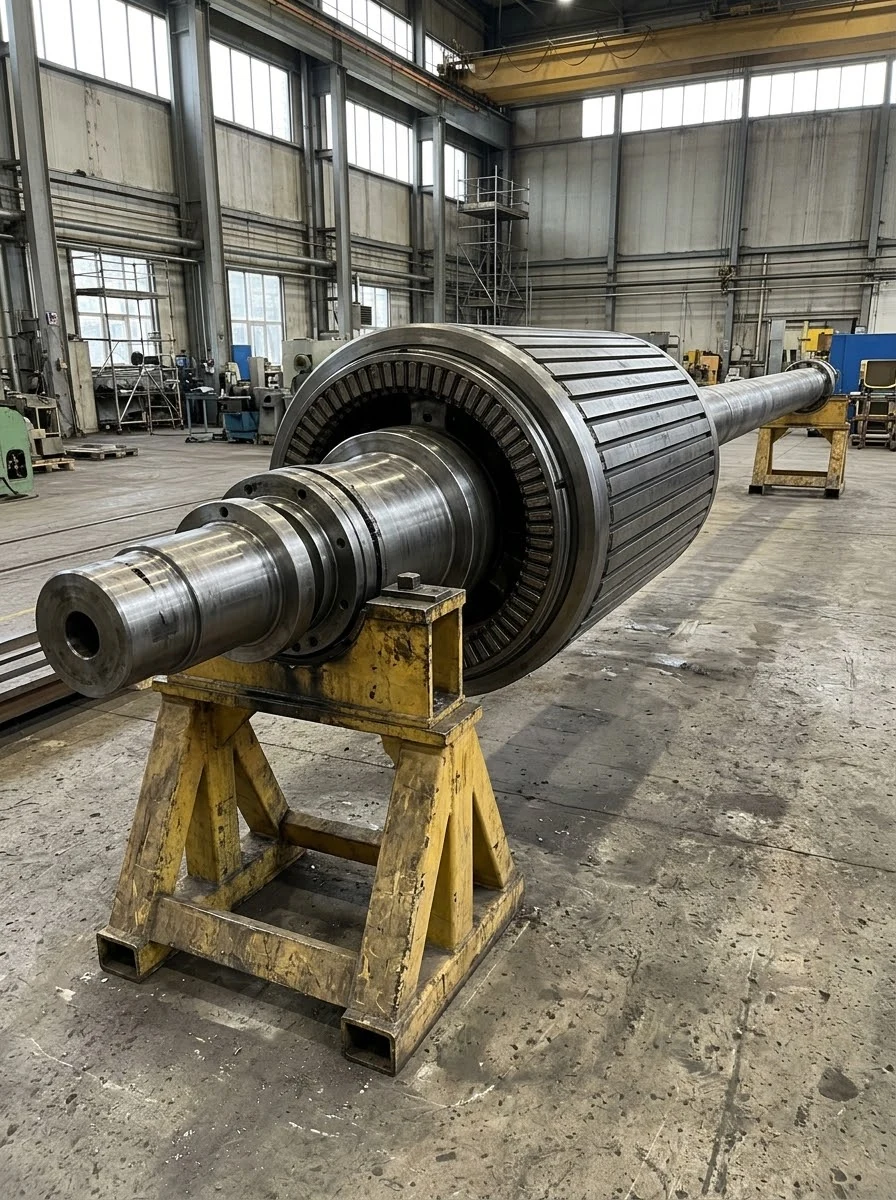
Generator & rotor tie-bolt assemblies
Inconel X-750 Stud BoltsOn generator and rotor tie connections, X-750 studs can serve a sustained axial load path in a heat-resistant alloy. End nuts allow the assembly load to be applied without rotating the stud. These components follow the rotor drawing's end geometry and retention details as well as its material condition.
Connection requirements
- Assembly joint thickness, gasket type, and required preload
- Stud diameter, overall length, and nut engagement at each end
- Temperature range, cyclic duty, and heat-number certification
Same stud. Different material priorities.
Inconel X-750 material dataInconel 718 Stud Bolts
Inconel 718 studs carry high tensile loads in turbine casings and hot valve bonnets where the hole pattern limits fastener size. Precipitation hardening supplies strength, and removable nuts provide service access. Sour-gas connections additionally require the prescribed heat-treatment and hardness condition.
Nimonic 80A Stud Bolts
Nimonic 80A studs carry hot tensile loads at selected valve bonnets, boiler supports and exchanger covers. Precipitation hardening supplies nickel-alloy strength at temperature. Accessible end nuts provide cover removal or support adjustment without requiring the stud itself to turn with every maintenance operation.
Incoloy 800H Stud Bolts
A hot cover can keep its studs in tension for months between shutdowns. Incoloy 800H studs address that sustained load with the controlled-carbon, coarse-grain condition that improves creep and rupture strength over Incoloy 800. They belong in a stud-and-nut assembly designed for the operating temperature and long-duration load, with accessible nuts for cover removal.
From drawing to documented delivery
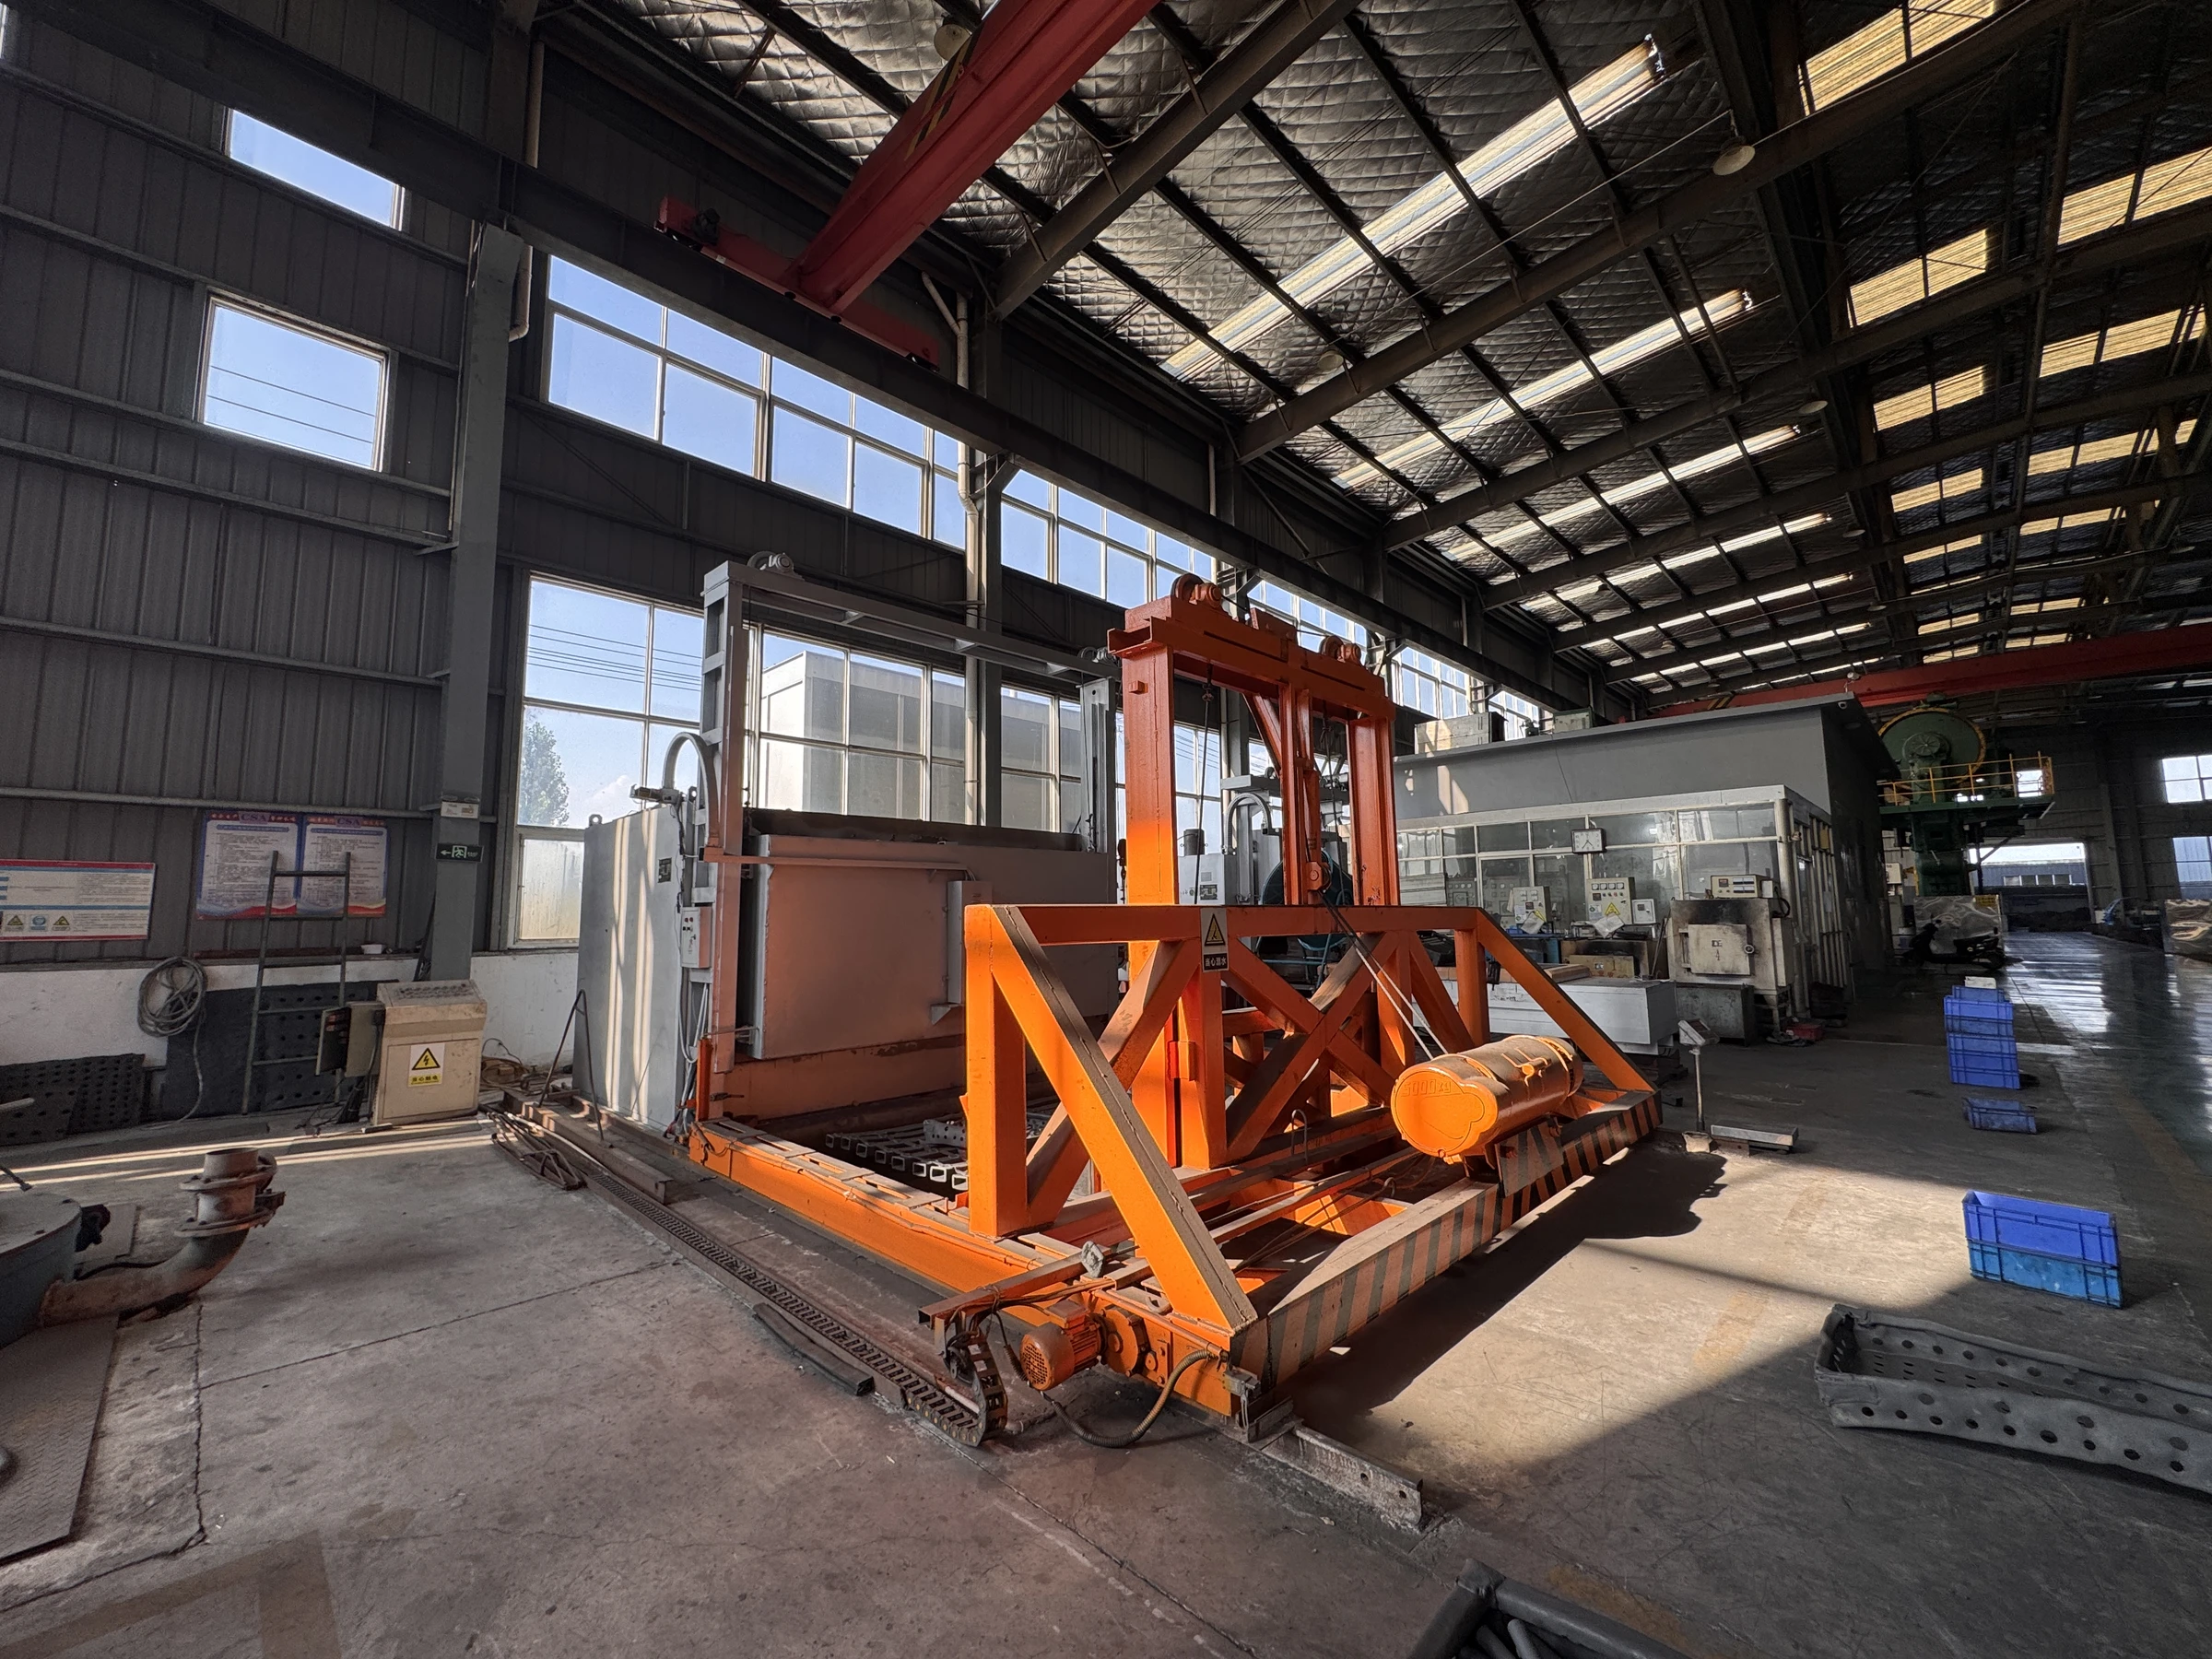
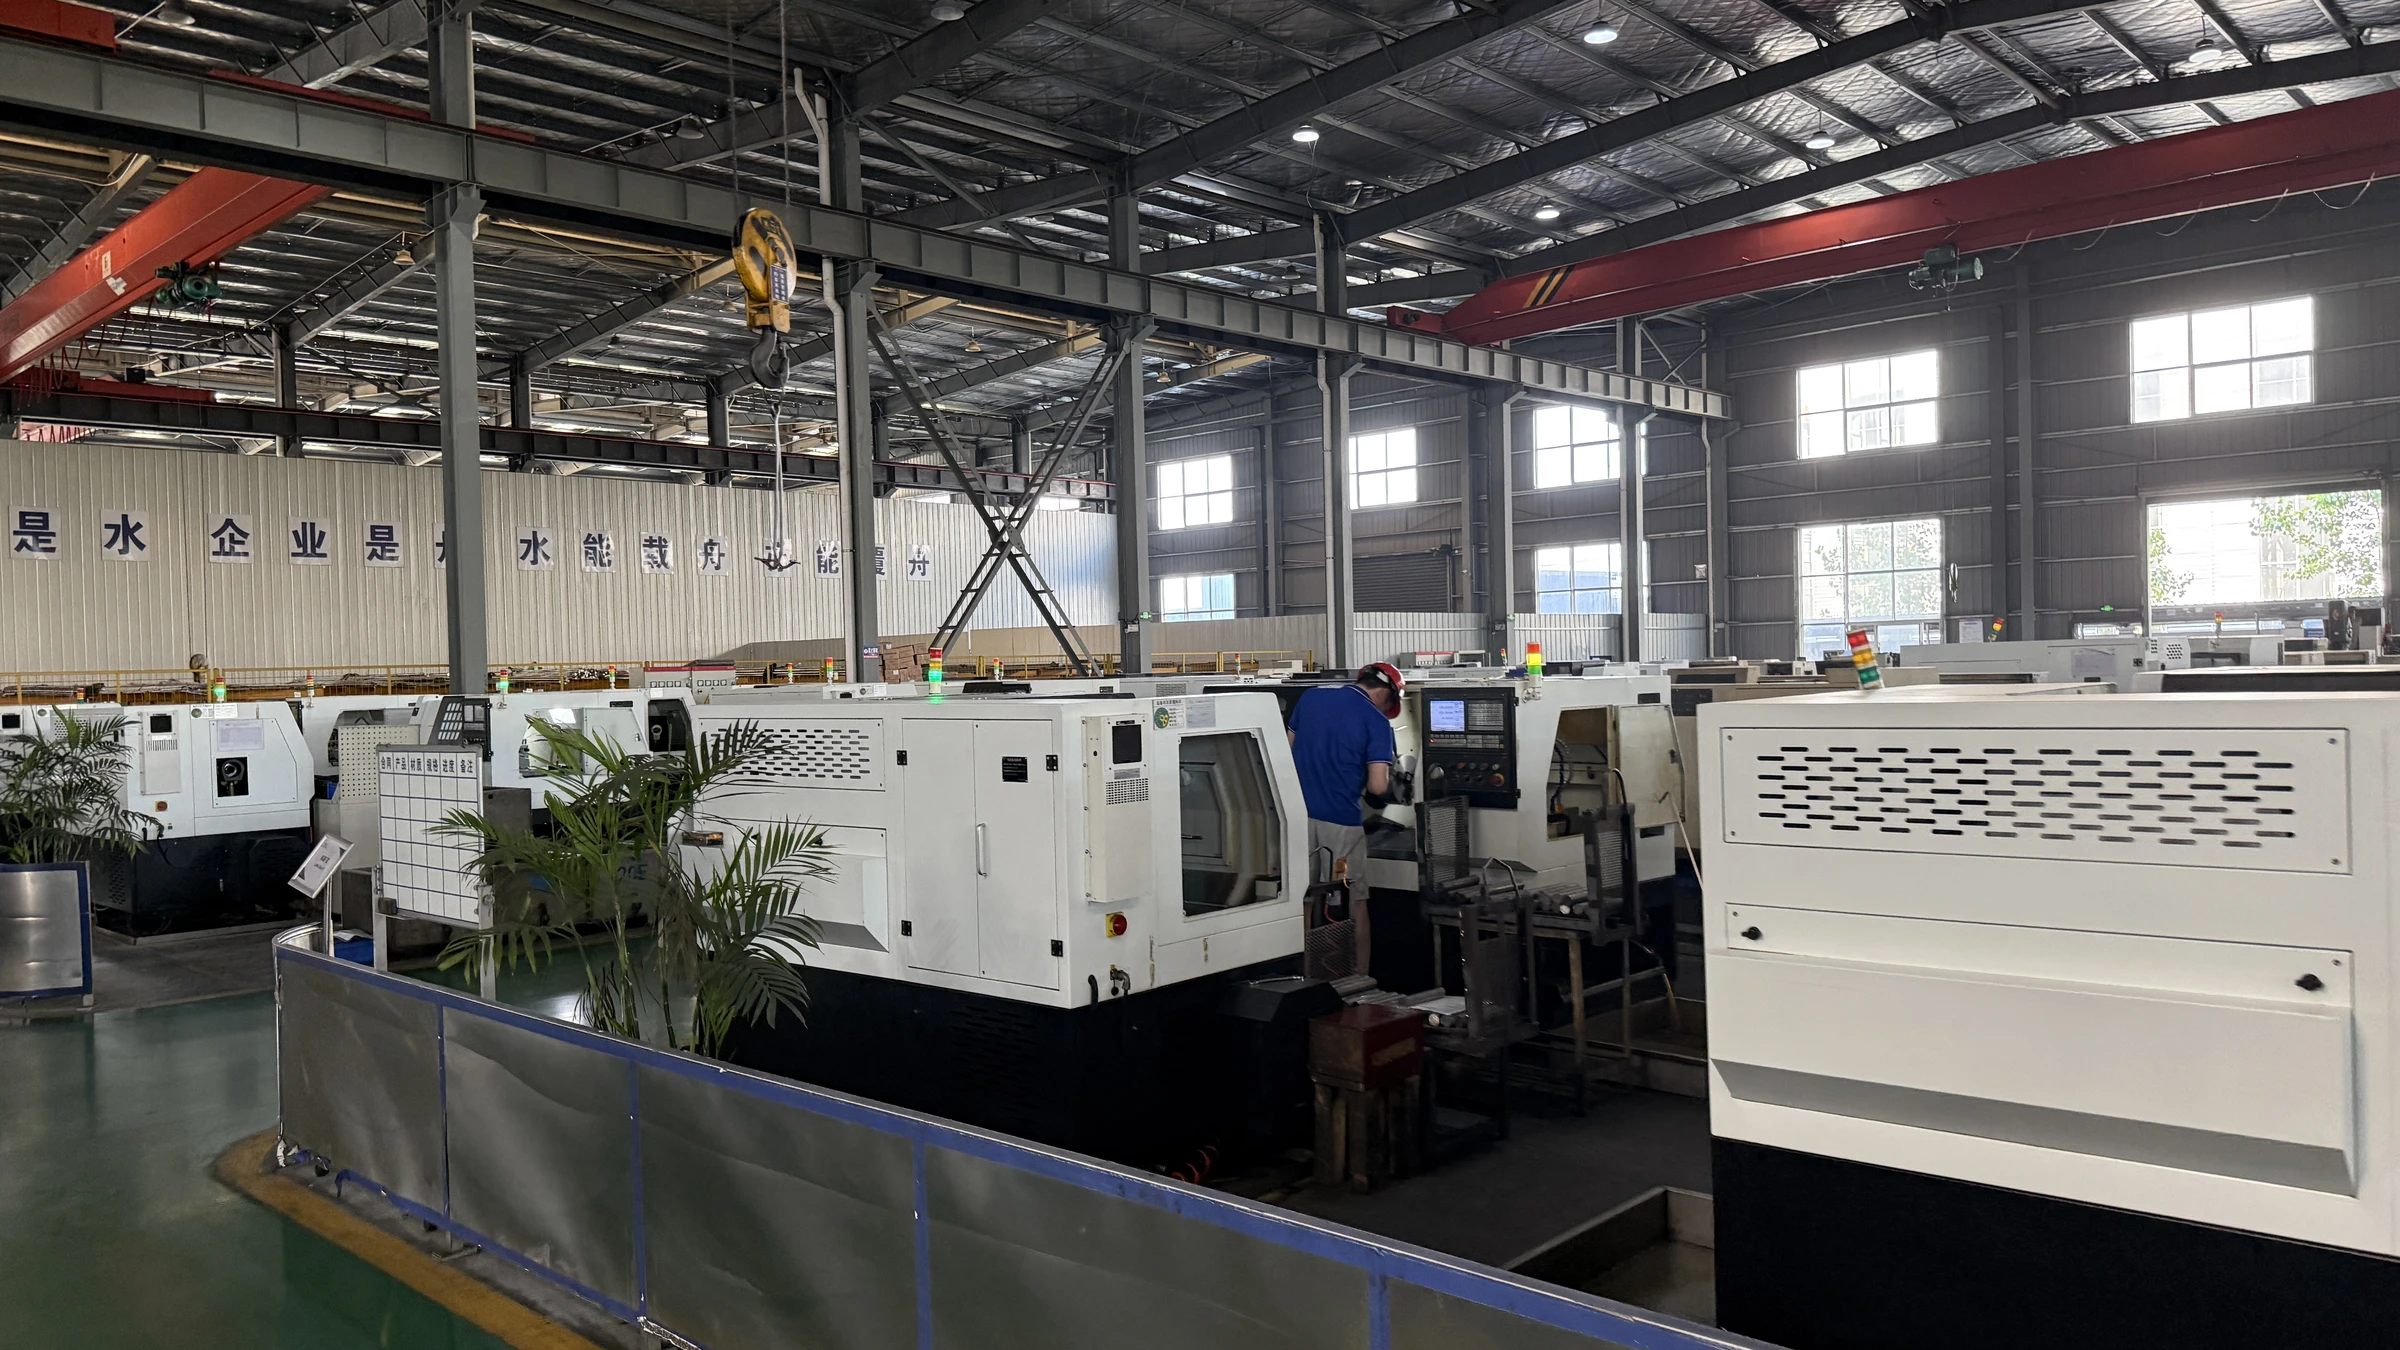
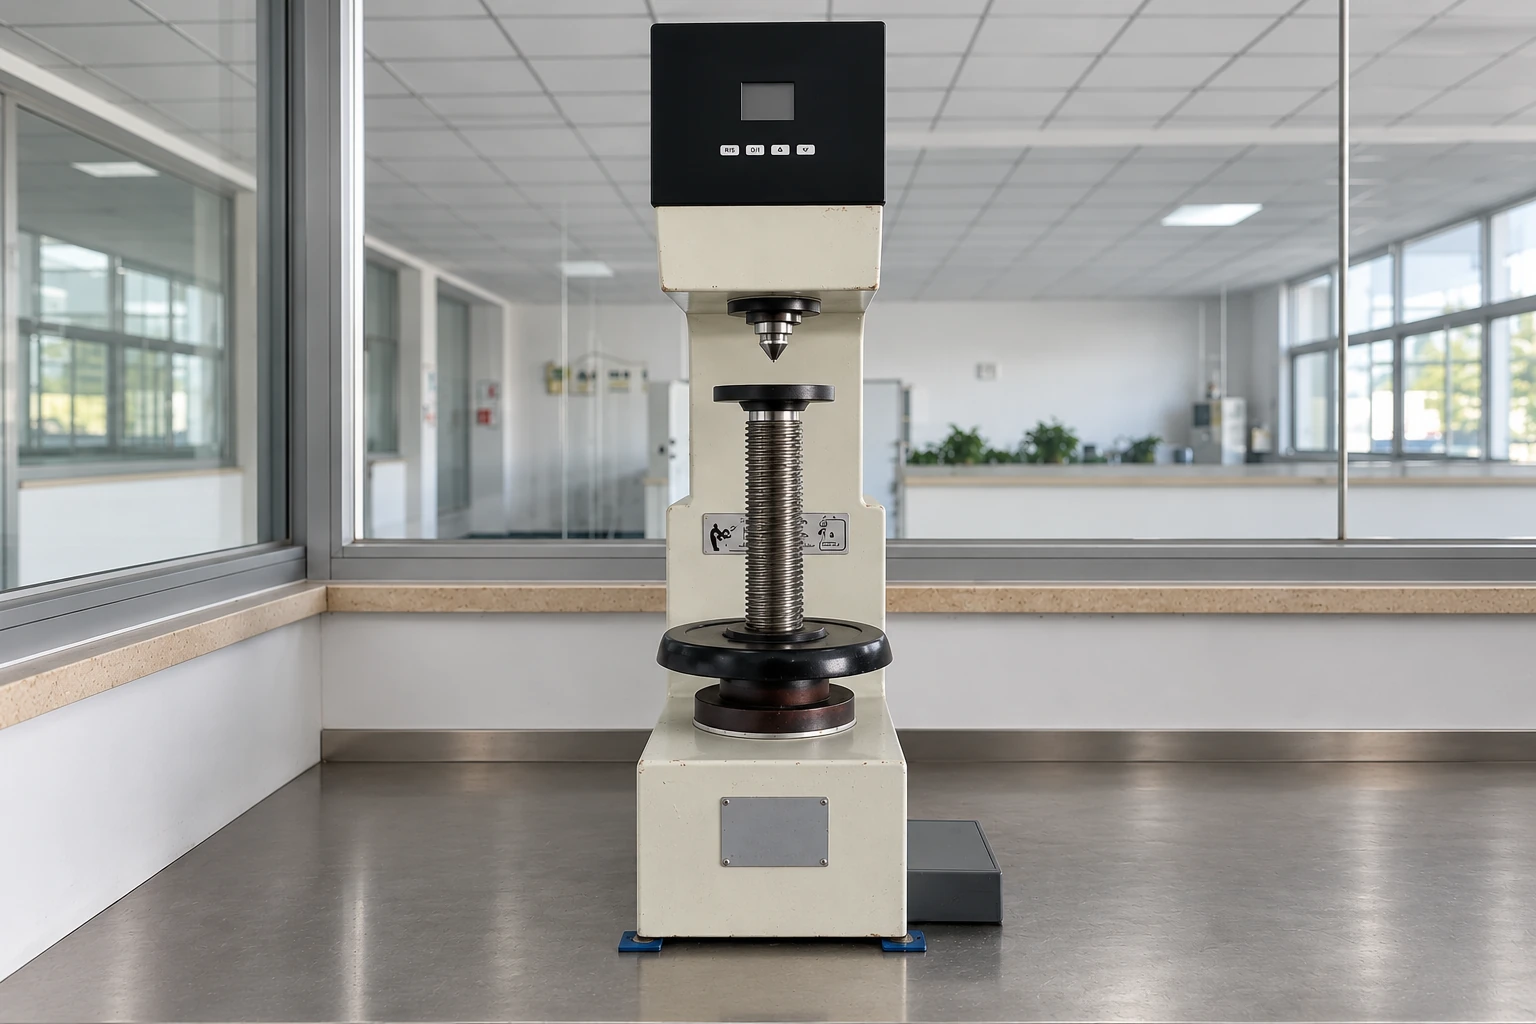
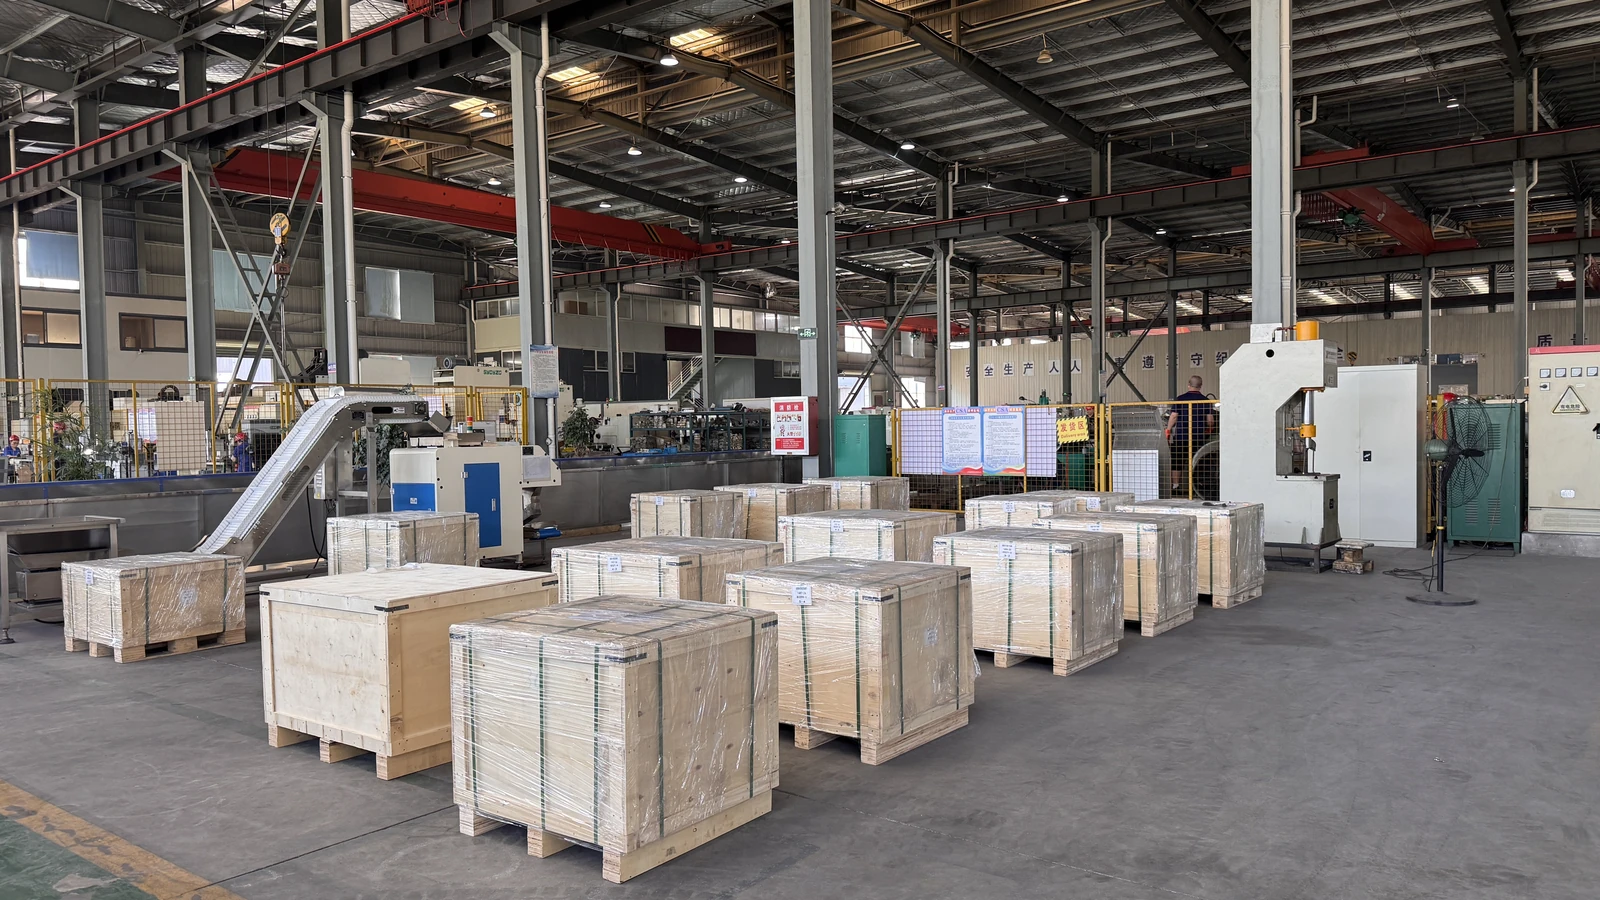
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N07750 · heat number · ordered condition
- Final-part acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Matching Kit
Flange Stud Bolt Kits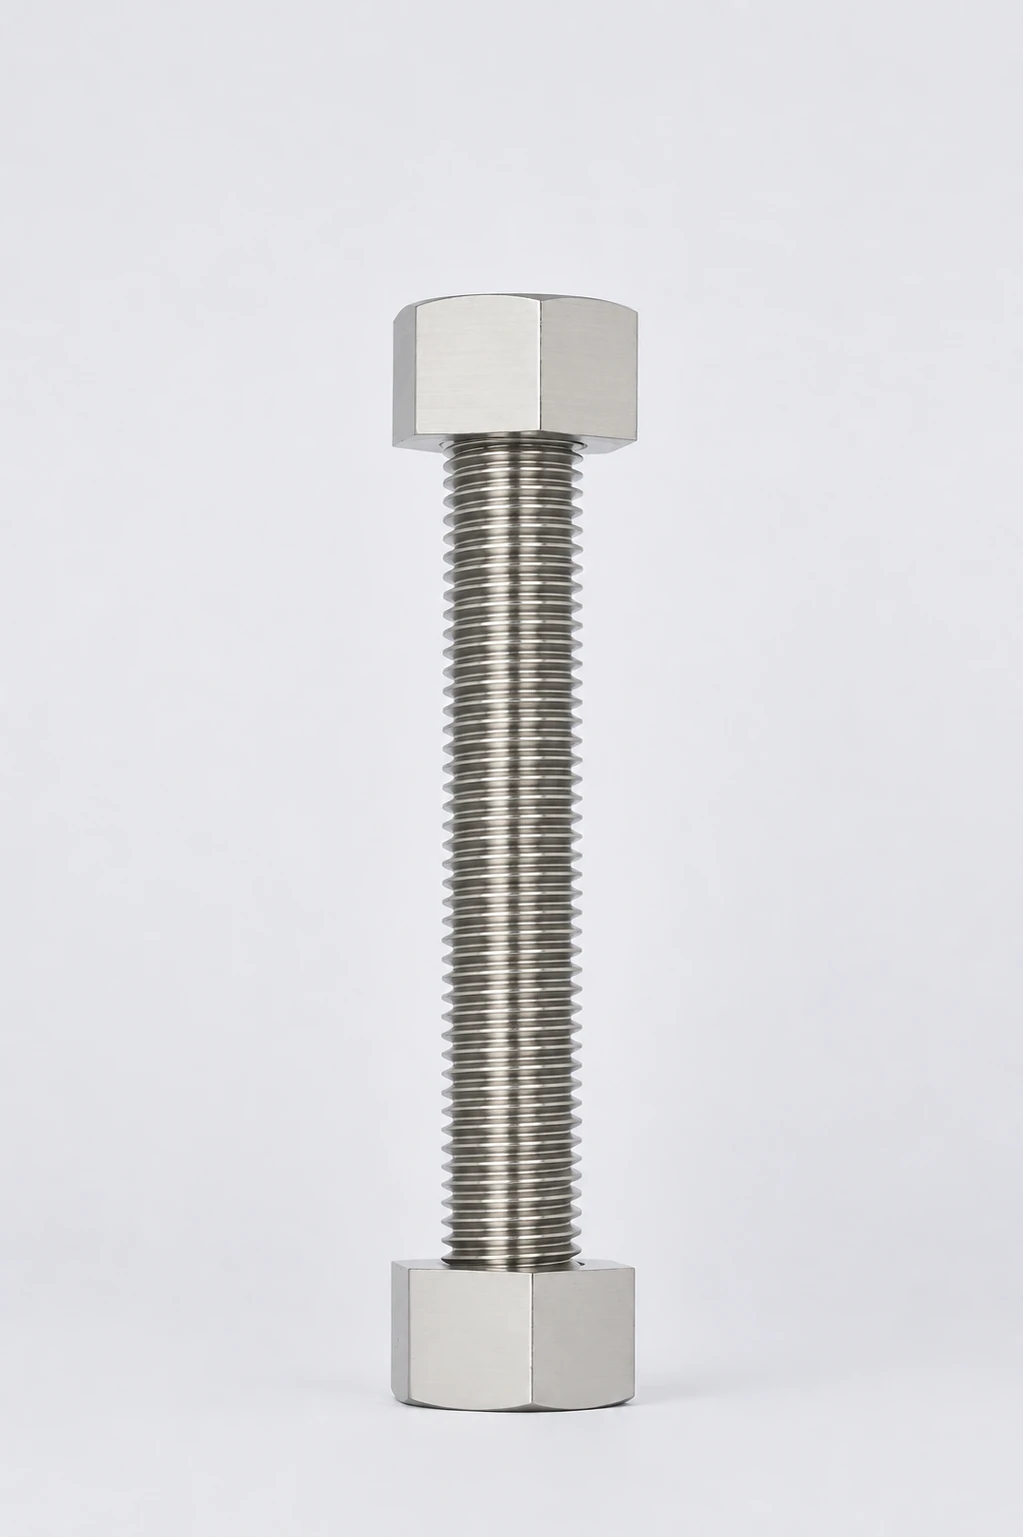
Build your X-750 stud enquiry
Questions about X-750 stud bolts & threaded rods
Does changing the stud alloy also change the nut selection?
The nut needs compatible internal threads, sufficient engaged height and a specified material condition. Select lubricant or surface treatment with the stud–nut pair, because assembly friction affects the preload obtained from tightening.