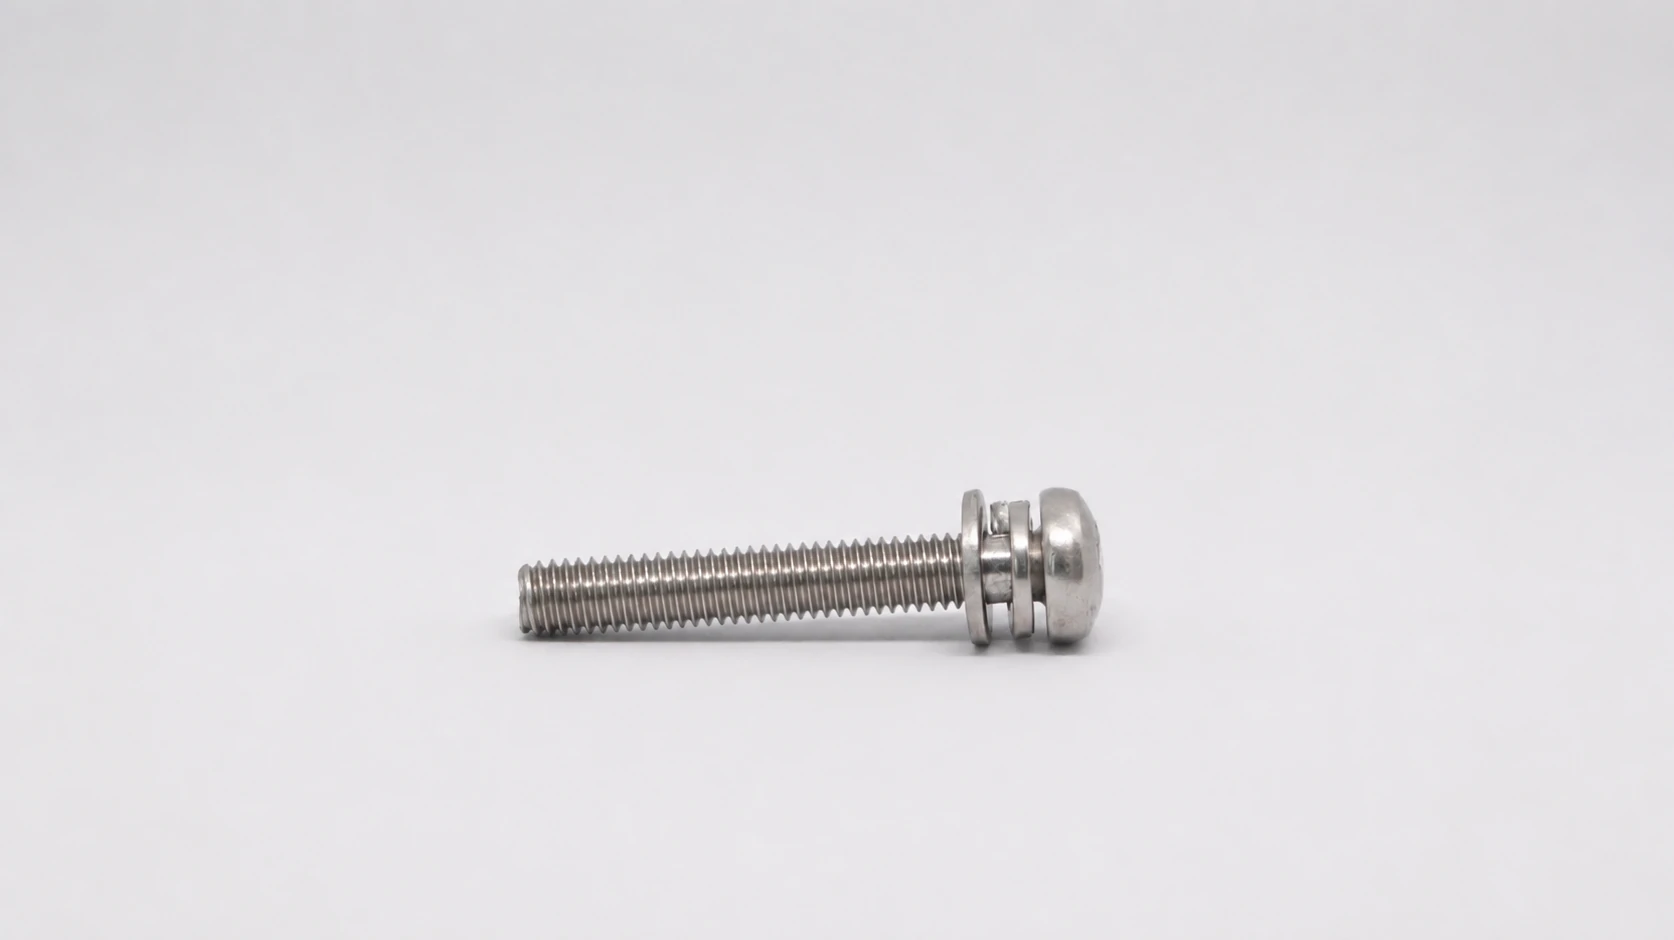
Special alloy phillips pan head screws
For covers and guards that allow a projecting head, pan-head machine screws retain a flat bearing seat without a countersink. Match the Phillips recess to the assembly tooling, and select thread engagement and alloy for the panel and mating component.
- Drive
- Type H cross recess
- Head
- Pan head
- Length basis
- Under head
- Thread
- Machine screw thread
- Materials
- Nickel alloys · Stainless steels · Titanium
EN 10204 3.1 MTC · Heat traceability
Phillips pan head screws material selection
Equipment & applications
Packaging machinery
Attach guards and access covers to packaging-machine frames. The pan head bears on a flat panel, avoiding a countersink in thin sheet.
Robot peripherals
Secure small covers and cable-retaining brackets on robot peripherals. A Phillips driver approaches from the front and the broad head bears above the mounting hole.
Assembly tooling
Mount labels, light guards and removable covers on assembly tooling. Machine threads engage a tapped bracket or captive nut for repeated access.
Phillips pan head screws configurations & dimensions
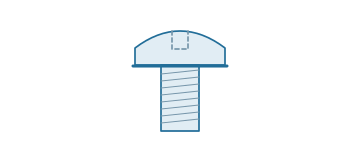
Pan head
Use for panels and covers that can accept a projecting head, avoiding a countersink in thin sheet. The flat underside needs sufficient seat area around the clearance hole.
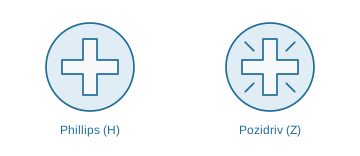
Phillips drive
Use a matching Phillips type H driver for service and assembly tools. A Pozidriv type Z bit is not the same fit; mismatched recess engagement increases cam-out and head damage.
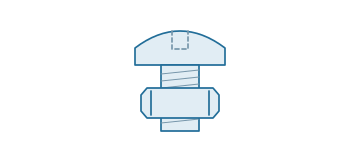
Machine screw
Use with a tapped boss, nut or threaded insert in equipment panels. Match screw length to the available engagement so a blind hole does not stop the screw before the cover is clamped.
Dimension guide
Loading 3D model…
Drag to rotate · Scroll to zoom
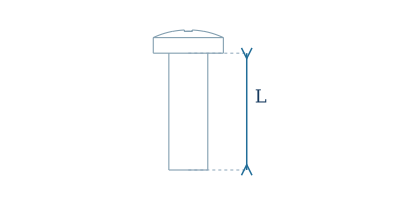
Product and thread standards
Raw Material Specifications
Other Materials & Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Production & heat treatment
CNC · Samples & Special Lengths
Machining suits small quantities, unusual shanks and non-standard lengths. The pan profile and flat bearing seat are produced before finishing the cross recess.
Drive & Machine Threads
The Phillips recess is formed and checked with the matching driver geometry. Threads are rolled for repeat sizes or cut for short runs, with burr removal around the recess and thread entry.
Cold Heading / Hot Forming
Small pan heads usually favour cold heading: the head and recess can be formed efficiently in repeat strokes with ductile feedstock. Hot forming is useful for oversized or high-resistance alloy blanks, followed by machining of the small drive details.
Heat Treatment & Recess Integrity
Inconel 625 annealing restores ductility after heading. Inconel 718 solution treatment and ageing increase resistance to permanent deformation in the head and threaded section. Final checks include recess engagement so the driver can transmit tightening torque without shallow contact.
Testing, MTC 3.1 & material traceability
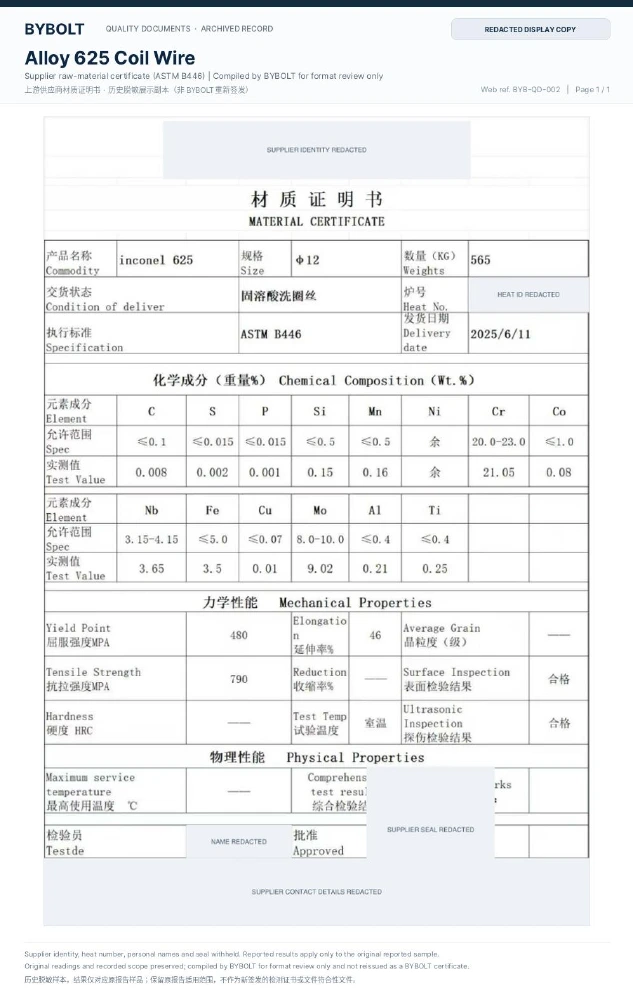
Material certificate
Inconel 625 · historical coil-wire sample
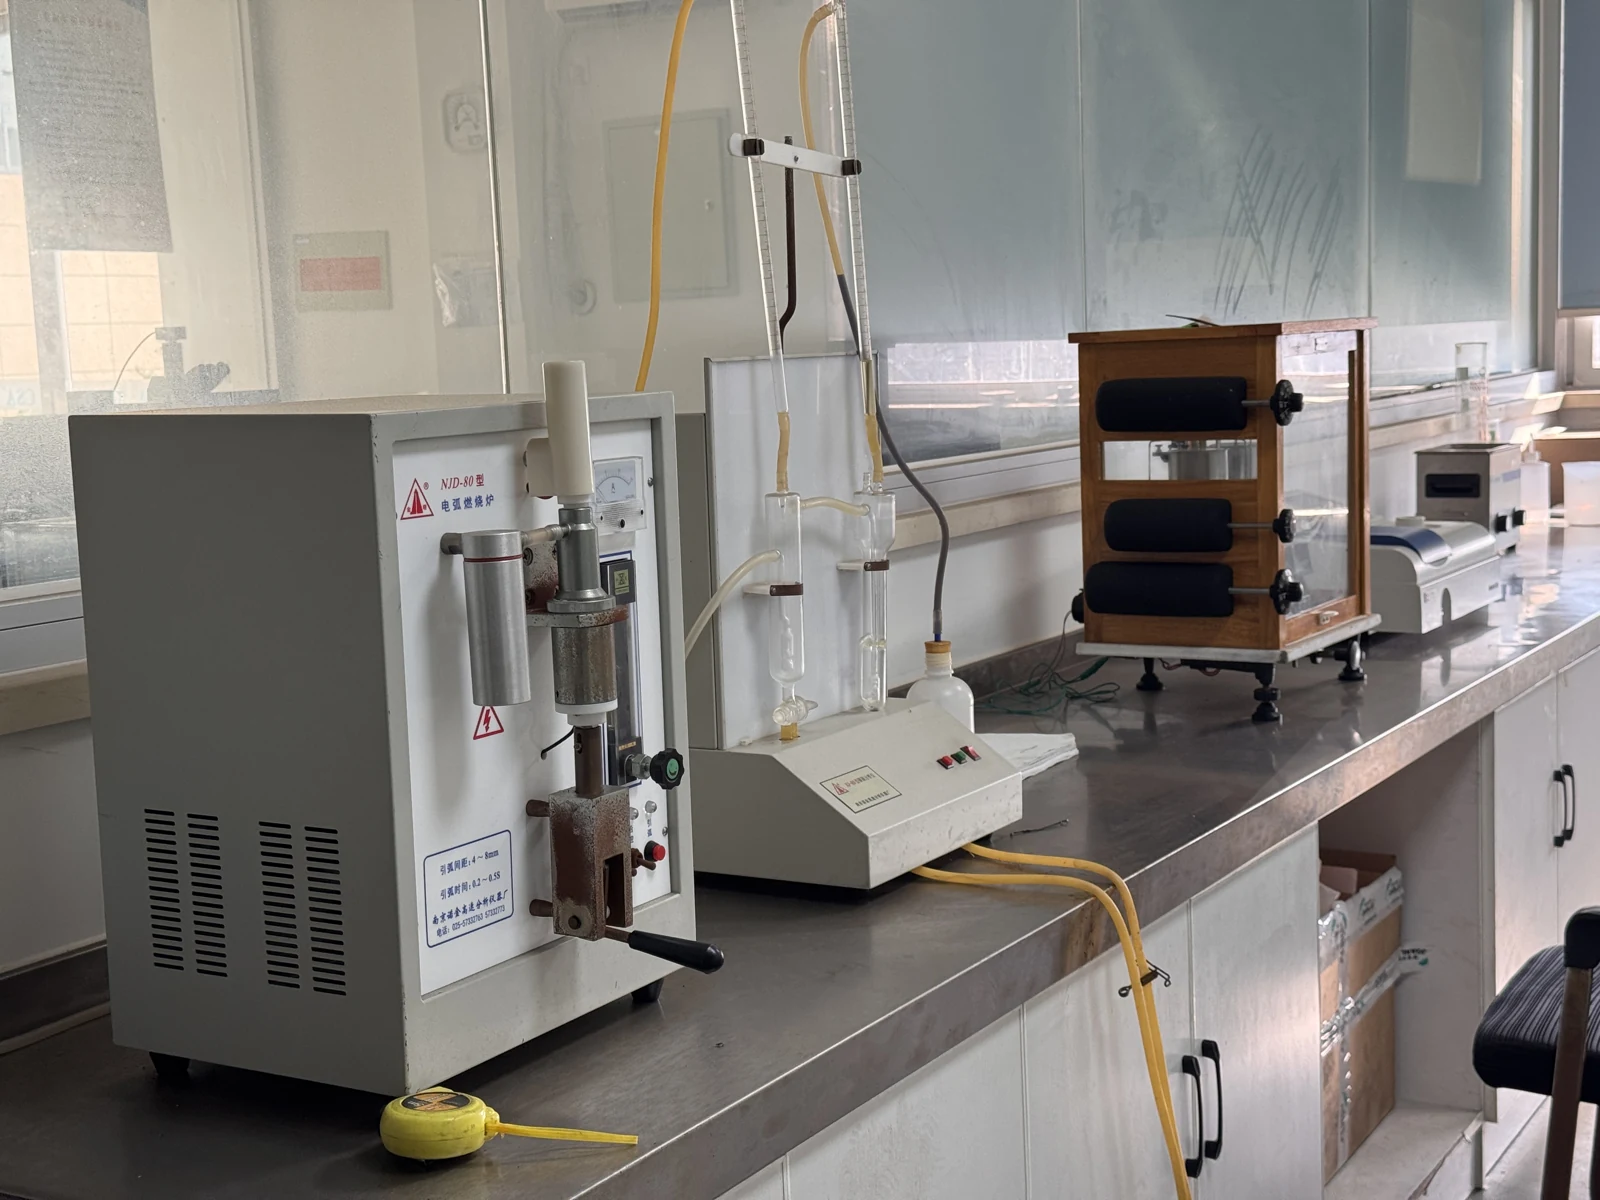
Laboratory report
Inconel 718 · chemistry, tensile & hardness
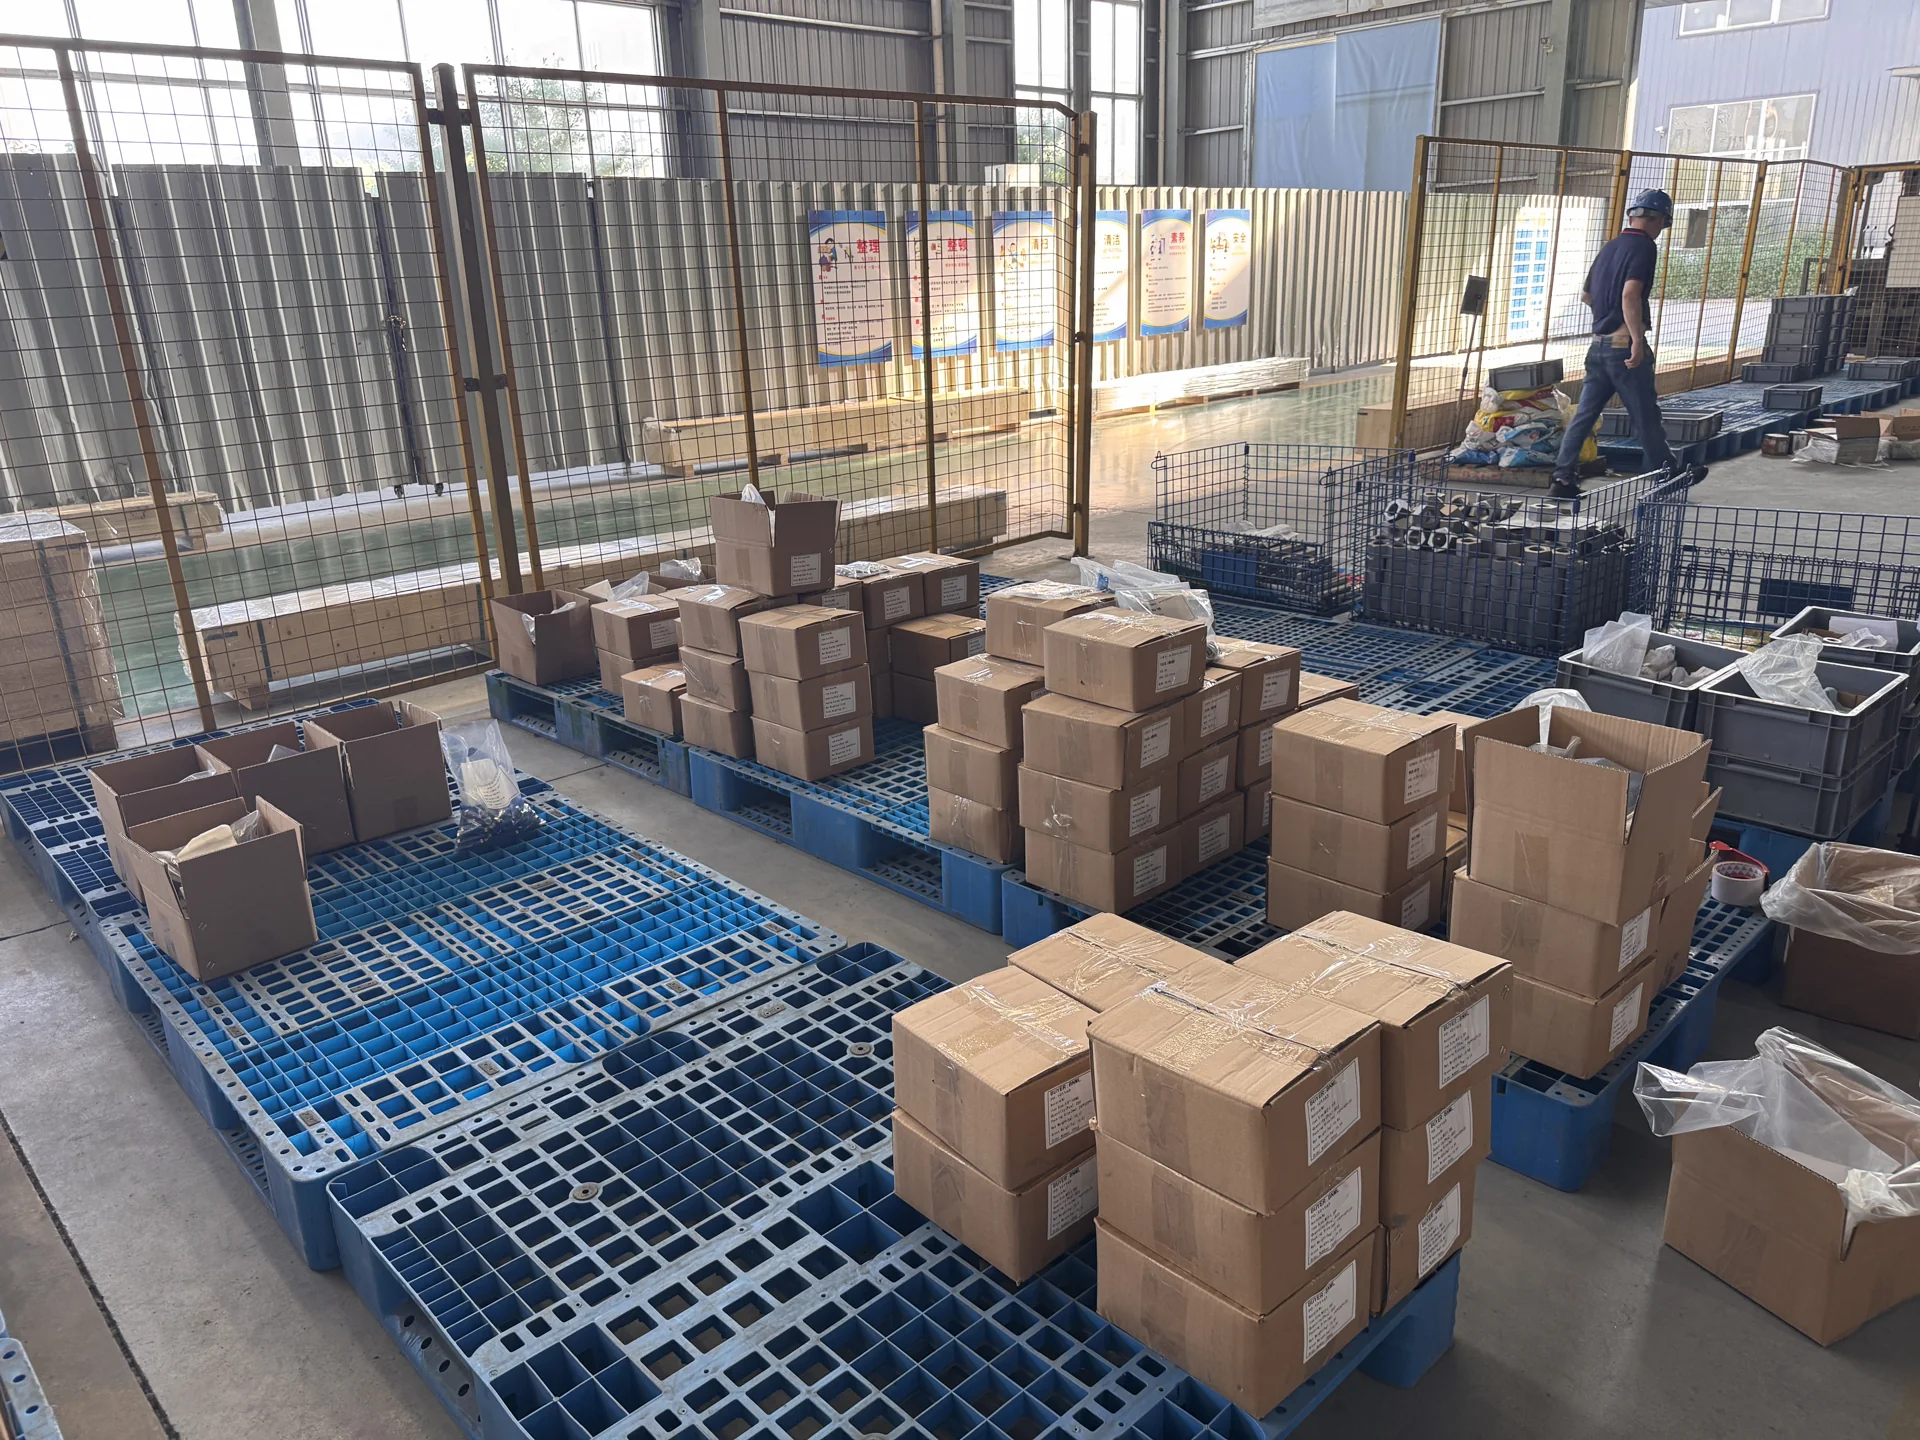
Identified packing
Heat and batch records linked to the shipment
Additional inspection requirements +
PMI, third-party inspection and witness testing are available by order. Project inspection plans can include UT/PT and heat-treatment records.
Matching products for phillips pan head screws
Prepare your enquiry
- Material
- Grade / UNS · Condition
- Size
- Diameter · Length / height
- Thread
- Pitch / TPI · Form & class
- Quantity
- Pieces per size