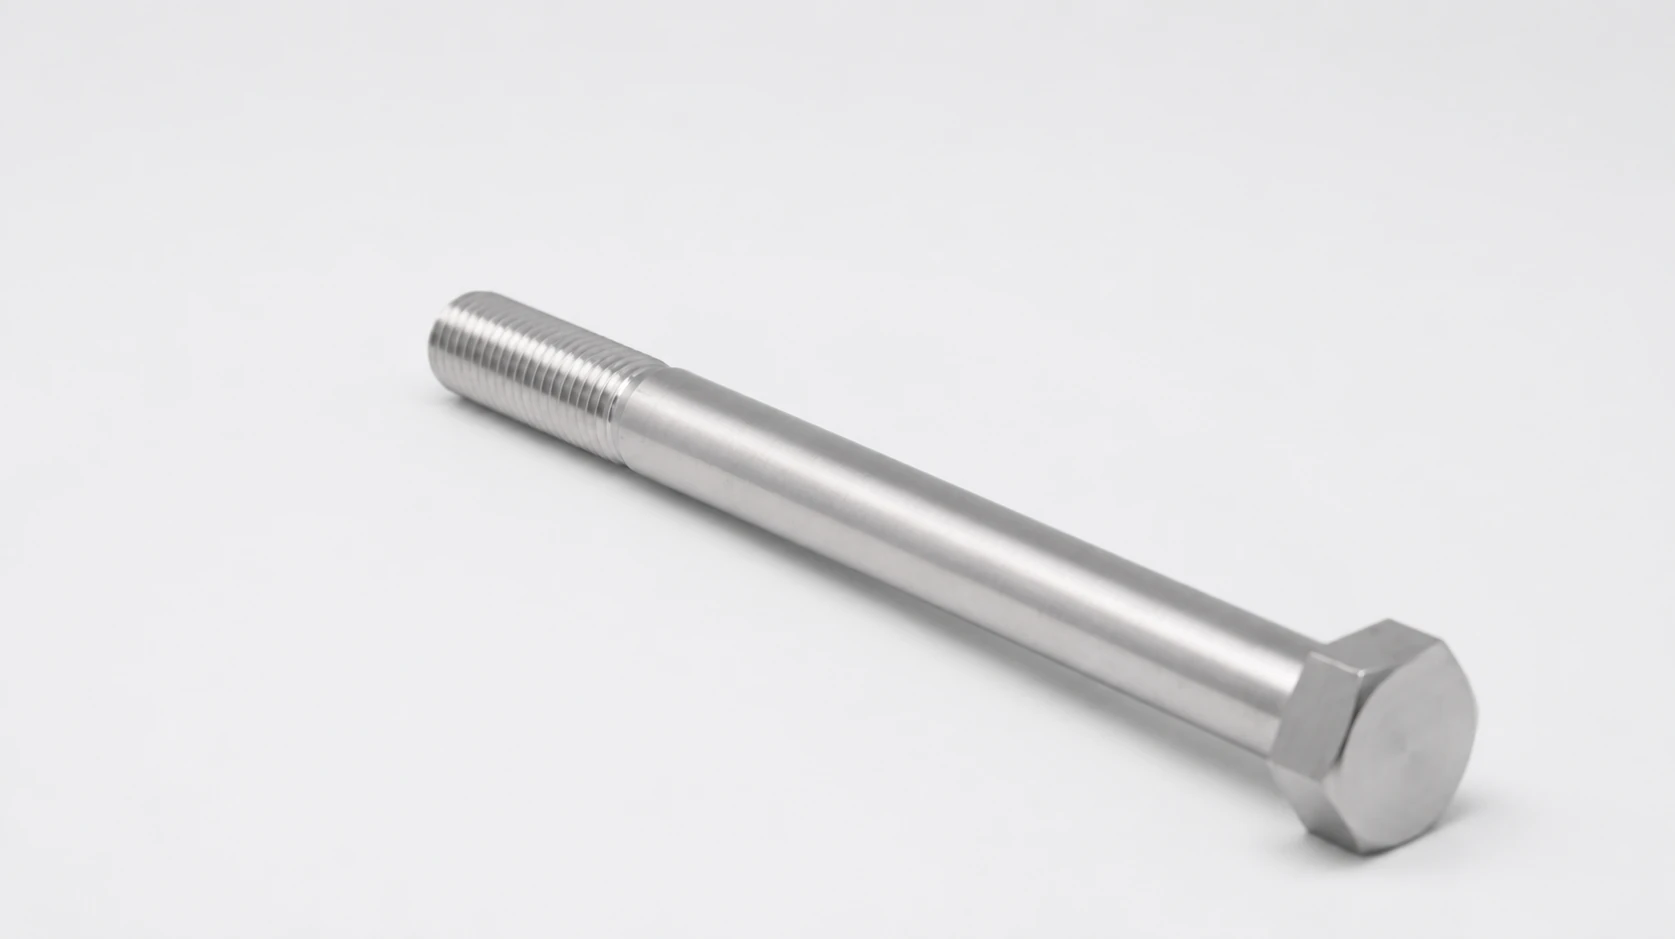
Special alloy long-shank hex head bolts
Thick joints need the plain shank and threaded end positioned around the actual grip stack. Long-shank hex bolts suit these assemblies; where the shank also locates a component, its diameter and fit need separate drawing control.
- Head
- External hex
- Shank
- Extended plain length
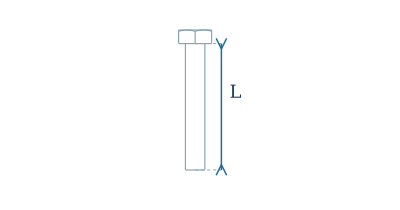
- Length basis
- Under head
- Threads
- Metric · UNC · UNF · UNJ
- Materials
- Nickel alloys · Duplex steels · Titanium
EN 10204 3.1 MTC · Heat traceability
Long-shank hex head bolts material selection
Equipment & applications
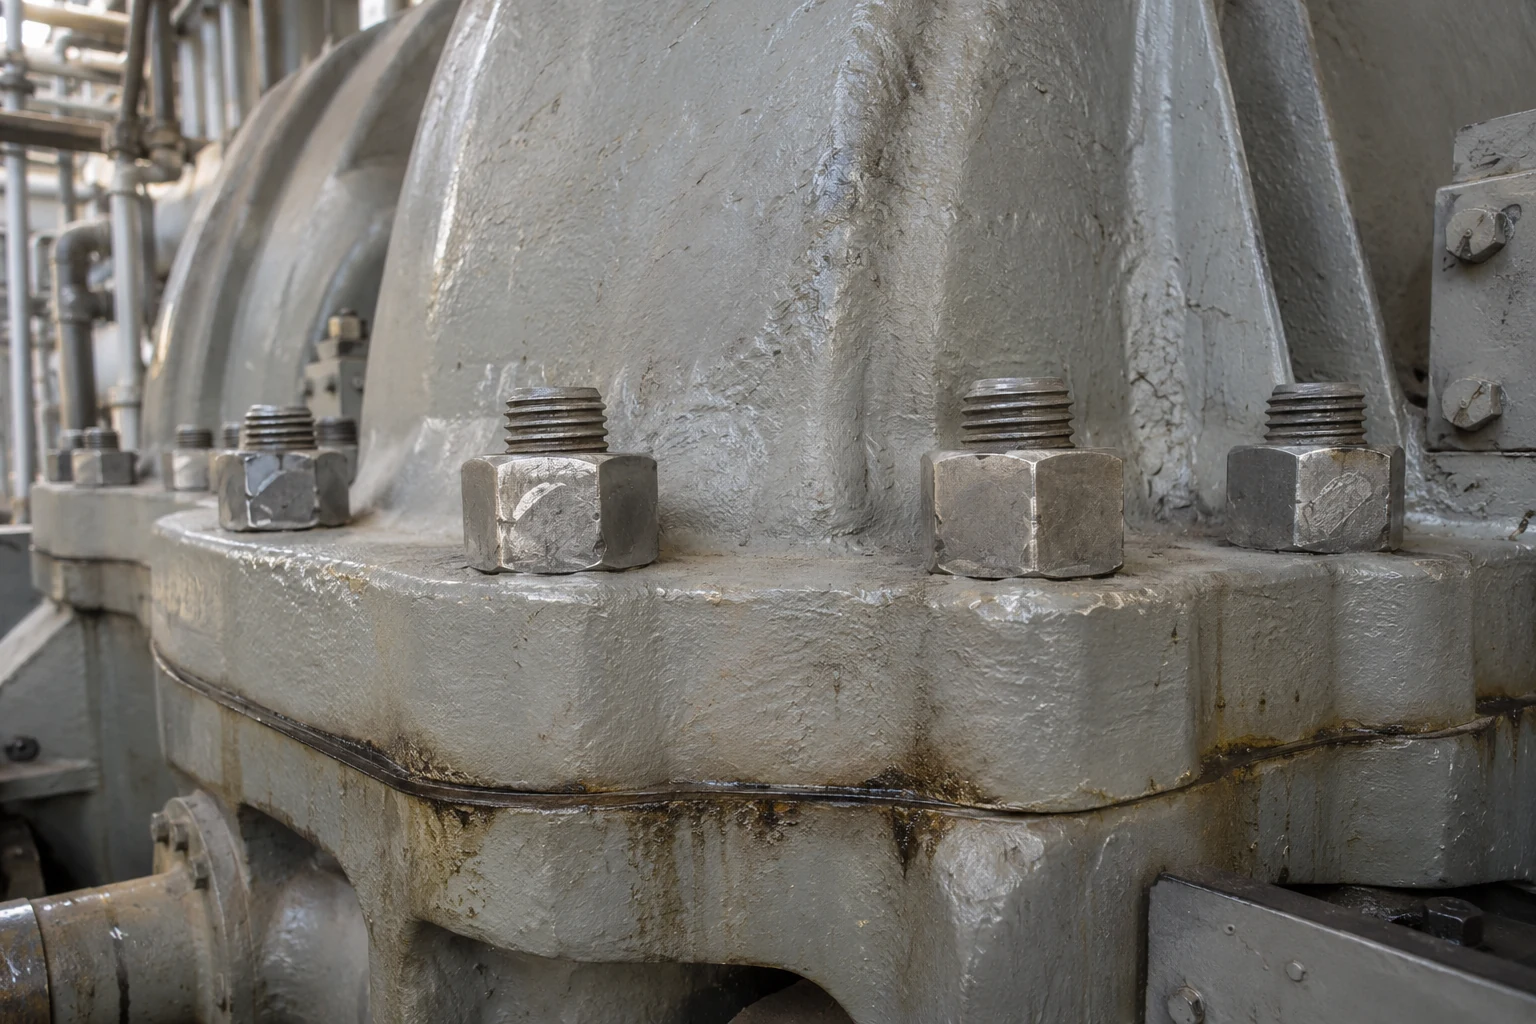
Turbine-casing joints
Span thick casing flanges with a continuous plain grip. The threaded end sits beyond the casing stack, leaving the shank through the joint instead of a thread run-out.
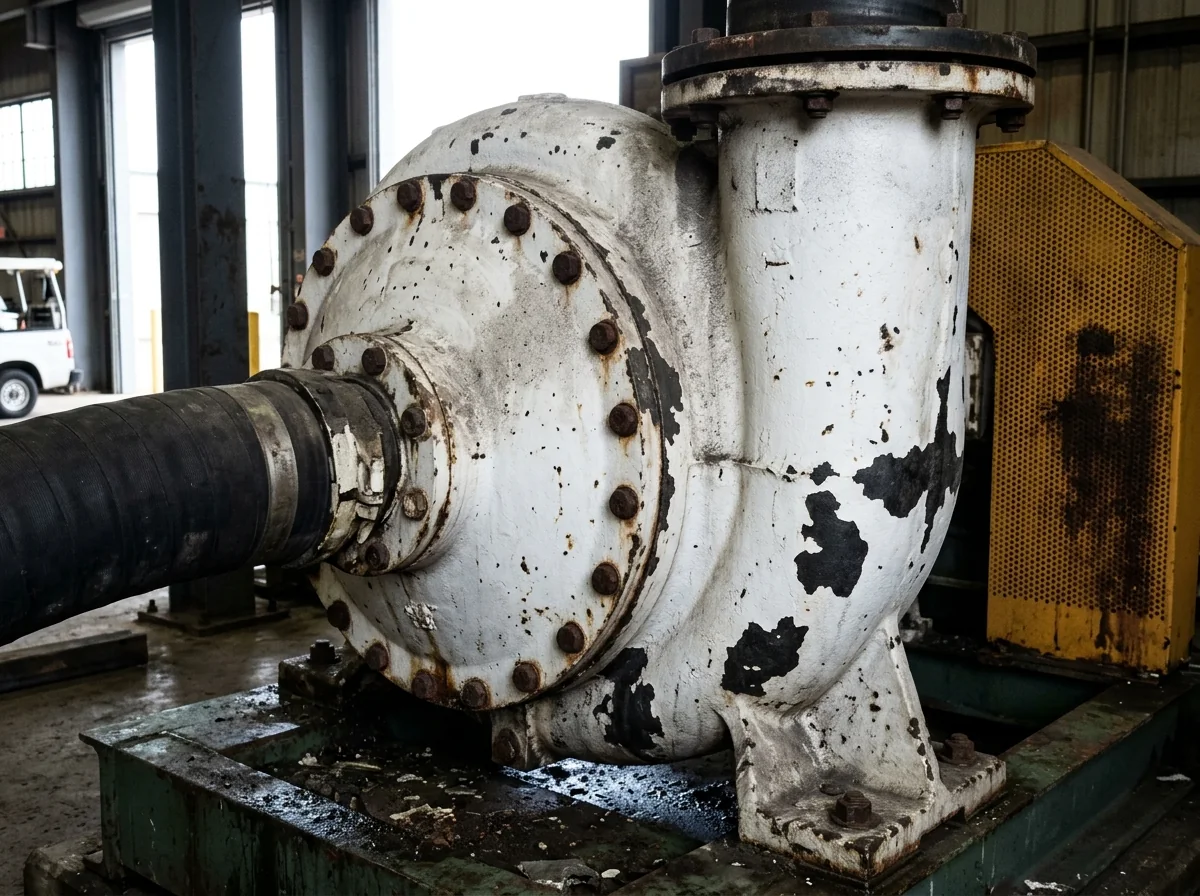
Pump casings
Clamp deep pump housings and spaced cover assemblies. A long plain shank crosses the housing, while the hex head remains accessible for servicing.
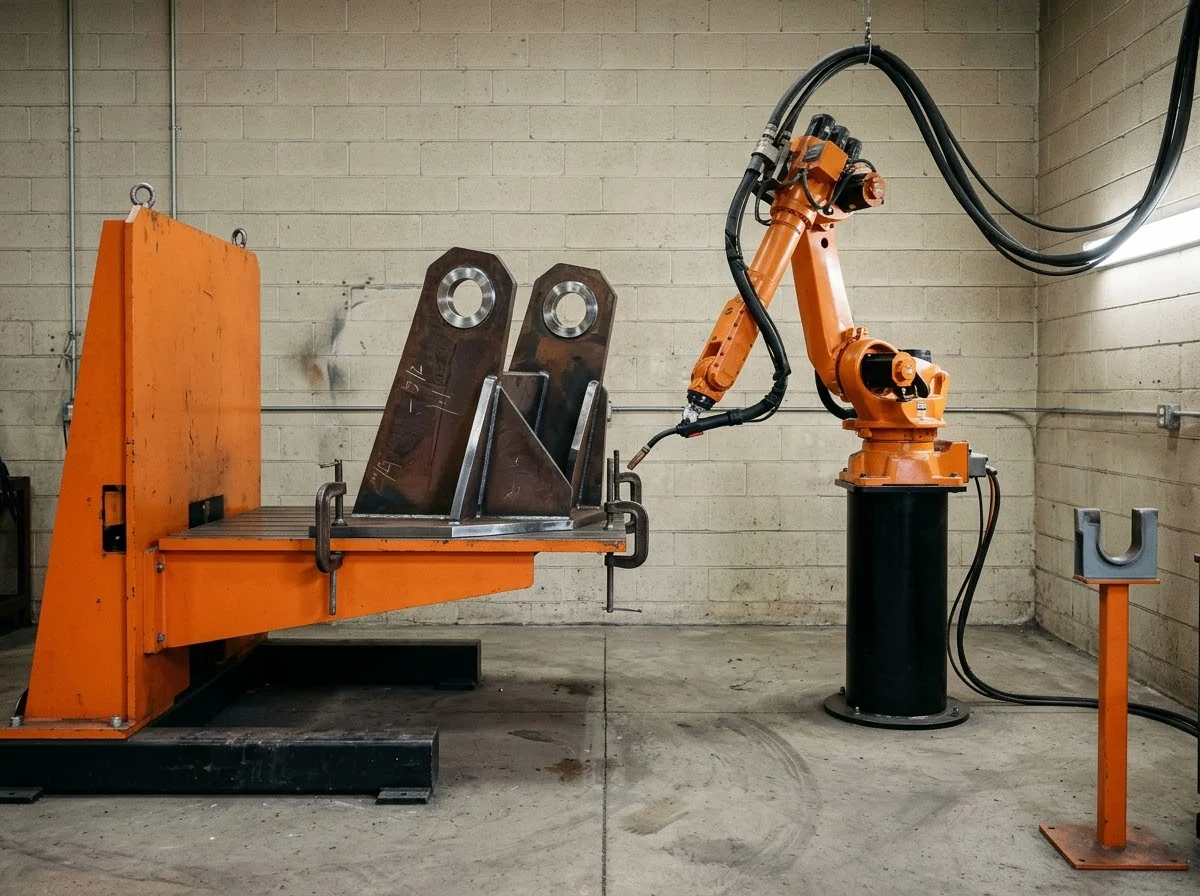
Assembly fixtures
Secure tall fixtures and spacer stacks to a base. Grip length positions the threads beyond the stack, and the head can be held with a spanner during nut tightening.
Long-shank hex head bolts configurations & dimensions
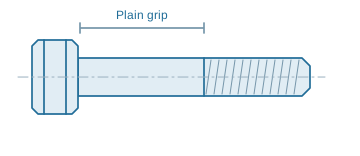
Plain grip section
Use across thick equipment flanges, spacers and mounting stacks where the grip requires a continuous plain shank. The grip length keeps the threaded transition beyond the intended bearing or shear section.
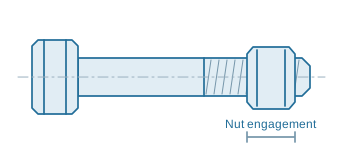
Threaded end
Allow enough usable thread beyond the stack for the nut, washer and tightening travel. Too little thread can leave the nut bottomed on the plain shank before the joint is clamped.
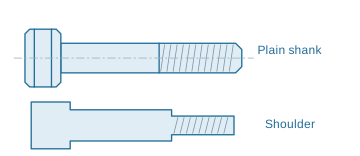
Long shank vs shoulder screw
For a pivot or locating bore, specify the actual shank diameter tolerance and surface finish. A long-shank bolt provides grip length; a shoulder-screw fit requires separate control of the locating surface.
Dimension guide
Loading 3D model…
Drag to rotate · Scroll to zoom
Product and thread standards
Raw Material Specifications
Other Materials & Specifications
Finished-Bolt Specifications
Other Materials & Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Production & heat treatment
CNC · Long Grip Sections
Short-run blanks are turned with support along the extended shank to control straightness. The shoulder-to-thread transition is placed beyond the measured joint grip.
Threading & Run-Out
The end thread is rolled or cut while retaining the plain grip. Thread length includes the nut engagement and projection, without allowing the nut to bottom on the thread run-out.
Cold Heading / Hot Upsetting
Small, ductile long-shank bolts can be headed cold in repeat runs with the shank supported against buckling. Large heads or resistant nickel alloys favour heating the head-forming zone before upsetting, reducing the load applied through the long blank.
Heat Treatment & Straightness
Inconel 718 ageing develops strength after solution treatment; annealing of cold-worked Inconel 625 restores ductility. Long shanks are checked for straightness after heating so the bolt can pass through the complete housing stack.
Testing, MTC 3.1 & material traceability
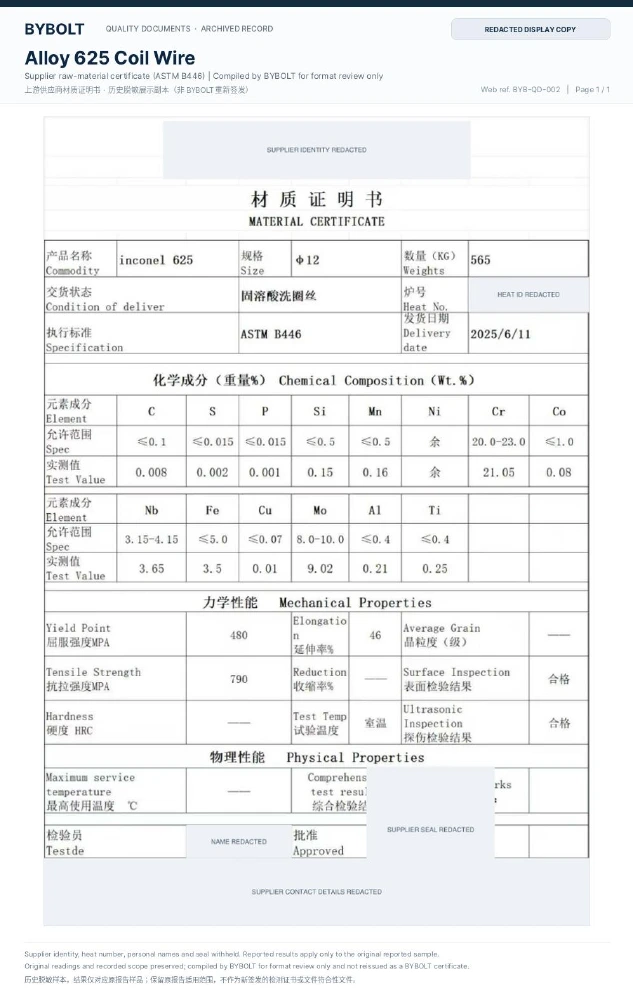
Material certificate
Inconel 625 · historical coil-wire sample
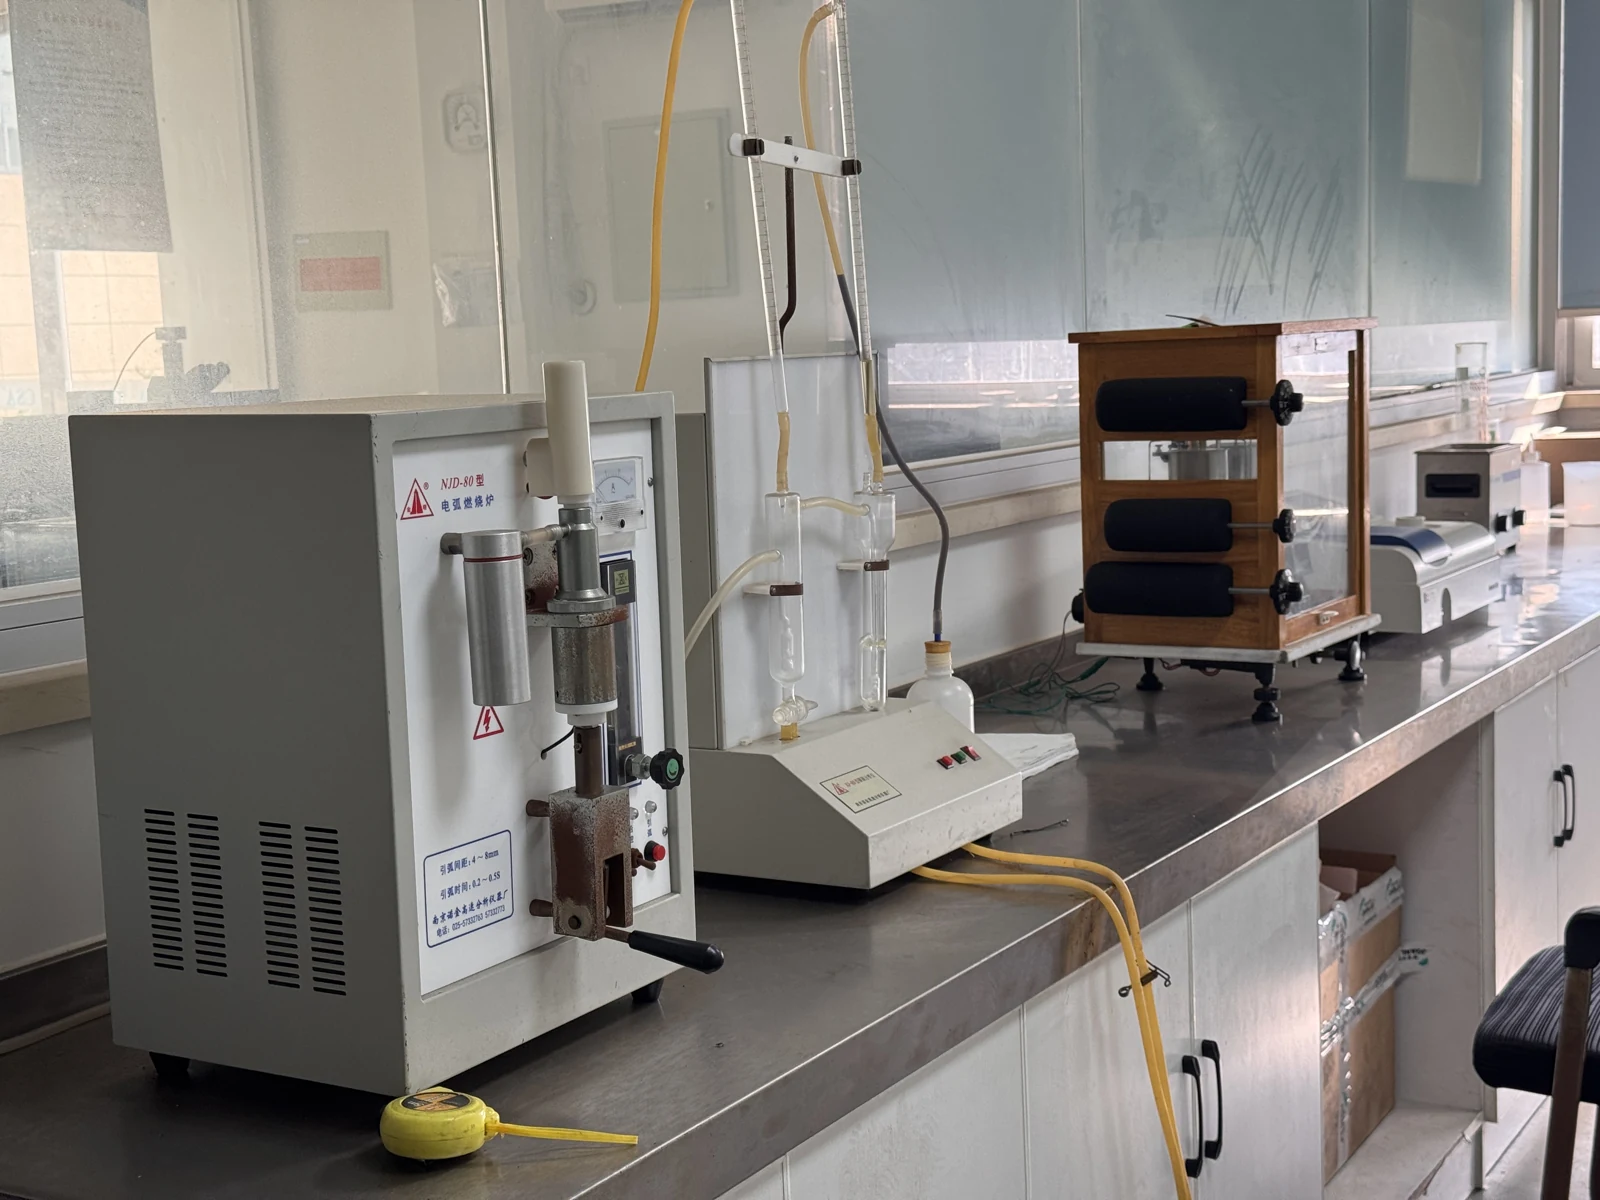
Laboratory report
Inconel 718 · chemistry, tensile & hardness
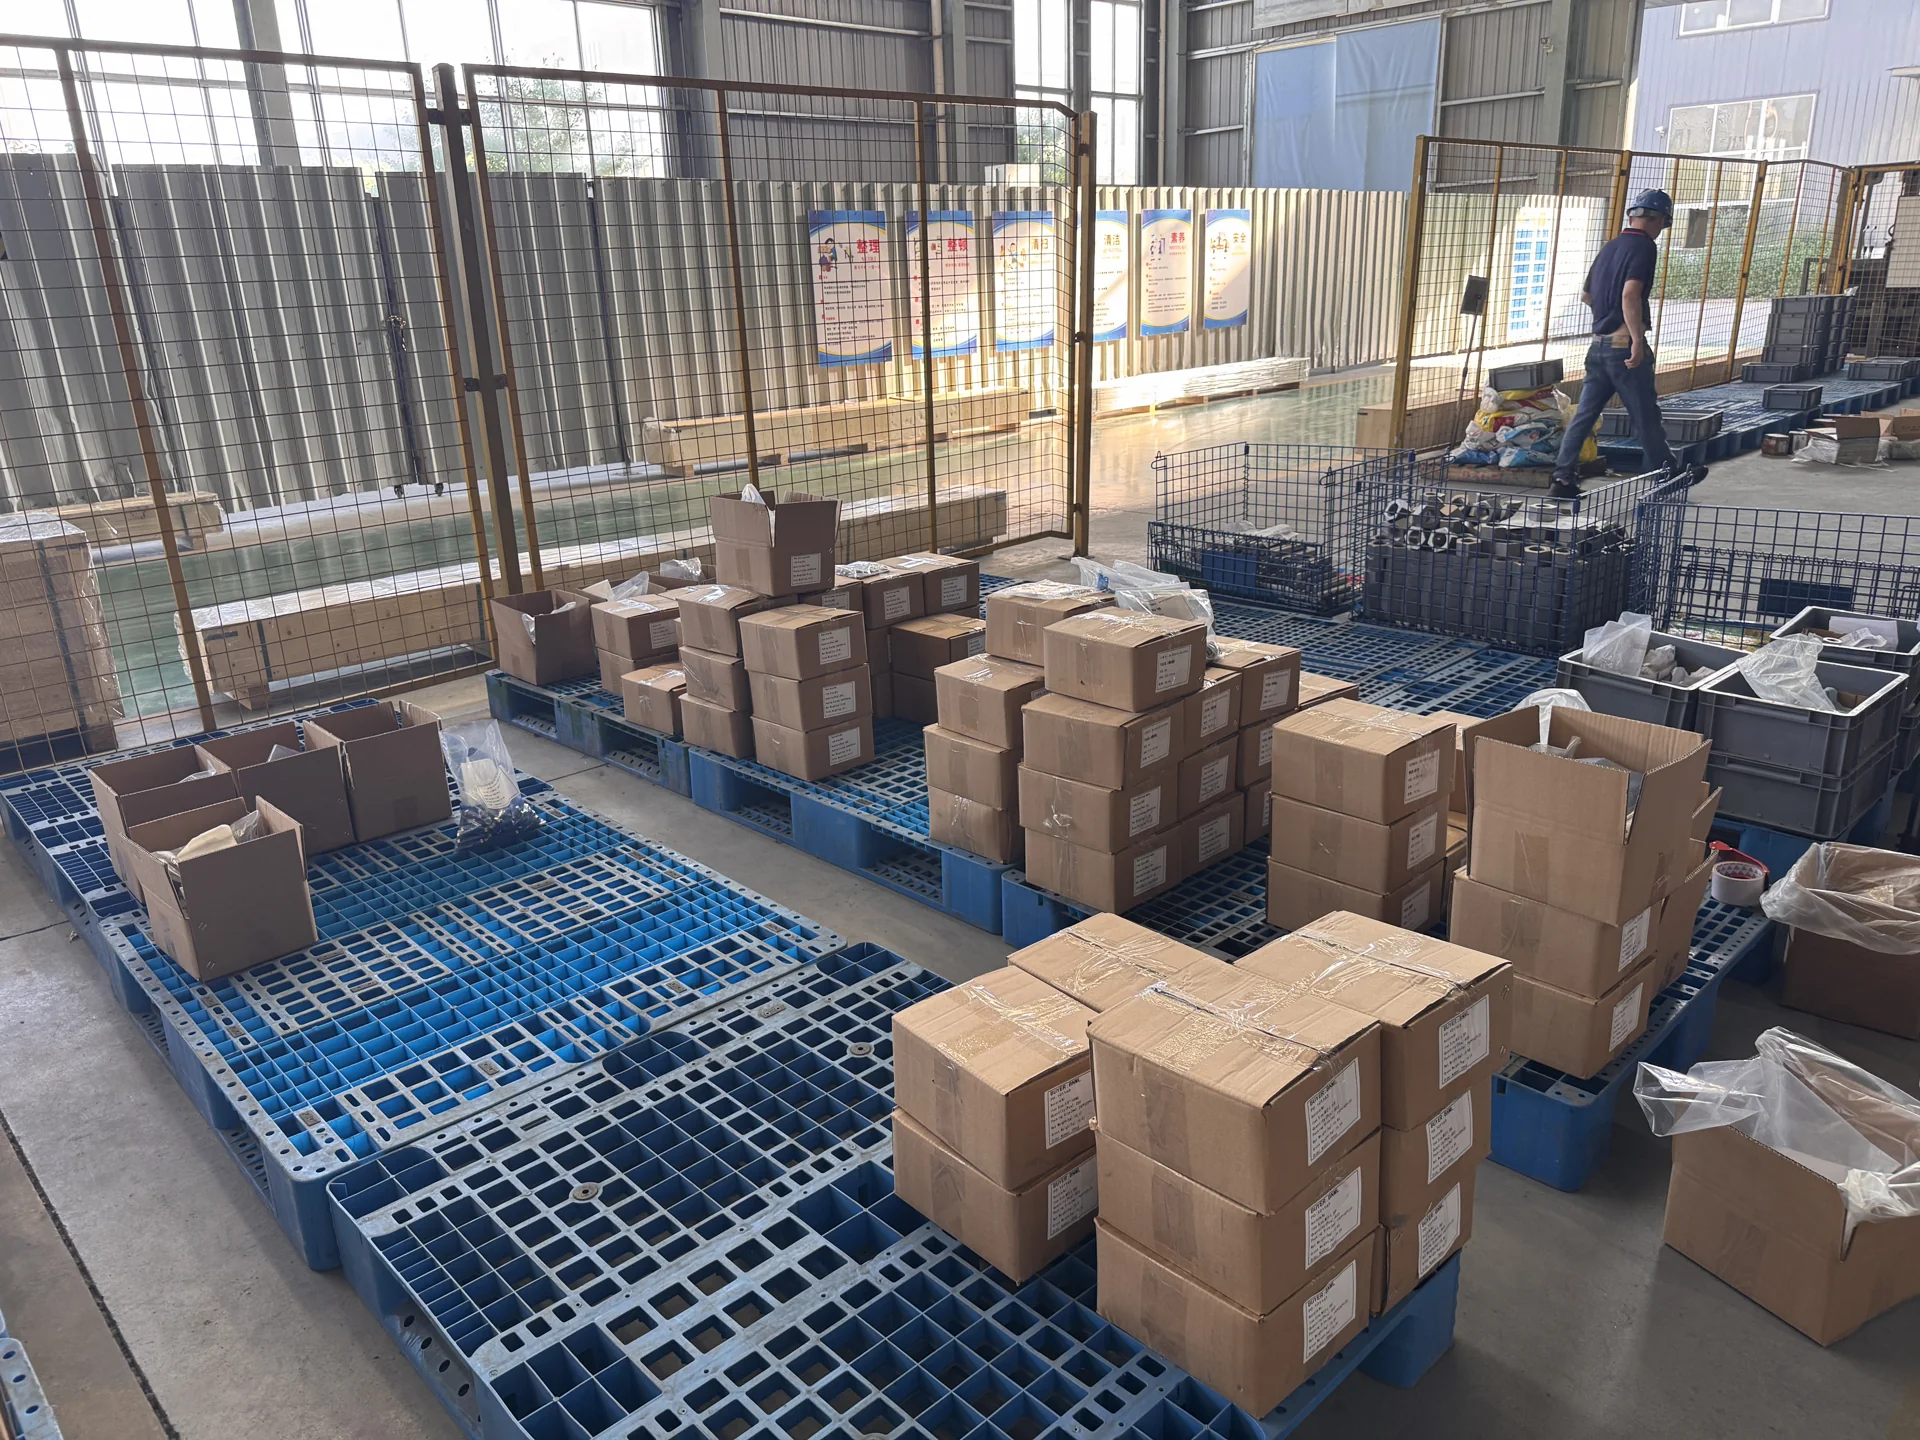
Identified packing
Heat and batch records linked to the shipment
Additional inspection requirements +
PMI, third-party inspection and witness testing are available by order. Project inspection plans can include UT/PT and heat-treatment records.
Matching products for long-shank hex head bolts
Prepare your enquiry
- Material
- Grade / UNS · Condition
- Size
- Diameter · Length / height
- Thread
- Pitch / TPI · Form & class
- Quantity
- Pieces per size