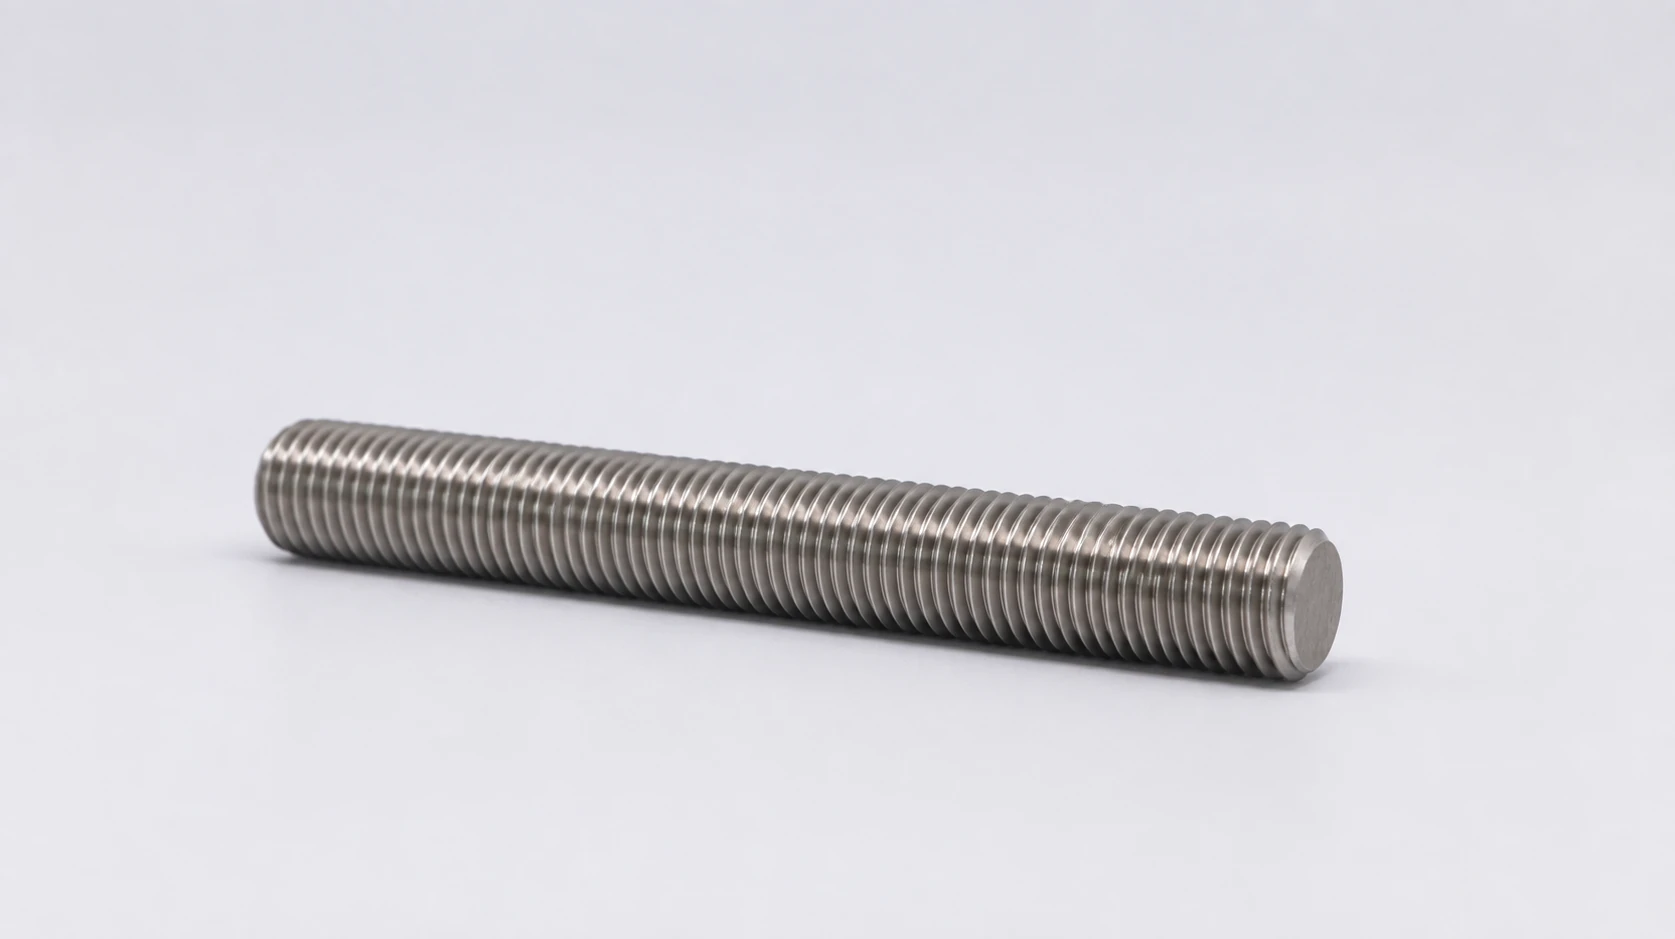
Incoloy 800HT Stud Bolts
ASME B18.31.2ASTM B408
Incoloy 800HT stud bolts bring tightly controlled carbon and Al + Ti for creep duty to flange and cover joints. The stud condition, mating nuts and end form determine how the assembly carries and retains clamp load.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed (≥1149°C / 2100°F)
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealedThe specified solution treatment develops the controlled grain structure needed for sustained high-temperature creep duty.
What we can make in Alloy 800HT
Fully threaded
Two nuts clamp the flange or cover; usable thread length spans the assembled grip.
Double-end
A plain centre spans the grip, with a threaded portion at each end for the nuts.
Tap-end
One end engages a tapped casing; the exposed end accepts the cover nut.
- Threads
- Metric · UNC · UNF · 8UN · UNJ
- Forms
- Continuous thread · Double-end · Tap-end
- Final condition
- Solution annealed (≥1149°C / 2100°F)
- Inspection
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
Manufacturing route
CNC machining suits samples and special end forms. Repeat lots use cut-to-length stock with rolling or cutting selected for the ordered thread and material condition.
Heat treatment & final condition
Solution annealing at a minimum of 1149°C (2100°F) establishes the coarse-grain condition used for creep resistance. The heat-treatment record and grain-size result identify this delivery state.
Finished geometry
End lengths, runout and effective thread engagement are checked separately from overall length; tap ends are gauged to their own fit requirement.
Where 800HT fits — and what matters
Furnaces & Heat Treatment
Retort and furnace-access coversIncoloy 800HT stud bolts & threaded rods clamp retort and furnace-access covers with nuts on the exposed ends, keeping the stud in place when a cover is removed. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
Power & Turbines
Hot-gas access covers and inspection closuresIncoloy 800HT stud bolts & threaded rods clamp hot-gas access covers and inspection closures with nuts on the exposed ends, keeping the stud in place when a cover is removed. Hot dwell and start-stop expansion act on the supported or moving component.
Chemical Processing
Reformer access covers and hot-gas inspection closuresIncoloy 800HT stud bolts & threaded rods clamp reformer access covers and hot-gas inspection closures with nuts on the exposed ends, keeping the stud in place when a cover is removed. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same stud. Different material priorities.
Incoloy 800HT material dataIncoloy 800
UNS N08800- Carbon
- ≤0.10%
- What changes
- General heat and oxidation resistance; no grain-size requirement in the family comparison.
Incoloy 800H
UNS N08810- Carbon
- 0.05–0.10%
- What changes
- Controlled carbon and coarse-grain condition for creep and stress-rupture duty.
Incoloy 800HT
UNS N08811 · Current grade- Carbon
- 0.06–0.10%
- What changes
- Tighter carbon and Al + Ti control (0.85–1.20%), with solution treatment and coarse grain for creep duty.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N08811 · heat number · ordered condition
- Final-part acceptance
- UNS grade, carbon and alloy chemistry, solution-treatment record and ordered grain-size evidence.
- Dimensional record
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Matching Kit
Flange Stud Bolt Kits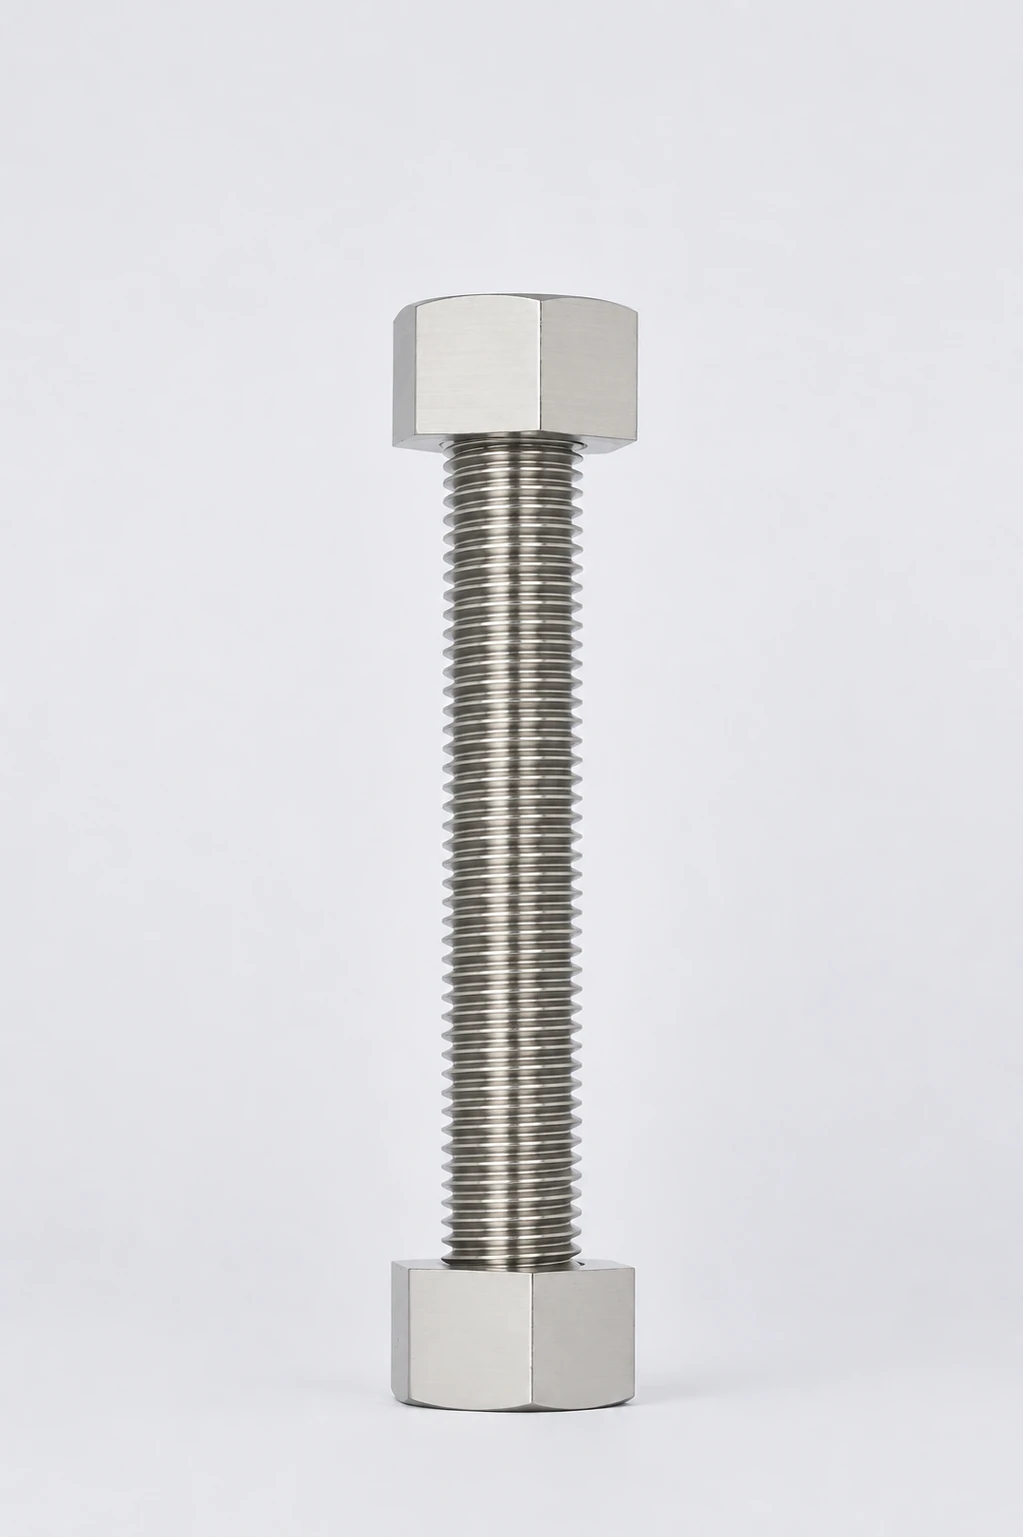
Build your 800HT stud enquiry
Questions about 800HT stud bolts & threaded rods
Does changing the stud alloy also change the nut selection?
The nut needs compatible internal threads, sufficient engaged height and a specified material condition. Select lubricant or surface treatment with the stud–nut pair, because assembly friction affects the preload obtained from tightening.