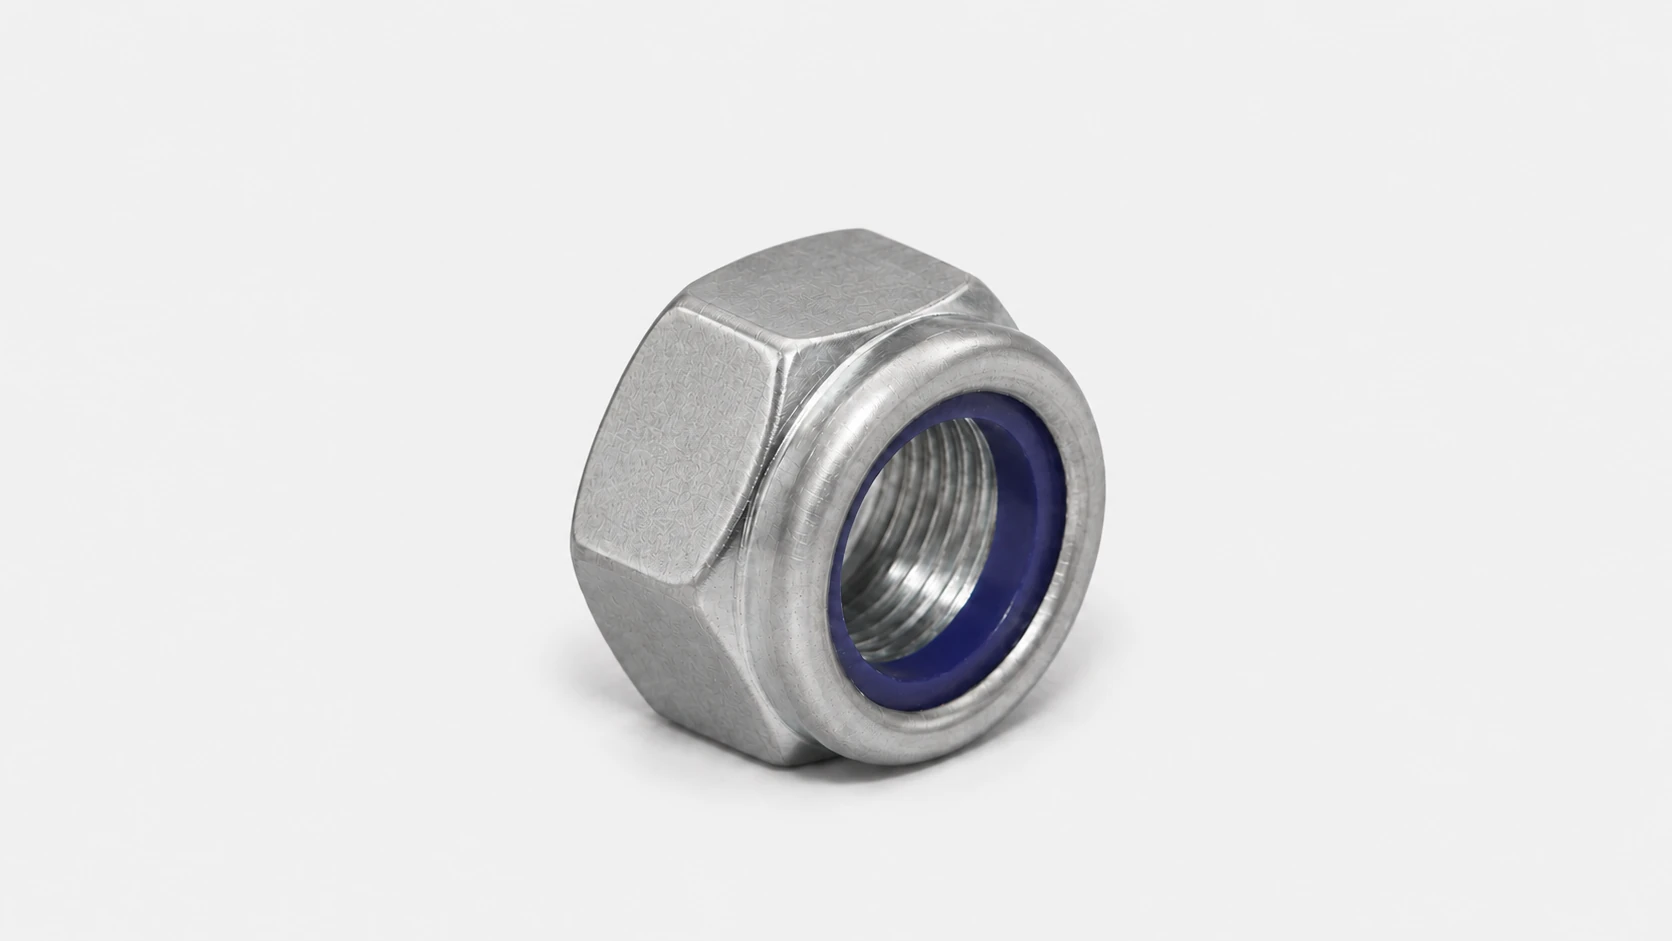
Incoloy 800HT Nylon-insert lock nuts
ISO 7040ASTM B408
Incoloy 800HT nylon-insert nuts combine a specified alloy body with polymer-generated prevailing torque. Insert temperature, chemical compatibility and reuse performance define the complete nut’s service, including when the body is selected for tightly controlled carbon and Al + Ti for creep duty.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed (≥1149°C / 2100°F)
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealedThe specified solution treatment develops the controlled grain structure needed for sustained high-temperature creep duty.
What we can make in Alloy 800HT
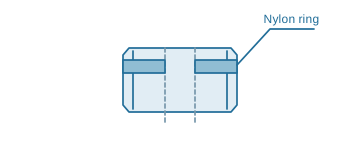
Nylon insert
Use where a prevailing-torque nut helps retain an adjustment or mounting connection without a separate locking part. The bolt must engage through the nylon ring for the insert to act.
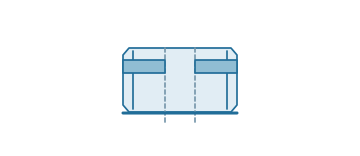
Metal body
The metal threads carry the axial clamp load. Select the body pattern and strength for that load, then check the additional running torque from the insert when setting the tightening process.
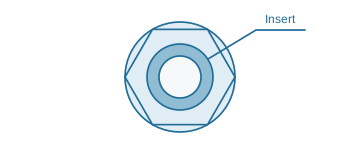
Temperature & chemicals
Choose this form for equipment temperatures and chemicals compatible with the insert. A nickel-alloy body does not make nylon suitable for furnace service; use an all-metal locking arrangement for elevated-temperature joints.
- Locking element
- Nylon insert
- Drive
- External hex
- Threads
- Metric · Inch
- Service limit
- Controlled by the insert
- Final condition
- Solution annealed (≥1149°C / 2100°F)
- Inspection
- Insert retention · Prevailing torque · Dimensions
Manufacturing route
Small lots use machined blanks. Volume nut blanks use a forming route compatible with the alloy before machining the bore and tapping.
Heat treatment & final condition
Solution annealing at a minimum of 1149°C (2100°F) establishes the coarse-grain condition used for creep resistance. The heat-treatment record and grain-size result identify this delivery state.
Finished geometry
The nylon insert is installed after metal heat treatment and finishing. Prevailing torque is checked on the complete nut, including the specified reuse requirement.
Where 800HT fits — and what matters
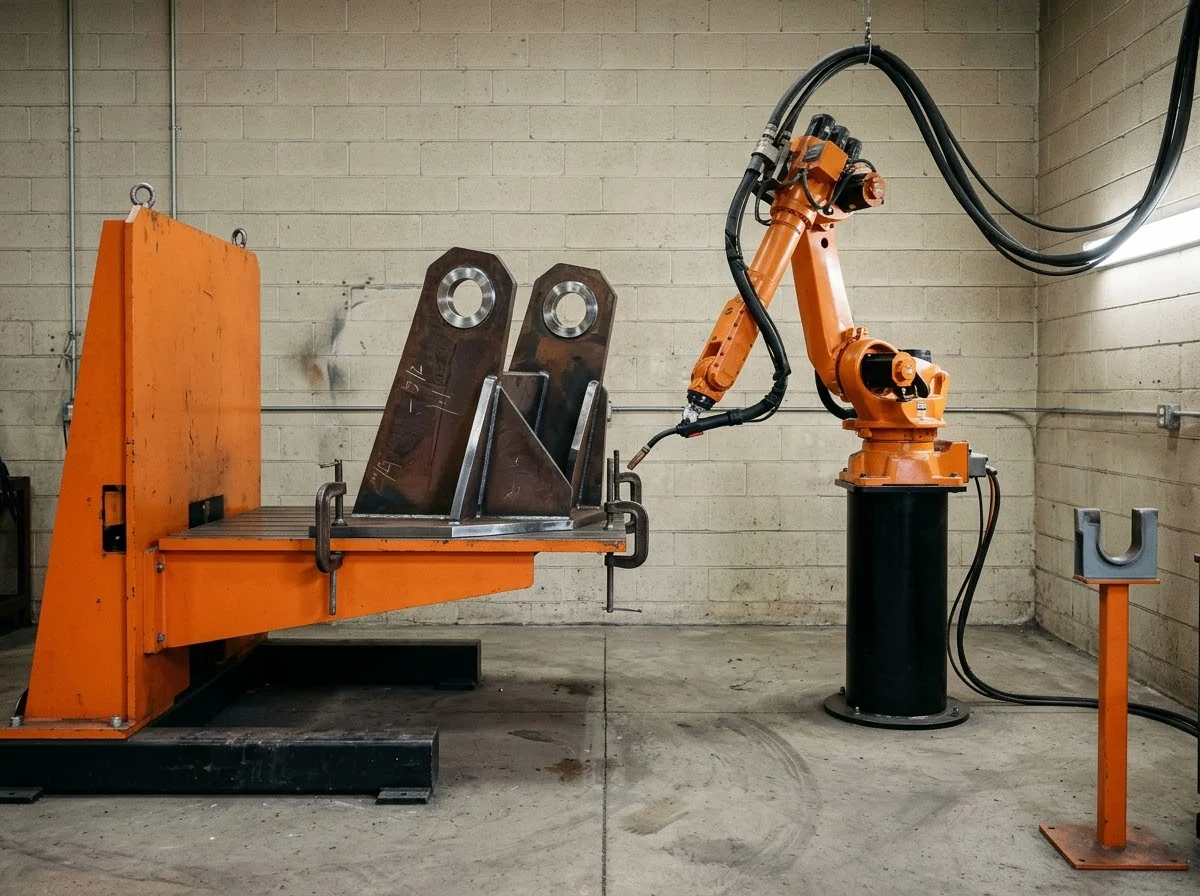
Industrial Machinery & Automation
Machine frames and positioning fixturesIncoloy 800HT nylon-insert lock nuts retain the threaded mountings on machine frames and positioning fixtures using insert-generated prevailing torque. The nylon insert defines the temperature and reuse limits of the complete nut. Alignment, operating cycles and replacement access define the working interface.
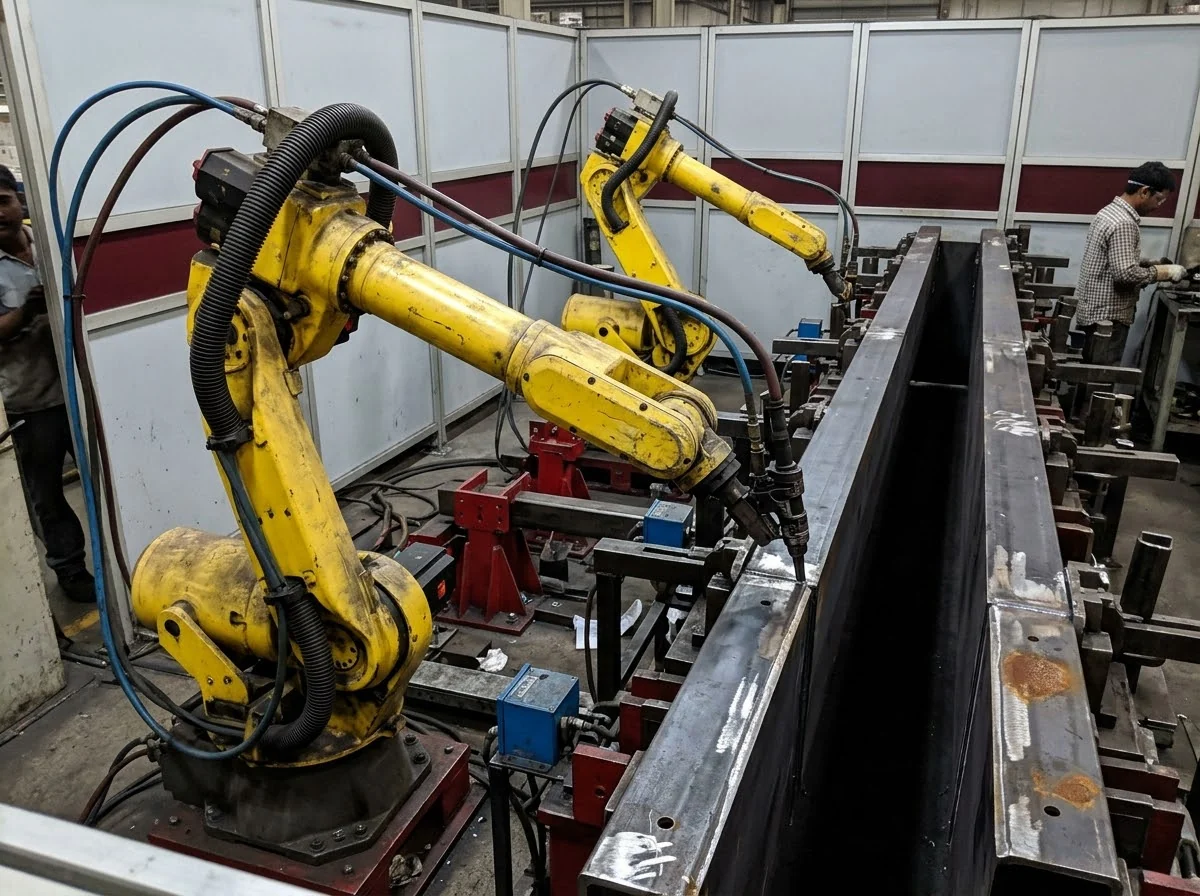
Automotive & EV Manufacturing Equipment
Assembly fixtures and test-rig framesIncoloy 800HT nylon-insert lock nuts retain the threaded mountings on assembly fixtures and test-rig frames using insert-generated prevailing torque. The nylon insert defines the temperature and reuse limits of the complete nut. Repeated tooling changes require consistent seating and repeatable assembly dimensions.
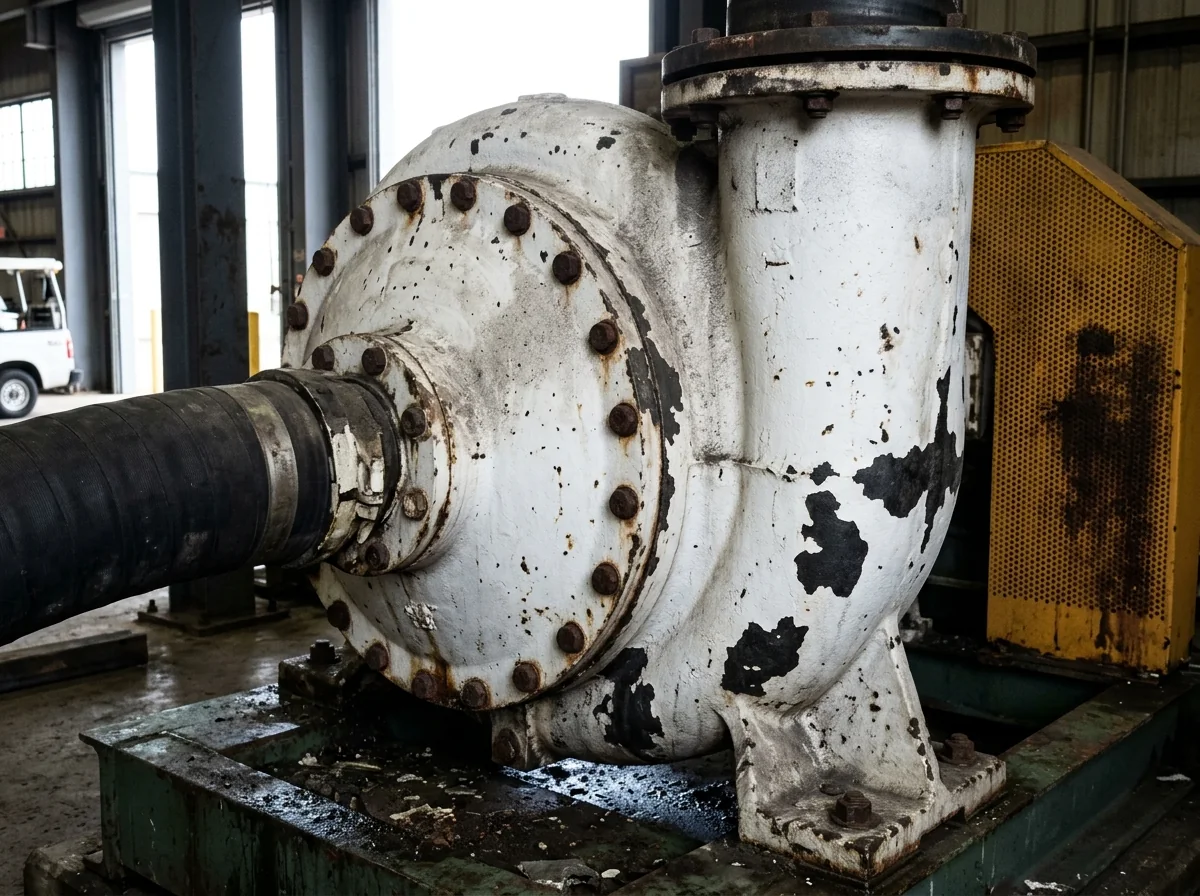
Pumps, Valves & OEM
Actuator mounts and pump baseplatesIncoloy 800HT nylon-insert lock nuts retain the threaded mountings on actuator mounts and pump baseplates using insert-generated prevailing torque. The nylon insert defines the temperature and reuse limits of the complete nut. Repeated maintenance makes fit, engagement and access part of the component specification.
Same nylon-insert lock nut. Different material priorities.
Incoloy 800HT material dataIncoloy 800
UNS N08800- Carbon
- ≤0.10%
- What changes
- General heat and oxidation resistance; no grain-size requirement in the family comparison.
Incoloy 800H
UNS N08810- Carbon
- 0.05–0.10%
- What changes
- Controlled carbon and coarse-grain condition for creep and stress-rupture duty.
Incoloy 800HT
UNS N08811 · Current grade- Carbon
- 0.06–0.10%
- What changes
- Tighter carbon and Al + Ti control (0.85–1.20%), with solution treatment and coarse grain for creep duty.
From drawing to documented delivery
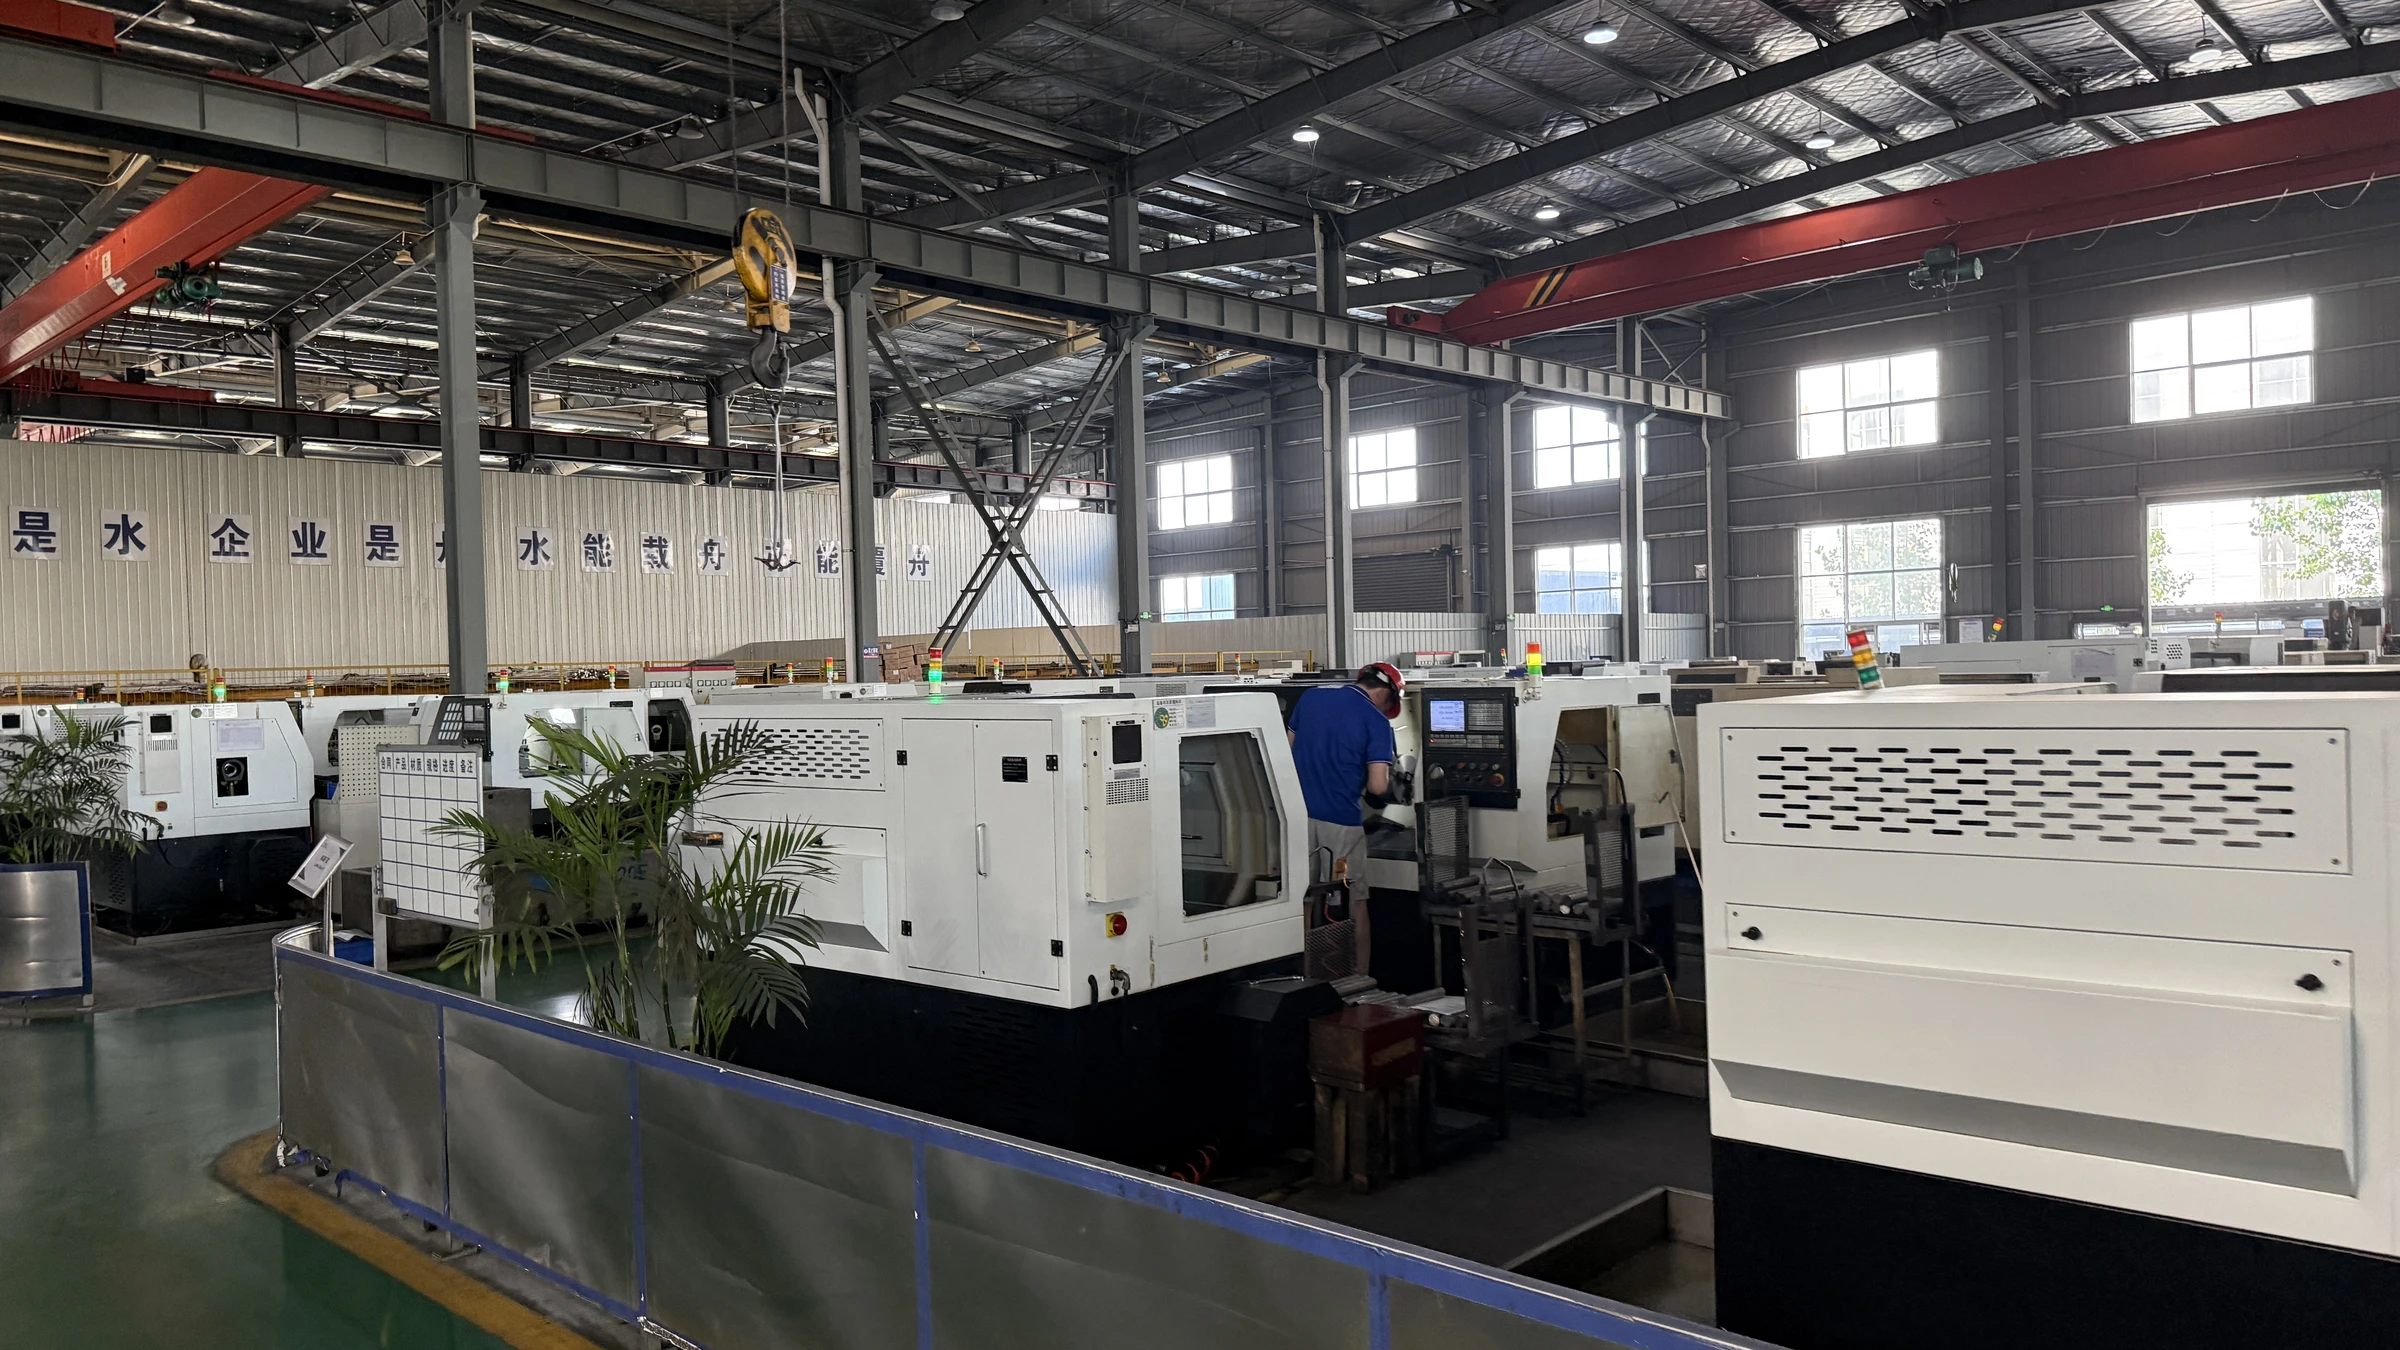
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
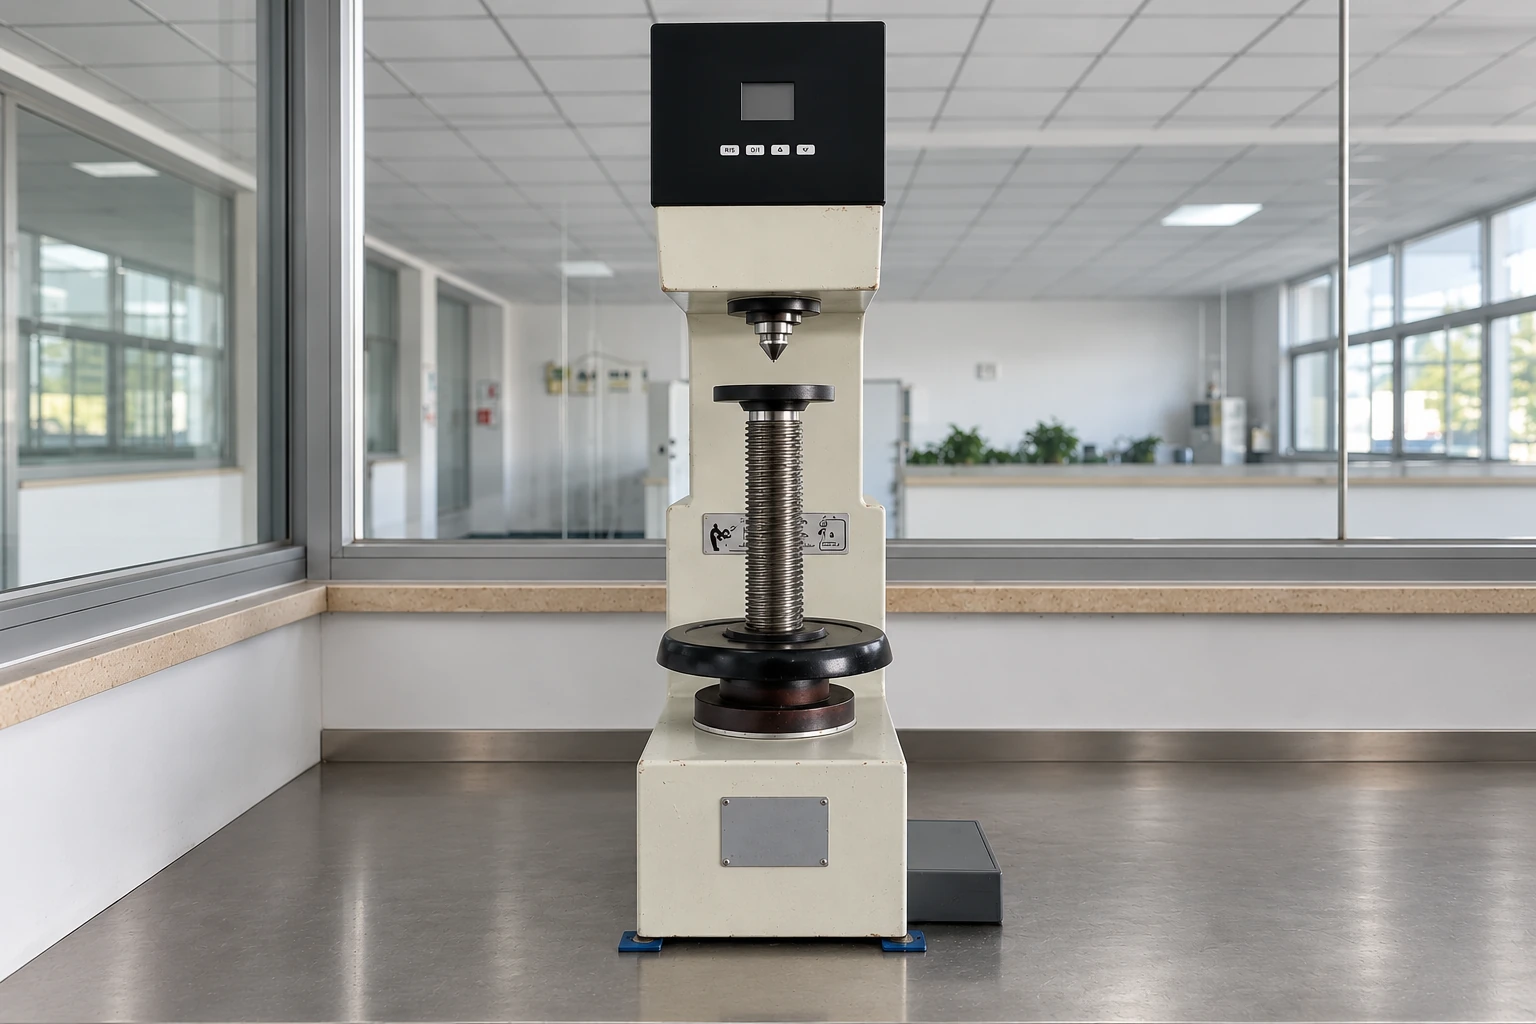
- 03Final inspectionGeometry, threads and ordered tests
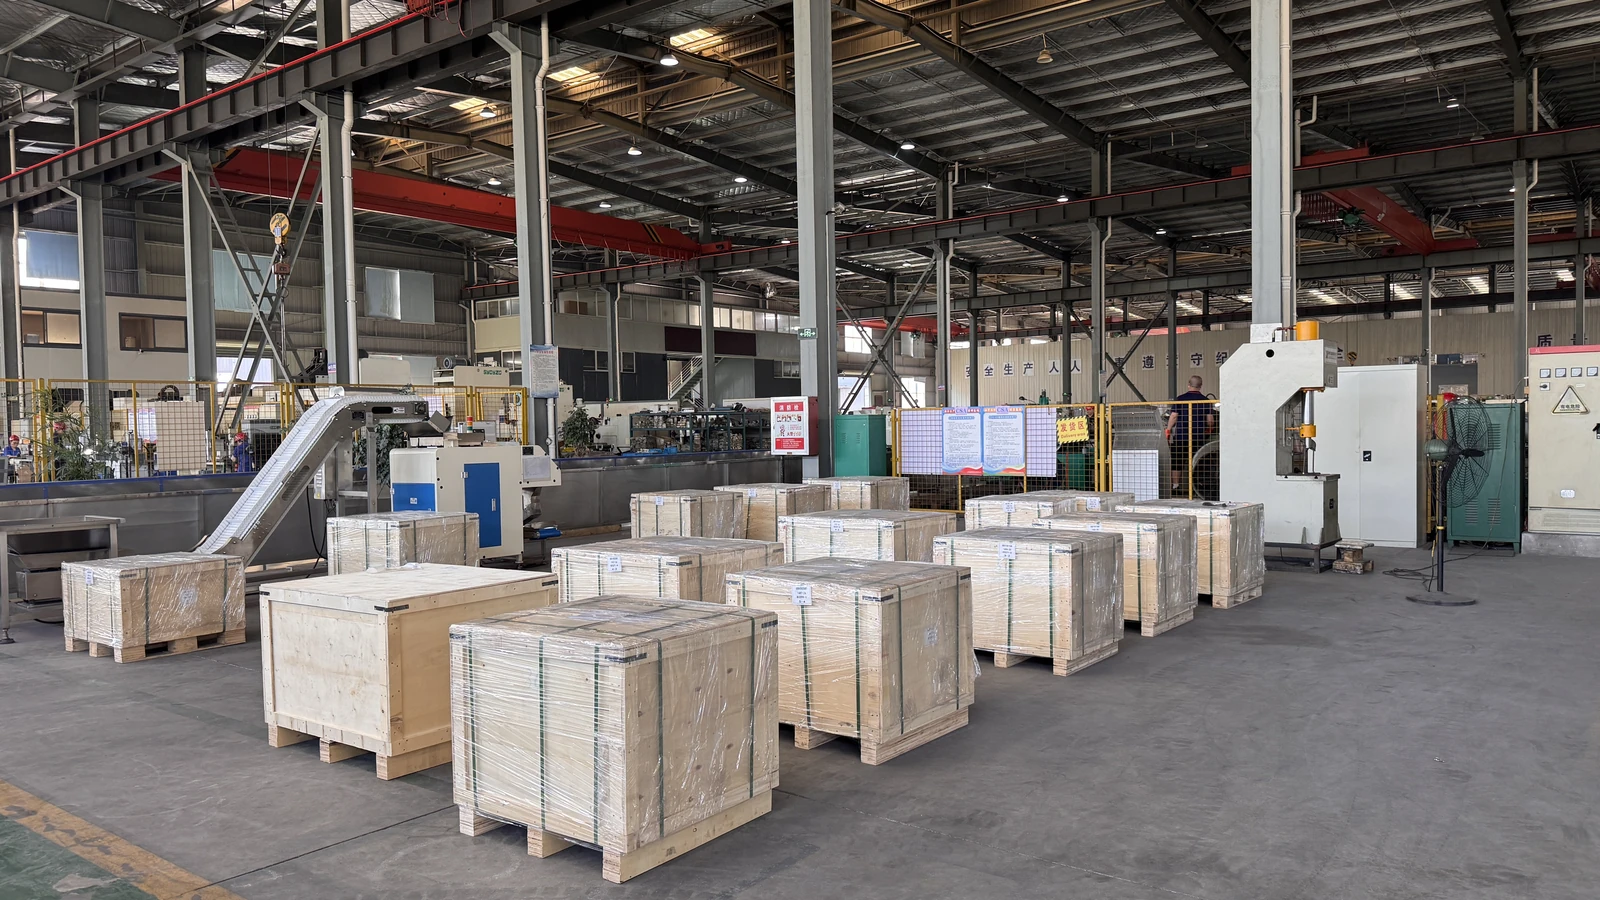
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N08811 · heat number · ordered condition
- Final-part acceptance
- UNS grade, carbon and alloy chemistry, solution-treatment record and ordered grain-size evidence. Insert identity and complete-nut prevailing-torque results.
- Dimensional record
- Insert retention · Prevailing torque · Dimensions
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your 800HT nylon-insert lock nut enquiry
Questions about 800HT nylon-insert lock nuts
Can a heat-resistant body make the nylon nut suitable for a hot joint?
The nylon remains the temperature-limiting part. Use the actual insert rating and required prevailing-torque performance; a hot-service metal grade does not extend the polymer’s limit.