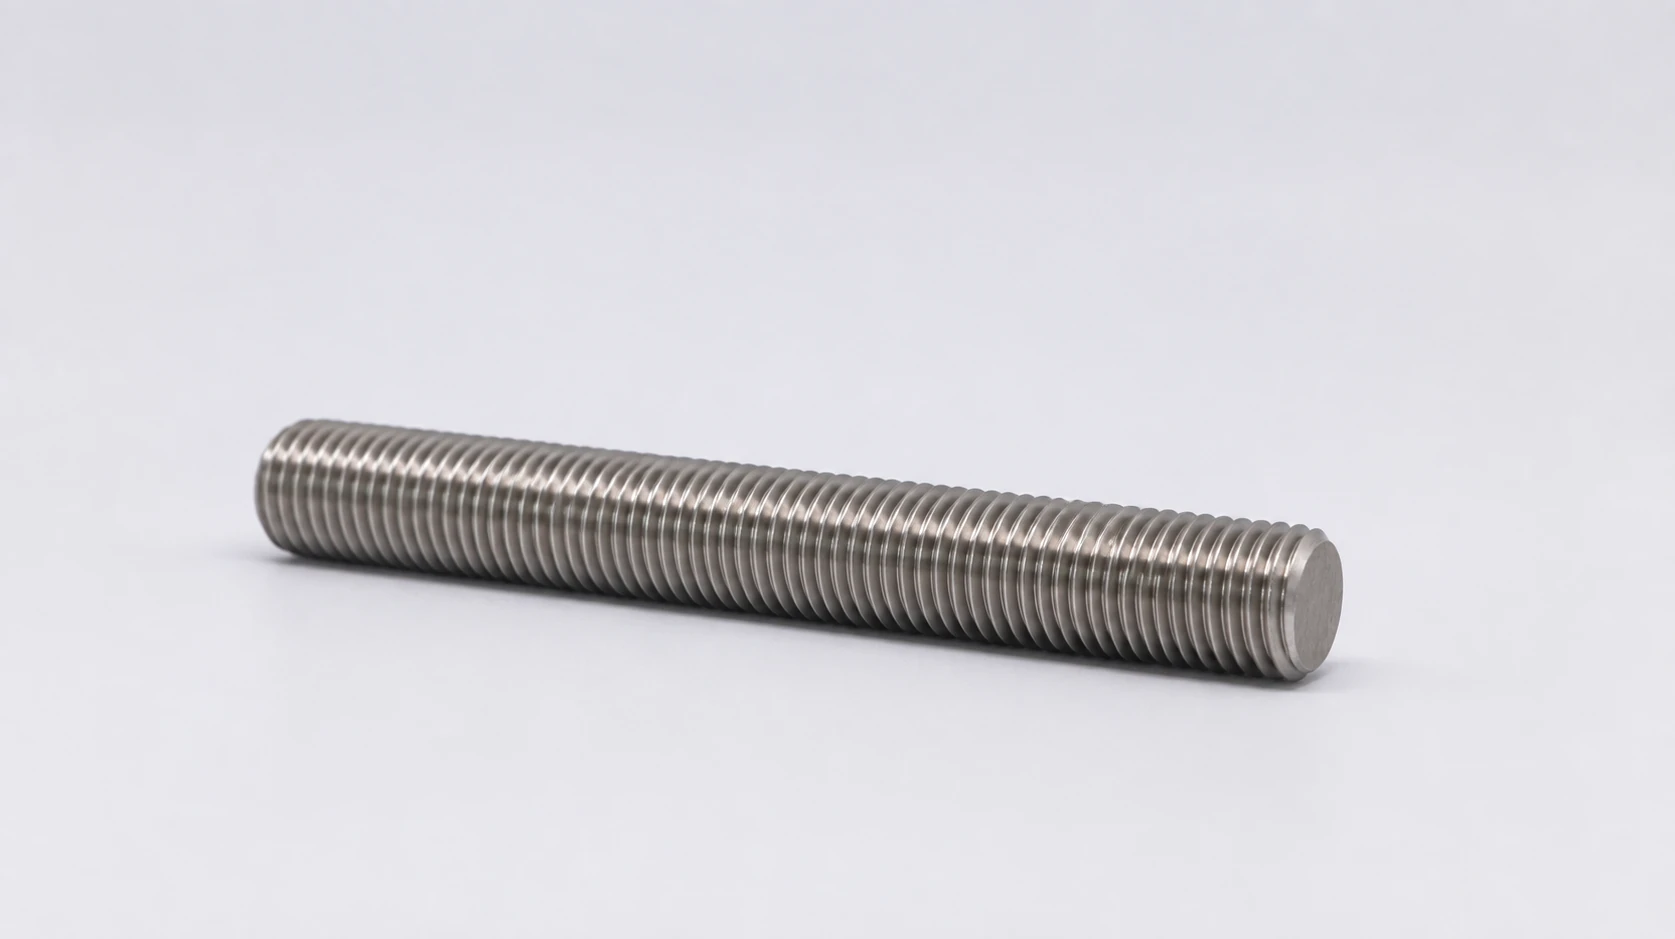
254 SMO Stud Bolts
ASME B18.31.2ASTM A276
254 SMO studs provide removable connections for seawater pump covers, bleach-plant equipment and chloride-bearing process flanges. Full-thread and double-end forms let the six-moly austenitic alloy serve both through-flange joints and tapped equipment housings.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealedSolution annealing and rapid cooling retain alloying elements in solution and restore the specified corrosion-resistant condition.
What we can make in 254 SMO
Fully threaded
Two nuts clamp the flange or cover; usable thread length spans the assembled grip.
Double-end
A plain centre spans the grip, with a threaded portion at each end for the nuts.
Tap-end
One end engages a tapped casing; the exposed end accepts the cover nut.
- Threads
- Metric · UNC · UNF · 8UN · UNJ
- Forms
- Continuous thread · Double-end · Tap-end
- Final condition
- Solution annealed
- Inspection
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
Manufacturing route
CNC machining suits samples and special end forms. Repeat lots use cut-to-length stock with rolling or cutting selected for the ordered thread and material condition.
Heat treatment & final condition
The final annealed or specified strengthened condition is linked to the lot; an aging treatment is not assumed for a solid-solution alloy.
Finished geometry
End lengths, runout and effective thread engagement are checked separately from overall length; tap ends are gauged to their own fit requirement.
Where 254 SMO fits — and what matters
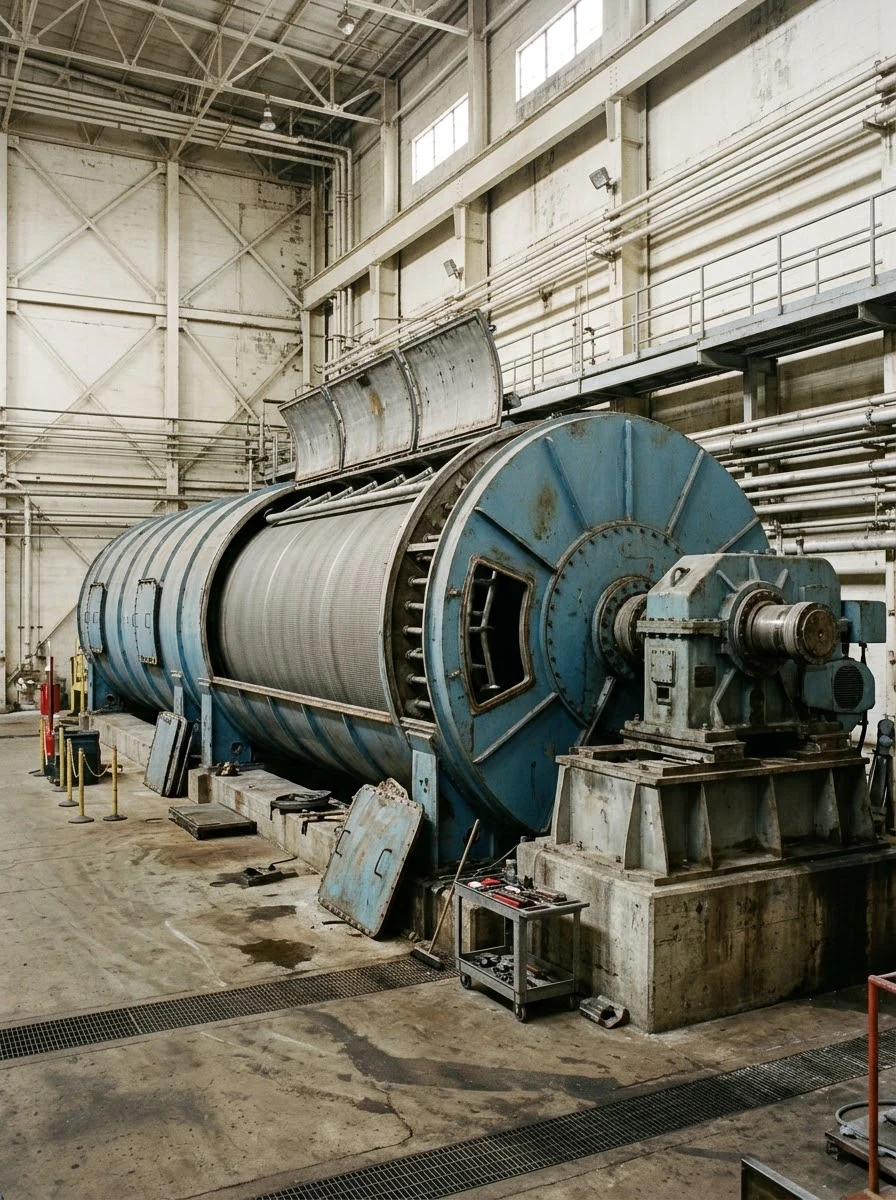
Bleach-plant washers & mixers (ClO2)
254 SMO Stud Bolts254 SMO studs suit bleach-plant washer and mixer covers exposed to chloride-bearing residue. On tapped housings, the studs can remain installed while the outer nuts and cover are removed for cleaning. That preserves the equipment-side thread through repeated servicing while putting six-moly corrosion resistance at the exposed fastening points.
Connection requirements
- Liquor chemistry and cleaning cycle
- Housing-side engagement
- Cover stack and nut projection
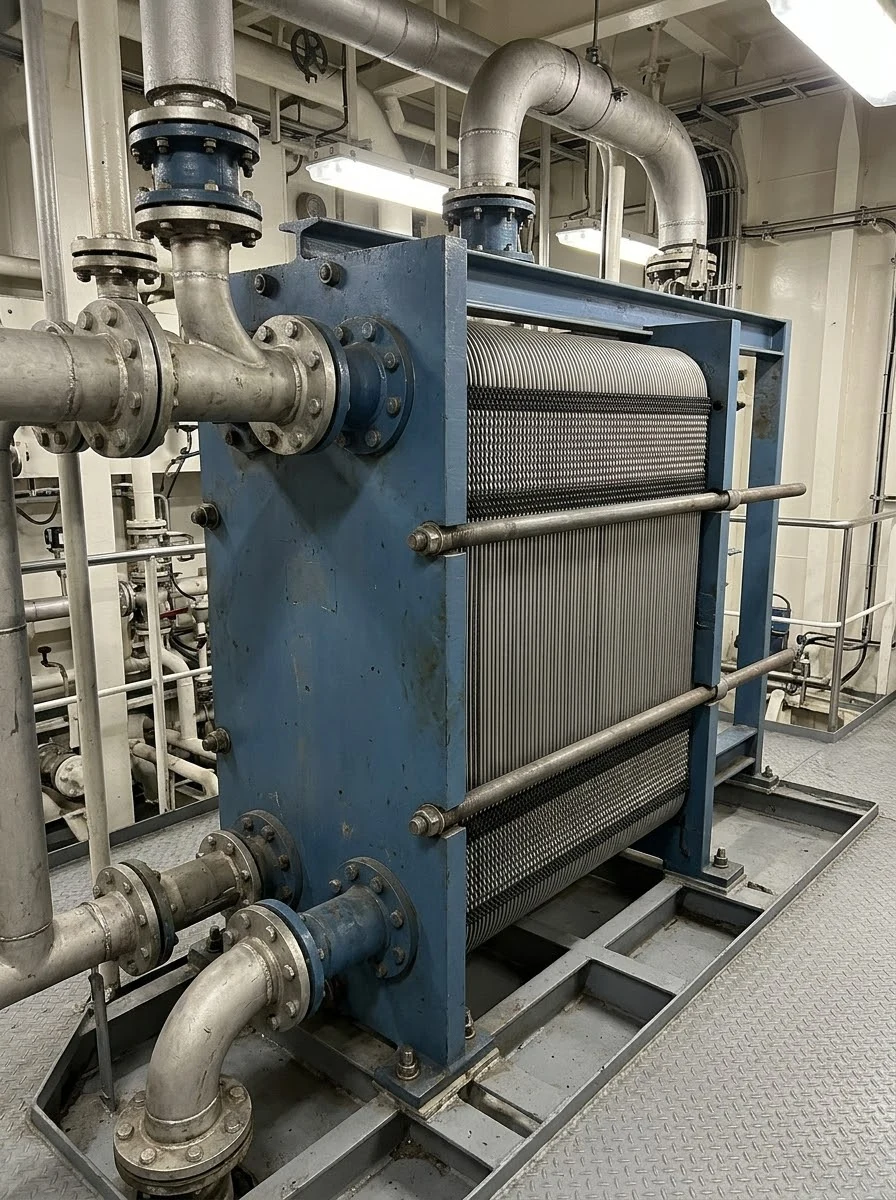
Plate & shell heat-exchanger covers
254 SMO Stud BoltsTapped heat-exchanger housings may use double-end studs to align a heavy end plate before the nuts are tightened. 254 SMO is useful at chloride-exposed connections, including areas reached by seawater leakage. Stud length follows the actual cover and gasket stack, while the nut pairing must carry the closure load through repeated service cycles.
Connection requirements
- Cover and gasket stack
- Water temperature and deposits
- Stud tension and mating-nut capacity
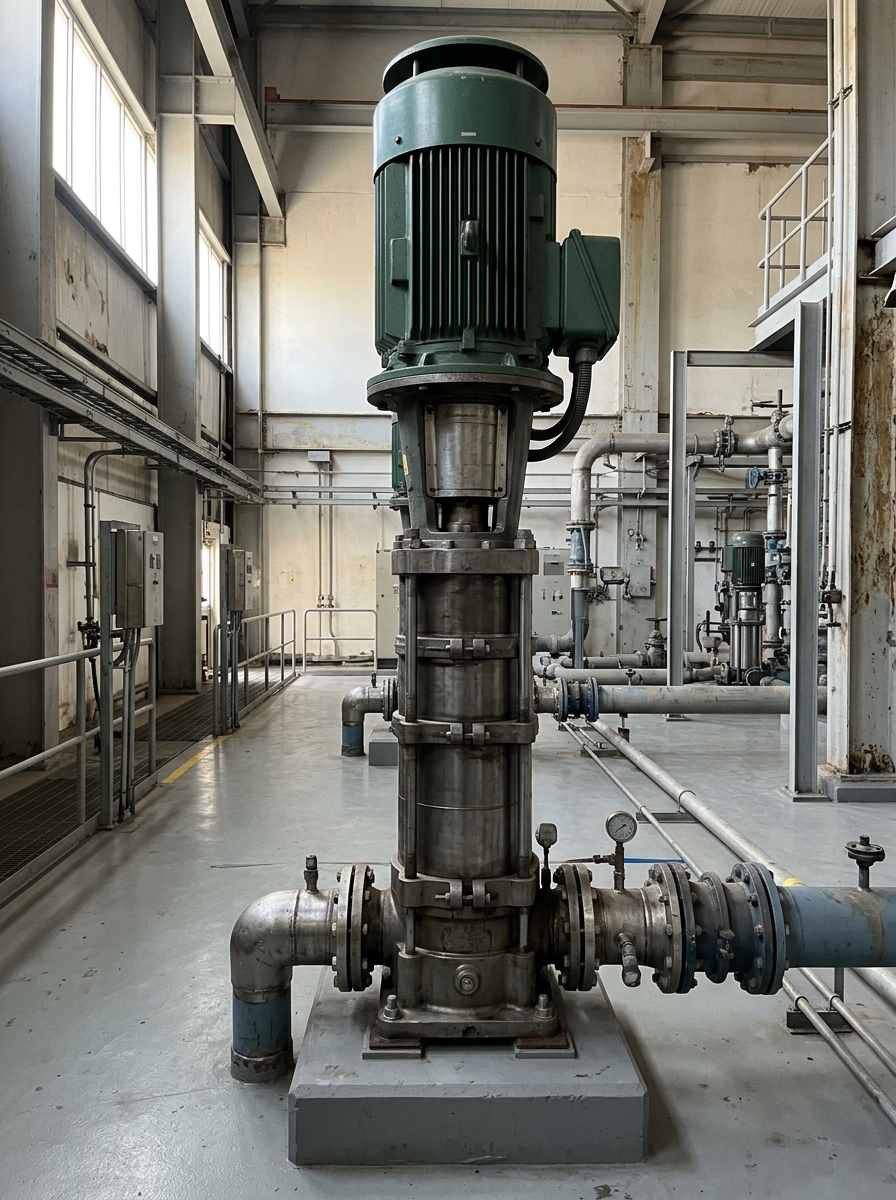
Brine booster & high-pressure pumps
254 SMO Stud BoltsOn brine-pump covers, 254 SMO studs offer an austenitic route to improved chloride resistance over 316. Double-end studs allow the housing engagement and nut-end length to be set separately. Concentrated brine retained near the nut seat is a different exposure from the pumped water and should be represented in material selection.
Connection requirements
- Brine concentration and temperature
- Tapped housing depth
- Finished-stud properties and nut seat
Same stud. Different material priorities.
254 SMO material dataDuplex 2205 Stud Bolts
Duplex 2205 studs carry loaded process-water and brackish-water closures where strength and chloride resistance matter together. Double-end forms stay in tapped casings during cover removal, reducing repeated assembly of the housing thread. Independently dimensioned ends leave the nut accessible above the cover and washer stack.
Super Duplex 2507 Stud Bolts
2507 studs are useful on seawater pump covers and high-pressure desalination connections where corrosion resistance and strength are both priorities. The stud arrangement keeps nuts accessible and helps locate removable covers. Compared with 2205 studs, they address more demanding chloride exposure; the final heat-treated condition is central to that performance.
Inconel 625 Stud Bolts
Offshore flanges and marine valve bonnets put the stud threads, nut seats and exposed shank in different pockets of chloride exposure. Inconel 625 studs bring pitting and crevice-corrosion resistance to that loaded connection. On tapped-stud bonnets, crews can remove the nuts and cover while leaving the studs installed in the valve body.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S31254 · heat number · ordered condition
- Final-part acceptance
- Grade chemistry, supplied condition and ordered mechanical requirements.
- Dimensional record
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Matching Kit
Flange Stud Bolt Kits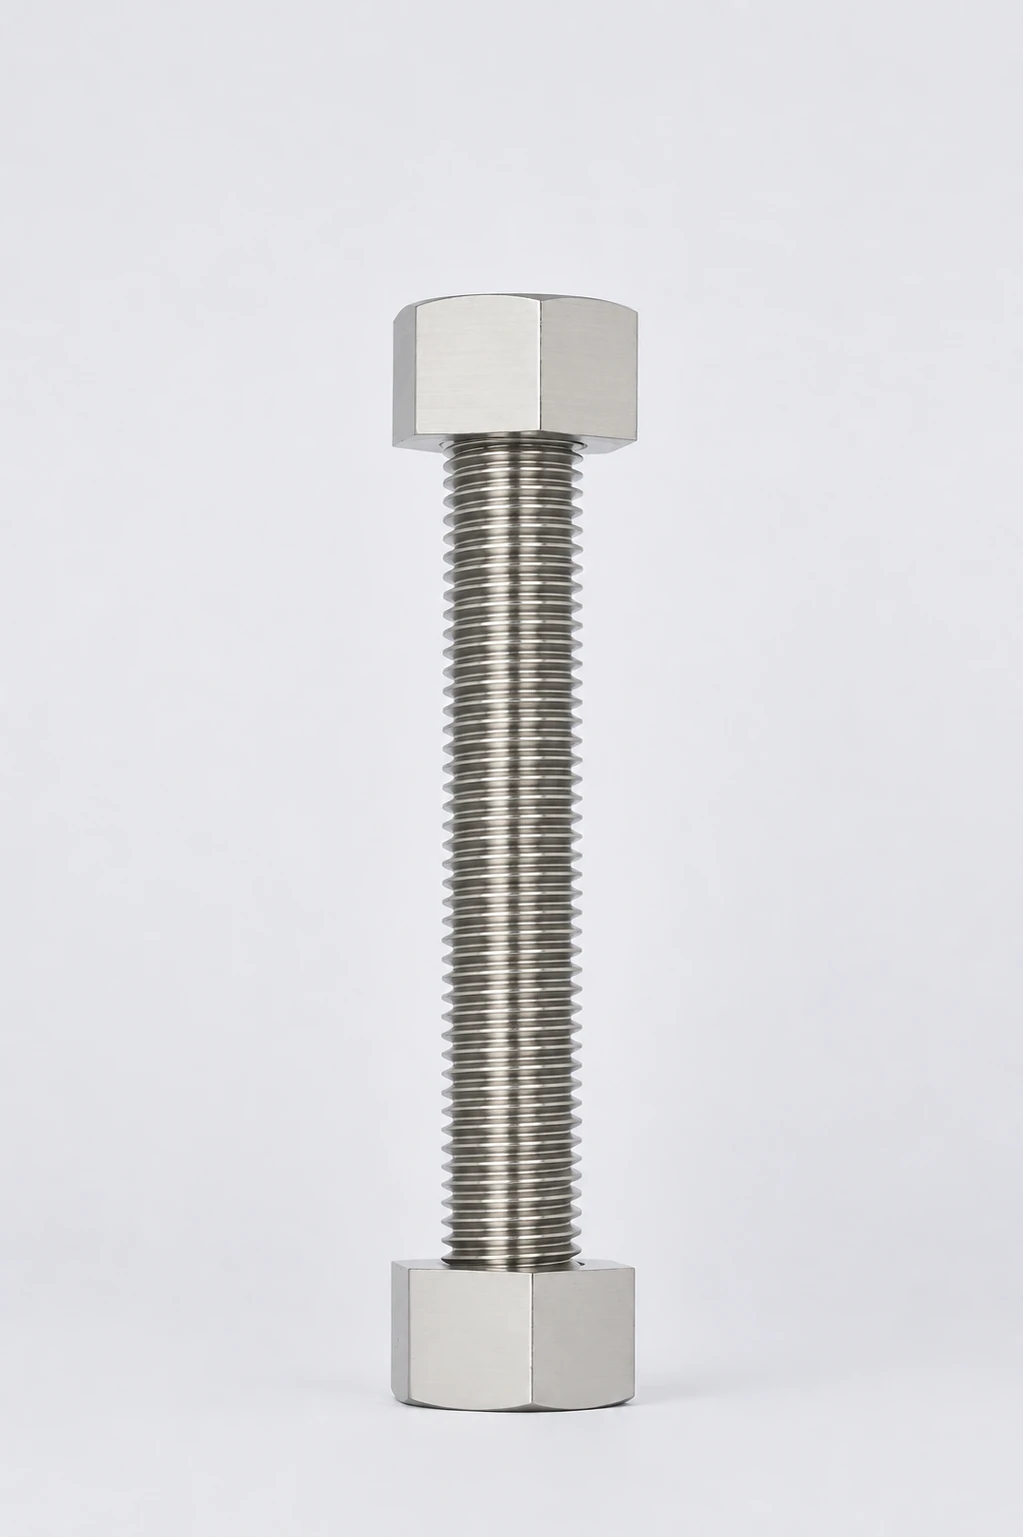
Build your 254 SMO stud enquiry
Questions about 254 SMO stud bolts & threaded rods
Does changing the stud alloy also change the nut selection?
The nut needs compatible internal threads, sufficient engaged height and a specified material condition. Select lubricant or surface treatment with the stud–nut pair, because assembly friction affects the preload obtained from tightening.