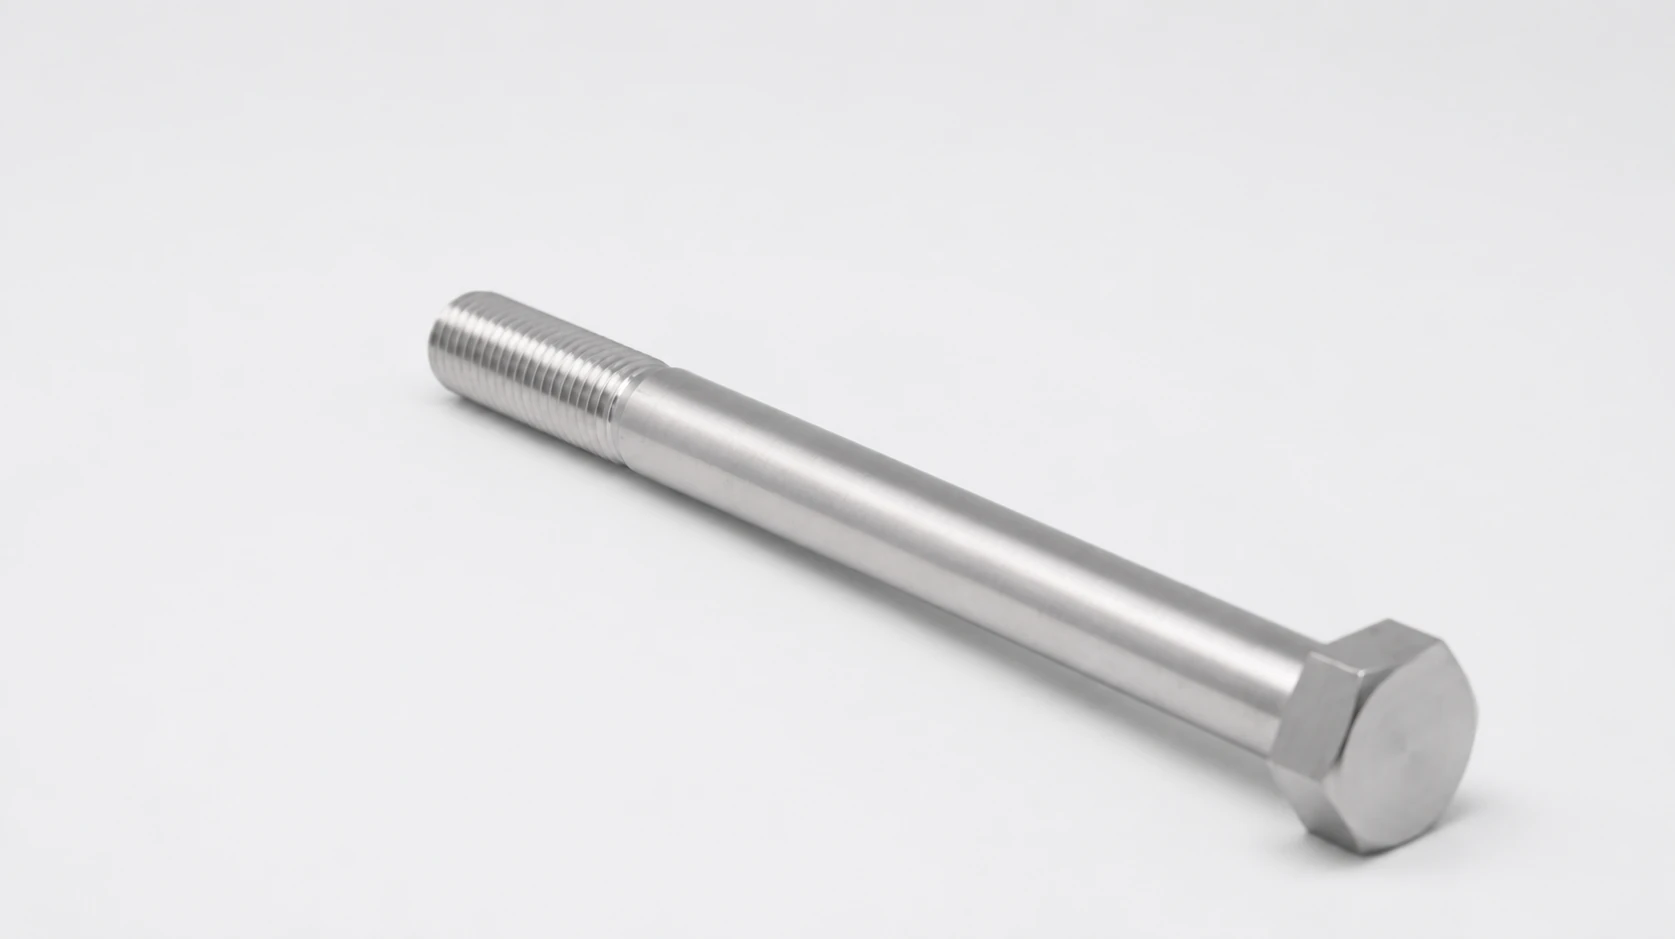
Inconel X-750 Long-shank hex head bolts
ISO 4014ASTM B637
Inconel X-750 long-shank hex bolts carry the grip through a plain section while providing age-hardened strength and a choice of hot-service heat treatments. Grip length and thread runout locate the loaded interfaces along the extended shank.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated and agedSolution treatment prepares the alloy for controlled precipitation aging, which develops the strength of the ordered condition.
What we can make in Alloy X-750
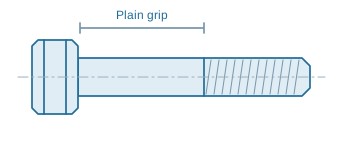
Plain grip section
Use across thick equipment flanges, spacers and mounting stacks where the grip requires a continuous plain shank. The grip length keeps the threaded transition beyond the intended bearing or shear section.
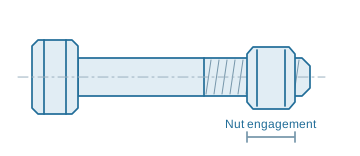
Threaded end
Allow enough usable thread beyond the stack for the nut, washer and tightening travel. Too little thread can leave the nut bottomed on the plain shank before the joint is clamped.
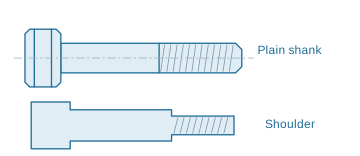
Long shank vs shoulder screw
For a pivot or locating bore, specify the actual shank diameter tolerance and surface finish. A long-shank bolt provides grip length; a shoulder-screw fit requires separate control of the locating surface.
- Head
- External hex
- Shank
- Extended plain length
- Length basis
- Under head
- Threads
- Metric · UNC · UNF · UNJ
- Final condition
- Solution treated and aged
- Inspection
- Thread gauges · Head and shank dimensions
Manufacturing route
CNC machining suits samples and small batches. Volume heads are formed in a workable condition with the final aging route included in process planning.
Heat treatment & final condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
Head geometry, bearing face, shank and thread fit are checked after the final machining and thermal operations.
Where X-750 fits — and what matters
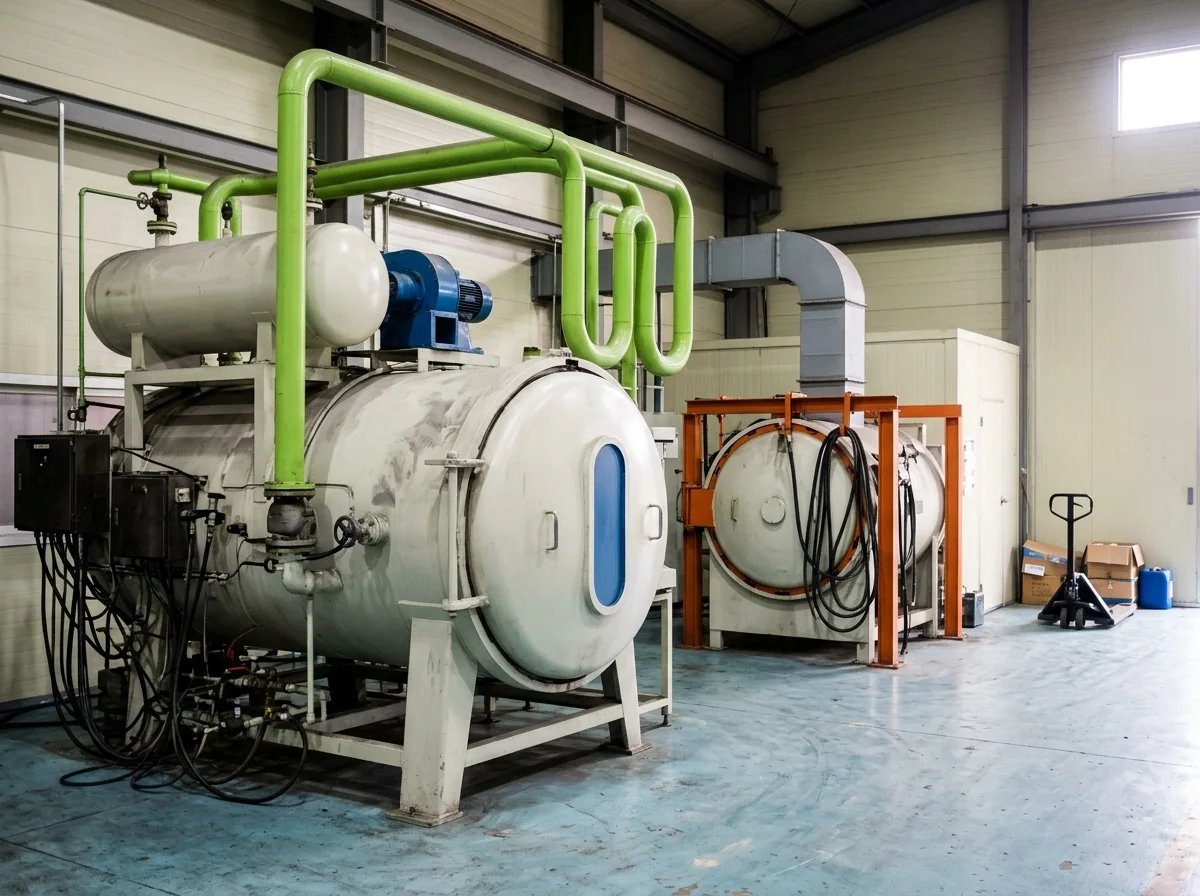
Furnaces & Heat Treatment
Heat-treatment fixturesInconel X-750 long-shank hex head bolts pass through the deeper grip of heat-treatment fixtures; the extended plain shank locates the joint before the nut takes up the thread. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
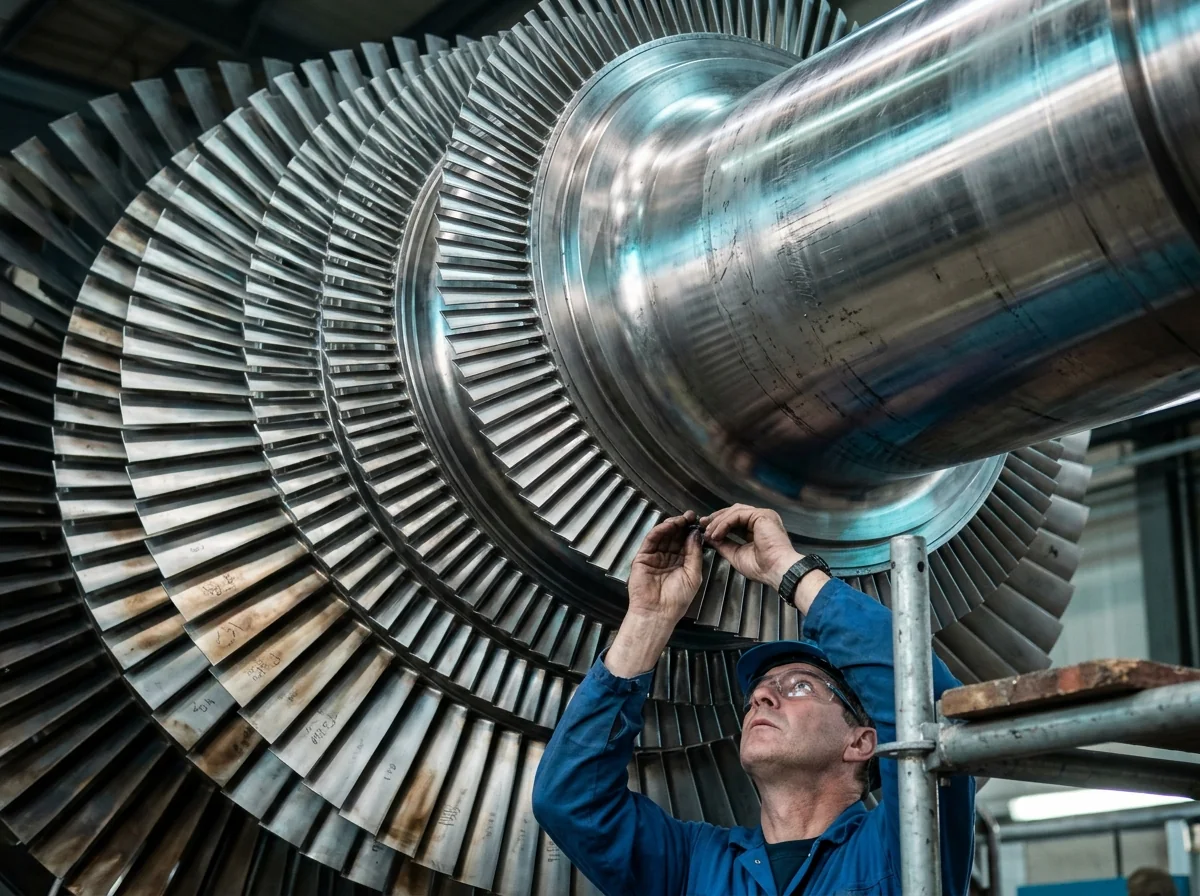
Power & Turbines
Boiler-duct supports and hot auxiliary bracketsInconel X-750 long-shank hex head bolts pass through the deeper grip of boiler-duct supports and hot auxiliary brackets; the extended plain shank locates the joint before the nut takes up the thread. Hot dwell and start-stop expansion act on the supported or moving component.
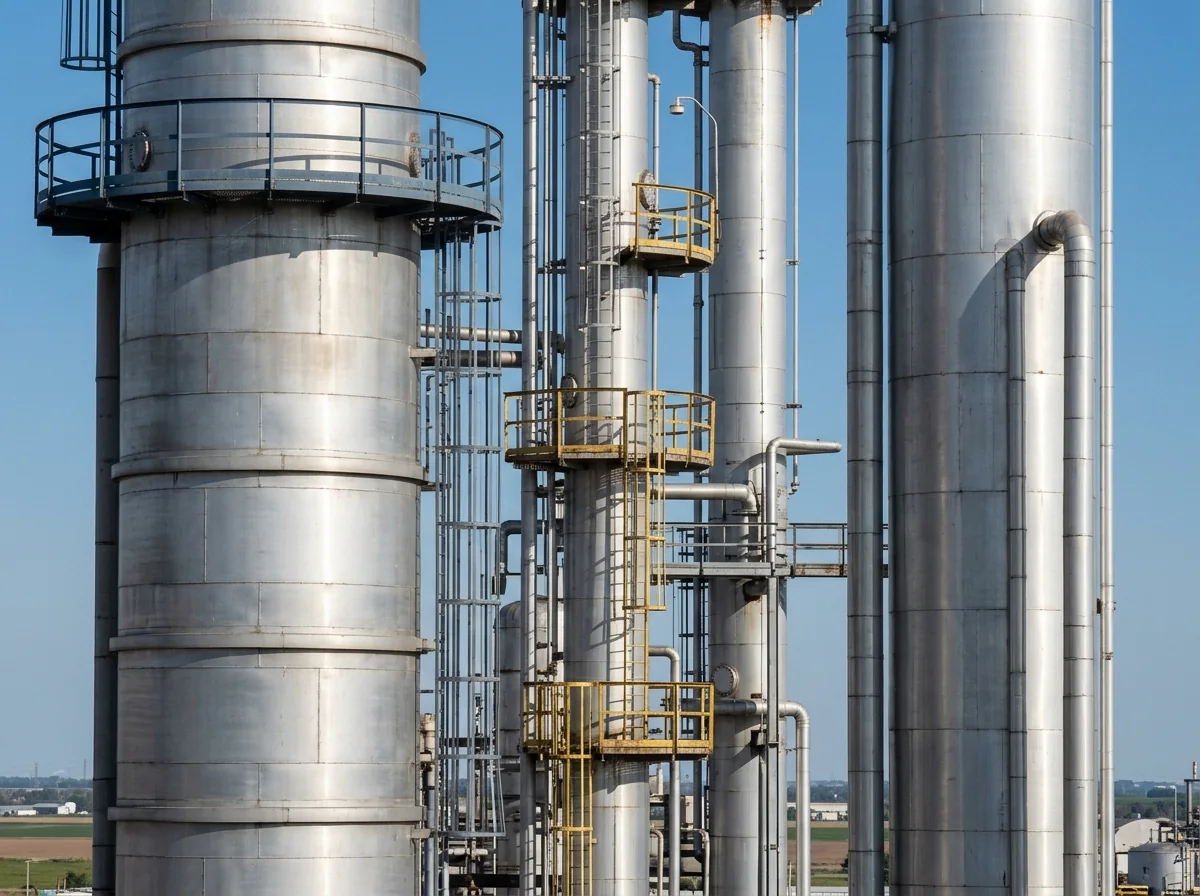
Chemical Processing
Reformer tube-support and heater fixturesInconel X-750 long-shank hex head bolts pass through the deeper grip of reformer tube-support and heater fixtures; the extended plain shank locates the joint before the nut takes up the thread. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same long-shank hex head bolt. Different material priorities.
Inconel X-750 material dataIncoloy 800HT
Tightly controlled carbon and Al + Ti for creep duty.
- Connection priority
- Tension and thermal expansion along the extended shank
- N08811 material control
- 800HT tightens the 800-family chemistry around creep performance. Its solution-treated, coarse-grain condition and N08811 identity should remain linked through forming and final acceptance. At the long grip inside the joint and the under-head seat, the relevant metal temperature can differ from the process or furnace set point.
Inconel 718
Precipitation-hardened strength for compact, highly loaded connections.
- Connection priority
- Tension and thermal expansion along the extended shank
- Strength after aging
- Machine-stock properties and final aged properties describe different states. The final heat-treatment lot and mechanical results establish the strength available in the installed part. At the long grip inside the joint and the under-head seat, the relevant metal temperature can differ from the process or furnace set point.
A-286
Aged iron–nickel alloy strength for hot bolting.
- Connection priority
- Tension and thermal expansion along the extended shank
- Grade 660 class
- An ASTM A453 Grade 660 order includes its class and corresponding processing requirements. The alloy name A-286 alone does not identify that acceptance condition. At the long grip inside the joint and the under-head seat, the relevant metal temperature can differ from the process or furnace set point.
From drawing to documented delivery
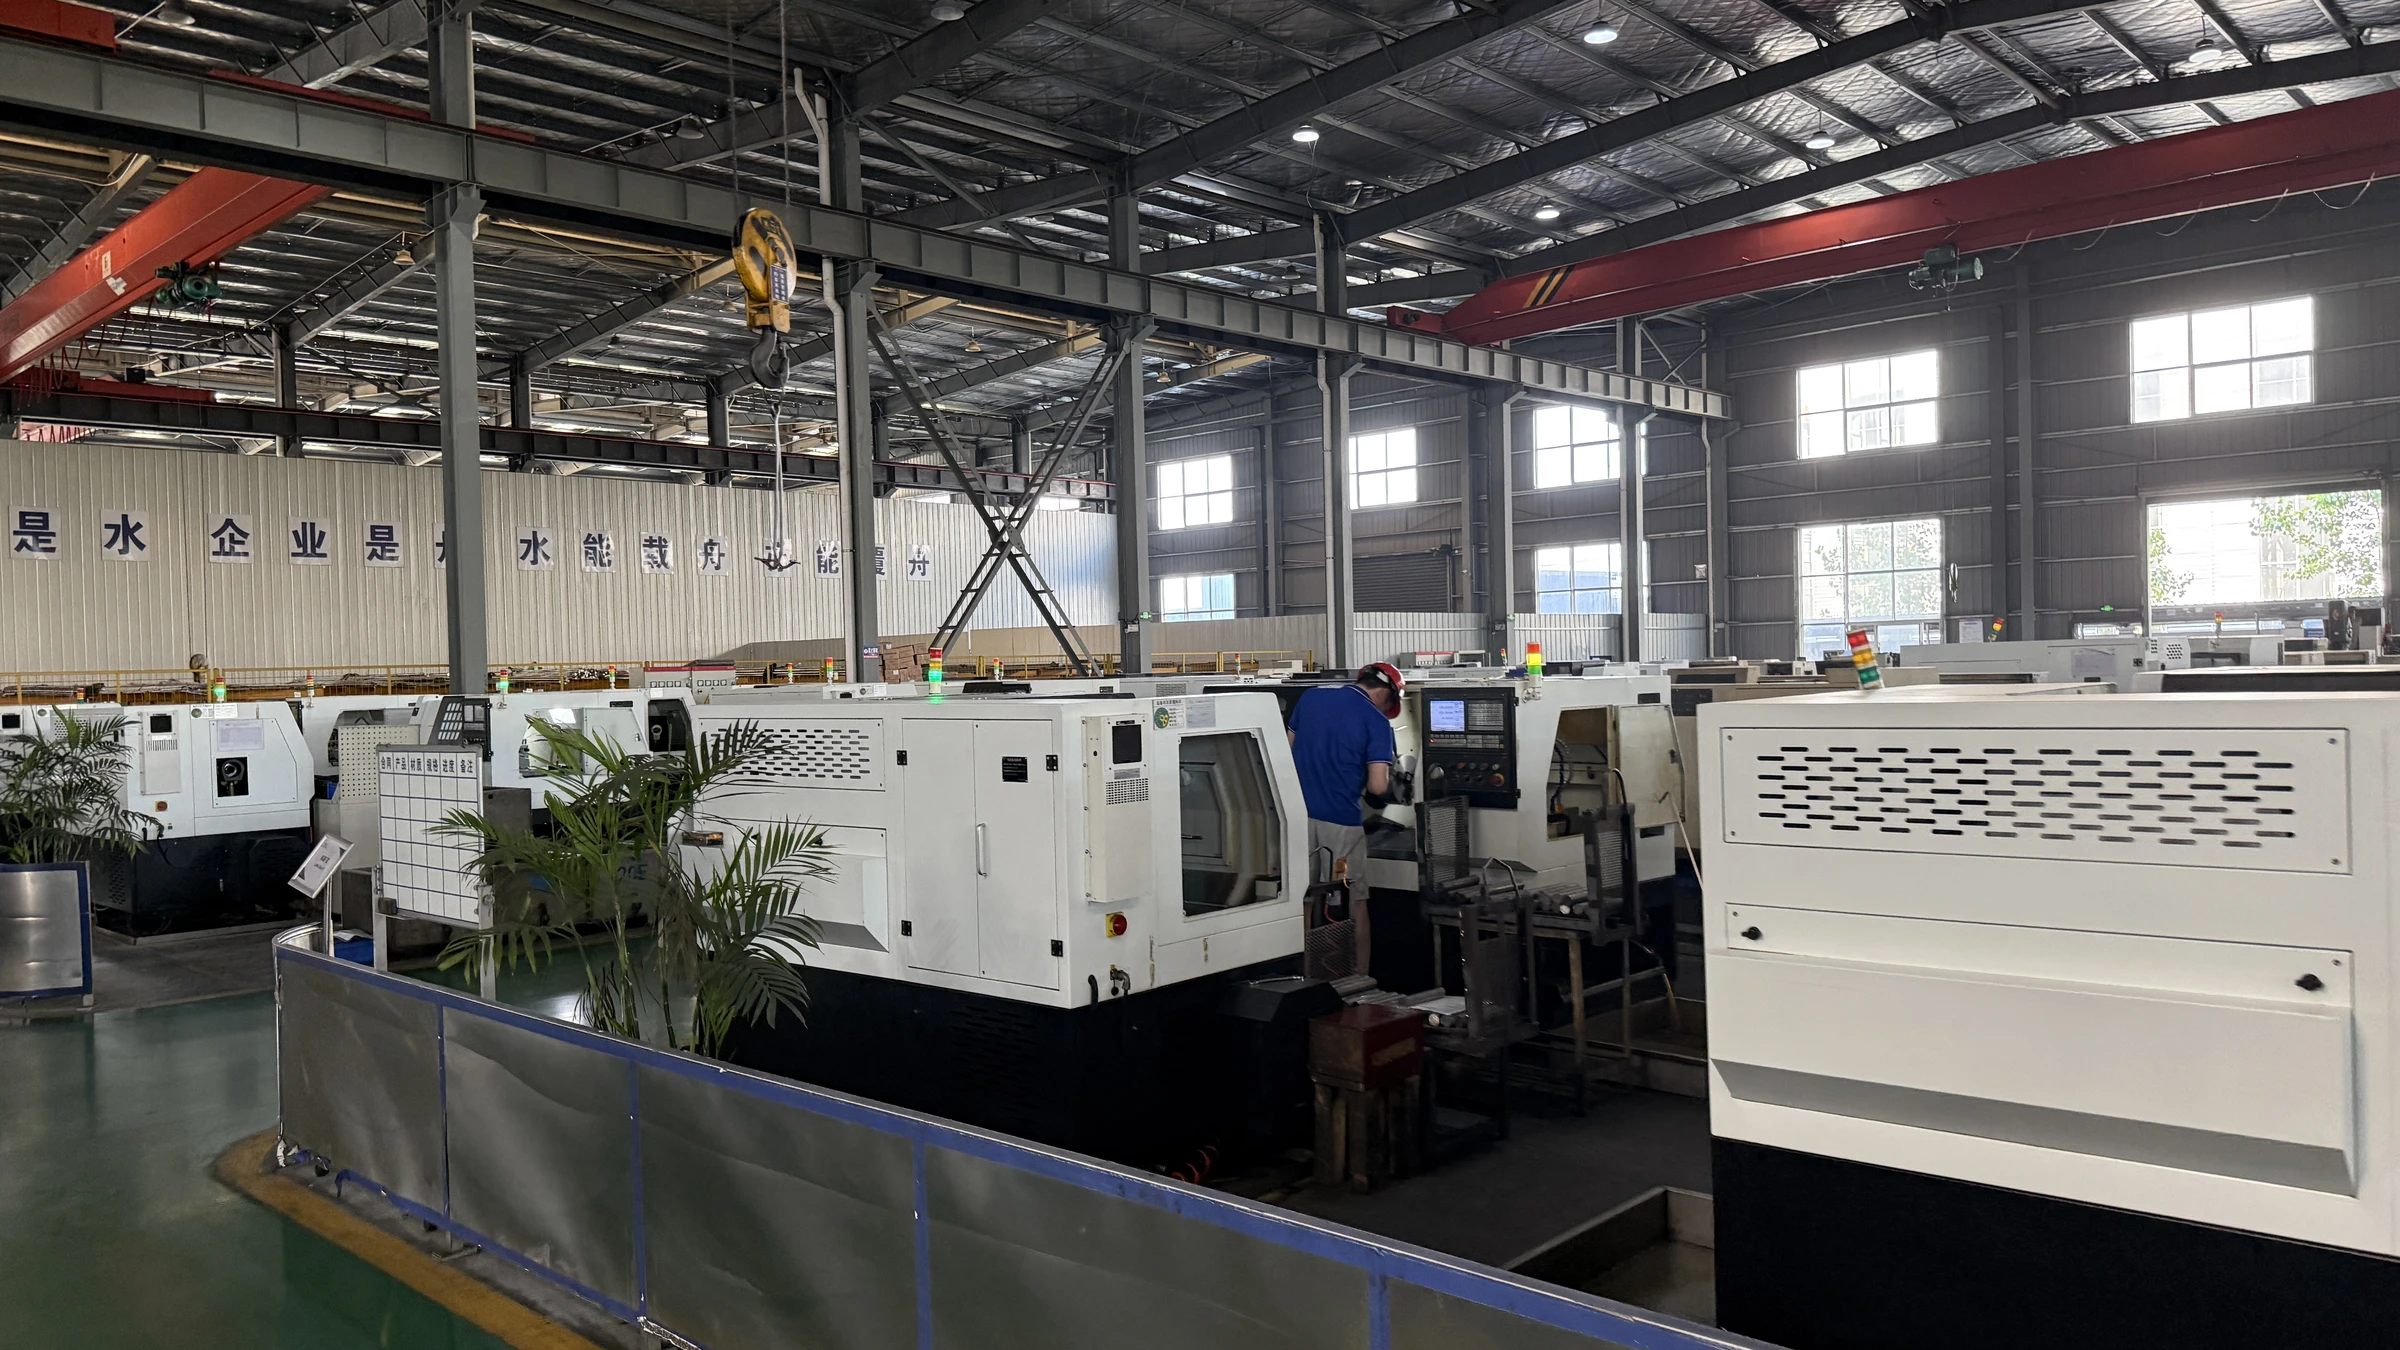
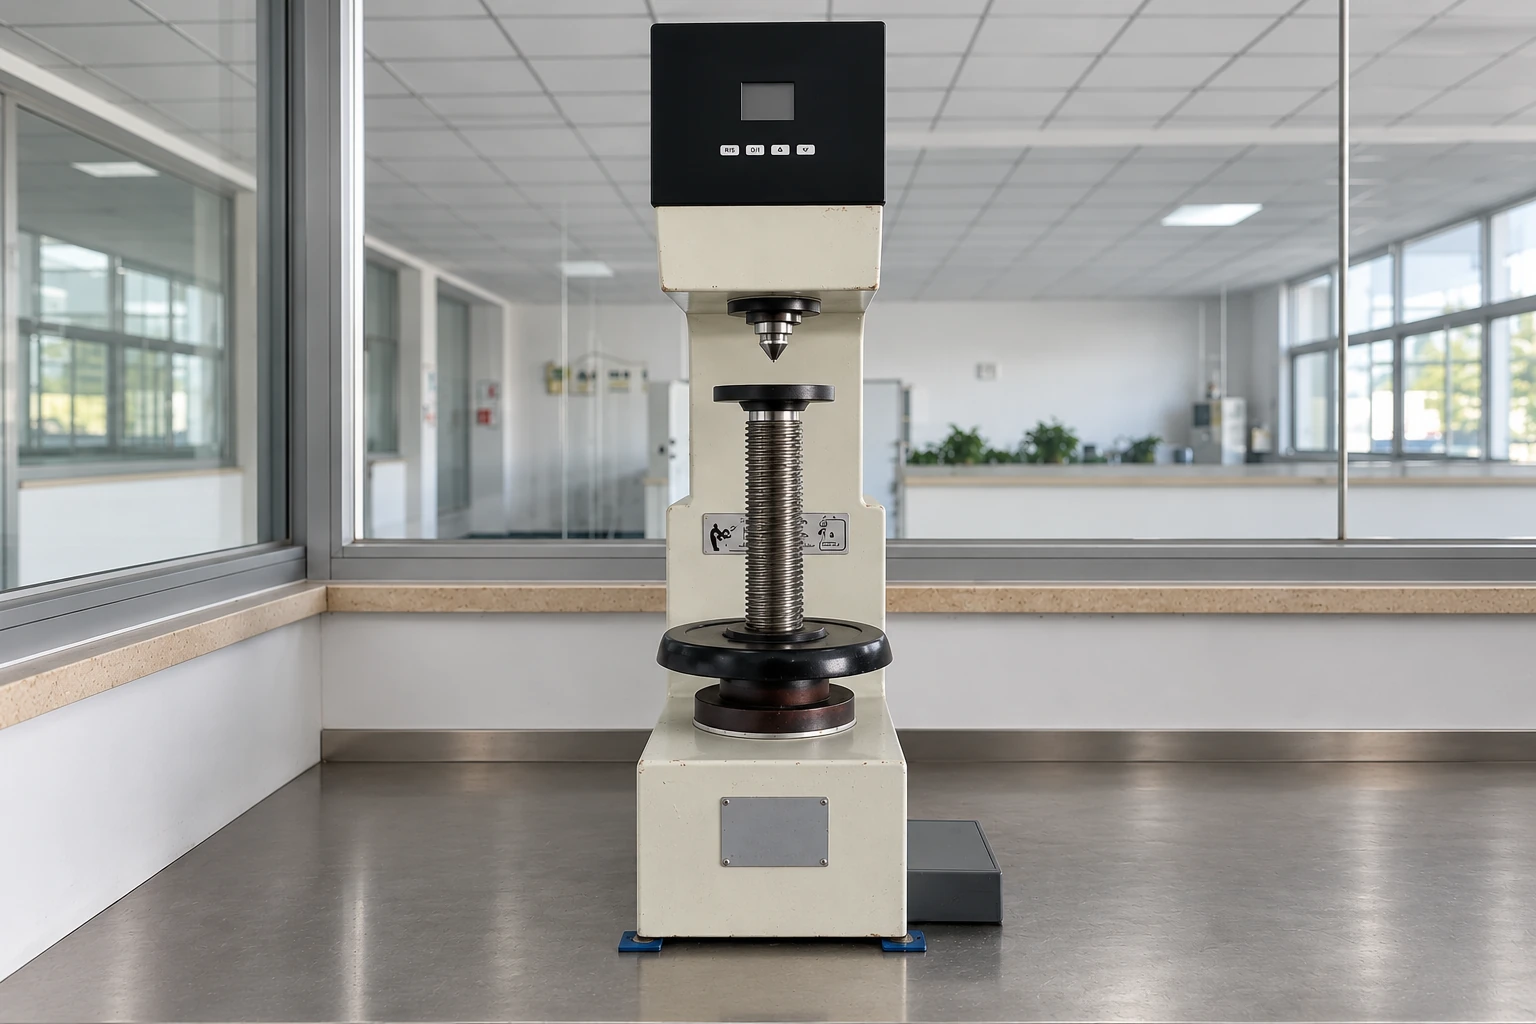
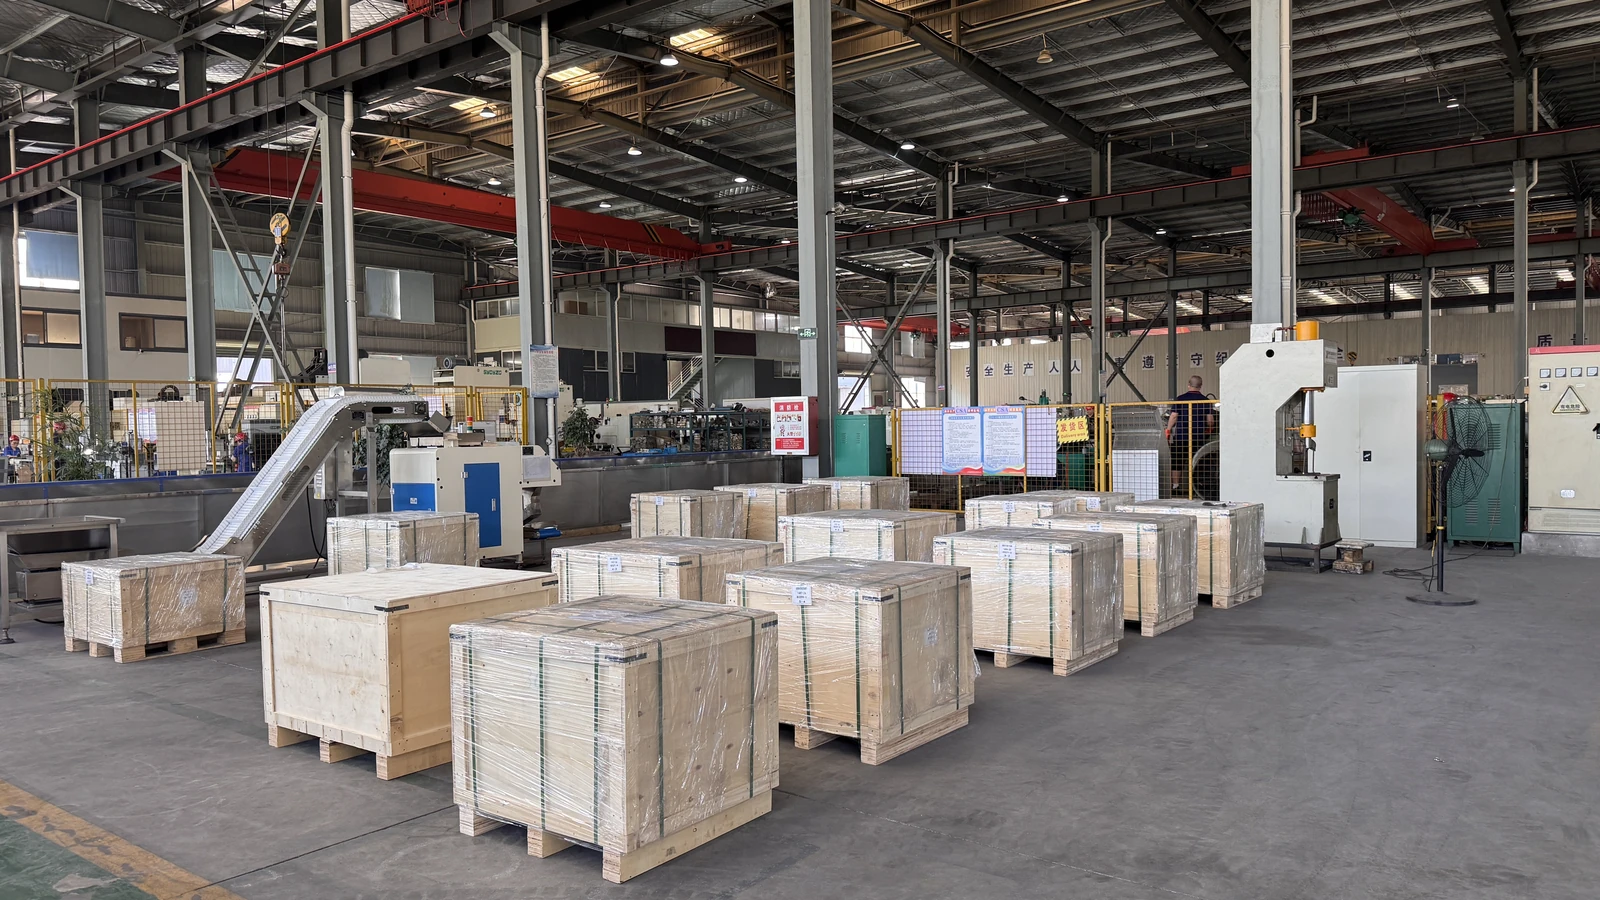
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N07750 · heat number · ordered condition
- Final-part acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Thread gauges · Head and shank dimensions
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your X-750 long-shank hex head bolt enquiry
Questions about X-750 long-shank hex head bolts
Why is total length insufficient for a long-shank bolt?
Two bolts of the same total length can put the thread runout in different places. The joint needs a defined grip length so its bearing or shear interface meets the intended shank section.