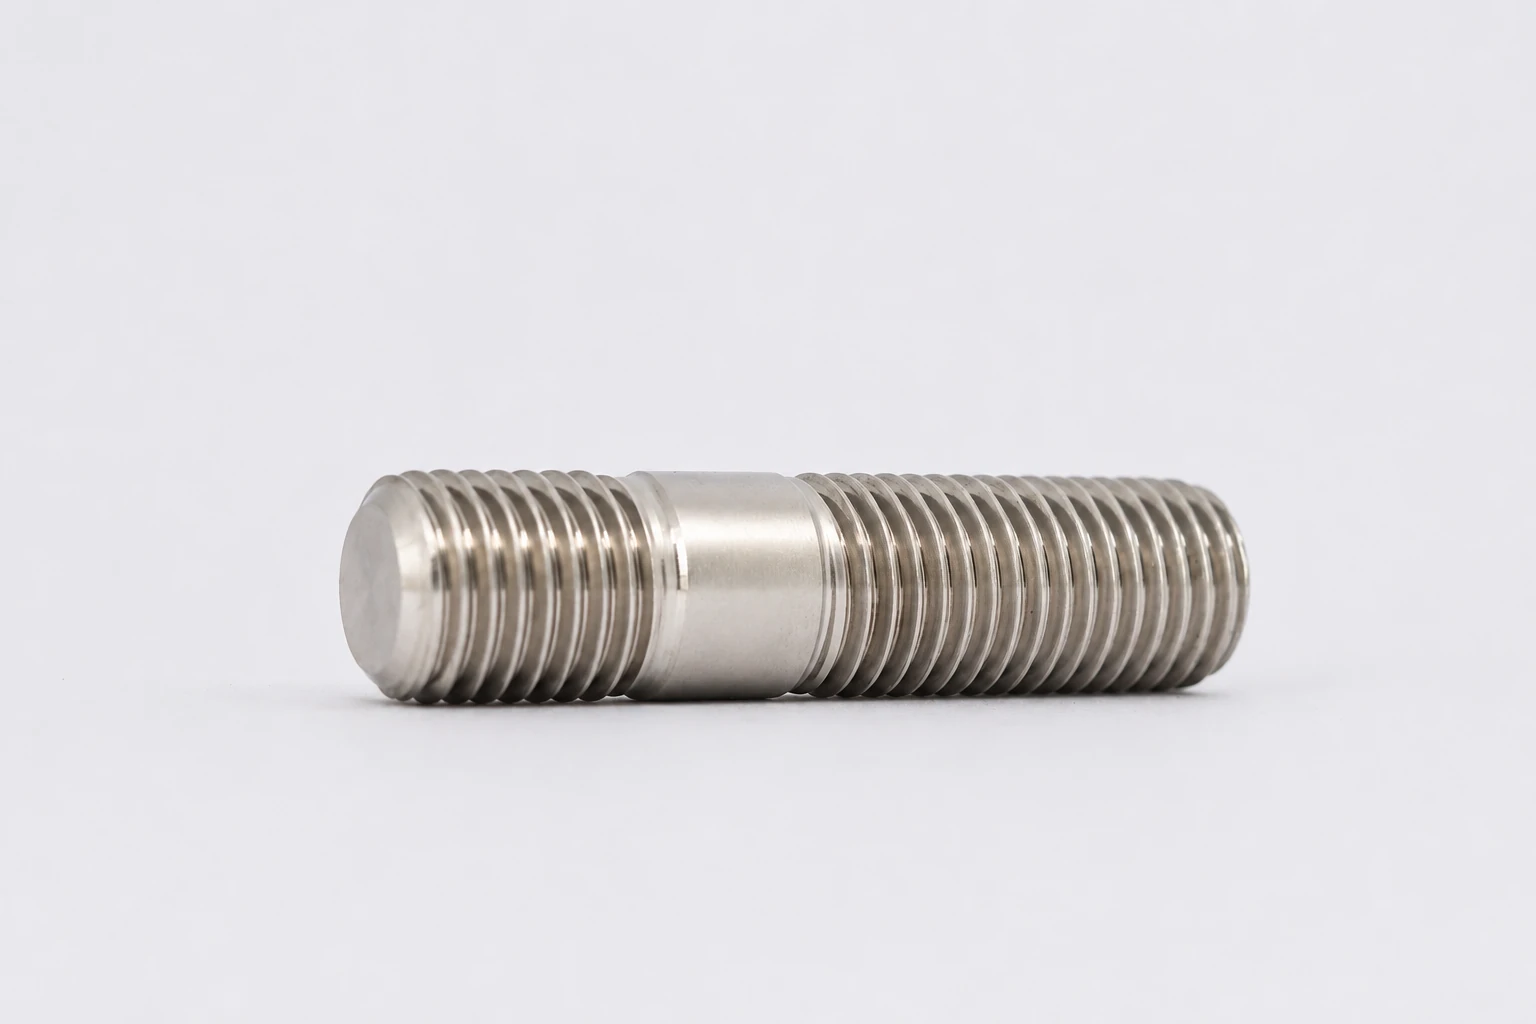
Inconel 718 Double-End Studs
ASME B18.31.2 · DIN 938 / 939ASTM B637 — bar / forgings
Inconel 718 double-end studs for hot casing and bonnet joints, where an aged high-strength alloy and a controlled unthreaded grip work together.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated / solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Inconel 718 in this connection
Precipitation hardening gives 718 its high strength; its specified condition is central to loaded and hot-service joints.
- Connection
- Steam-valve bonnets & turbine auxiliary casings
- Critical dimensions
- Overall length · central grip · each end length and fit
Which standard is on your order?
Raw Material Specifications
Finished-Stud Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated and agedFor A1014 bolting, solution treatment is followed by precipitation aging to develop the specified high-temperature strength.
What we can make in Alloy 718
Forms & dimension guide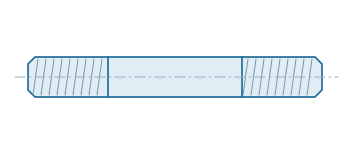
Clamping stud
Use for through-bolted covers and housings with access to both nuts. The plain grip spans the joint; independently sized threaded ends accommodate unequal nut-side clearances.
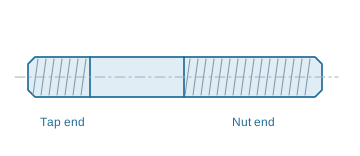
Tap-end stud
Use on valve bonnets and machine housings opened repeatedly for maintenance. The insertion end remains in the body while the outer nut is removed, reducing repeated wear of the housing thread.
- Product forms
- Equal threaded ends · Unequal threaded ends · Tap-end — specified fit
- Dimensional control
- Overall length · central grip · each end length and fit
- Manufacturing
- CNC-turn the central grip and shoulders, then produce the two thread ends to their separate lengths and fits.
- Final condition
- Solution treatment and aging establish the ordered strength and hardness. Hot-service and oilfield routes may differ.
- Inspection
- Heat-treatment lot · tensile / hardness · specified elevated-temperature tests
Where 718 fits — and what matters
Power & Turbines
Hot-gas access covers and inspection closuresInconel 718 double-end studs connect hot-gas access covers and inspection closures through a threaded body end and an accessible nut end. The plain shank spans the cover grip. Hot dwell and start-stop expansion act on the supported or moving component.
Furnaces & Heat Treatment
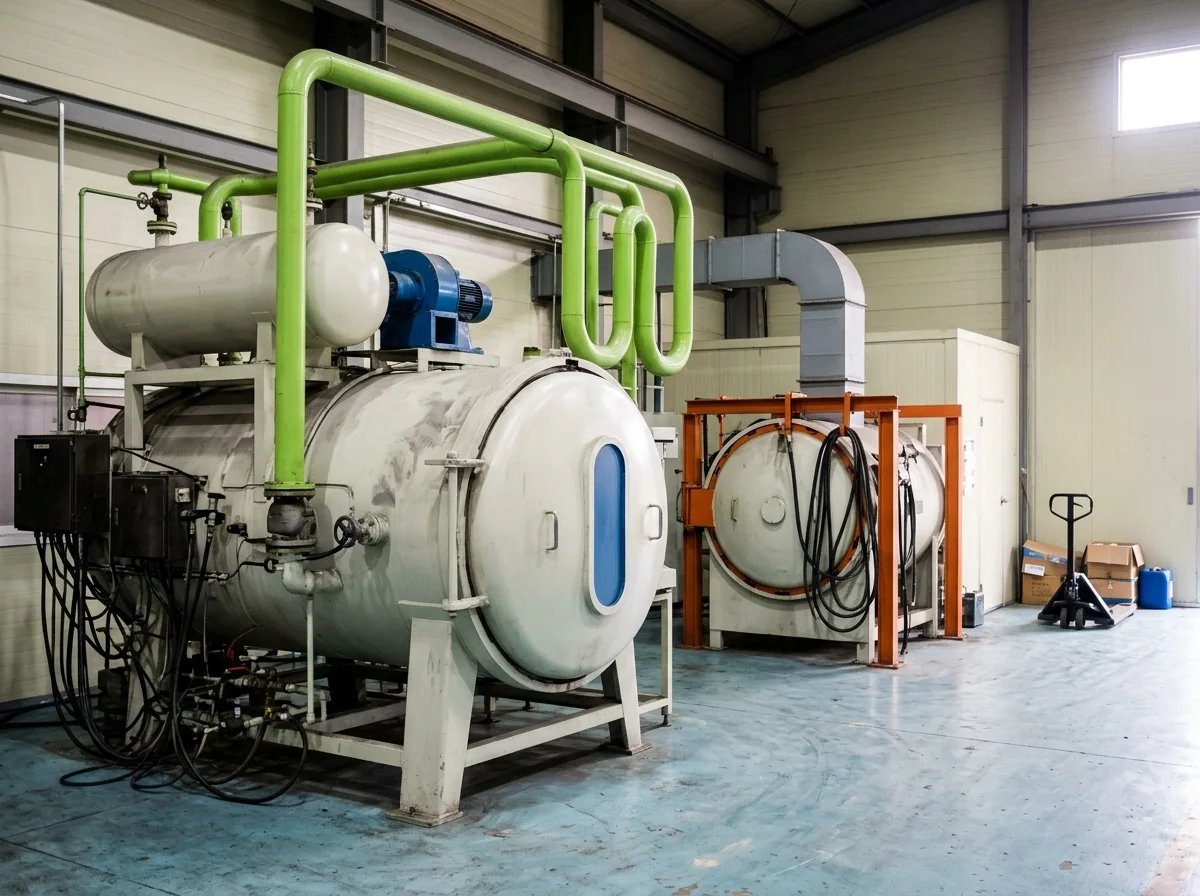
Retort and furnace-access coversInconel 718 double-end studs connect retort and furnace-access covers through a threaded body end and an accessible nut end. The plain shank spans the cover grip. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
Chemical Processing
Reformer access covers and hot-gas inspection closuresInconel 718 double-end studs connect reformer access covers and hot-gas inspection closures through a threaded body end and an accessible nut end. The plain shank spans the cover grip. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same double-end stud. Different material priorities.
Inconel 718 material dataInconel 625
Molybdenum and niobium provide solid-solution strength, combined with resistance to chloride pitting and crevice corrosion.
Inconel 625 Double-End StudsA-286
An iron-based precipitation-hardening alloy for high-strength connections operating at elevated temperature.
A-286 Double-End StudsIncoloy 800H
Controlled carbon and grain structure distinguish 800H from ordinary 800 for creep and stress-rupture duties.
Incoloy 800H Double-End StudsIncoloy 925
Age-hardenable nickel alloy combines strength with corrosion resistance for specified sour-service equipment.
Incoloy 925 Double-End StudsFrom drawing to documented delivery
- 01Drawing & BOMGrade, condition and part dimensions
- 02Sample lotOptional · typically ~20 days
- 03Production & testingTypically 25–35 days
- 04Documents & dispatchHeat-linked lots and packing
Connection & acceptance
Steam-valve bonnets & turbine auxiliary casings: Steam-valve metal temperature · start / stop cycles · aged-condition acceptance.
Material & final condition
Solution treatment and aging establish the ordered strength and hardness. Hot-service and oilfield routes may differ.
Connection inspection
Overall length · central grip · each end length and fit. Heat-treatment lot · tensile / hardness · specified elevated-temperature tests.
Build your 718 double-end stud enquiry
Upload drawing insteadQuestions about 718 double-end studs
Why is grip length important in a hot 718 double-end stud?
The grip spans the clamped stack and influences joint stiffness and thermal response. End-thread lengths establish engagement; the full drawing, rather than overall length alone, defines the replacement part.
Technical references & photo credits
Catalogue photography shows product form. Application examples connect alloy properties to equipment duties; they are not customer installation records. Quantities, schedules and the inspection scope are confirmed in the quotation.