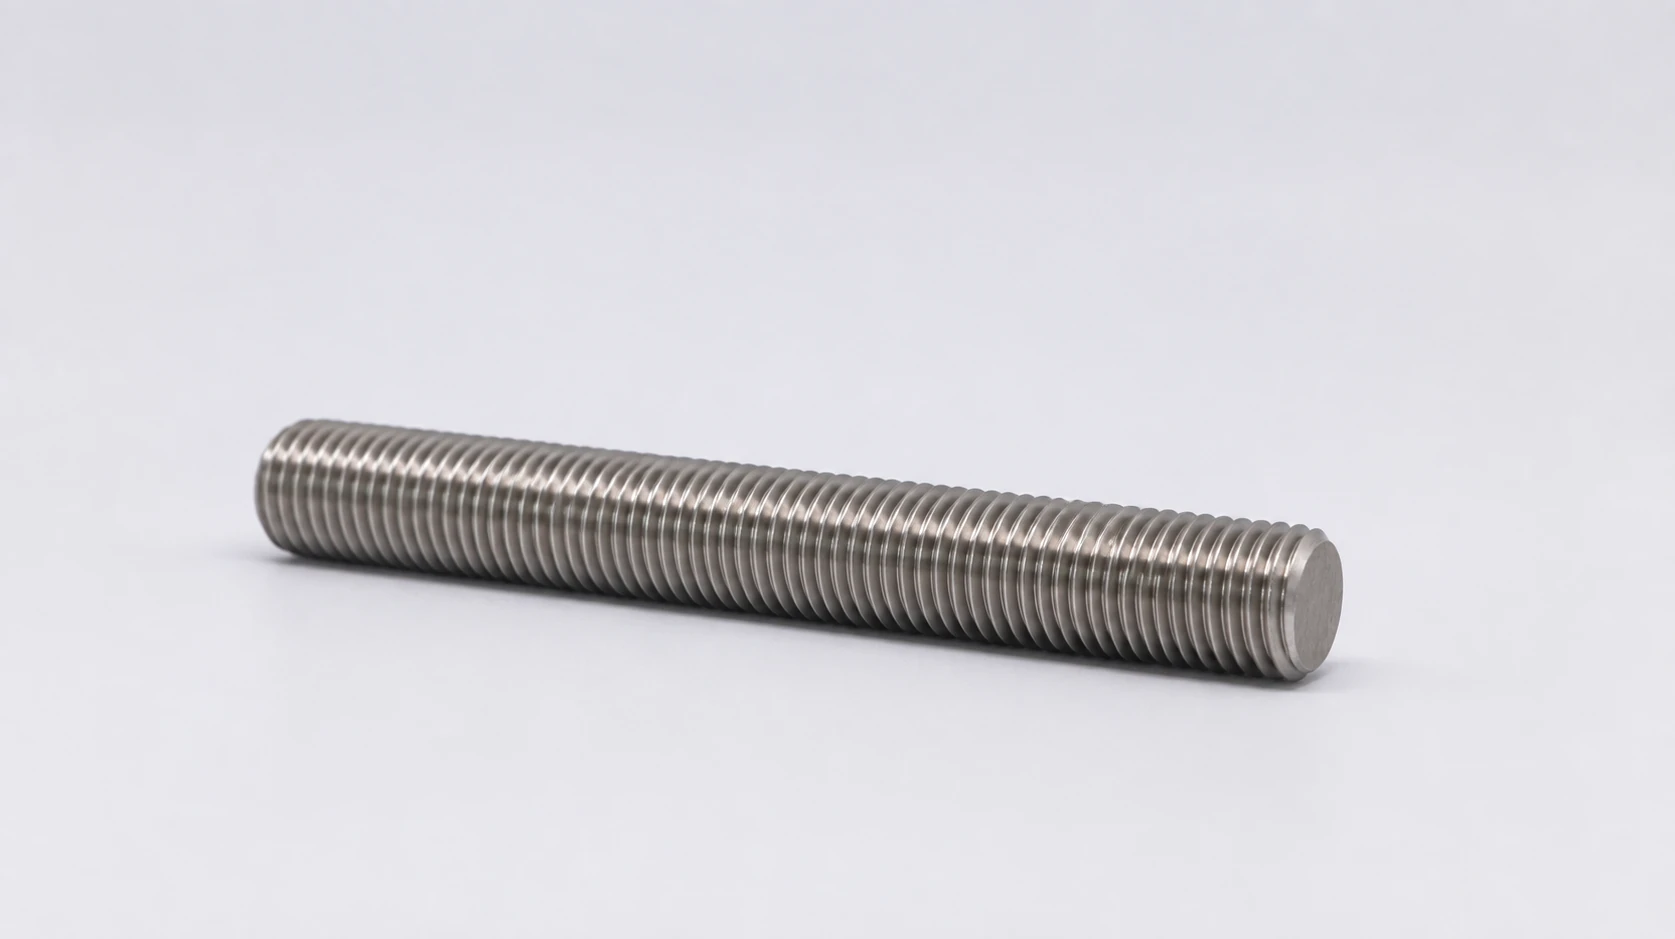
904L Stud Bolts
ASME B18.31.2ASTM A276
904L stud bolts bring molybdenum- and copper-bearing resistance to selected acids to flange and cover joints. The stud condition, mating nuts and end form determine how the assembly carries and retains clamp load.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealedSolution annealing and rapid cooling retain alloying elements in solution and restore the specified corrosion-resistant condition.
What we can make in 904L
Fully threaded
Two nuts clamp the flange or cover; usable thread length spans the assembled grip.
Double-end
A plain centre spans the grip, with a threaded portion at each end for the nuts.
Tap-end
One end engages a tapped casing; the exposed end accepts the cover nut.
- Threads
- Metric · UNC · UNF · 8UN · UNJ
- Forms
- Continuous thread · Double-end · Tap-end
- Final condition
- Solution annealed
- Inspection
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
Manufacturing route
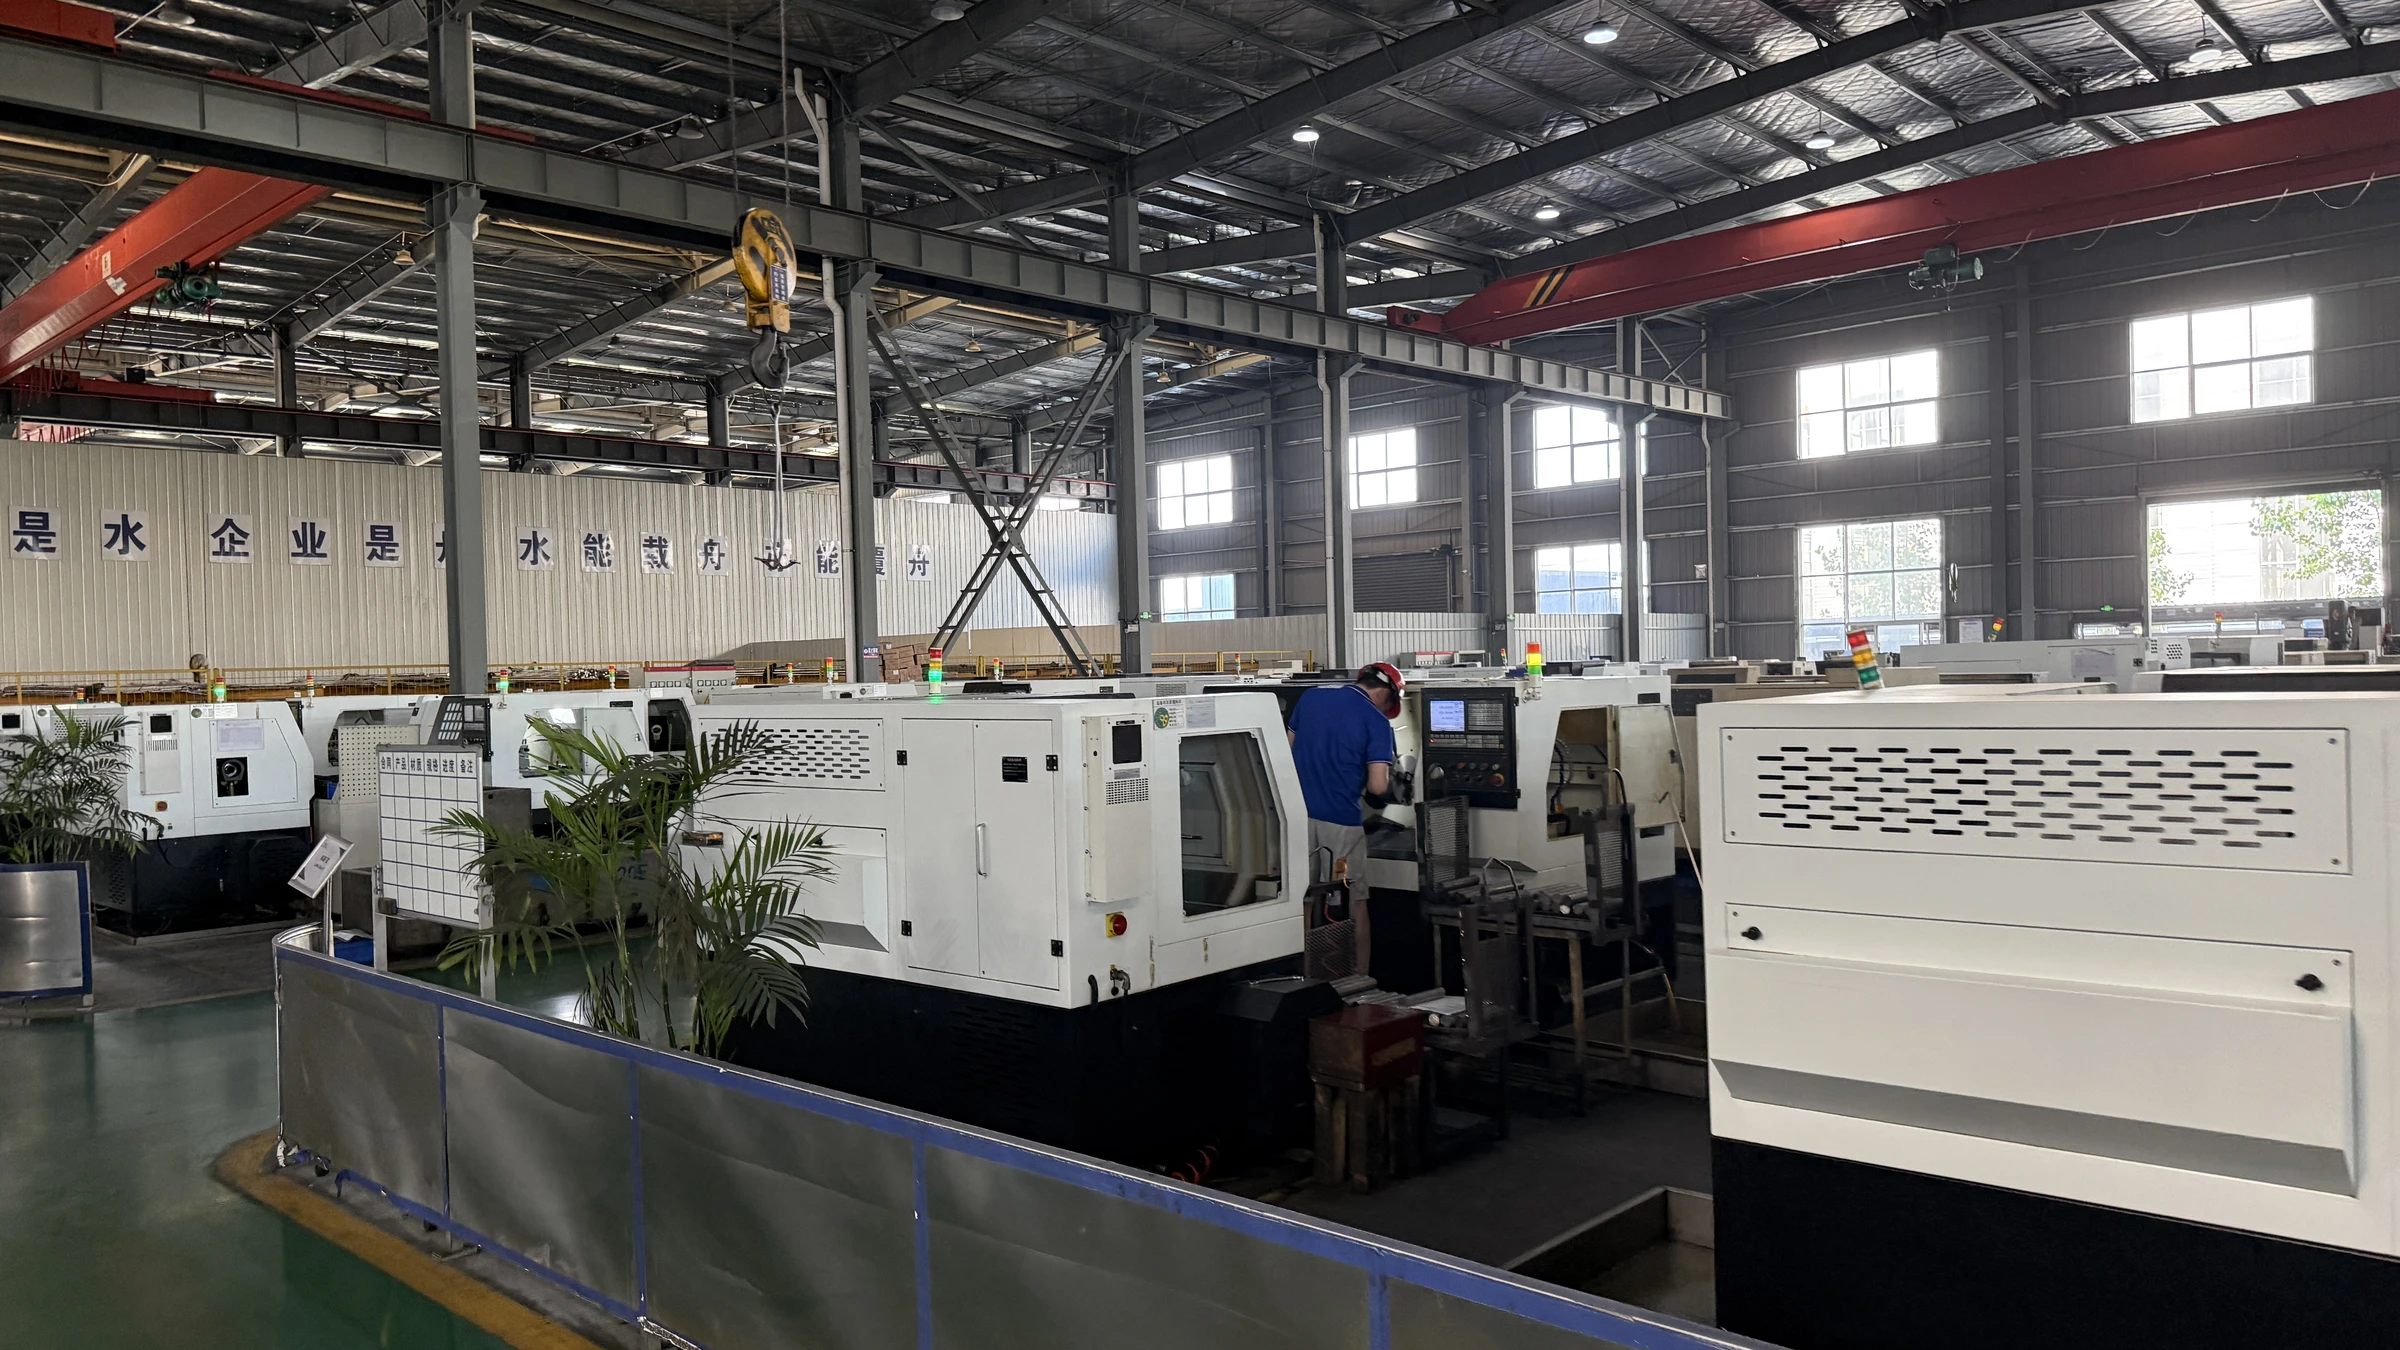
CNC machining suits samples and special end forms. Repeat lots use cut-to-length stock with rolling or cutting selected for the ordered thread and material condition.
Heat treatment & final condition
The final annealed or specified strengthened condition is linked to the lot; an aging treatment is not assumed for a solid-solution alloy.
Finished geometry
End lengths, runout and effective thread engagement are checked separately from overall length; tap ends are gauged to their own fit requirement.
Where 904L fits — and what matters
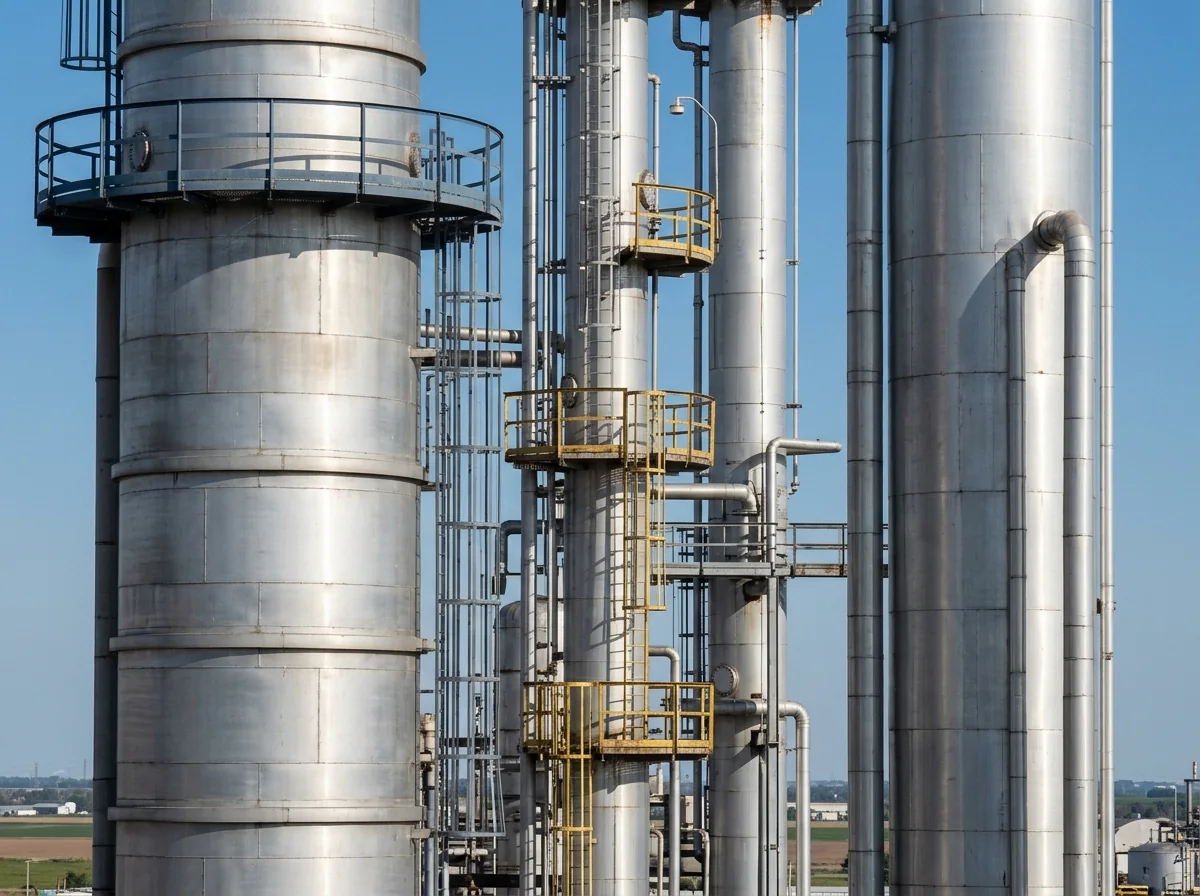
Chemical Processing
Chemical pump covers and reactor connections904L stud bolts & threaded rods clamp chemical pump covers and reactor connections with nuts on the exposed ends, keeping the stud in place when a cover is removed. Process liquid can remain at the contact after the exposed surface drains.
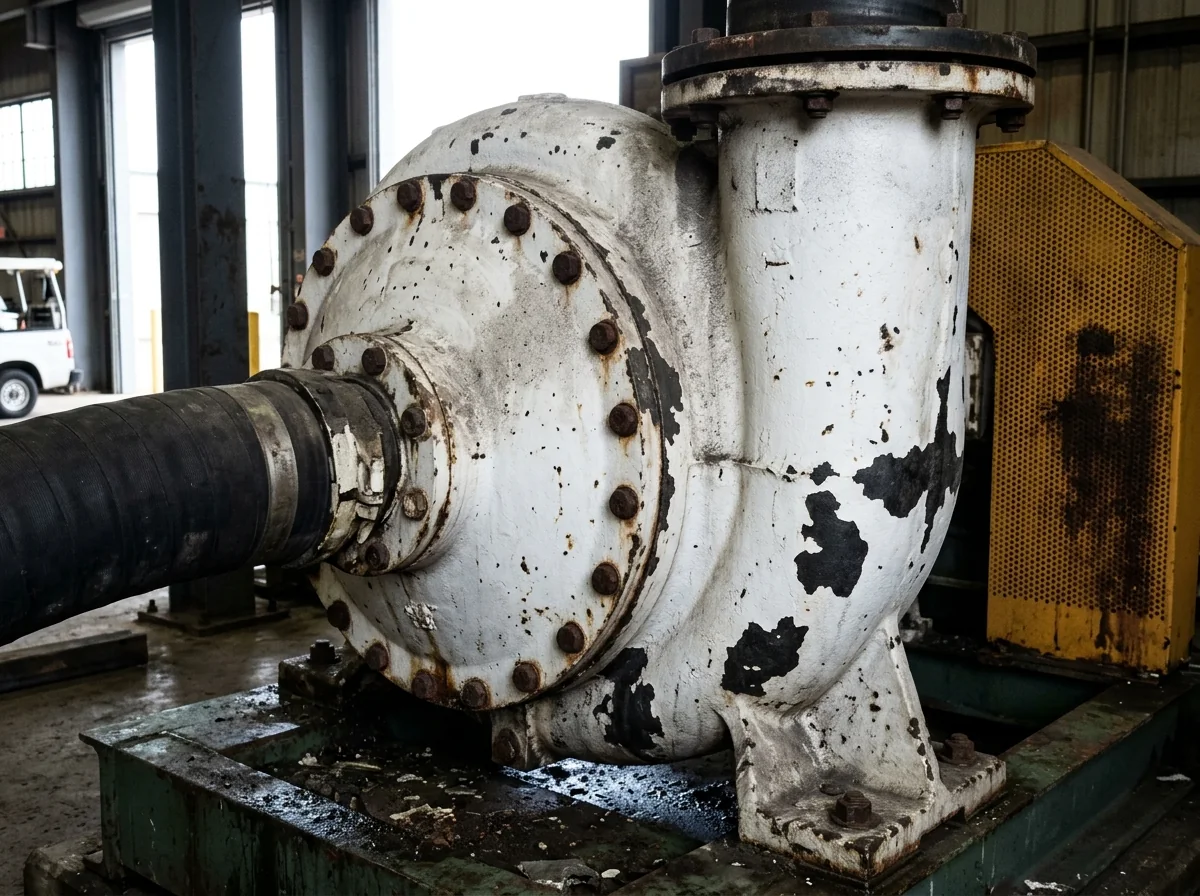
Pumps, Valves & OEM
Pump casings and valve bonnets904L stud bolts & threaded rods clamp pump casings and valve bonnets with nuts on the exposed ends, keeping the stud in place when a cover is removed. Repeated maintenance makes fit, engagement and access part of the component specification.
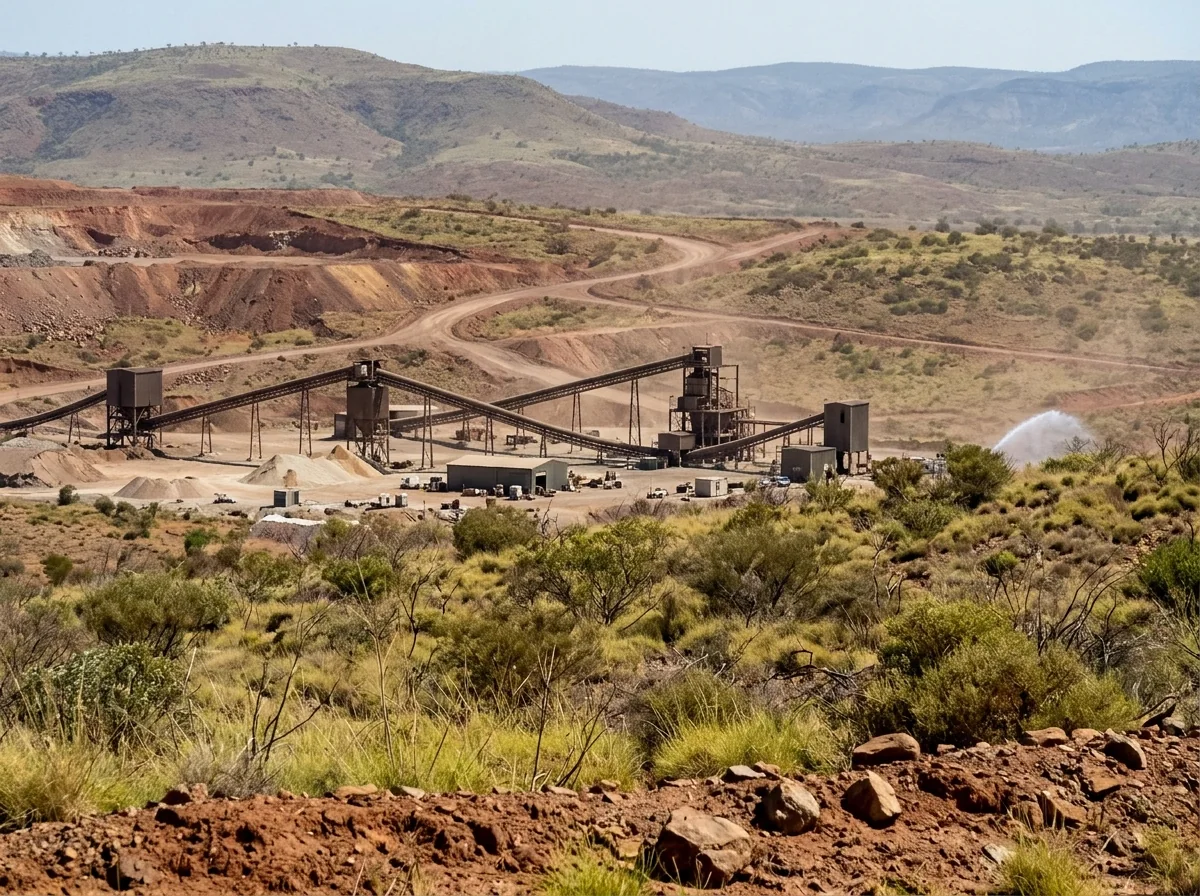
Mining & Mineral Processing
Chemical-recovery pump and vessel covers904L stud bolts & threaded rods clamp chemical-recovery pump and vessel covers with nuts on the exposed ends, keeping the stud in place when a cover is removed. Leach solution and deposits act on the installed part; corrosion duty is separate from abrasive wear.
Same stud. Different material priorities.
904L material dataHastelloy C-276
Resistance to chemically aggressive, mixed process streams.
- Connection priority
- Stud tension and clamp-load retention
- Process liquid and shutdown chemistry
- C-276 is selected for its nickel–chromium–molybdenum–tungsten chemistry. Residual product, cleaning liquid and oxidising contamination can expose a sheltered connection differently from the main flow. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
Inconel 625
Solid-solution strength and resistance to aggressive process liquids.
- Connection priority
- Stud tension and clamp-load retention
- Annealed or solution-annealed 625
- The delivery condition affects strength and high-temperature response. Keep the specified condition with the component’s mechanical acceptance; 718-style aging is not the strengthening route for 625. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
Hastelloy C-22
Corrosion resistance across oxidising and reducing process exposures.
- Connection priority
- Stud tension and clamp-load retention
- Production and cleaning cycles
- C-22’s chromium-bearing chemistry is relevant when chemical exposure changes between operating and cleaning cycles. Include both liquids when comparing it with C-276 or a B-type nickel alloy. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
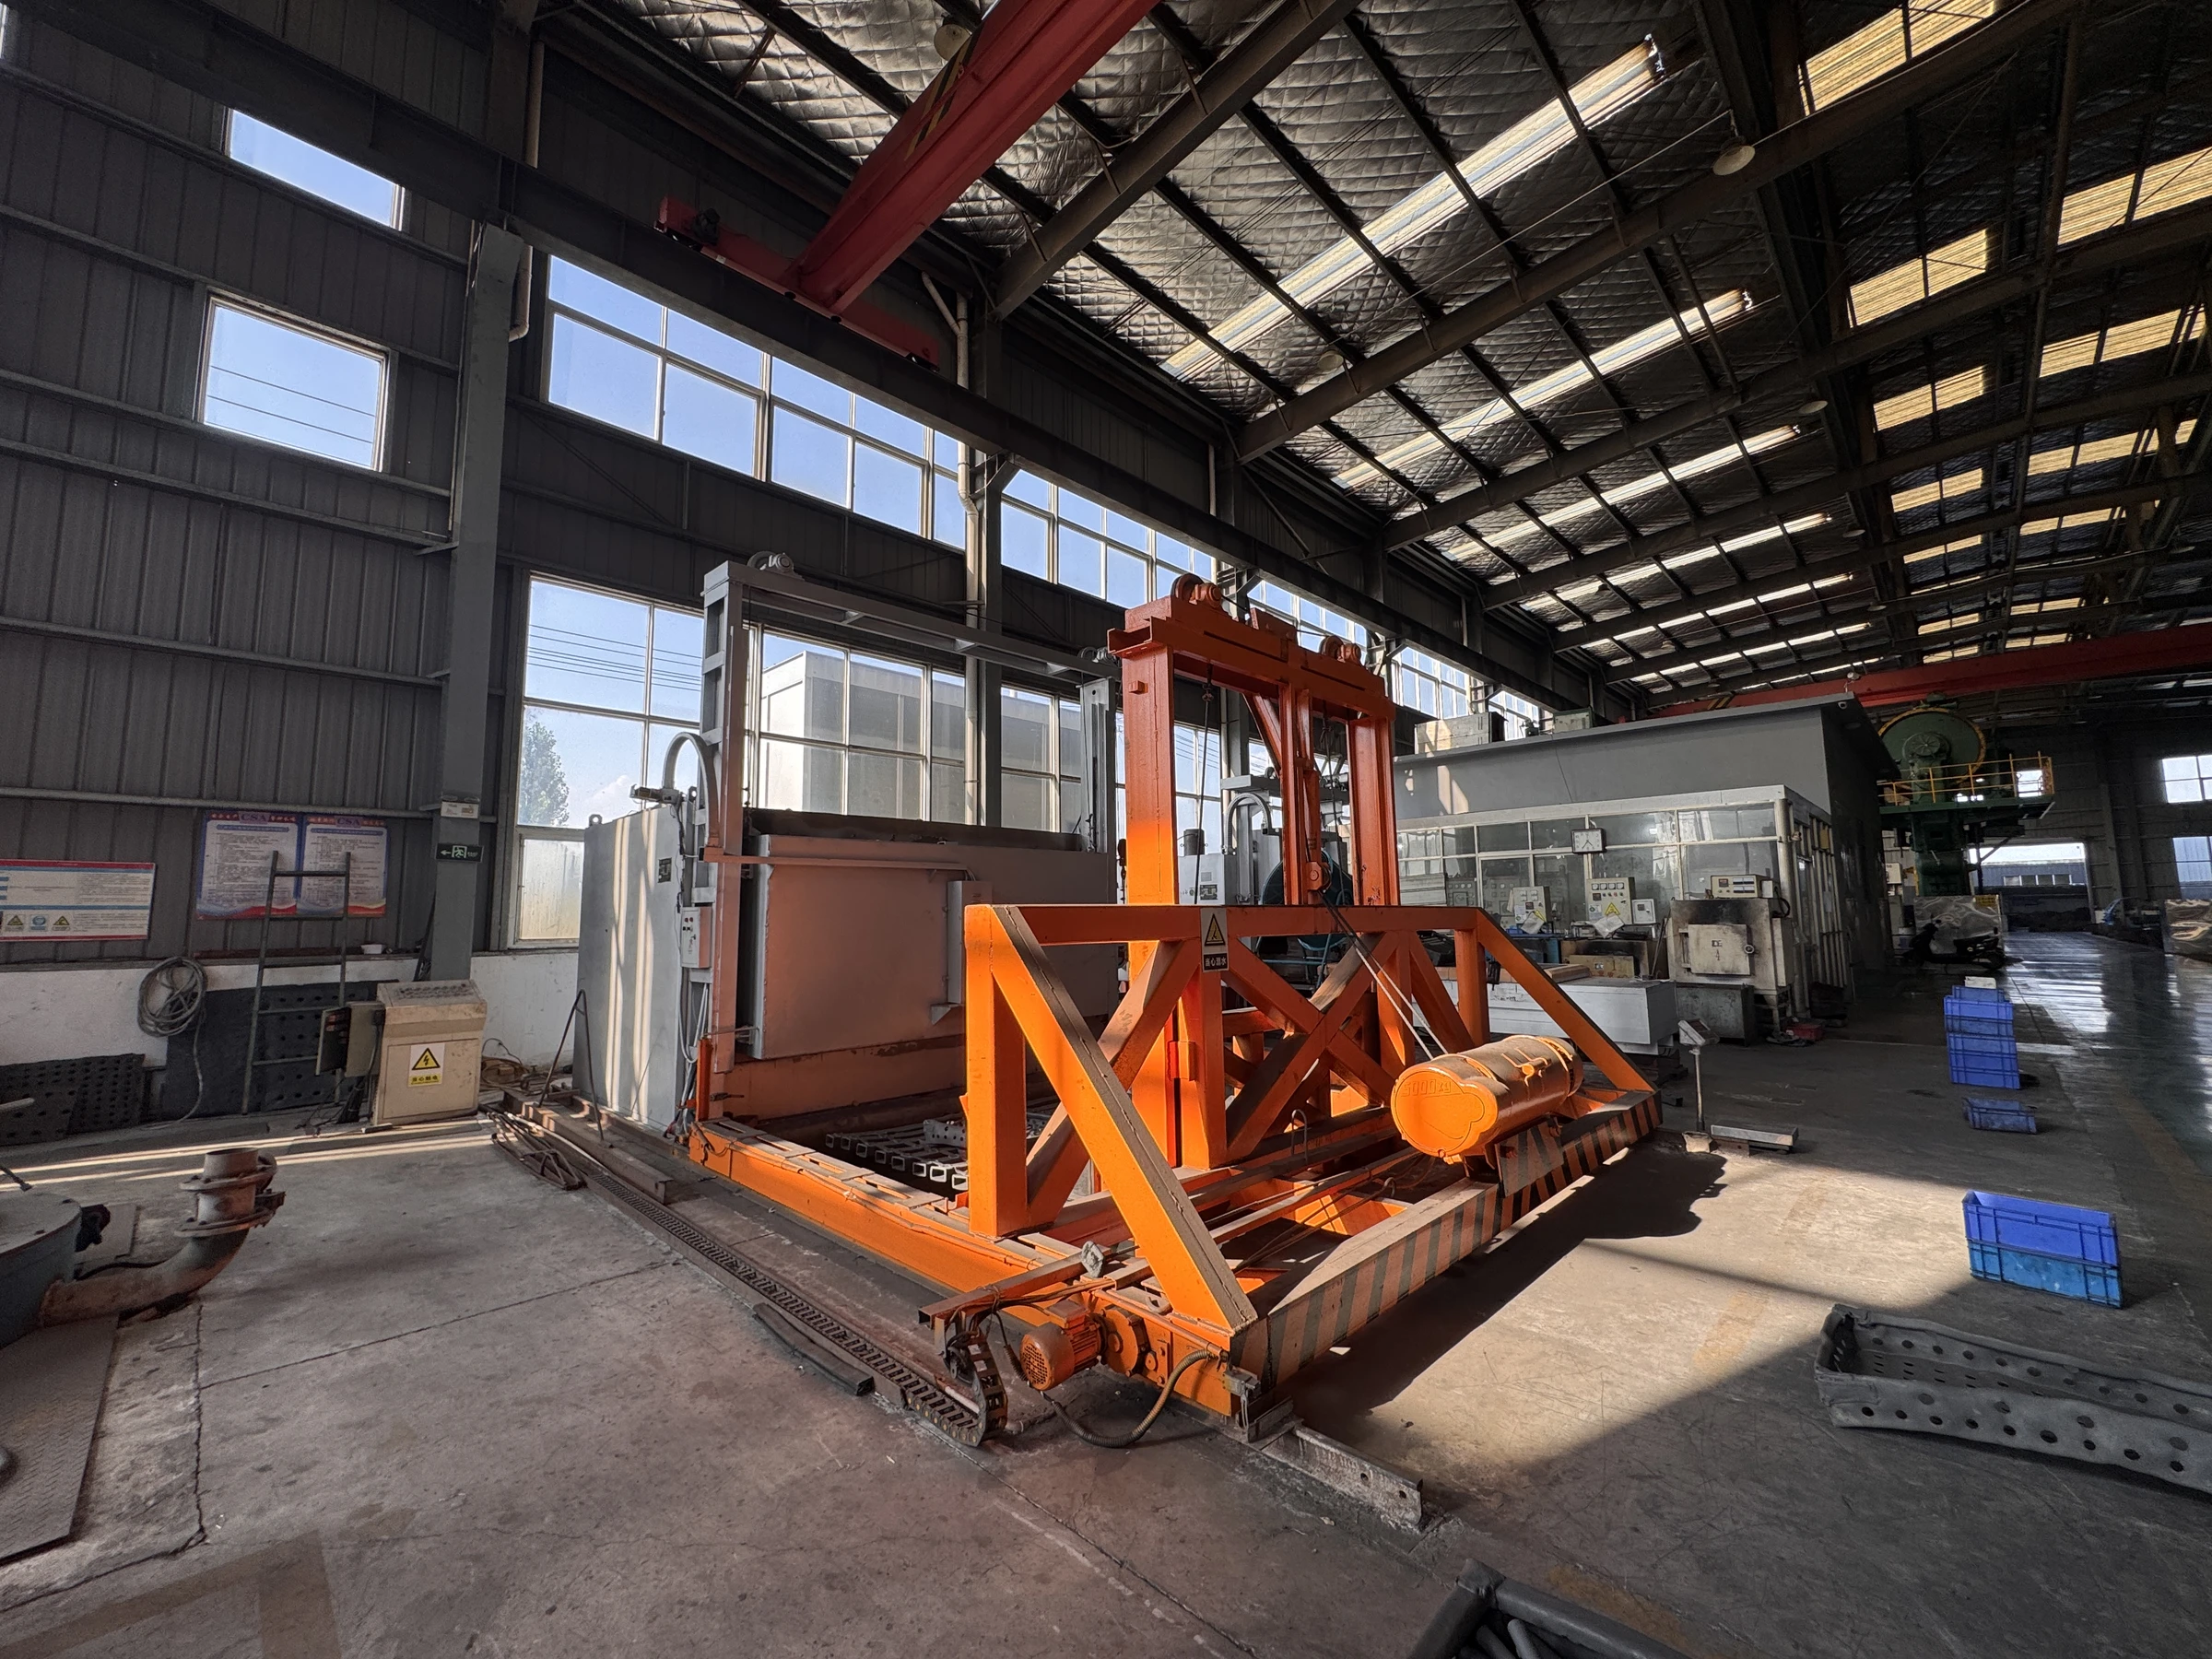
- 02Material & formingGrade, heat and manufacturing route
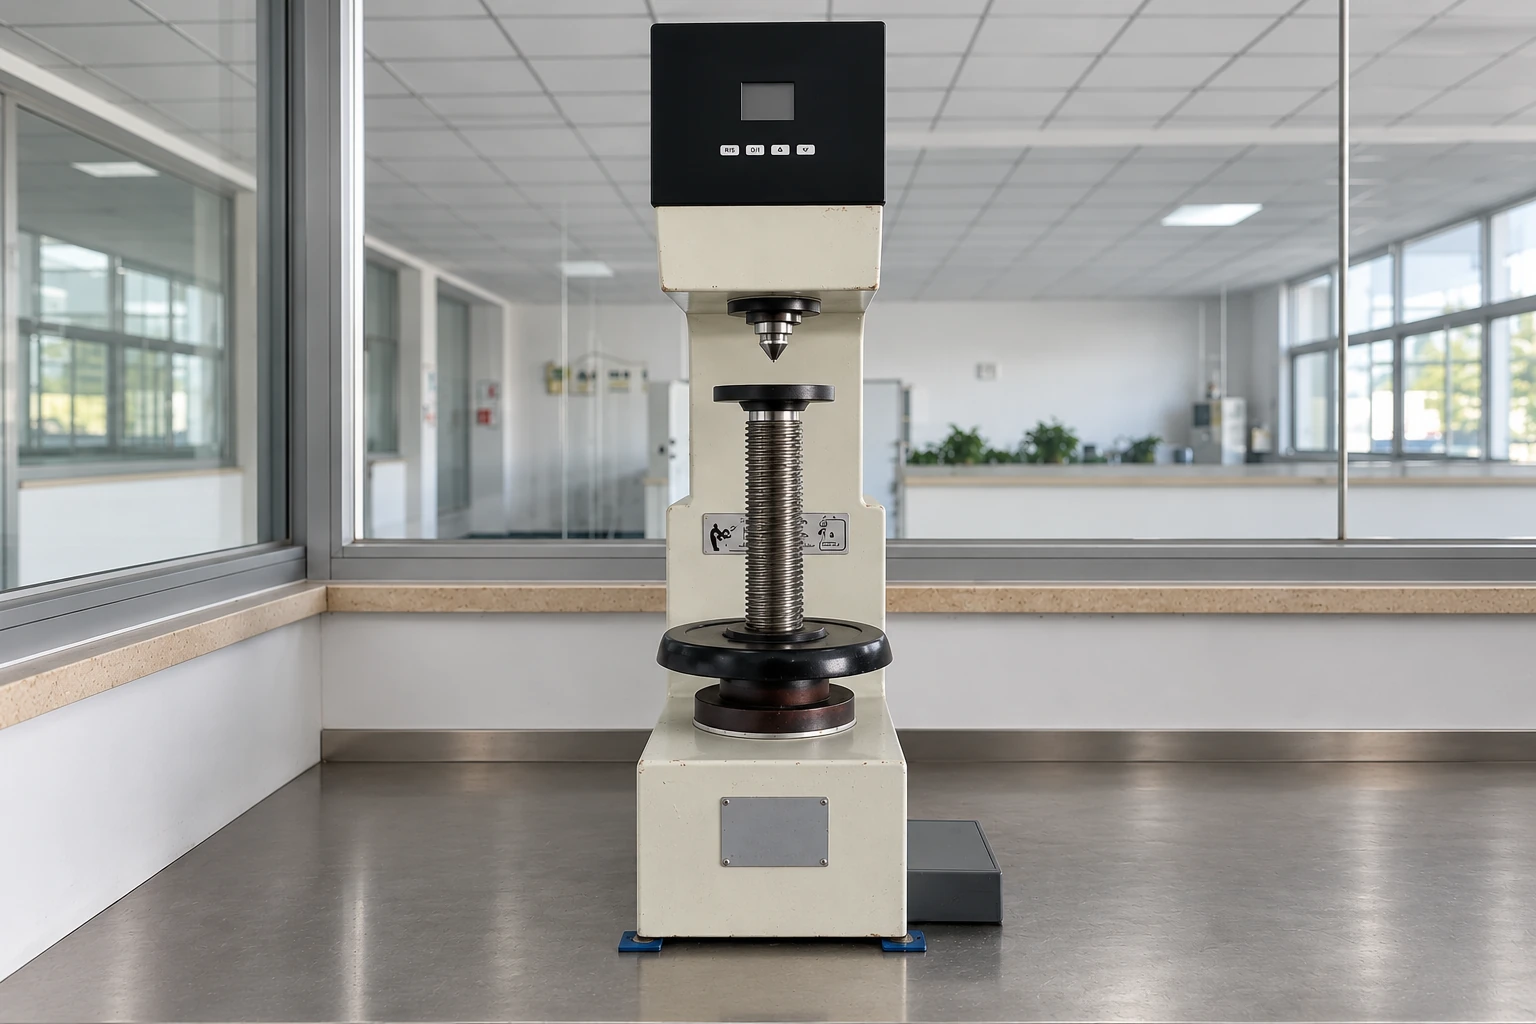
- 03Final inspectionGeometry, threads and ordered tests
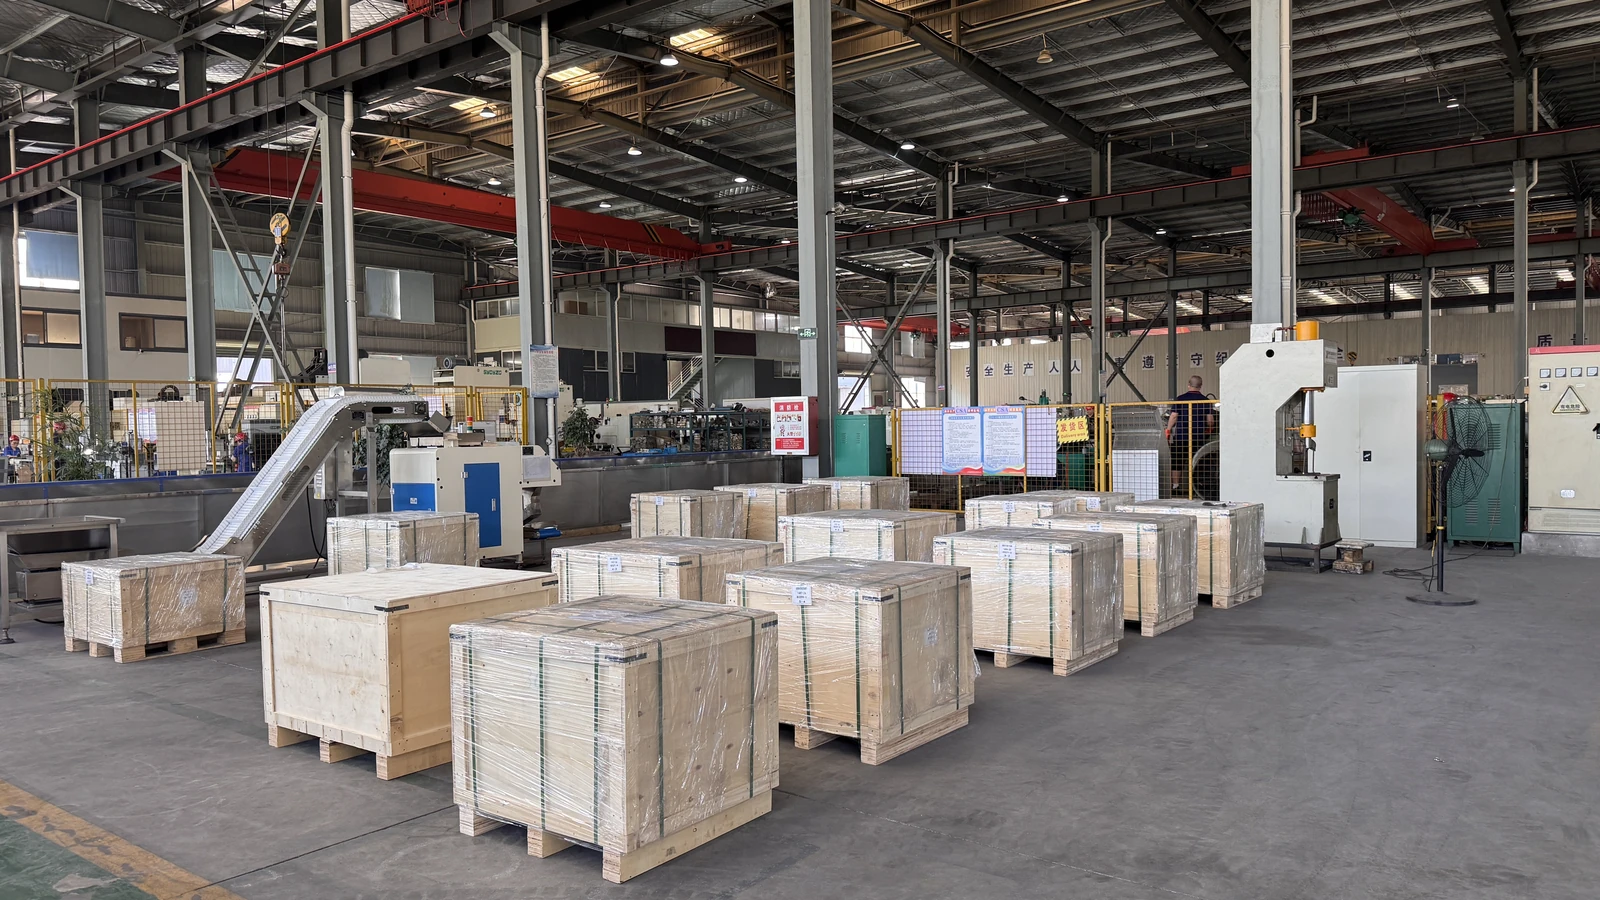
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N08904 · heat number · ordered condition
- Final-part acceptance
- Grade chemistry, supplied condition and ordered mechanical requirements.
- Dimensional record
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Matching Kit
Flange Stud Bolt Kits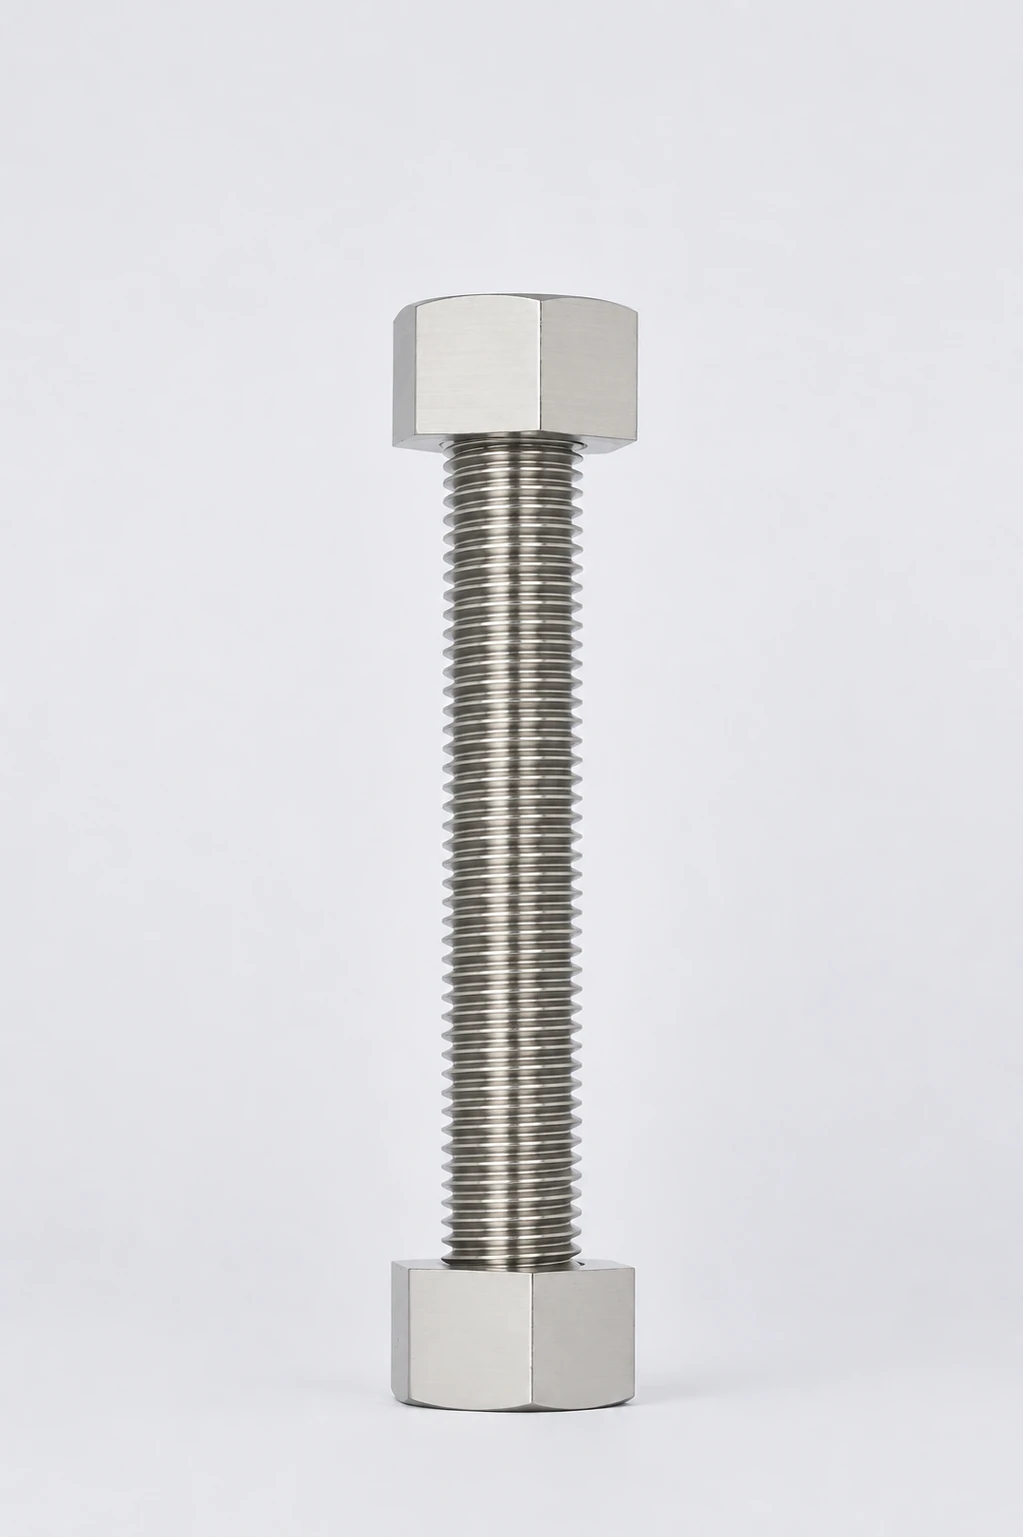
Build your 904L stud enquiry
Questions about 904L stud bolts & threaded rods
Does changing the stud alloy also change the nut selection?
The nut needs compatible internal threads, sufficient engaged height and a specified material condition. Select lubricant or surface treatment with the stud–nut pair, because assembly friction affects the preload obtained from tightening.