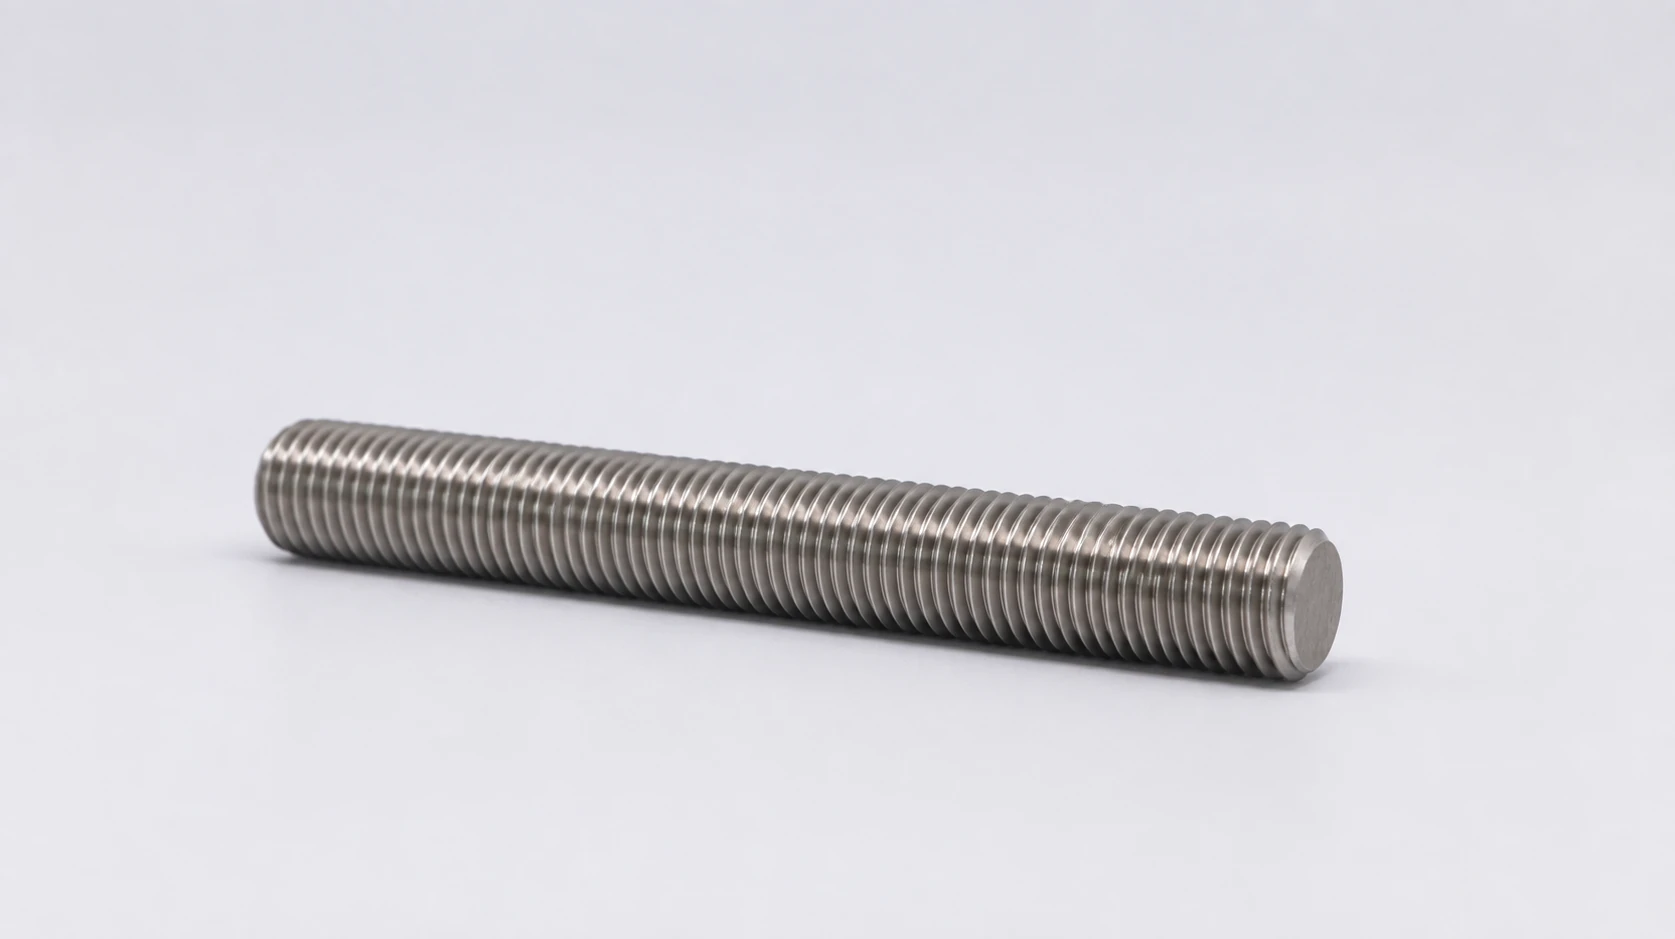
17-4 PH Stud Bolts
ASME B18.31.2ASTM A564
17-4 PH stud bolts bring aging-controlled strength and hardness to flange and cover joints. The stud condition, mating nuts and end form determine how the assembly carries and retains clamp load.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated (Condition A) / Age hardened H900 / Age hardened H1025 / Age hardened H1150
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Finished-Stud Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated, then aged to the specified H conditionCondition A is the solution-treated starting state; aging to H900, H1025 or H1150 sets the final strength–toughness balance.
What we can make in 17-4 PH
Fully threaded
Two nuts clamp the flange or cover; usable thread length spans the assembled grip.
Double-end
A plain centre spans the grip, with a threaded portion at each end for the nuts.
Tap-end
One end engages a tapped casing; the exposed end accepts the cover nut.
- Threads
- Metric · UNC · UNF · 8UN · UNJ
- Forms
- Continuous thread · Double-end · Tap-end
- Final condition
- Solution treated (Condition A) · Age hardened H900 · Age hardened H1025 · Age hardened H1150
- Inspection
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
Manufacturing route
CNC machining suits samples and special end forms. Repeat lots use cut-to-length stock with rolling or cutting selected for the ordered thread and material condition.
Heat treatment & final condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
End lengths, runout and effective thread engagement are checked separately from overall length; tap ends are gauged to their own fit requirement.
Where 17-4 PH fits — and what matters
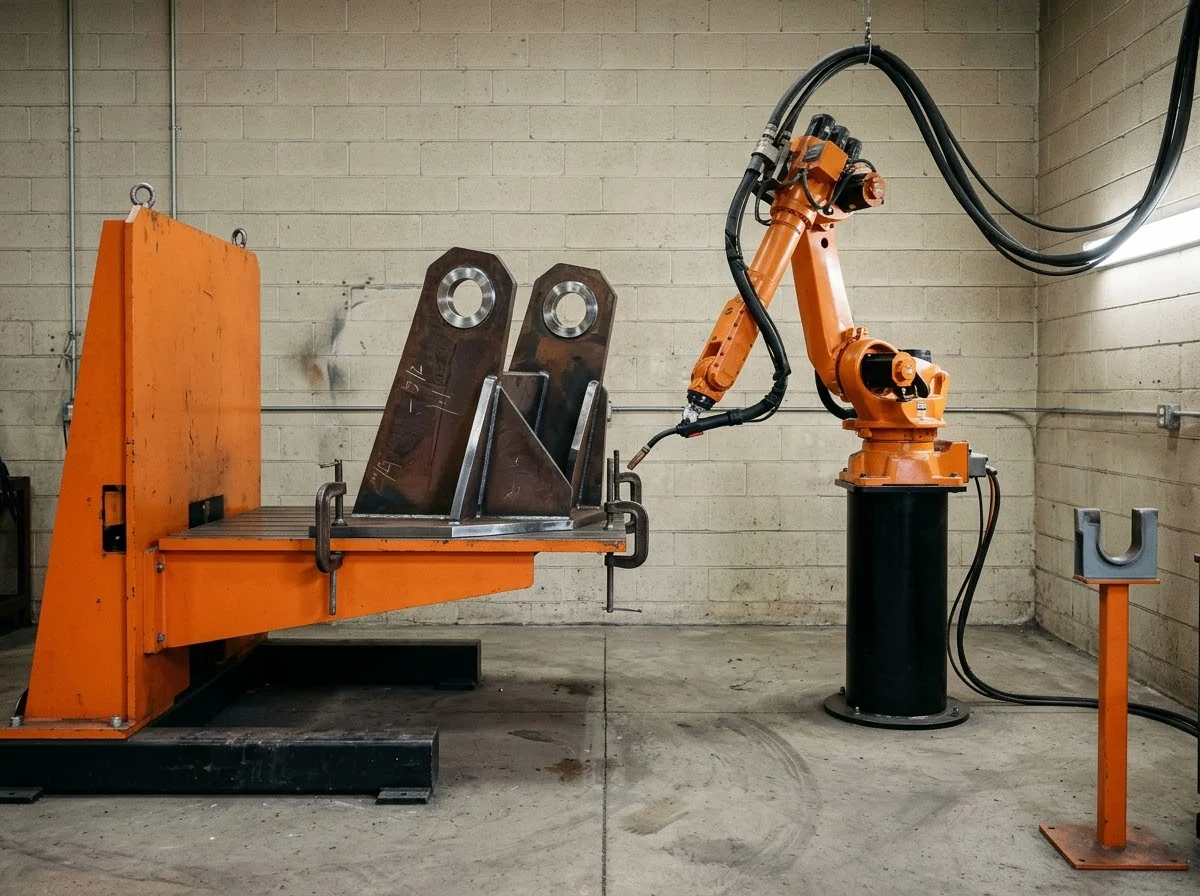
Industrial Machinery & Automation
Machine housings and service covers17-4 PH stud bolts & threaded rods clamp machine housings and service covers with nuts on the exposed ends, keeping the stud in place when a cover is removed. Alignment, operating cycles and replacement access define the working interface.
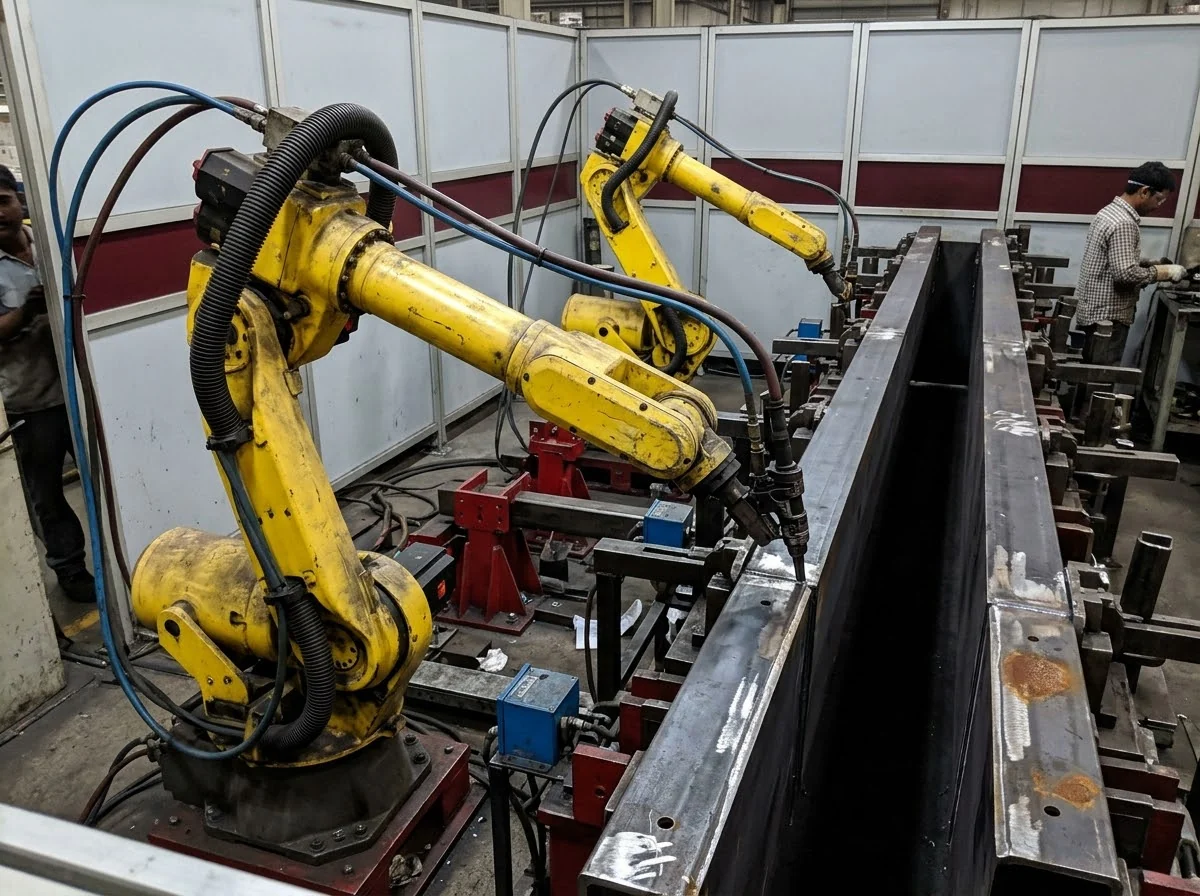
Automotive & EV Manufacturing Equipment
Test-equipment housings17-4 PH stud bolts & threaded rods clamp test-equipment housings with nuts on the exposed ends, keeping the stud in place when a cover is removed. Repeated tooling changes require consistent seating and repeatable assembly dimensions.
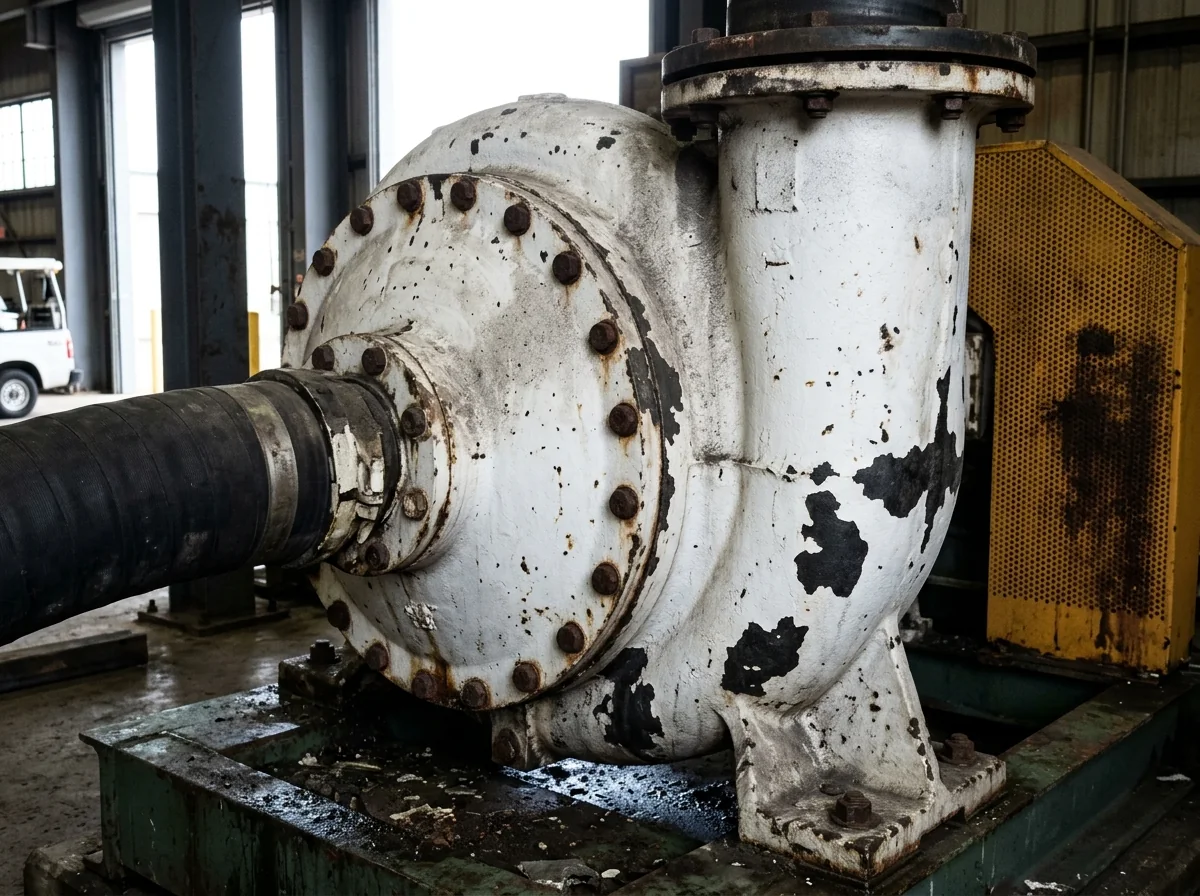
Pumps, Valves & OEM
Pump casings and valve bonnets17-4 PH stud bolts & threaded rods clamp pump casings and valve bonnets with nuts on the exposed ends, keeping the stud in place when a cover is removed. Repeated maintenance makes fit, engagement and access part of the component specification.
Same stud. Different material priorities.
17-4 PH material data316L
Molybdenum-bearing stainless performance in wet equipment.
- Connection priority
- Stud tension and clamp-load retention
- Washdown and retained cleaner
- Cleaner concentration, rinse quality and deposits determine the exposure in covered joints. The low-carbon designation does not independently establish a fastener strength class. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
Inconel 625
Solid-solution strength and resistance to aggressive process liquids.
- Connection priority
- Stud tension and clamp-load retention
- Annealed or solution-annealed 625
- The delivery condition affects strength and high-temperature response. Keep the specified condition with the component’s mechanical acceptance; 718-style aging is not the strengthening route for 625. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
Duplex 2205
Duplex strength and chloride-corrosion resistance.
- Connection priority
- Stud tension and clamp-load retention
- S31803 or S32205
- The specified UNS fixes the chemistry. Solution treatment, section size and the ordered mechanical or corrosion tests establish the final duplex condition. Include liquid retained at the exposed thread roots and nut-bearing faces in the exposure description.
From drawing to documented delivery
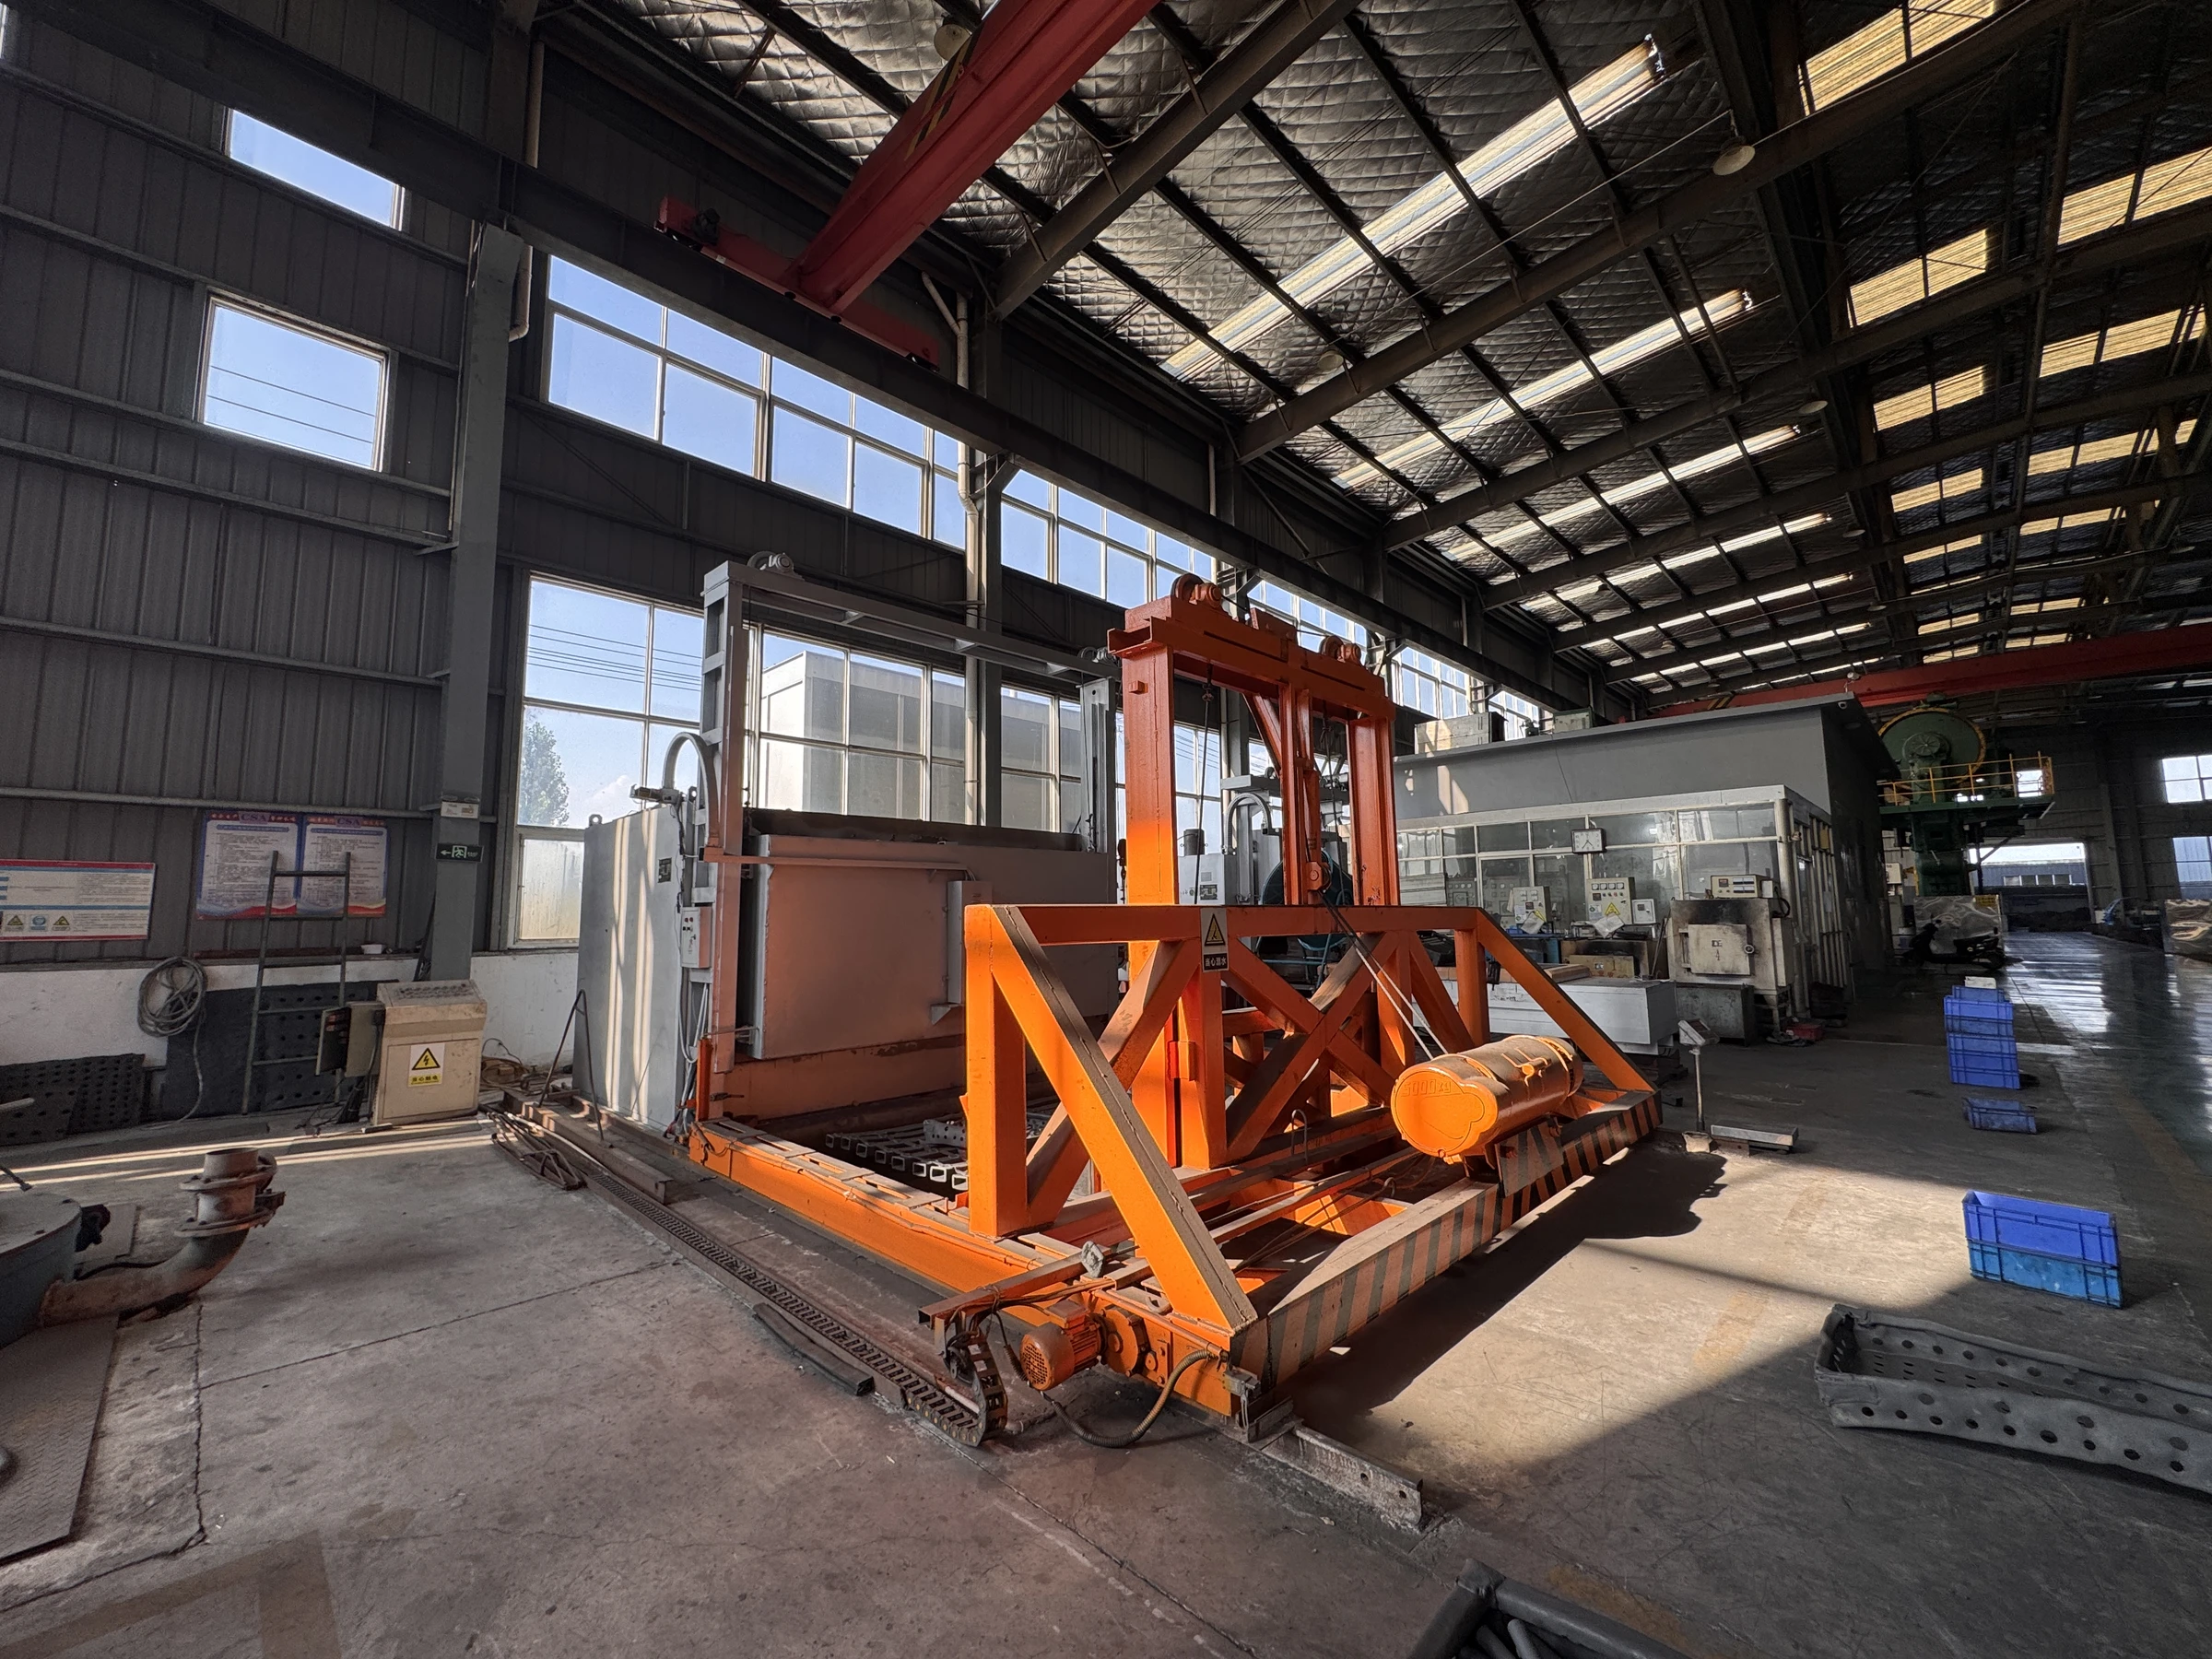
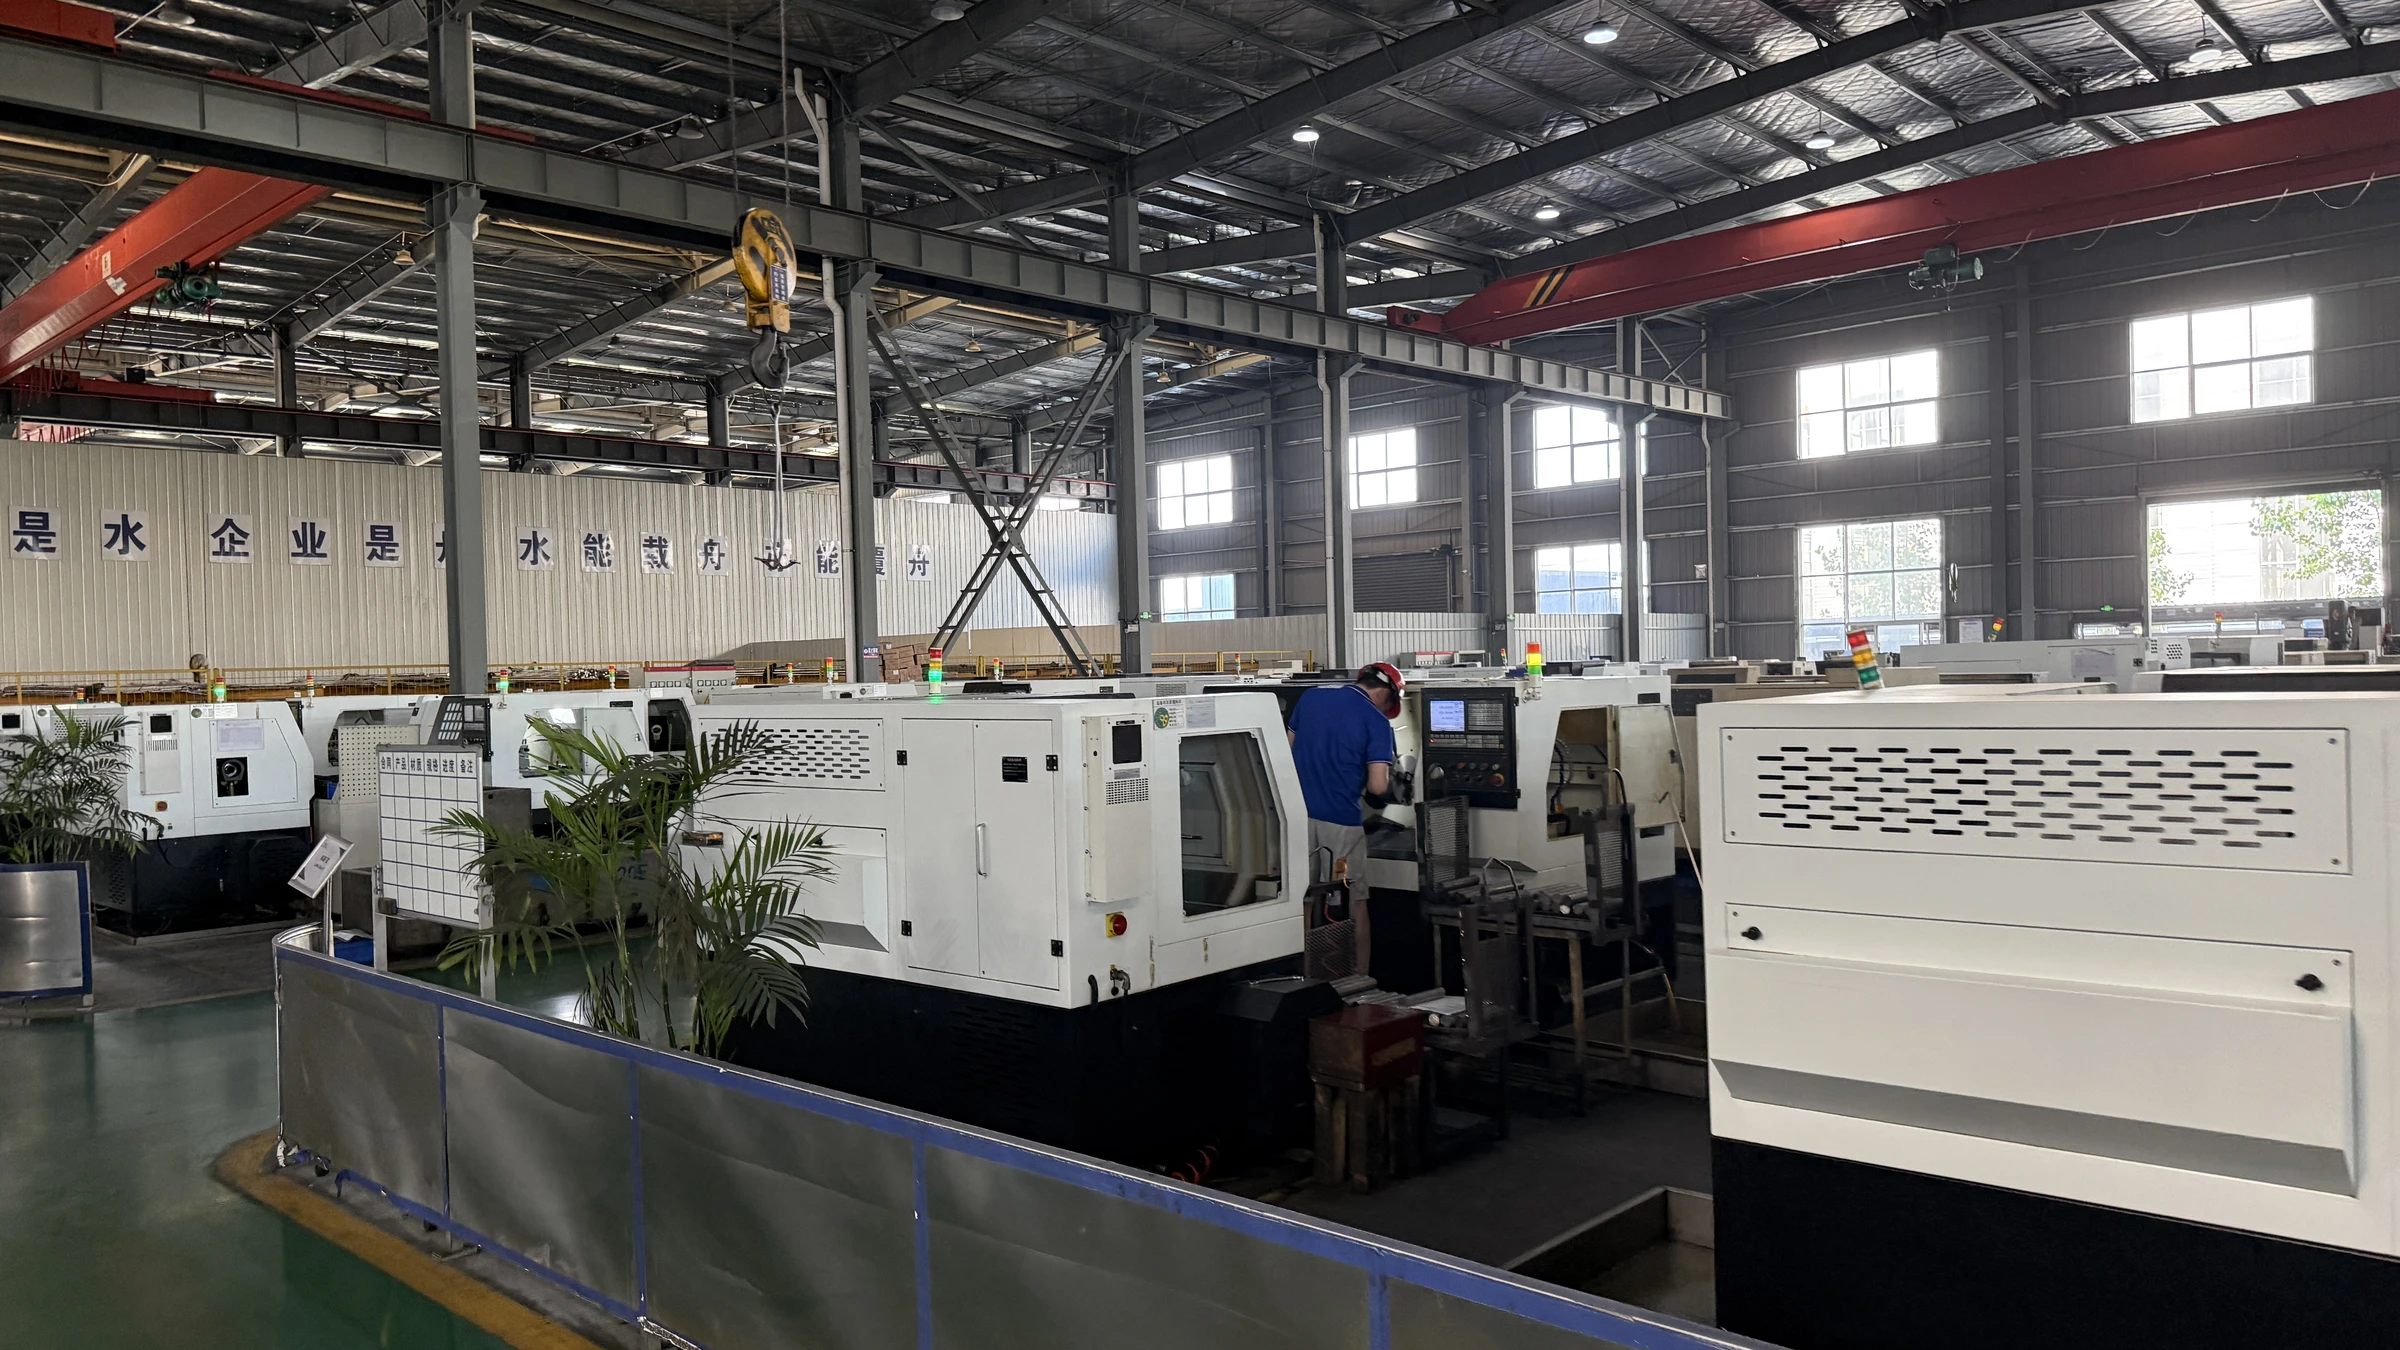
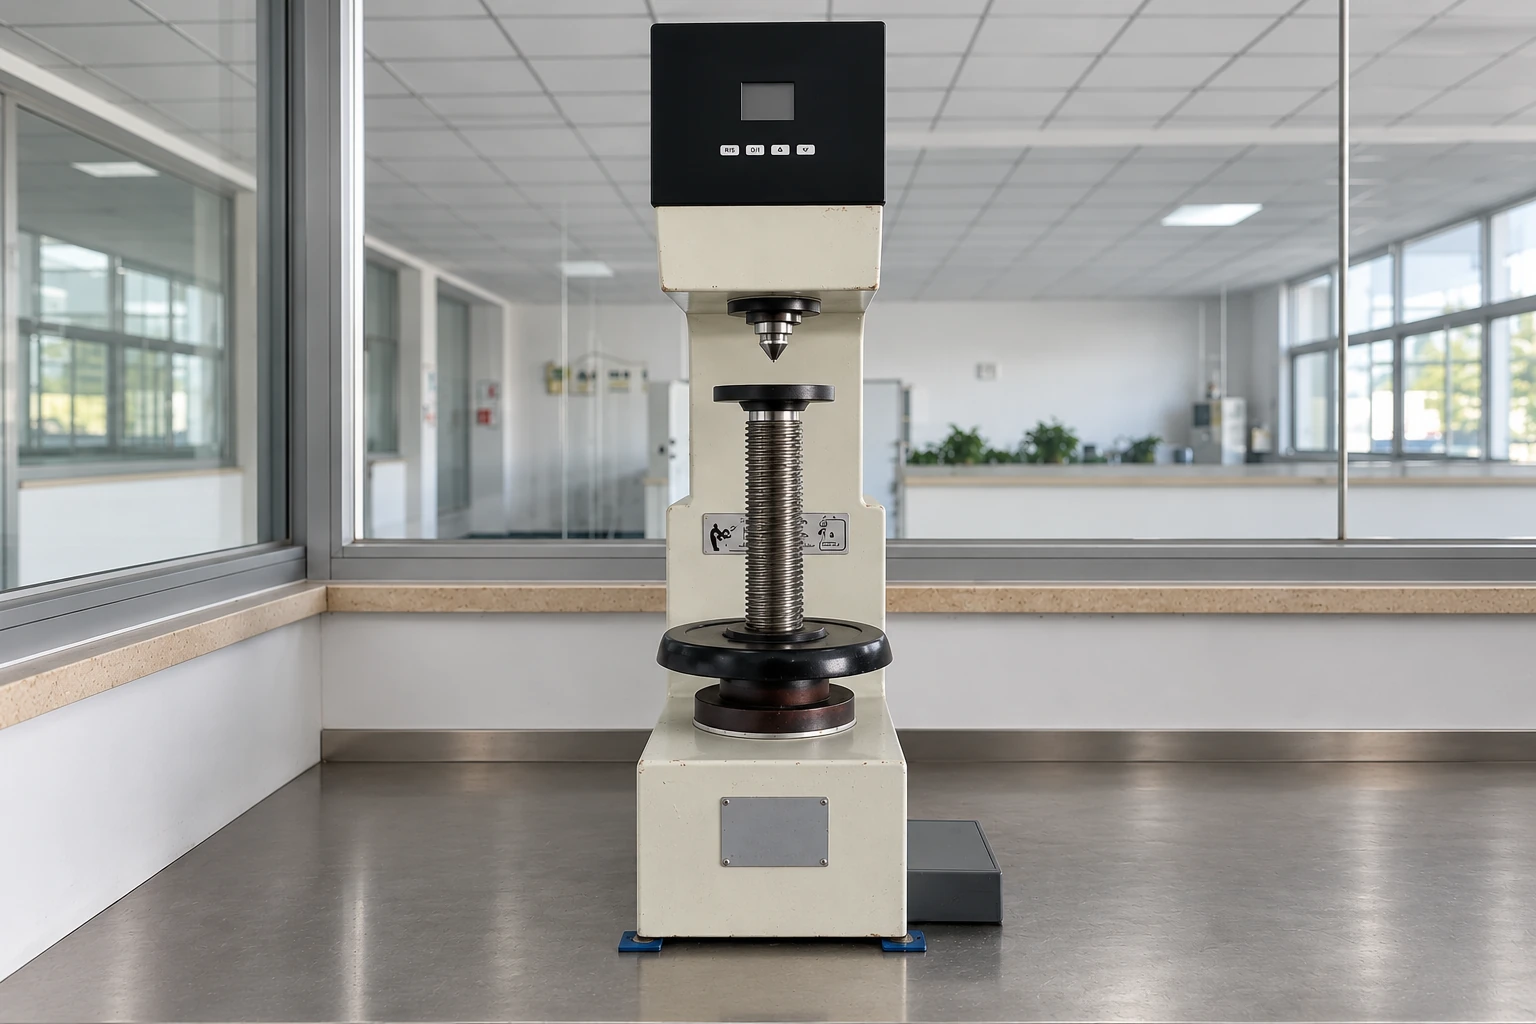
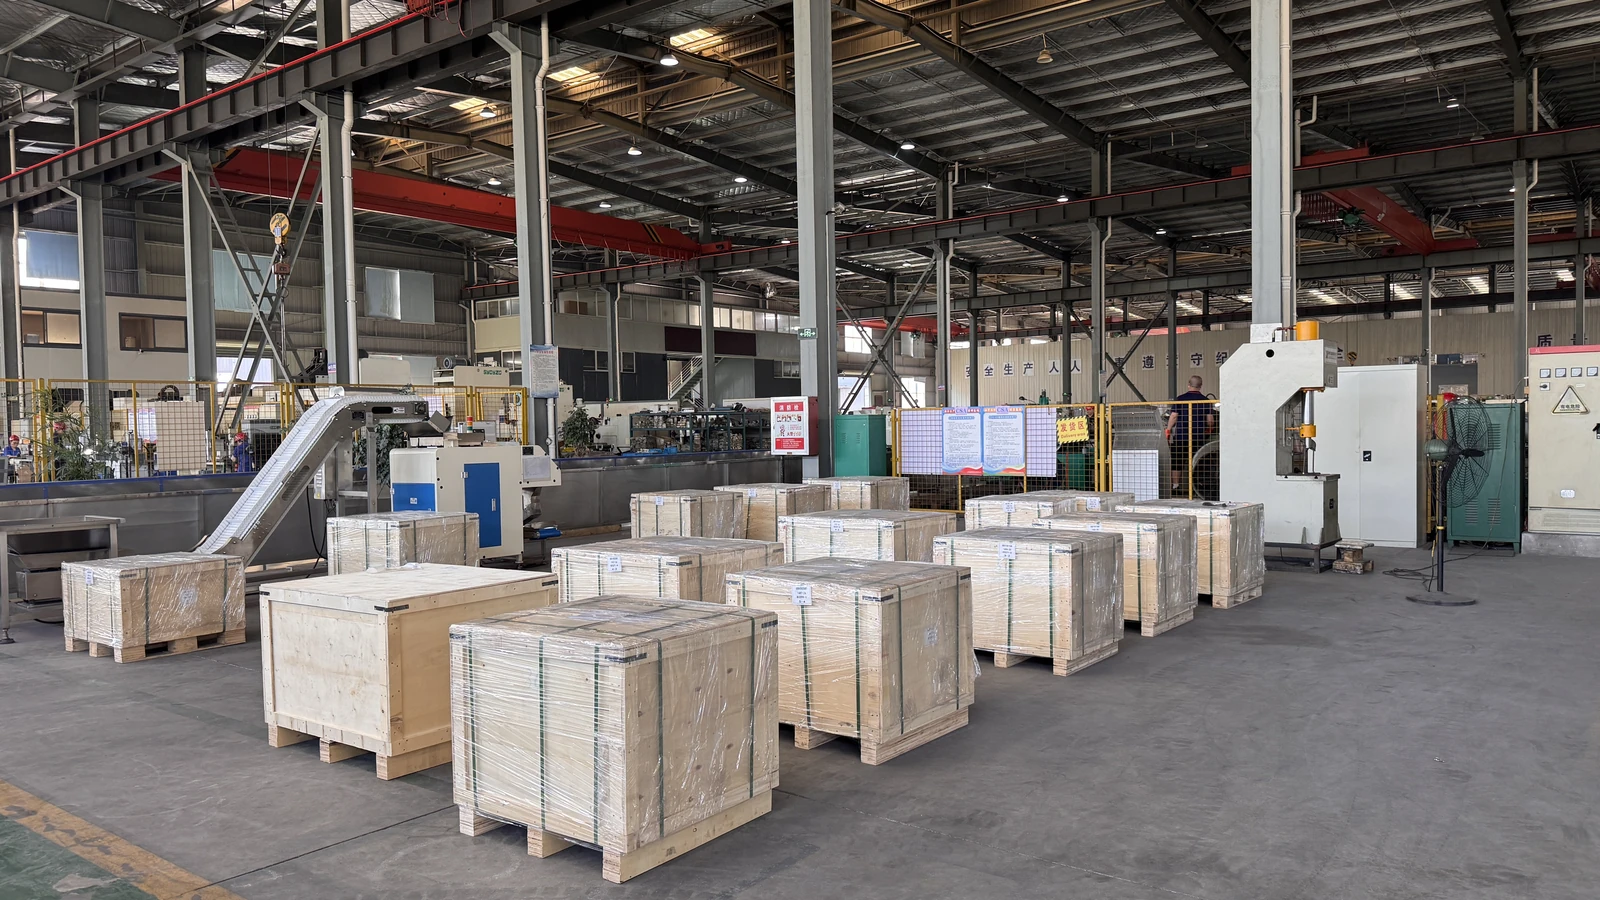
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S17400 · heat number · ordered condition
- Final-part acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Thread size and fit; overall and effective thread length; end geometry; lot identification.
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Matching Kit
Flange Stud Bolt Kits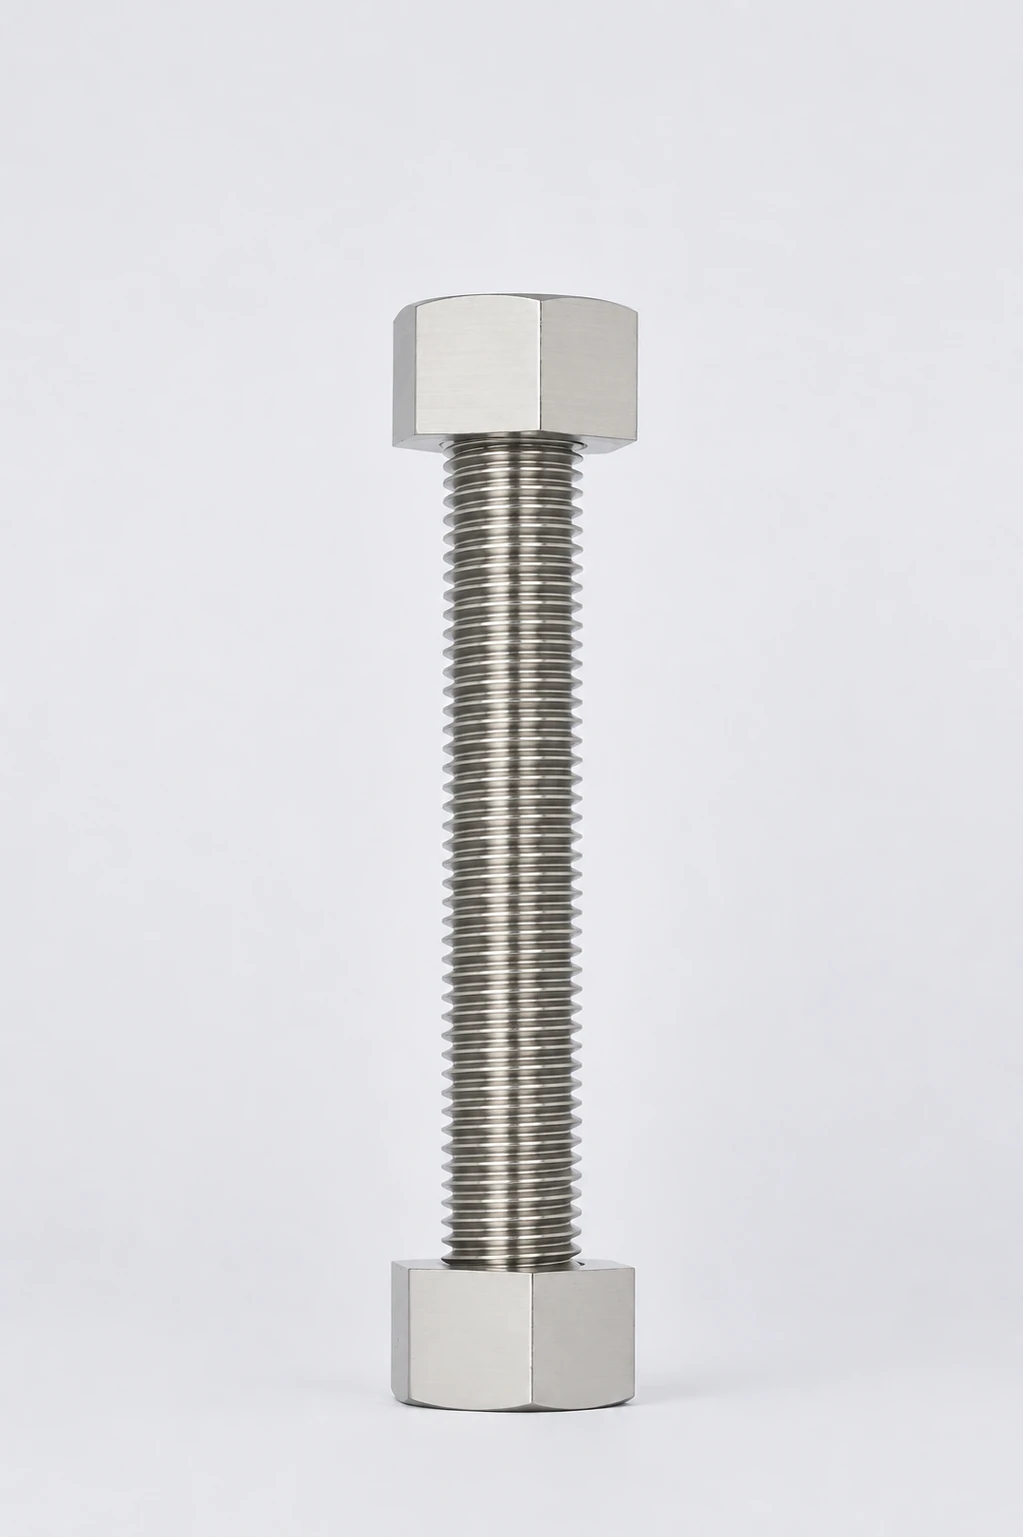
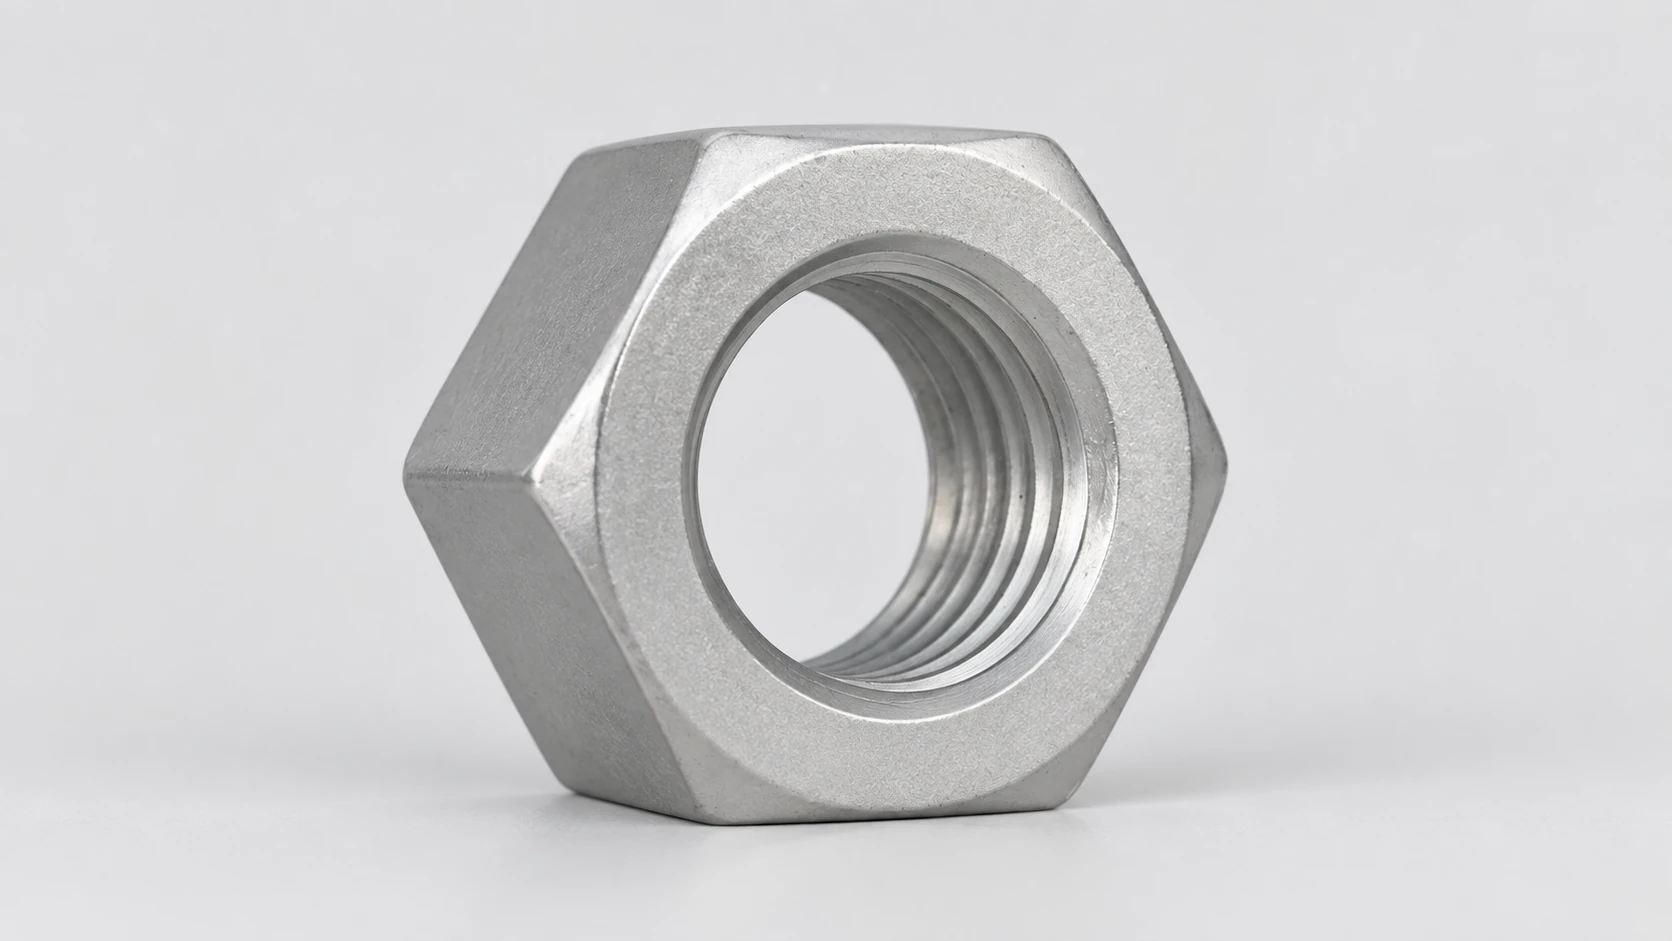
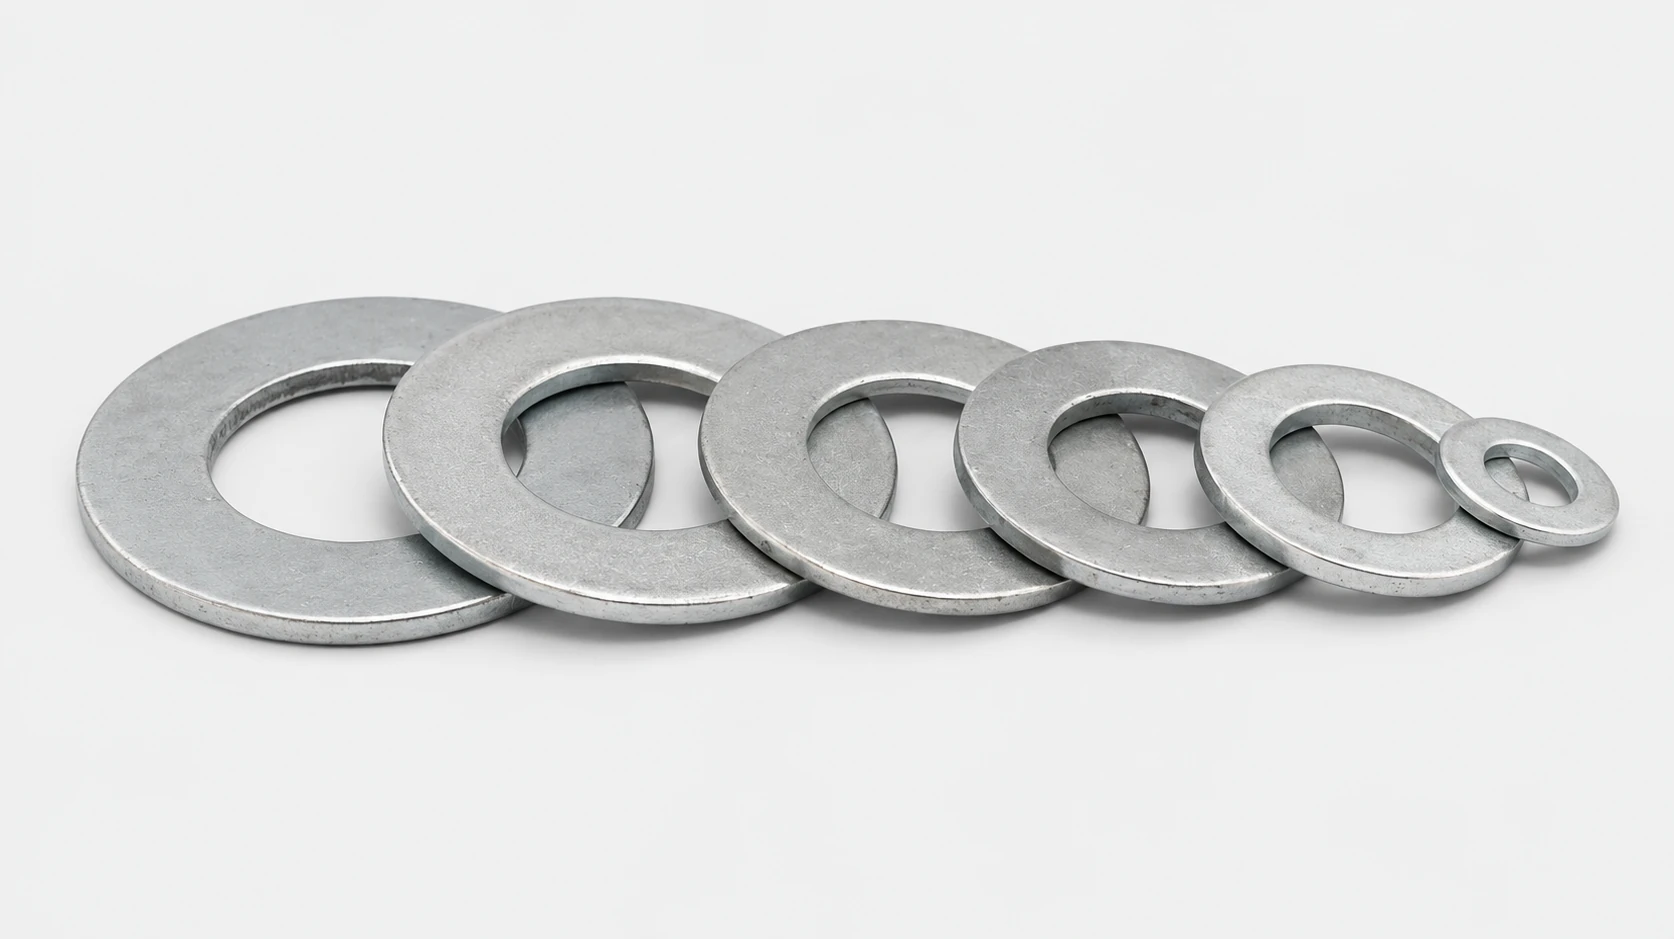
Build your 17-4 PH stud enquiry
Questions about 17-4 PH stud bolts & threaded rods
Does changing the stud alloy also change the nut selection?
The nut needs compatible internal threads, sufficient engaged height and a specified material condition. Select lubricant or surface treatment with the stud–nut pair, because assembly friction affects the preload obtained from tightening.