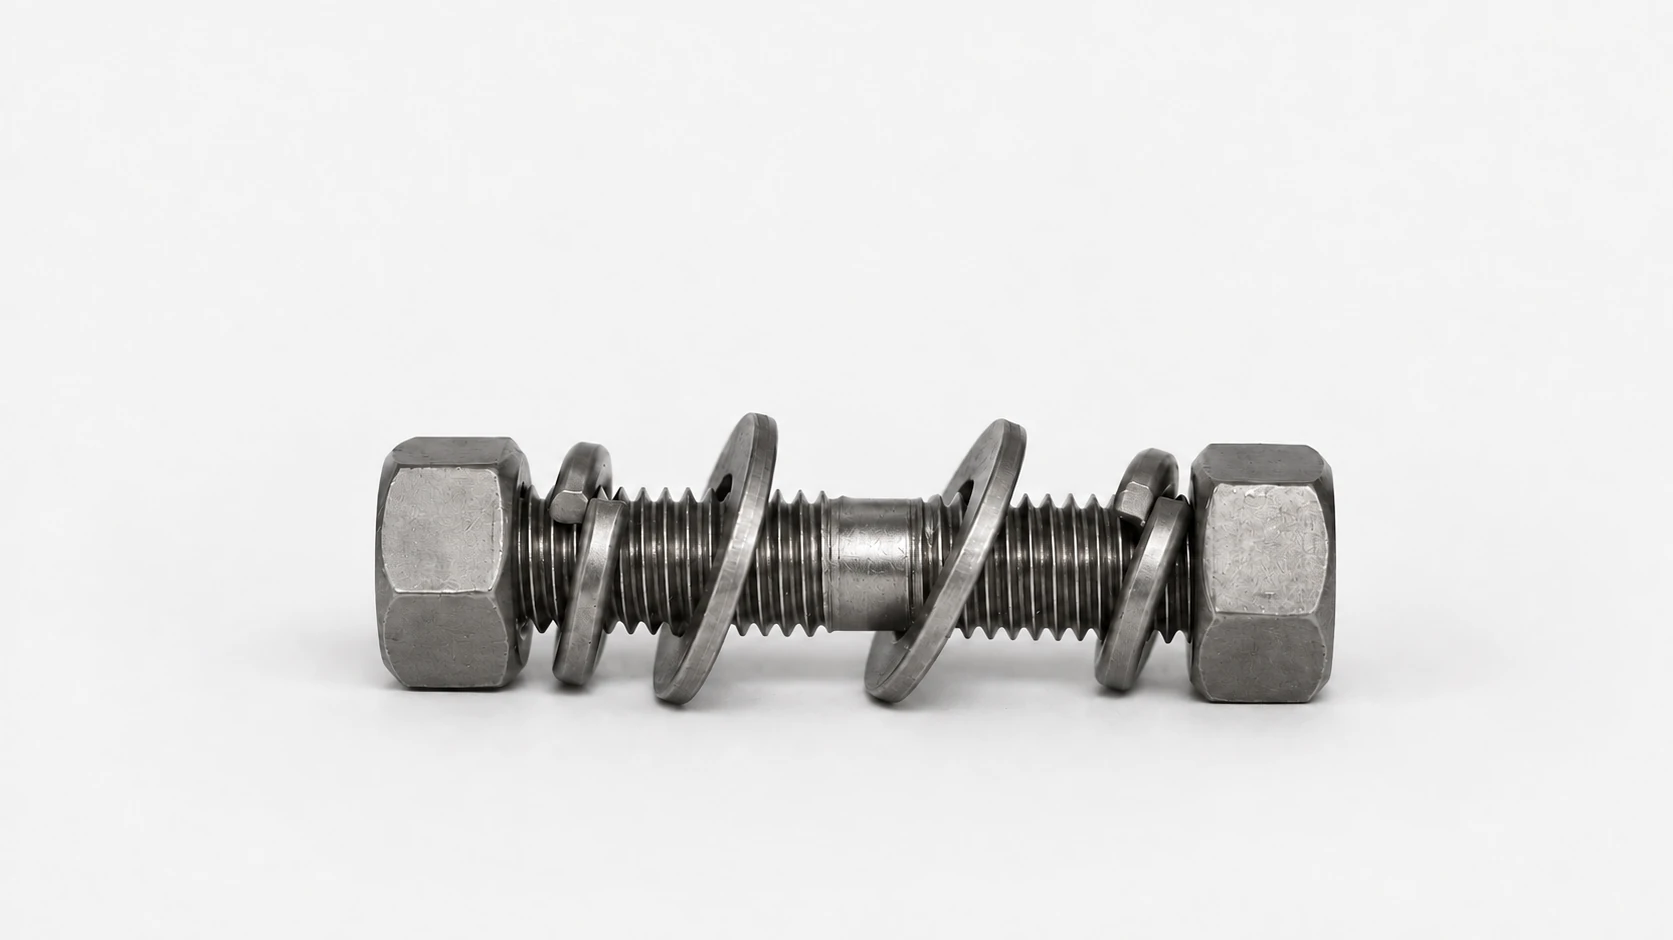
A-286 Stud, nut & washer sets
ASME B18.31.2
A-286 stud, nut and washer sets carry the connection from tensile member to bearing surface. Aged iron–nickel alloy strength for hot bolting must be matched by suitable nut engagement and washer bearing strength.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Finished-Component Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated and agedSolution treatment is followed by precipitation aging, with the Grade 660 class defining the required heat-treatment route and final properties.
What we can make in A-286
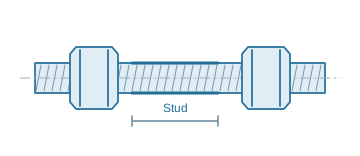
Stud
Include both washers when calculating the clamped stack and usable stud projection. Their thickness can change the stud length needed to engage both nuts.
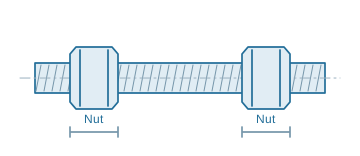
Nuts
Pair the nut grade, proof load and thread fit with the stud for the intended clamp load. Heavy-hex nuts also need enough radial clearance for the installation socket.
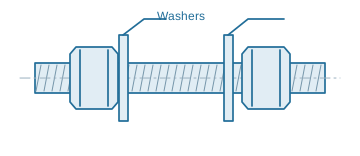
Washers
Use washers to provide the specified bearing footprint or replaceable seating surface. Bore clearance must accommodate the stud, while thickness must support the opening beneath the washer.
- Grade pairing
- Stud + two nuts + washers
- Grade pairing
- Metric · UNC · UNF · 8UN · UNJ
- Grade pairing
- Component-by-component grades
- Grade pairing
- Heat and batch identification
- Final condition
- Solution treated and aged
- Inspection
- Component count · Mating thread fit · Individual dimensions
Manufacturing route
Studs, nuts and washers are manufactured and inspected as separate components before the specified quantities are packed as a set.
Heat treatment & final condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
Thread engagement, nut pattern and component grades are checked together. Each component retains its heat or batch identity in the set documentation.
Where A-286 fits — and what matters
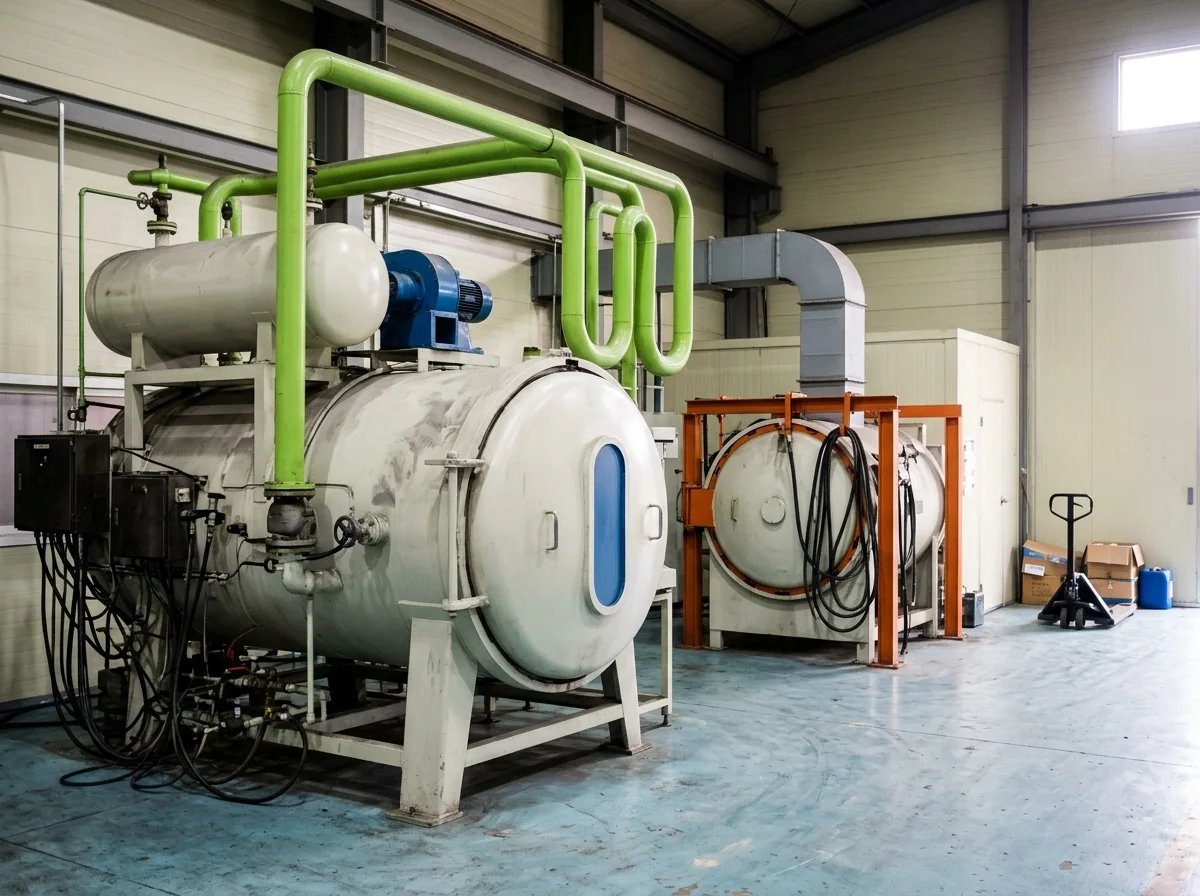
Furnaces & Heat Treatment
Retort and furnace-access coversA-286 stud, nut & washer sets bring the studs, mating nuts and specified bearing washers together for retort and furnace-access covers. The washer stack is included in the required usable stud length. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
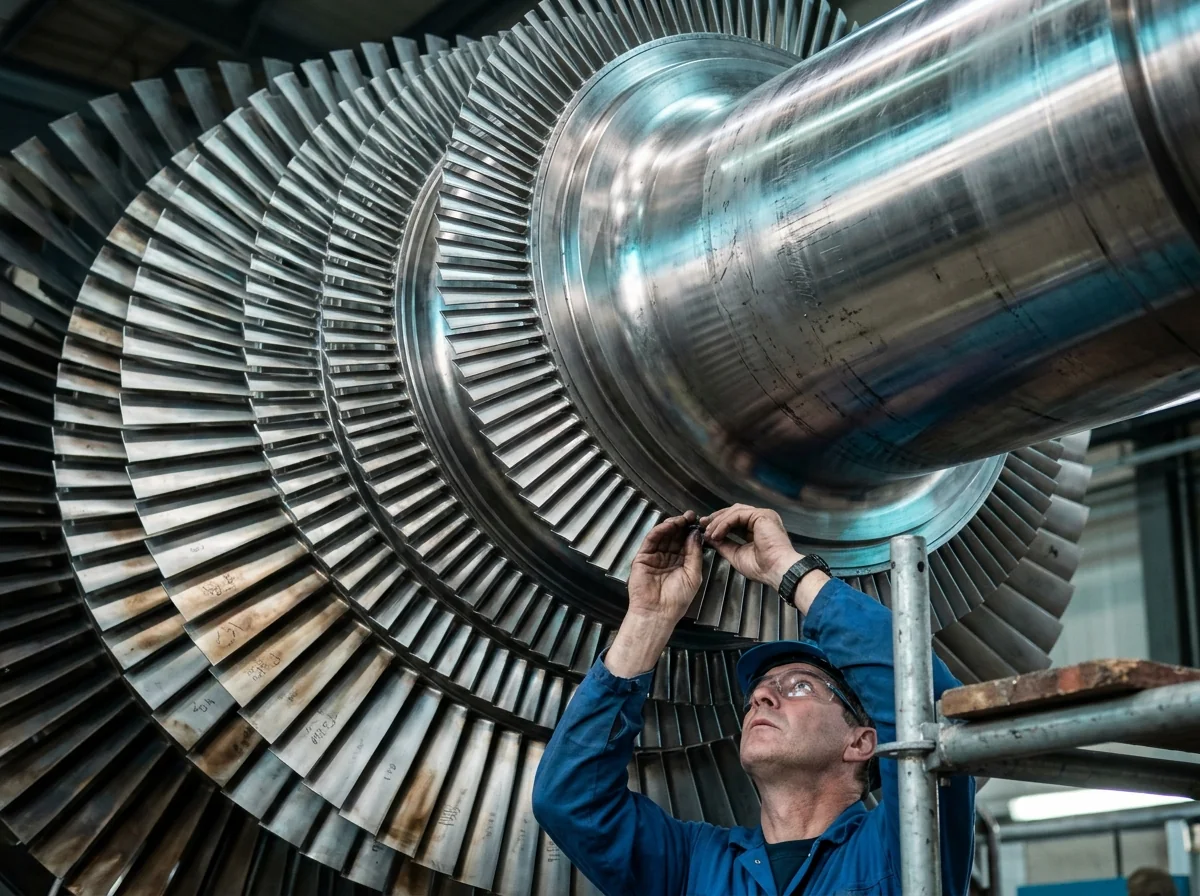
Power & Turbines
Hot-gas access covers and inspection closuresA-286 stud, nut & washer sets bring the studs, mating nuts and specified bearing washers together for hot-gas access covers and inspection closures. The washer stack is included in the required usable stud length. Hot dwell and start-stop expansion act on the supported or moving component.
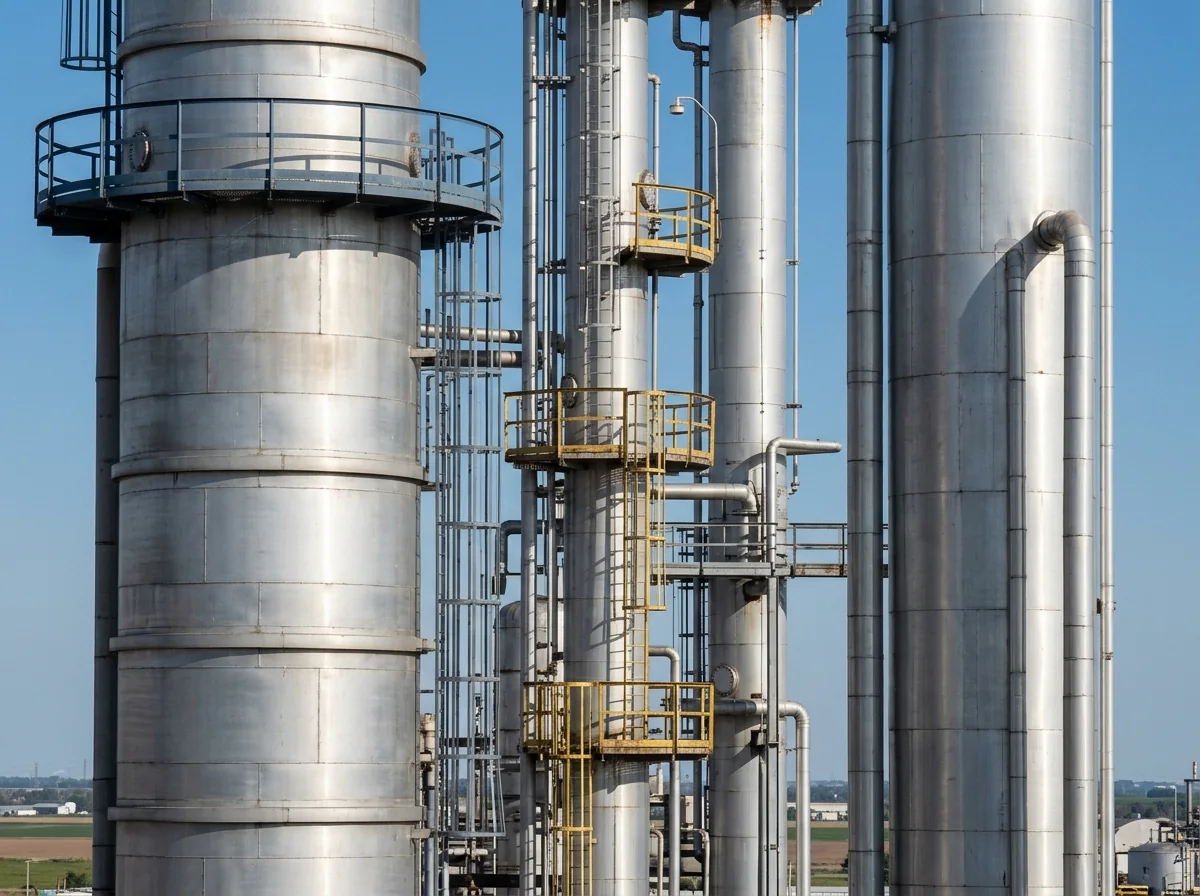
Chemical Processing
Reformer access covers and hot-gas inspection closuresA-286 stud, nut & washer sets bring the studs, mating nuts and specified bearing washers together for reformer access covers and hot-gas inspection closures. The washer stack is included in the required usable stud length. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same stud, nut & washer set. Different material priorities.
A-286 material dataIncoloy 800HT
Tightly controlled carbon and Al + Ti for creep duty.
- Connection priority
- Stud tension, nut engagement and washer bearing
- N08811 material control
- 800HT tightens the 800-family chemistry around creep performance. Its solution-treated, coarse-grain condition and N08811 identity should remain linked through forming and final acceptance. At the stud–nut threads and both washer-bearing interfaces, the relevant metal temperature can differ from the process or furnace set point.
Inconel 718
Precipitation-hardened strength for compact, highly loaded connections.
- Connection priority
- Stud tension, nut engagement and washer bearing
- Strength after aging
- Machine-stock properties and final aged properties describe different states. The final heat-treatment lot and mechanical results establish the strength available in the installed part. At the stud–nut threads and both washer-bearing interfaces, the relevant metal temperature can differ from the process or furnace set point.
310S
Low-carbon heat resistance in oxidation-exposed equipment.
- Connection priority
- Stud tension, nut engagement and washer bearing
- 310S is not 310H
- S31008 is the low-carbon grade. For a component under sustained hot load, distinguish that specification from the controlled-carbon creep purpose of S31009. At the stud–nut threads and both washer-bearing interfaces, the relevant metal temperature can differ from the process or furnace set point.
From drawing to documented delivery
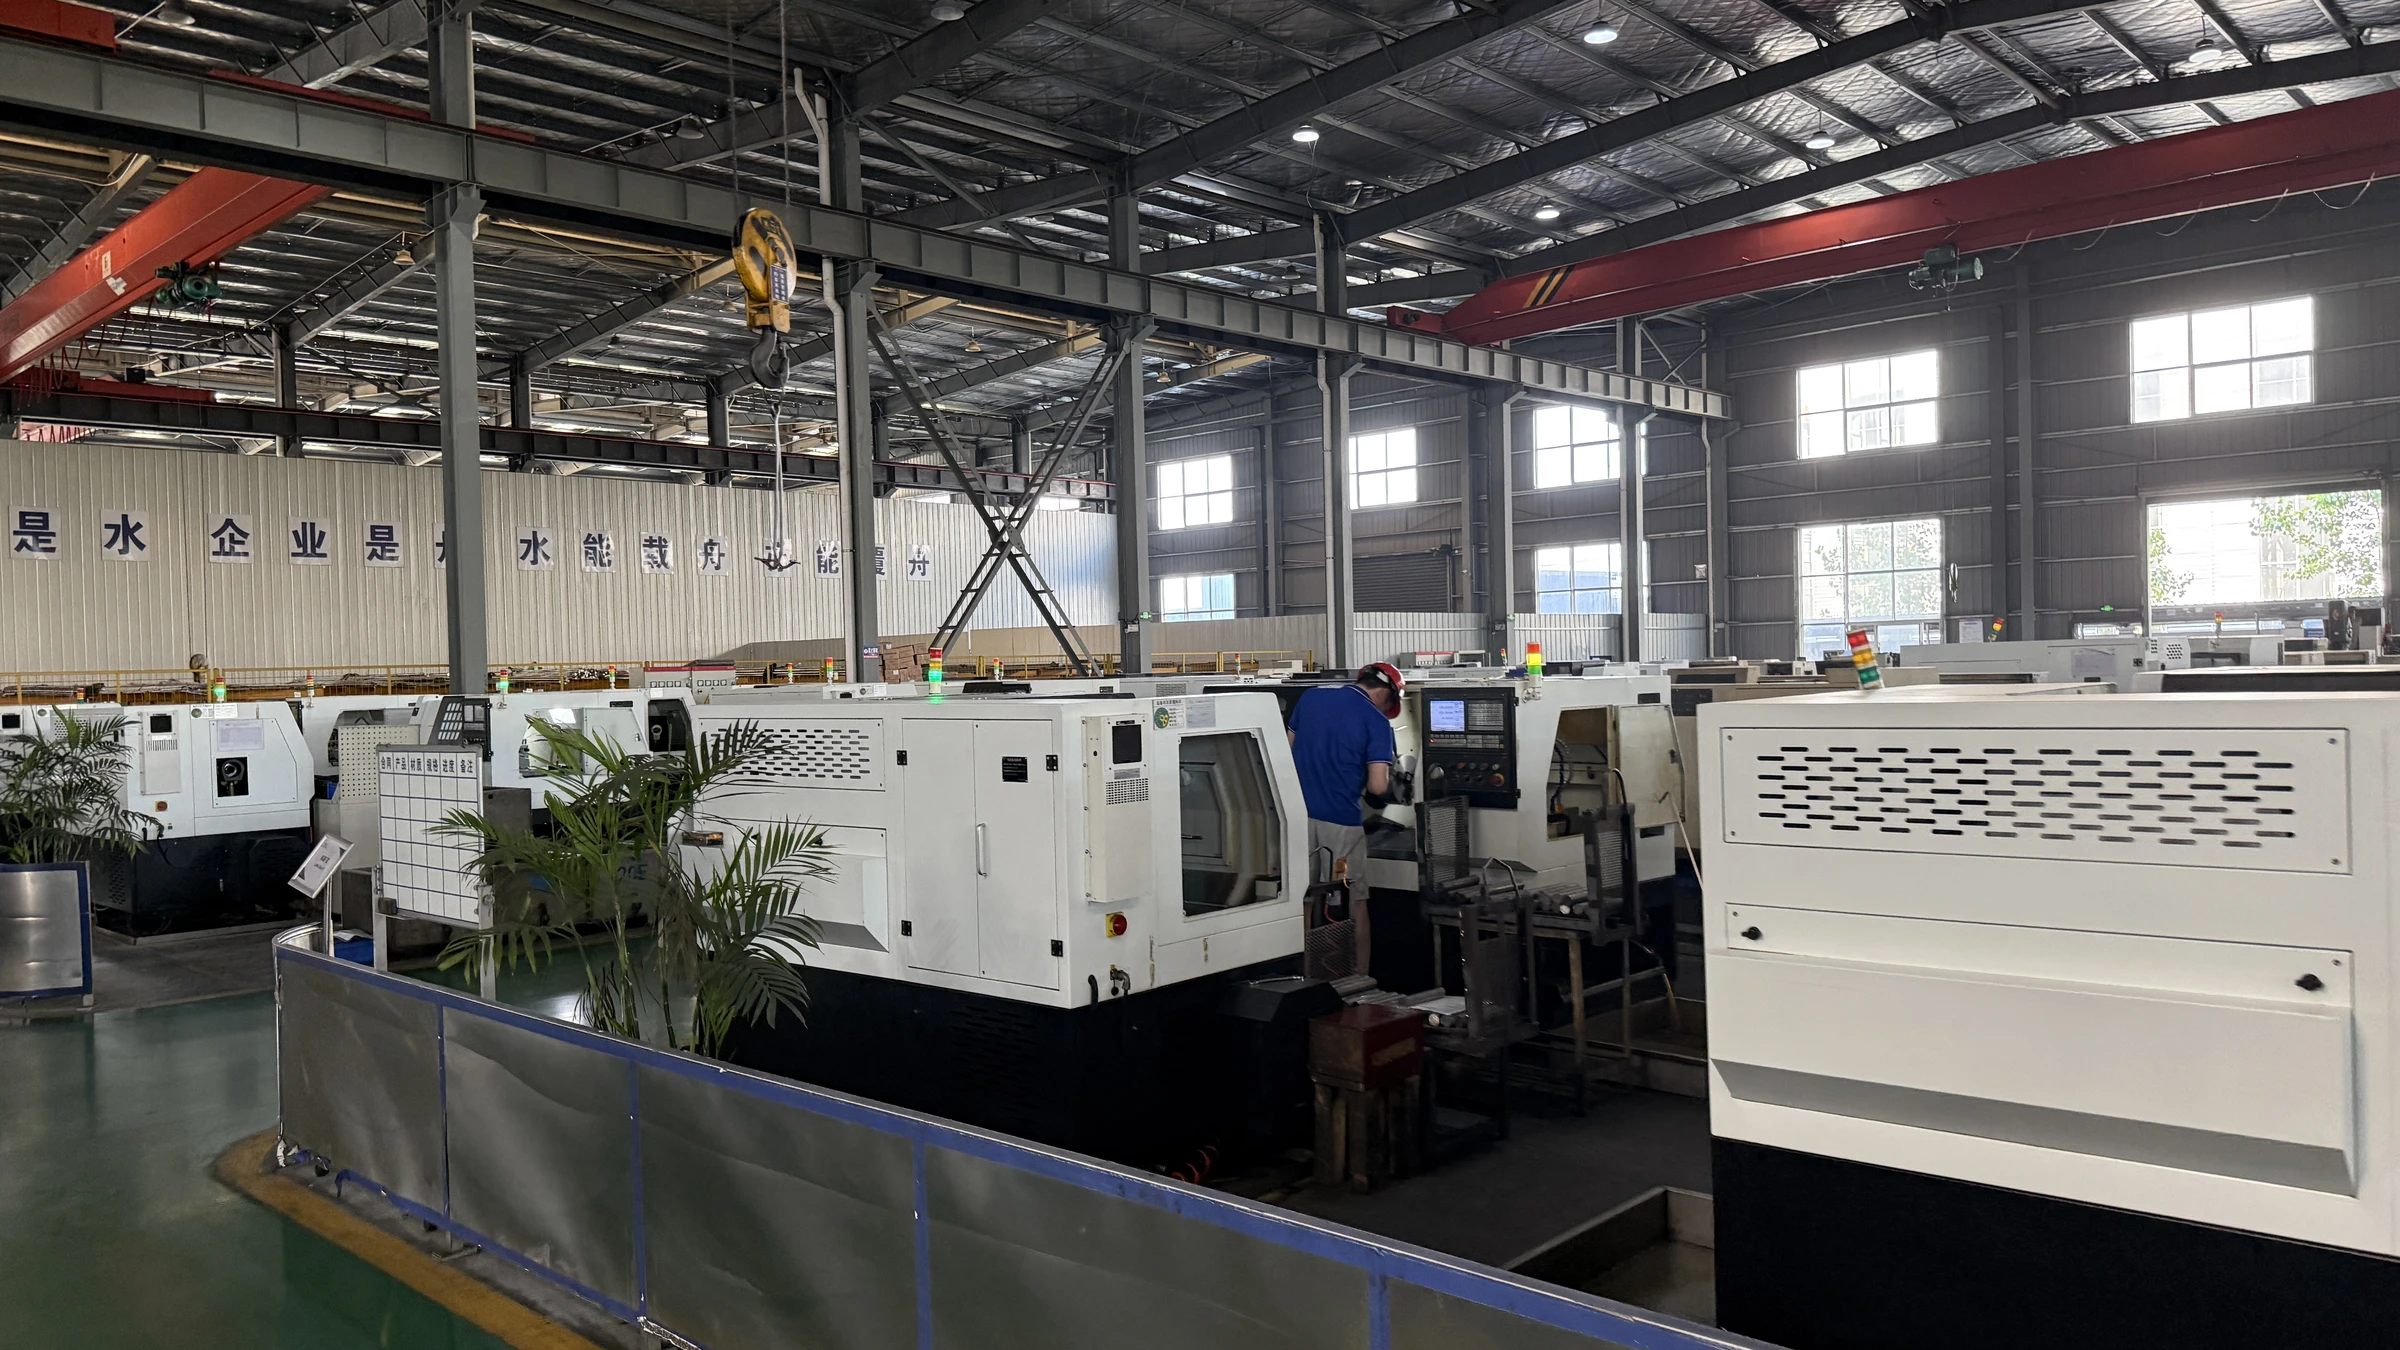
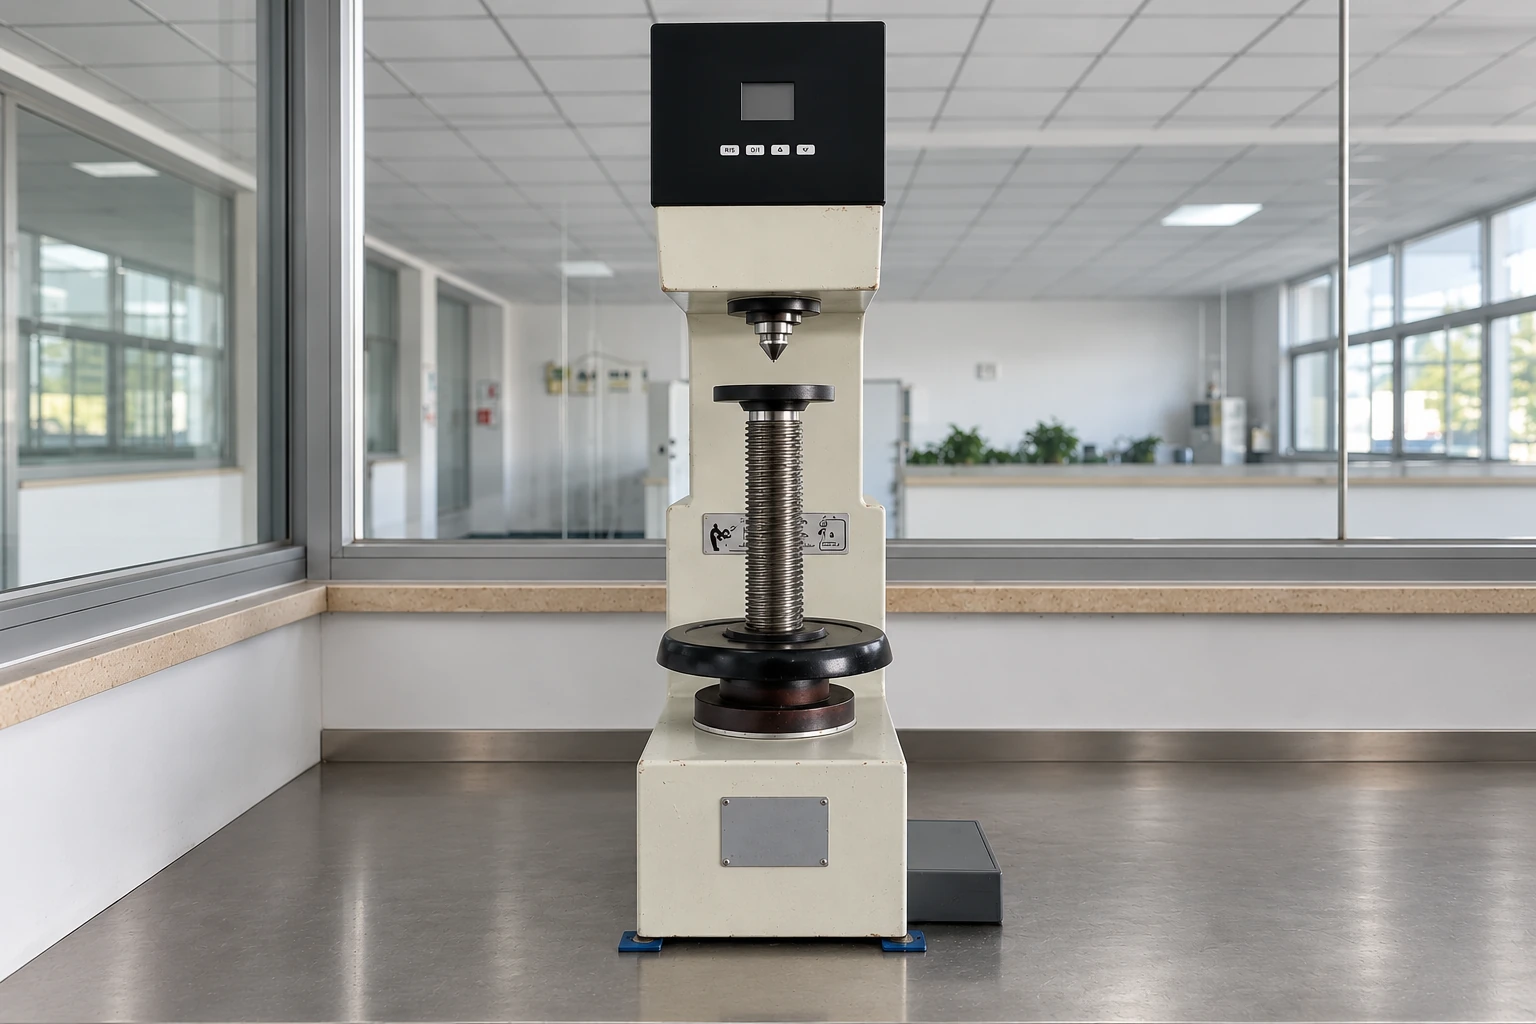
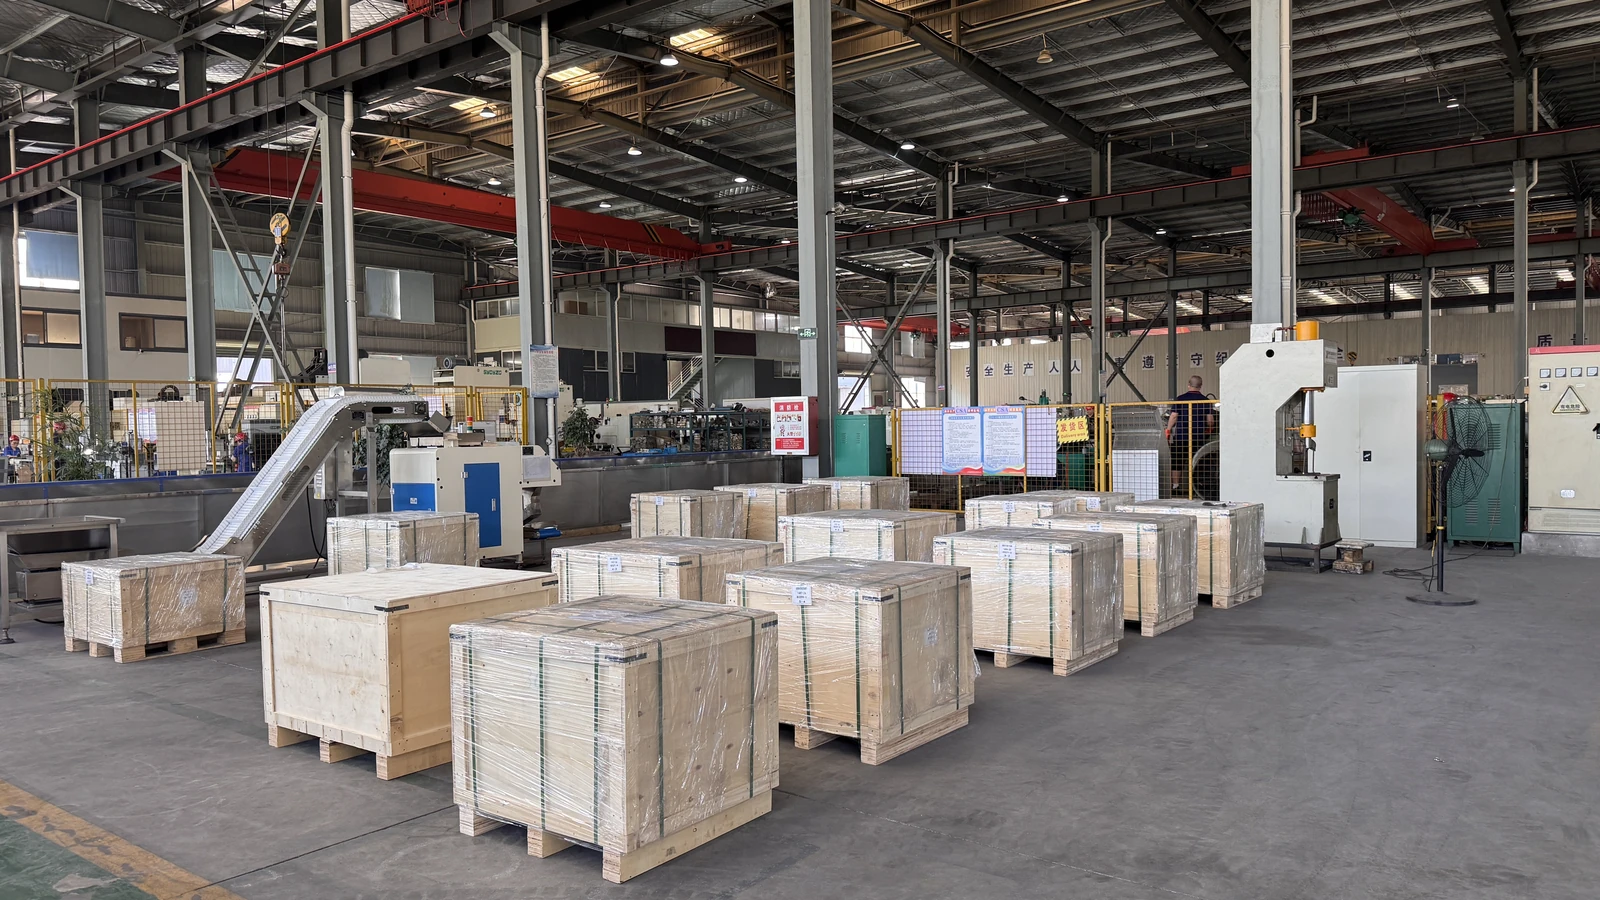
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S66286 · heat number · ordered condition
- Final-part acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Component count · Mating thread fit · Individual dimensions
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your A-286 stud, nut & washer set enquiry
Questions about A-286 stud, nut & washer sets
Can all components be accepted from the stud certificate?
Each component has its own job and material lot. The nut needs thread and strength acceptance, and the washer needs bearing geometry and the ordered condition; retain those records with the stud’s documentation.