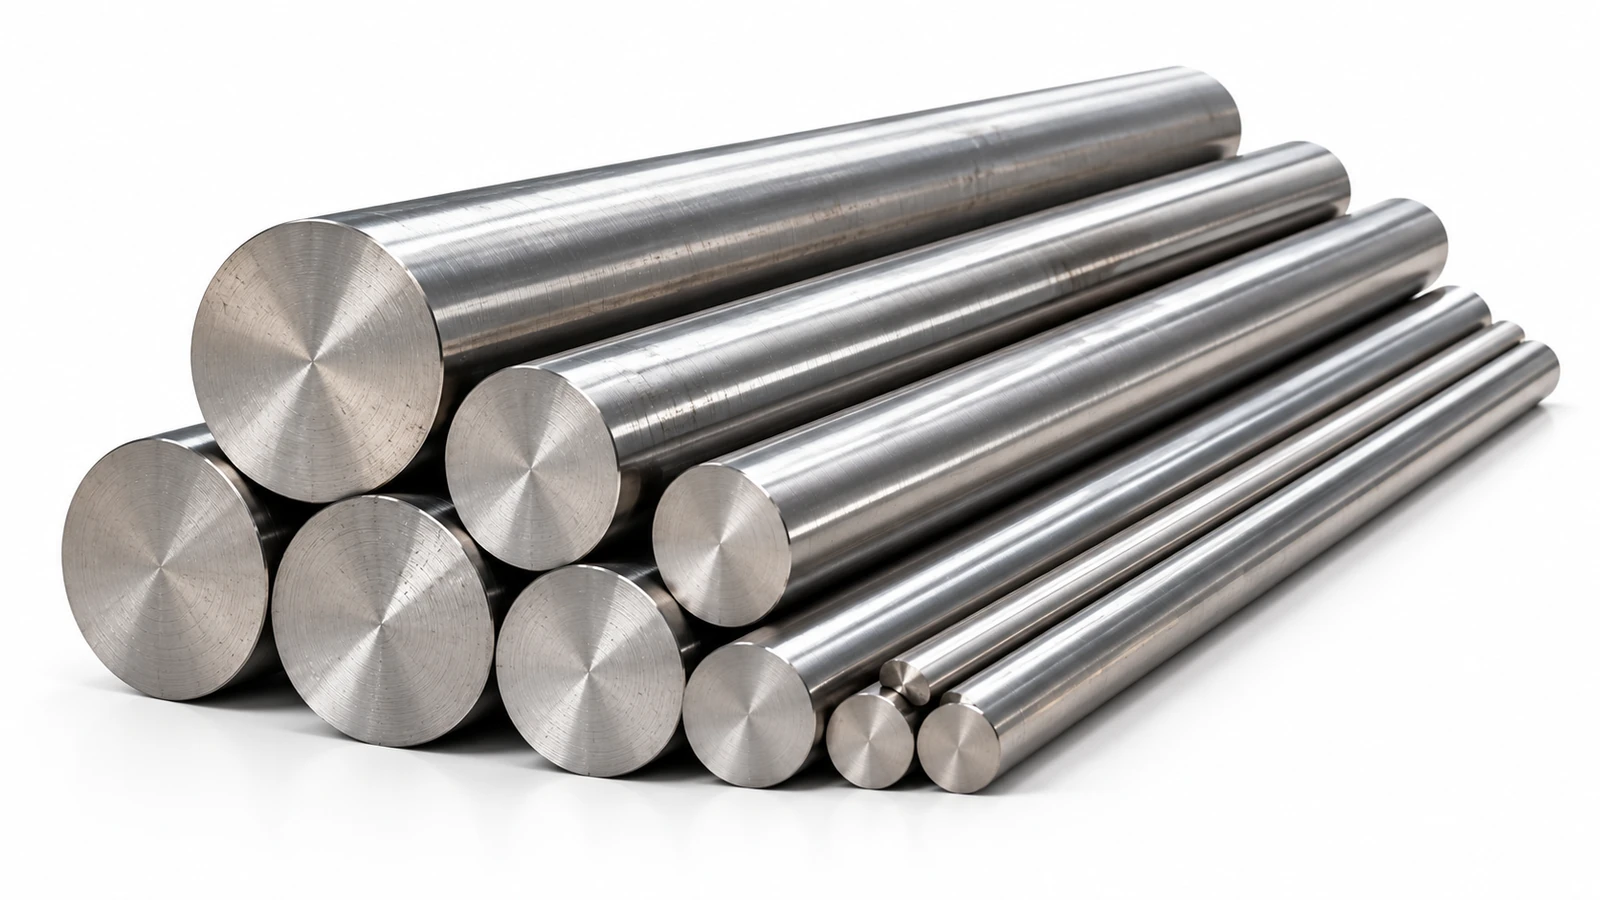
A-286 round bar
EN 10204 3.1
A-286 round bar supplies aged iron–nickel alloy strength for hot bolting to machined shafts, retainers and fastening parts. Diameter allowance and delivery condition determine the route from stock to the final loaded section.
- MOQ
- 100 kg
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Heat Treatment
Solution treated and agedSolution treatment is followed by precipitation aging, with the Grade 660 class defining the required heat-treatment route and final properties.
What we can make in A-286
Full-length bar
Use for repeated turning of shafts, studs and valve components from one heat-traceable stock length. Bar diameter must include machining allowance for the finished surface and straightness.
Cut blank
Use saw-cut blanks for short-run machining or forging starts. Cutting allowance and end squareness affect how much usable length remains after facing.
- Section
- Solid round
- Size
- Diameter × length
- Surface
- Turned · Ground · Drawn
- Supply form
- Bars · Cut pieces
- Final condition
- Solution treated and aged
- Inspection
- Cross-section · Surface · Delivery condition · Heat identity
Supply & preparation
Cut lengths preserve the heat identity of the original bar. Turning or grinding allowance follows the required finished diameter.
Material condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
Diameter, straightness, surface condition and cut length are checked against the stock order.
Where A-286 fits — and what matters
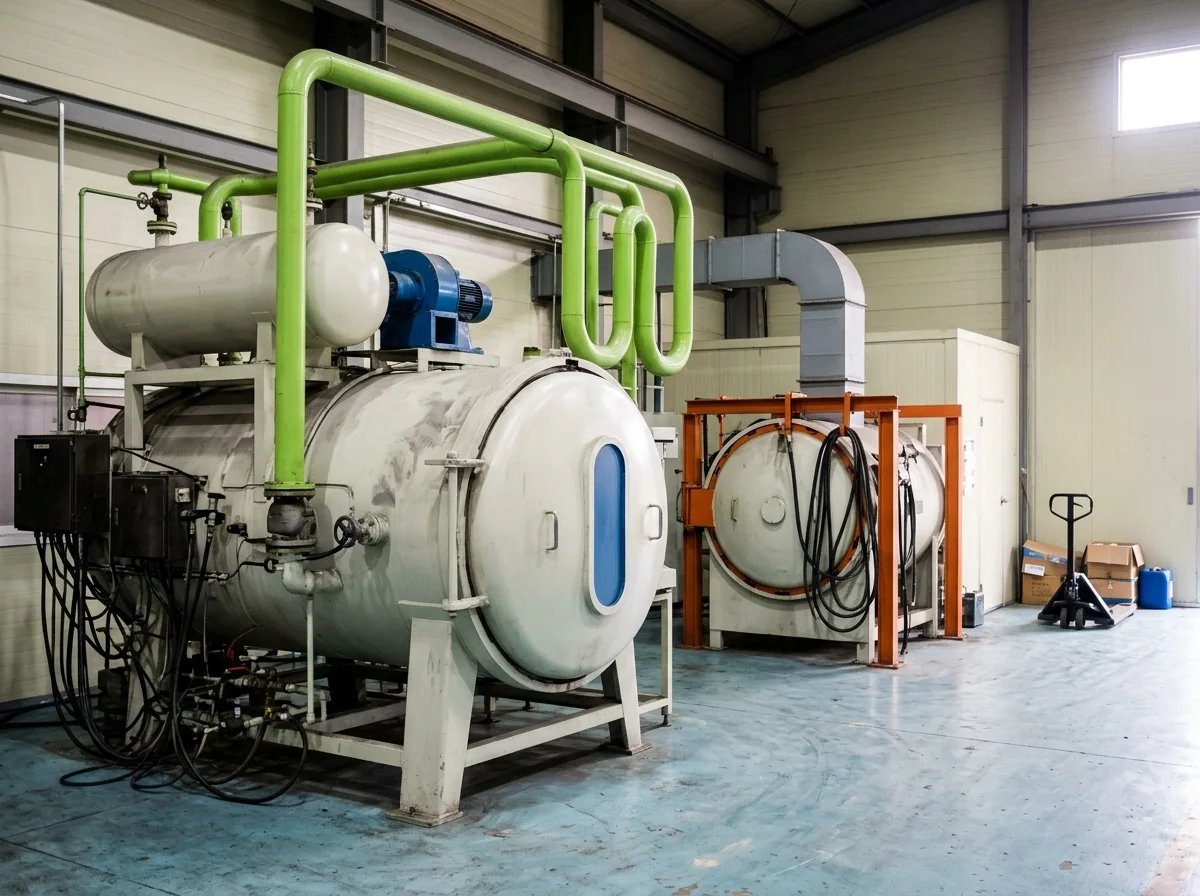
Furnaces & Heat Treatment
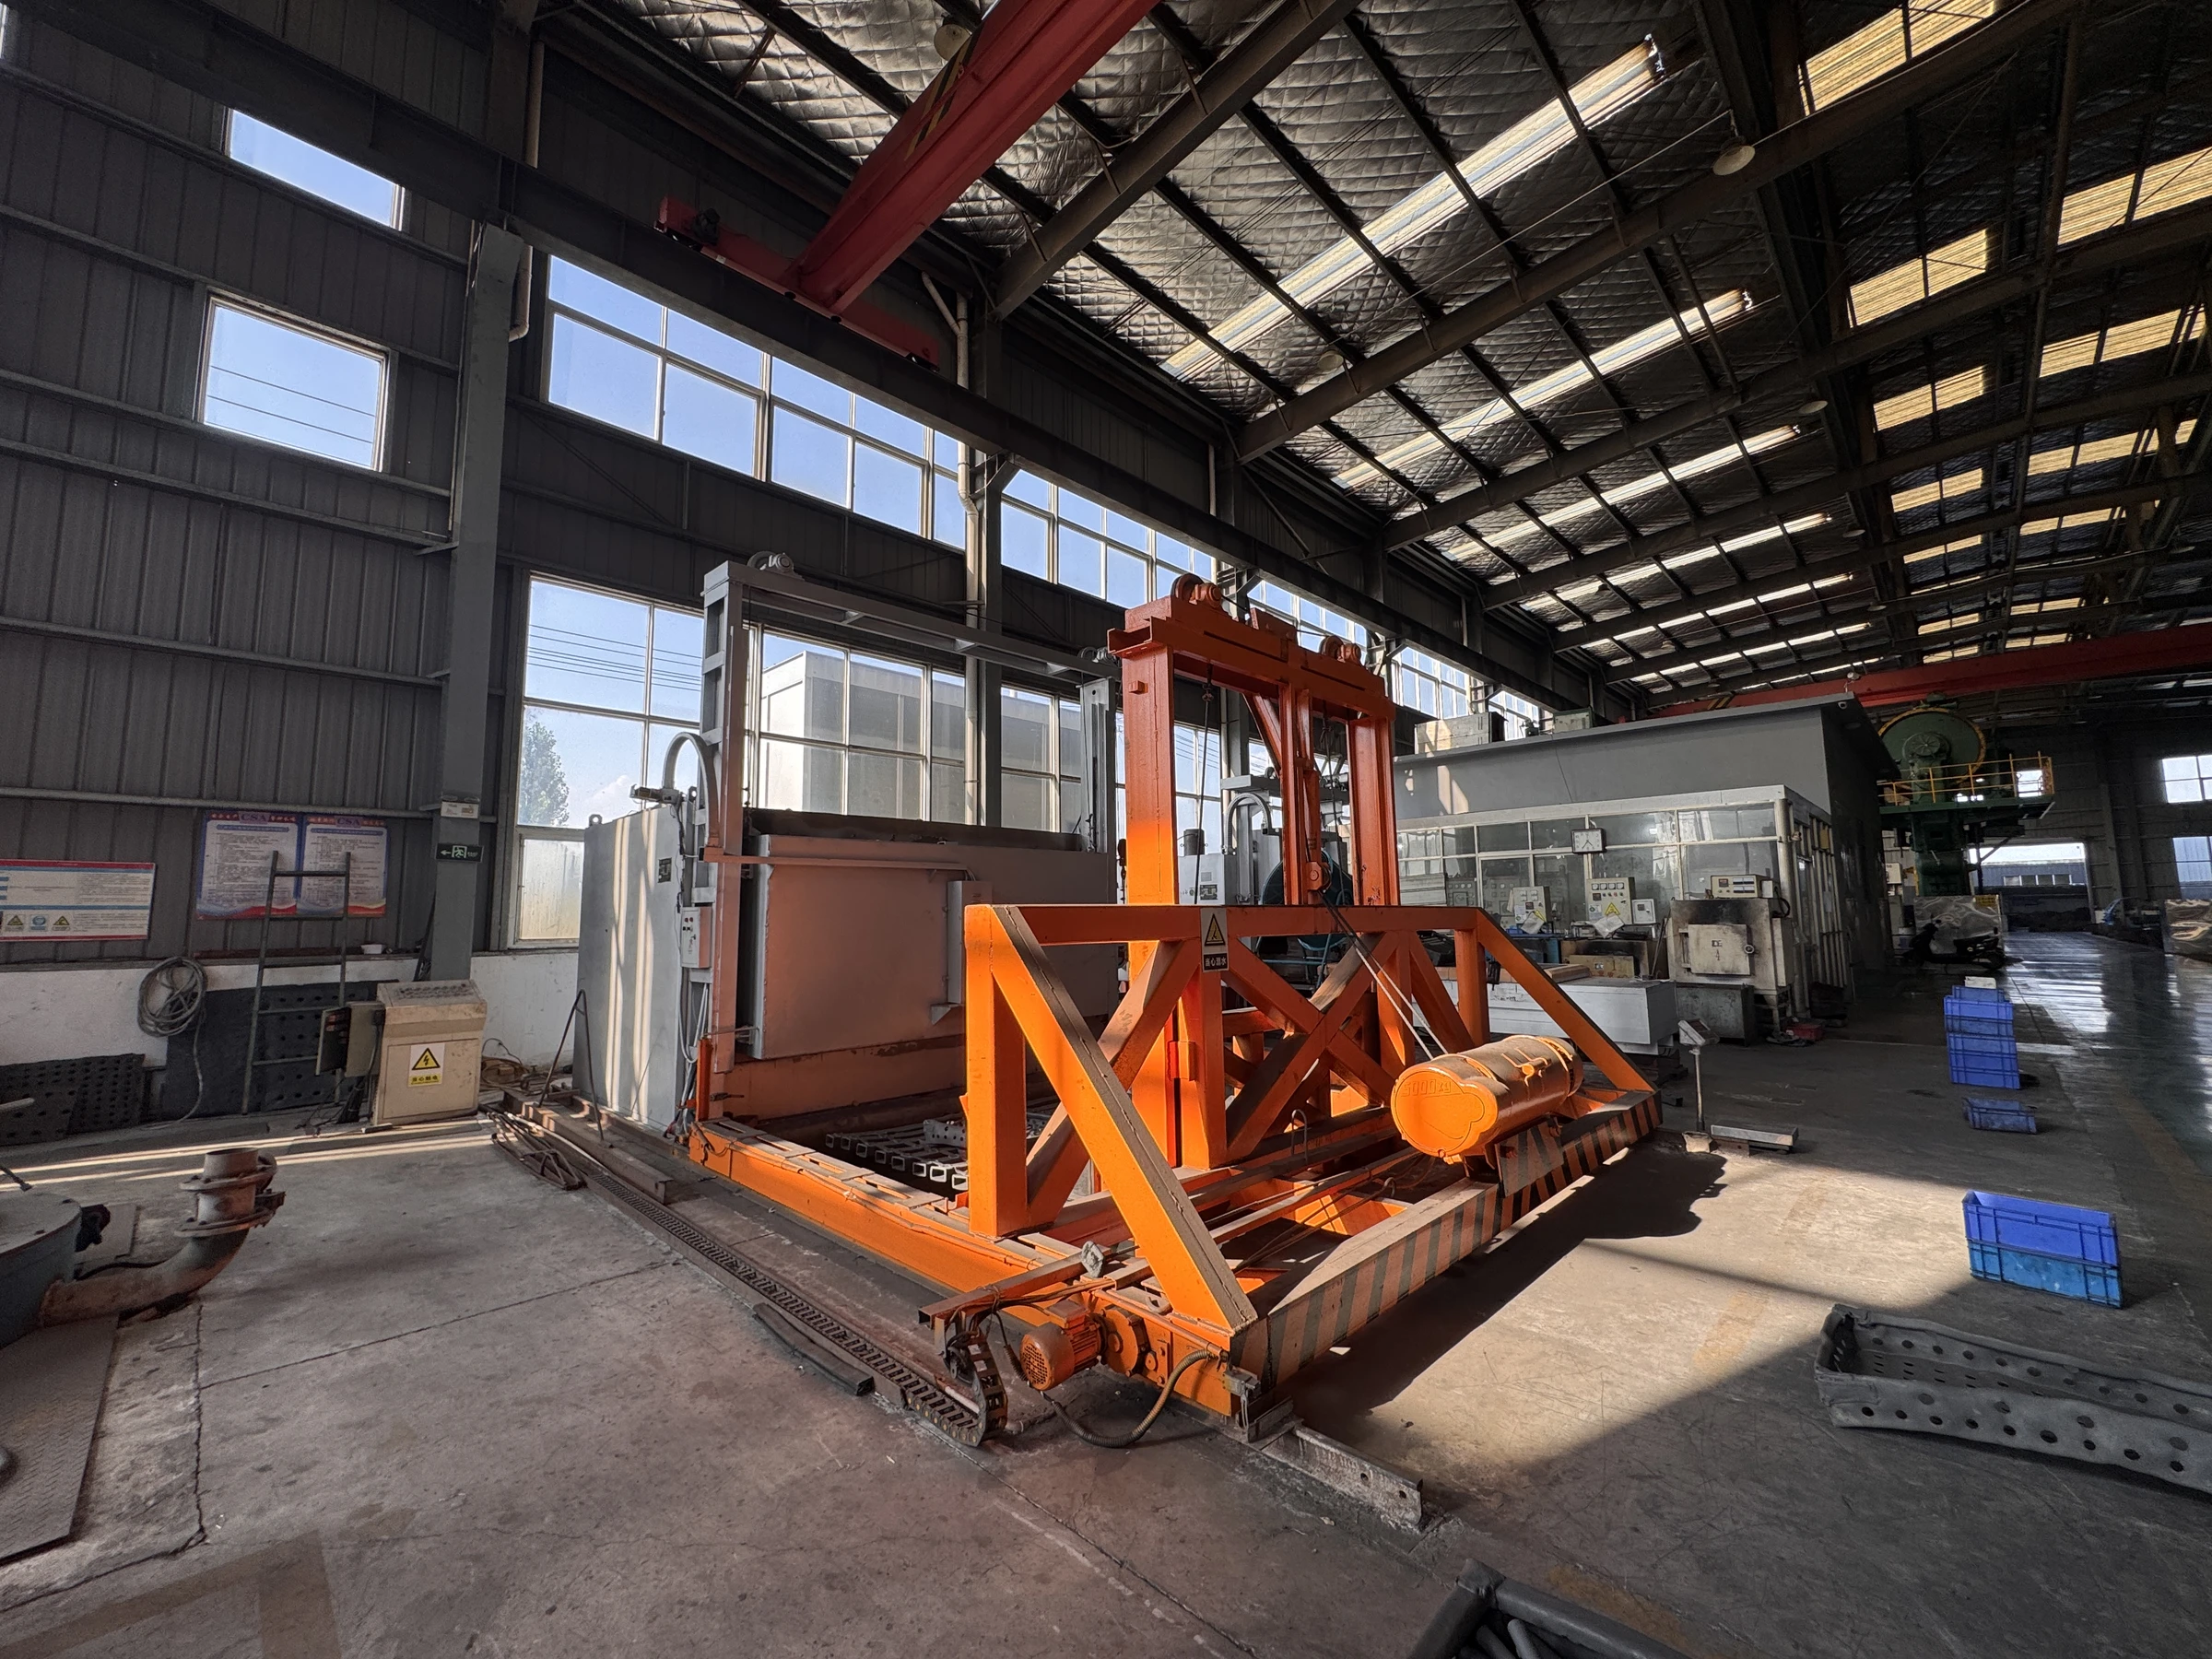
Fixture pivots and conveyor shaftsA-286 round bar provides machining stock for fixture pivots and conveyor shafts, including turned shoulders, bearing seats and threaded ends. Bar diameter includes the allowance for finishing the final part. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
Power & Turbines
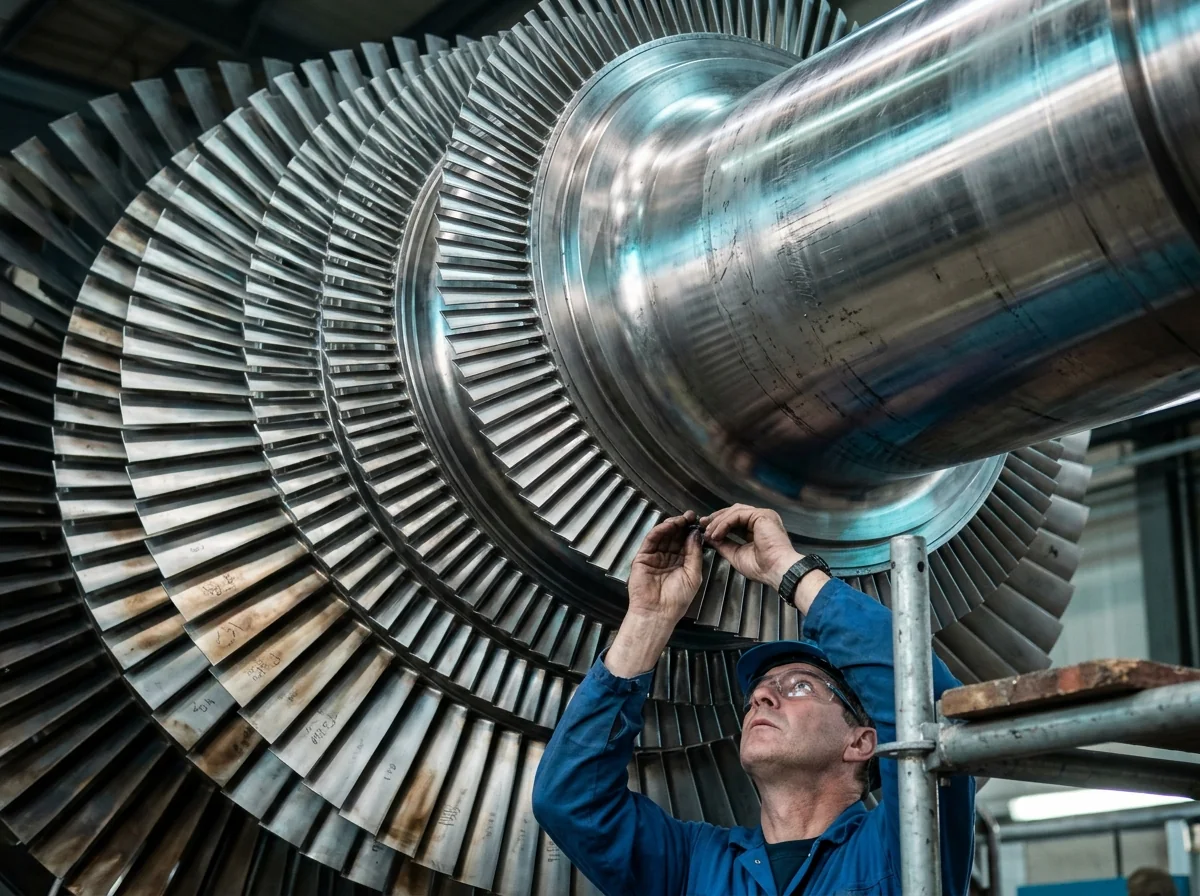
Hot-duct linkage pins and damper spindlesA-286 round bar provides machining stock for hot-duct linkage pins and damper spindles, including turned shoulders, bearing seats and threaded ends. Bar diameter includes the allowance for finishing the final part. Hot dwell and start-stop expansion act on the supported or moving component.
Chemical Processing
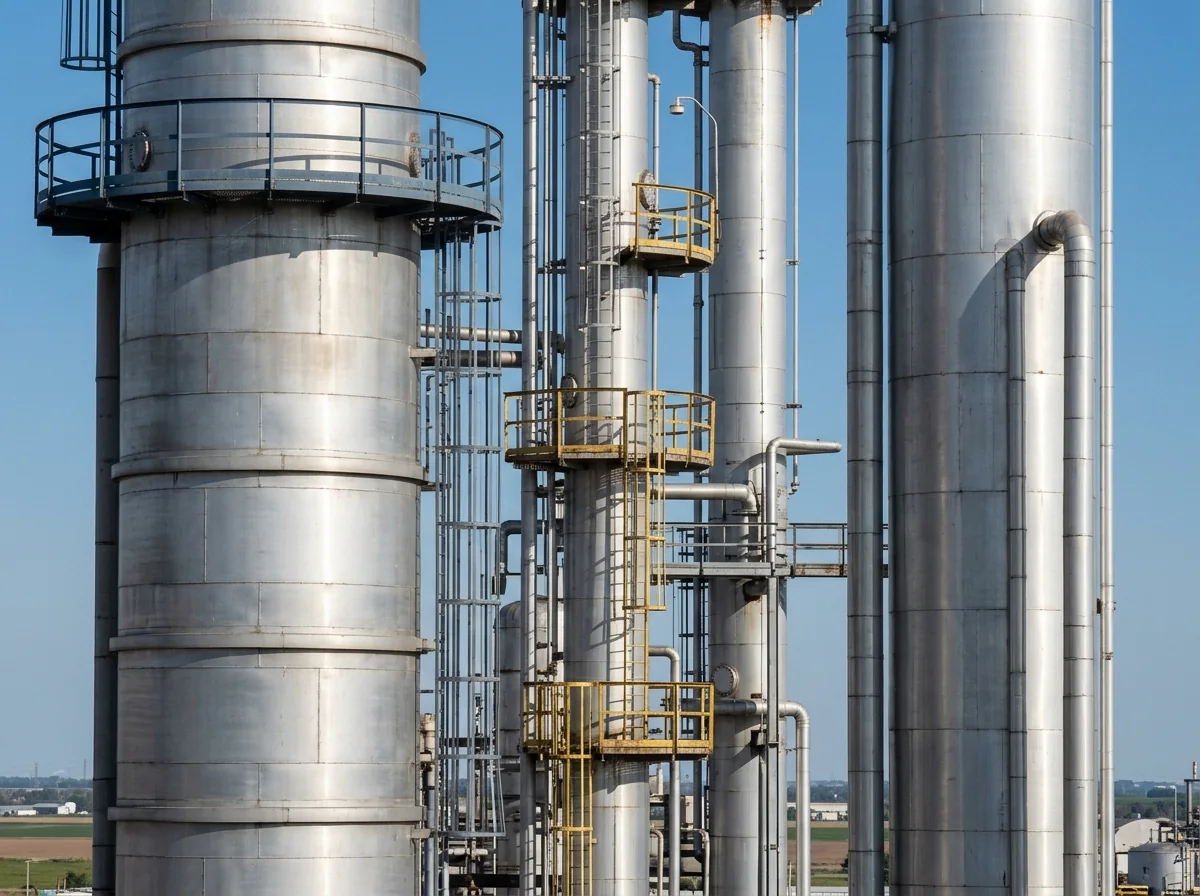
Reformer support pins and heater-fixture rodsA-286 round bar provides machining stock for reformer support pins and heater-fixture rods, including turned shoulders, bearing seats and threaded ends. Bar diameter includes the allowance for finishing the final part. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same round bar. Different material priorities.
A-286 material dataIncoloy 800HT
Tightly controlled carbon and Al + Ti for creep duty.
- Connection priority
- The mechanical requirement of the machined section
- N08811 material control
- 800HT tightens the 800-family chemistry around creep performance. Its solution-treated, coarse-grain condition and N08811 identity should remain linked through forming and final acceptance. At the machined diameter and cut surfaces of the future part, the relevant metal temperature can differ from the process or furnace set point.
Inconel 718
Precipitation-hardened strength for compact, highly loaded connections.
- Connection priority
- The mechanical requirement of the machined section
- Strength after aging
- Machine-stock properties and final aged properties describe different states. The final heat-treatment lot and mechanical results establish the strength available in the installed part. At the machined diameter and cut surfaces of the future part, the relevant metal temperature can differ from the process or furnace set point.
310S
Low-carbon heat resistance in oxidation-exposed equipment.
- Connection priority
- The mechanical requirement of the machined section
- 310S is not 310H
- S31008 is the low-carbon grade. For a component under sustained hot load, distinguish that specification from the controlled-carbon creep purpose of S31009. At the machined diameter and cut surfaces of the future part, the relevant metal temperature can differ from the process or furnace set point.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S66286 · heat number · ordered condition
- Stock acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Cross-section · Surface · Delivery condition · Heat identity
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your A-286 round bar enquiry
Questions about A-286 round bar
Is the bar condition the same as the finished-part condition?
Not necessarily. A solution-treated or annealed blank may be selected for machining before a specified final treatment. Stock and finished-part mechanical records need to identify the conditions they represent.