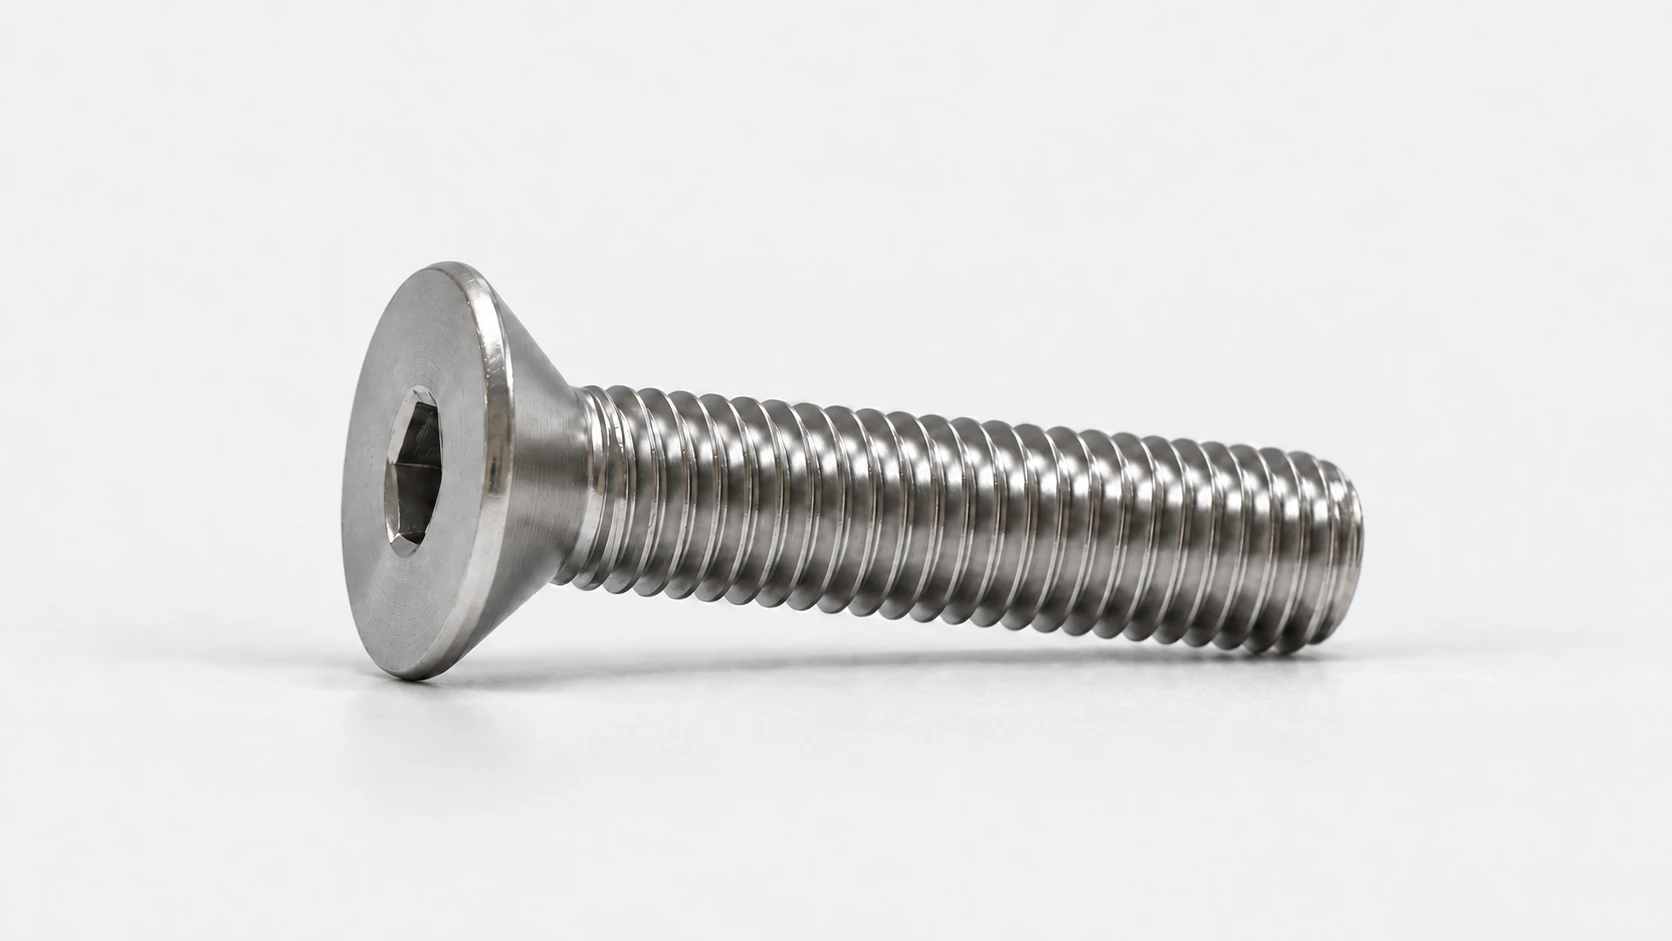
Nimonic 80A Hex socket countersunk screws
ISO 10642ASTM B637
Flush seating puts the load into the conical head of a Nimonic 80A countersunk screw. Aging-developed strength for loaded hot components is combined with a matching head angle and acceptance of the reduced head section.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution treated and aged
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution treated and agedSolution treatment prepares the alloy for controlled precipitation aging, which develops the strength of the ordered condition.
What we can make in Nimonic 80A
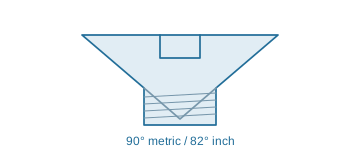
Head angle & seating
90° metric and 82° inch heads need matching countersinks. Head diameter and recess depth control whether the screw sits flush.
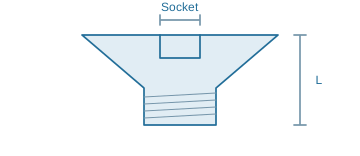
Socket & overall length
Specify overall length including the head. Socket size and depth govern key engagement, especially in shallow head sections.
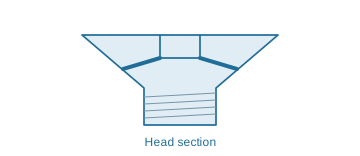
Reduced head loadability
ISO 10642 identifies reduced loadability from the countersunk head and socket geometry. For Inconel 718 or A-286, assess head capacity and seating contact alongside the specified material strength and assembly preload.
- Drive
- Internal hex socket
- Head angle
- 90° metric · 82° inch
- Length basis
- Overall, including head
- Threads
- Metric · UNC · UNF · UNJ
- Final condition
- Solution treated and aged
- Inspection
- Head angle & diameter · Socket size & depth · Overall length · Thread gauges
Manufacturing route
CNC machining suits samples and small batches. Volume heads are formed in a workable condition with the final aging route included in process planning.
Heat treatment & final condition
Solution treatment and the specified aging condition are recorded against the production lot; final dimensions are checked after thermal processing.
Finished geometry
Head angle, socket depth and the head-to-shank transition are inspected with the thread; the reduced head section remains part of finished-part acceptance.
Where Nimonic 80A fits — and what matters
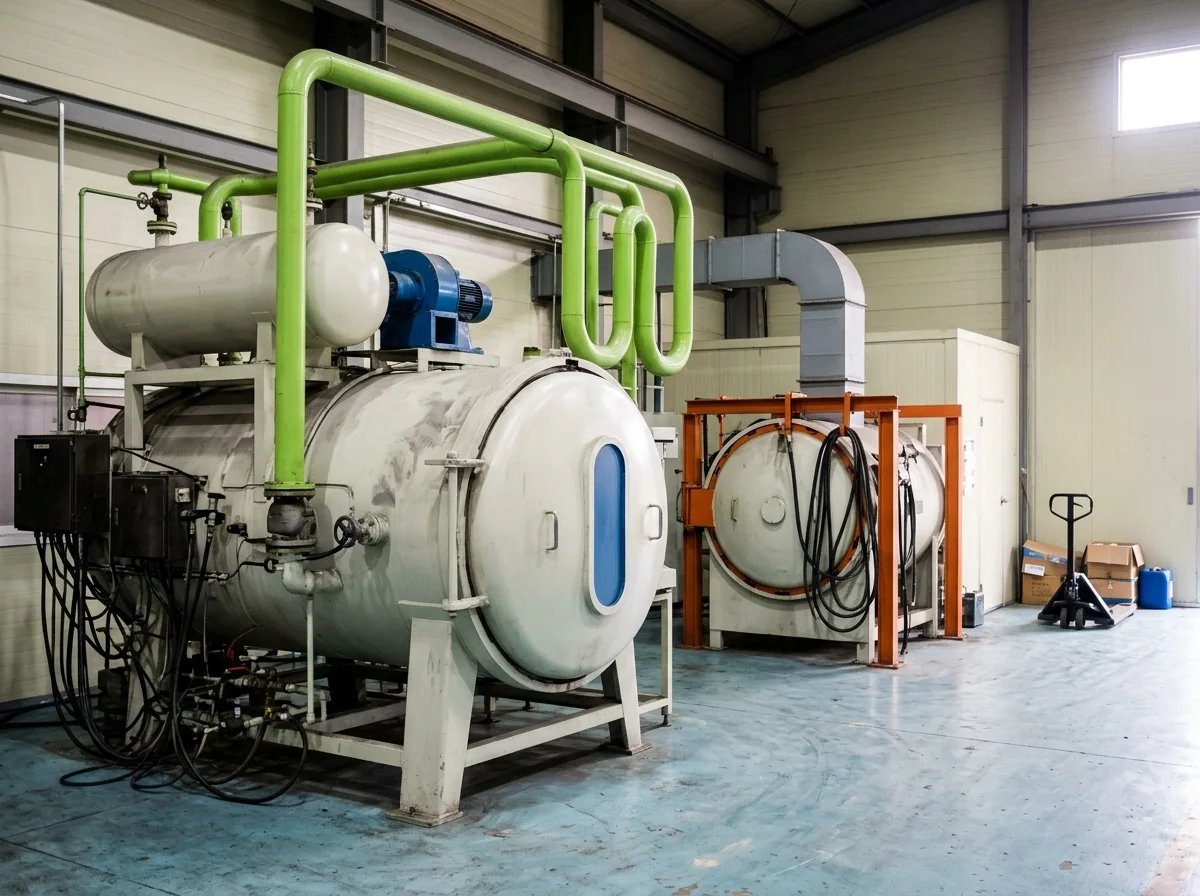
Furnaces & Heat Treatment
Furnace shields and casing panelsNimonic 80A hex socket countersunk screws secure furnace shields and casing panels with the head below or flush with the surface, leaving clearance for neighbouring moving parts or removable covers. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
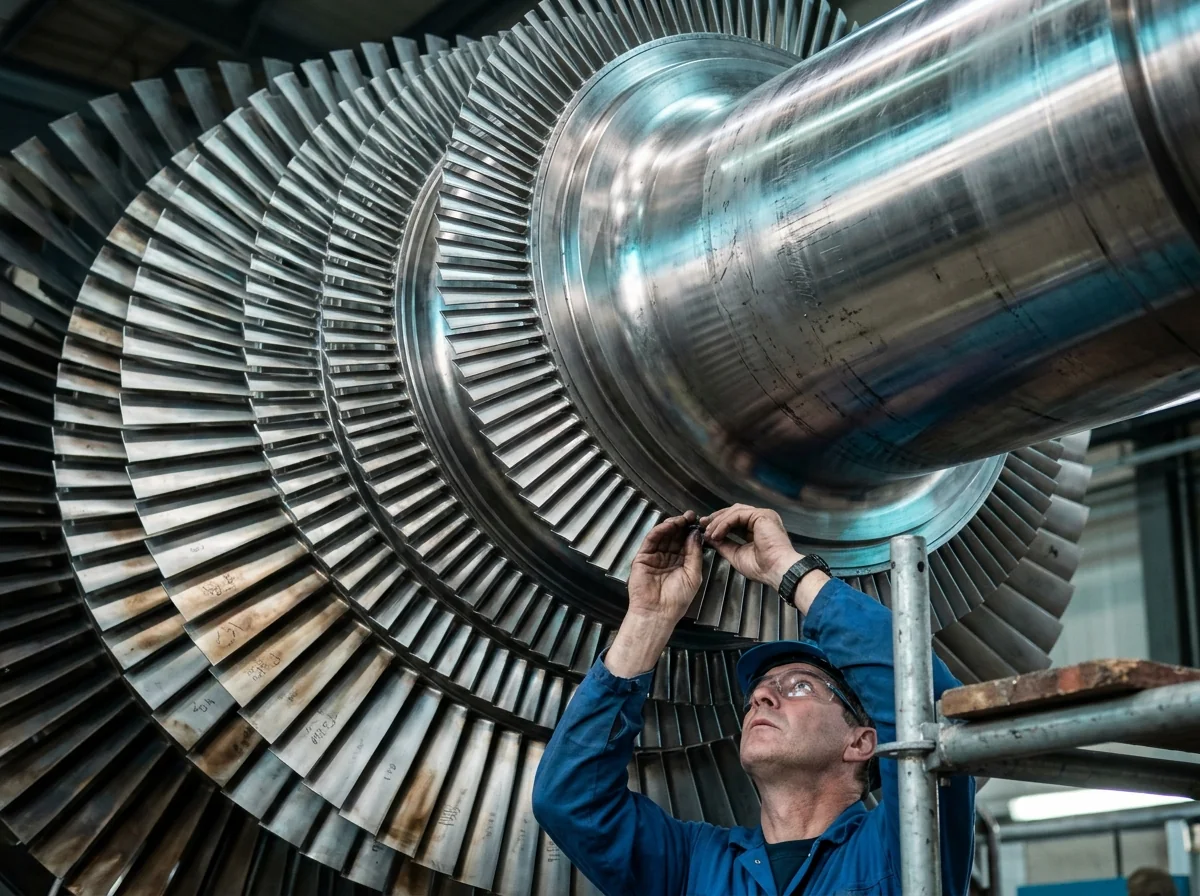
Power & Turbines
Hot-duct shields and thermal bafflesNimonic 80A hex socket countersunk screws secure hot-duct shields and thermal baffles with the head below or flush with the surface, leaving clearance for neighbouring moving parts or removable covers. Hot dwell and start-stop expansion act on the supported or moving component.
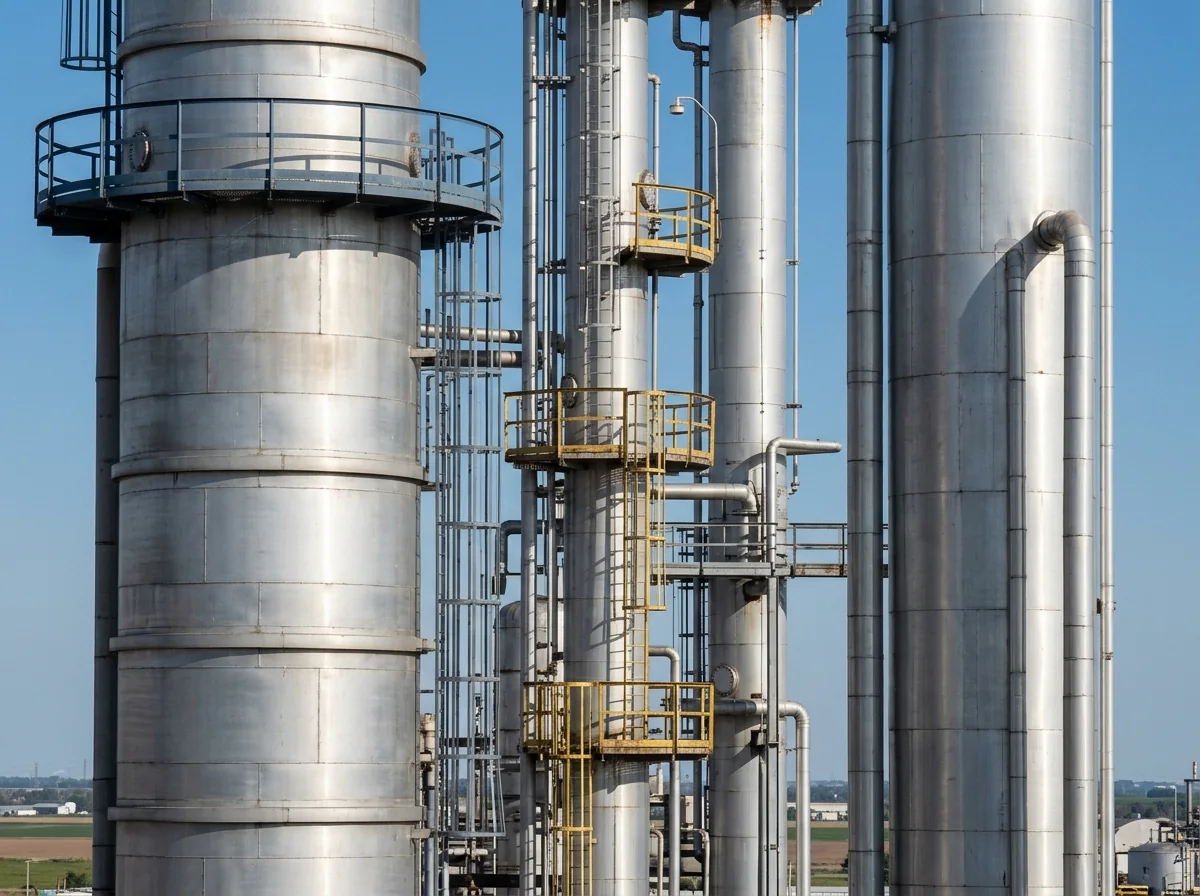
Chemical Processing
Process-heater shields and bafflesNimonic 80A hex socket countersunk screws secure process-heater shields and baffles with the head below or flush with the surface, leaving clearance for neighbouring moving parts or removable covers. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same hex socket countersunk screw. Different material priorities.
Nimonic 80A material dataIncoloy 800HT
Tightly controlled carbon and Al + Ti for creep duty.
- Connection priority
- Head-bearing stress in the reduced countersunk section
- N08811 material control
- 800HT tightens the 800-family chemistry around creep performance. Its solution-treated, coarse-grain condition and N08811 identity should remain linked through forming and final acceptance. At the conical seat and recessed socket, the relevant metal temperature can differ from the process or furnace set point.
Inconel 718
Precipitation-hardened strength for compact, highly loaded connections.
- Connection priority
- Head-bearing stress in the reduced countersunk section
- Strength after aging
- Machine-stock properties and final aged properties describe different states. The final heat-treatment lot and mechanical results establish the strength available in the installed part. At the conical seat and recessed socket, the relevant metal temperature can differ from the process or furnace set point.
A-286
Aged iron–nickel alloy strength for hot bolting.
- Connection priority
- Head-bearing stress in the reduced countersunk section
- Grade 660 class
- An ASTM A453 Grade 660 order includes its class and corresponding processing requirements. The alloy name A-286 alone does not identify that acceptance condition. At the conical seat and recessed socket, the relevant metal temperature can differ from the process or furnace set point.
From drawing to documented delivery
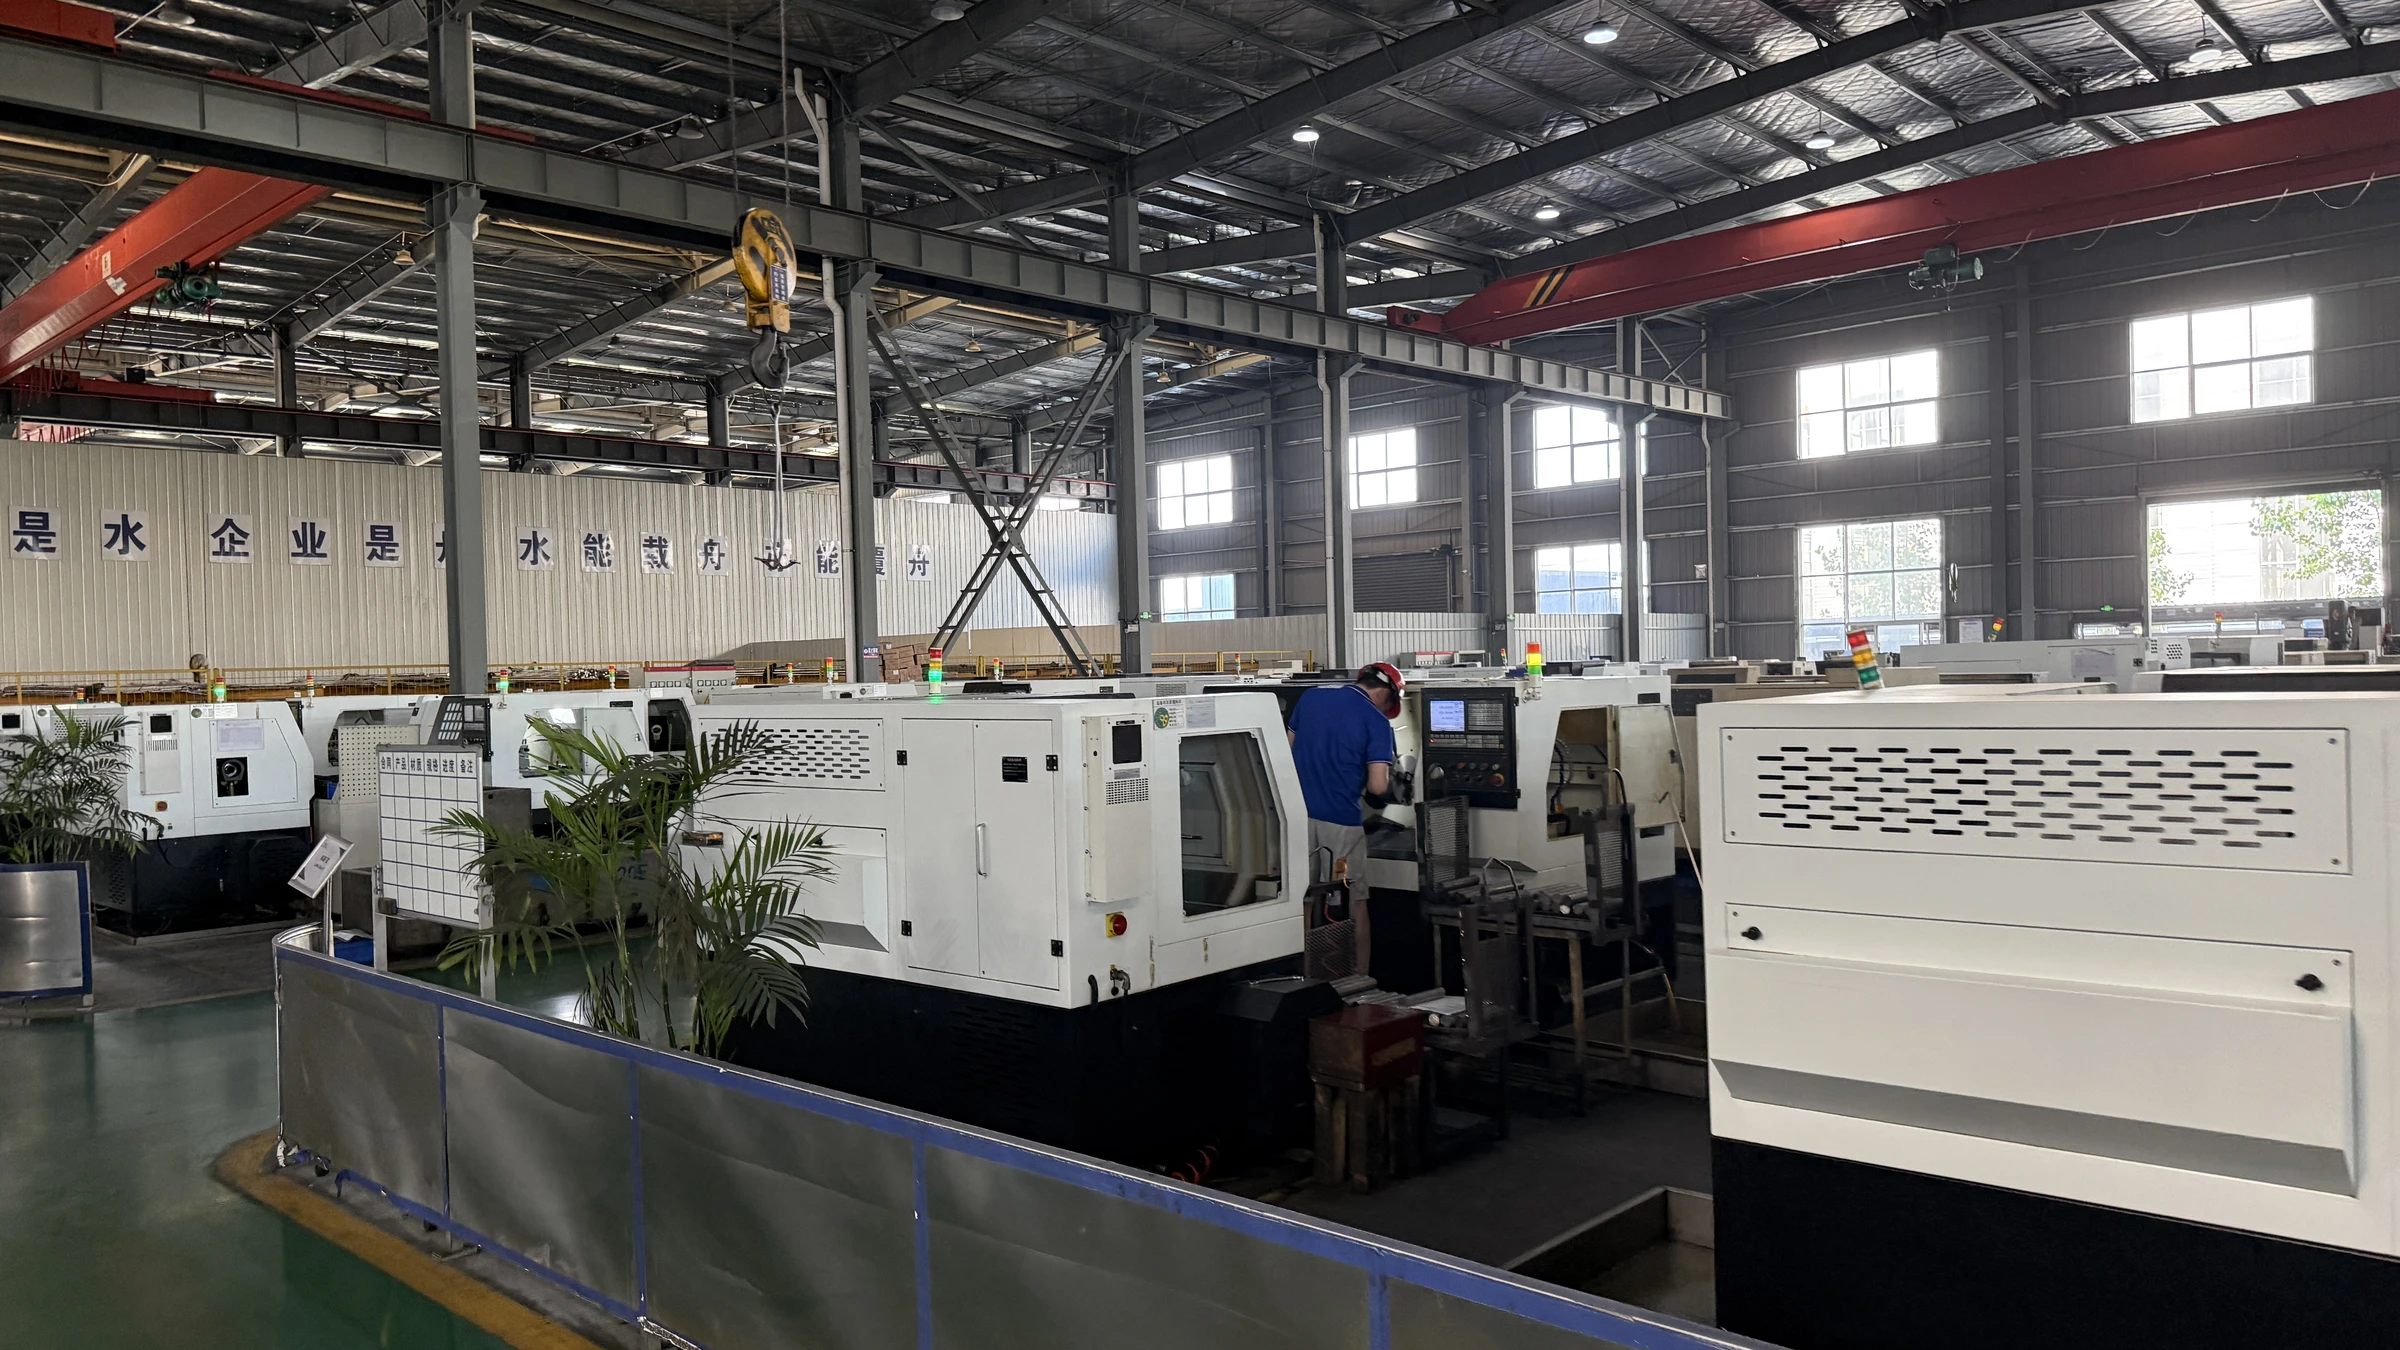
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
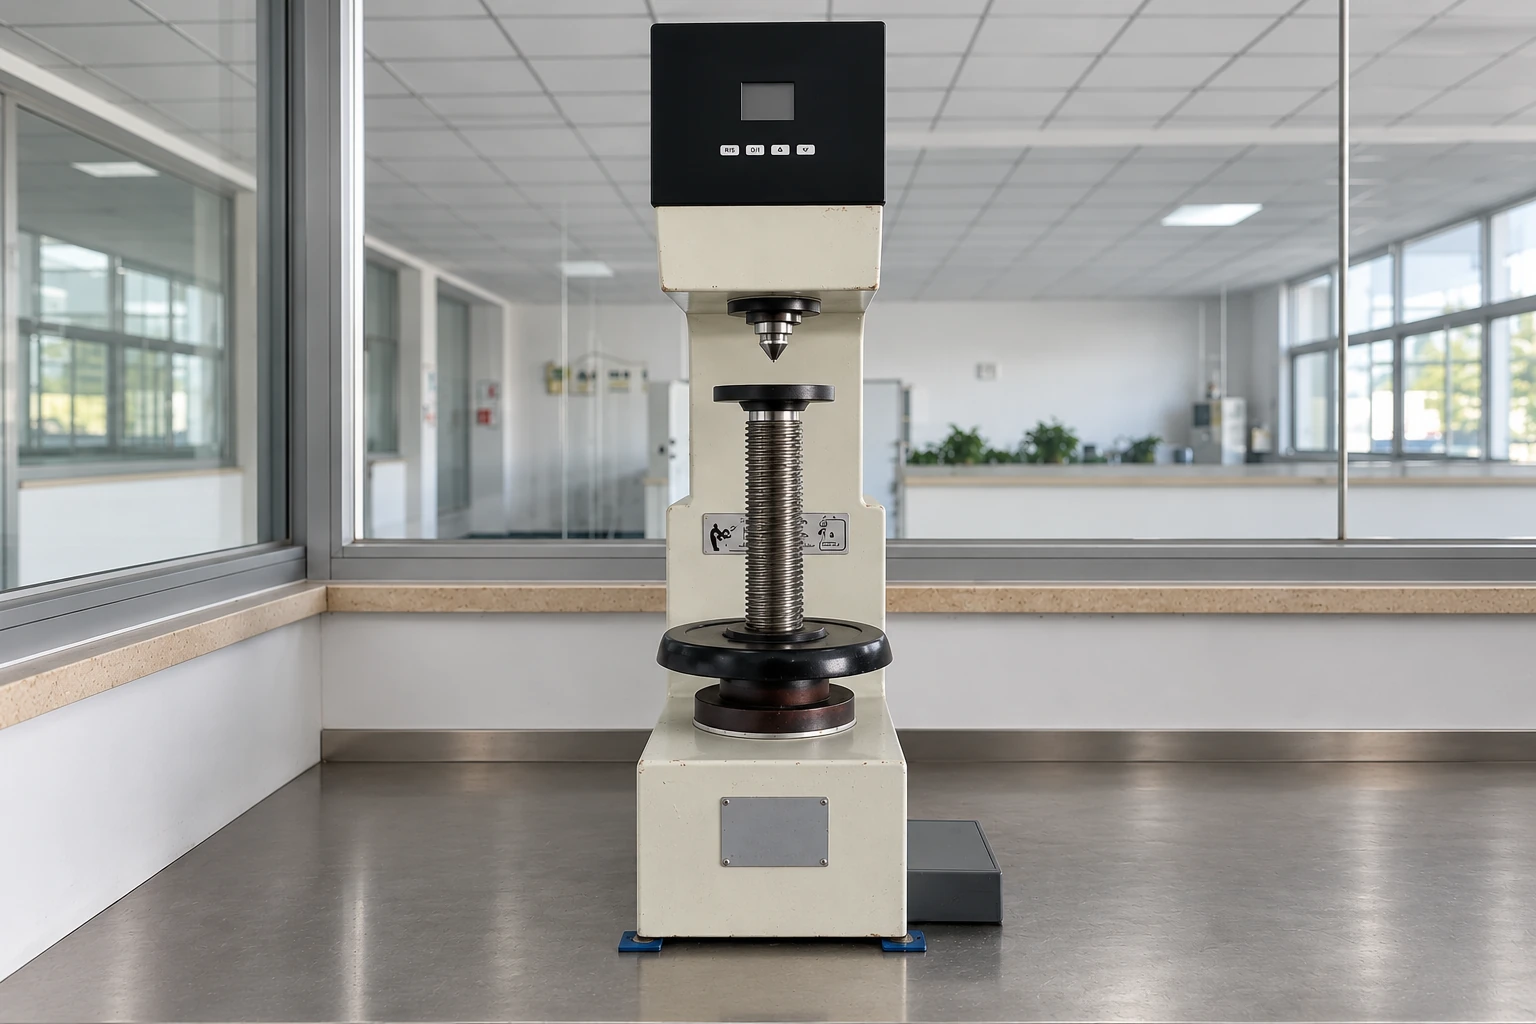
- 03Final inspectionGeometry, threads and ordered tests
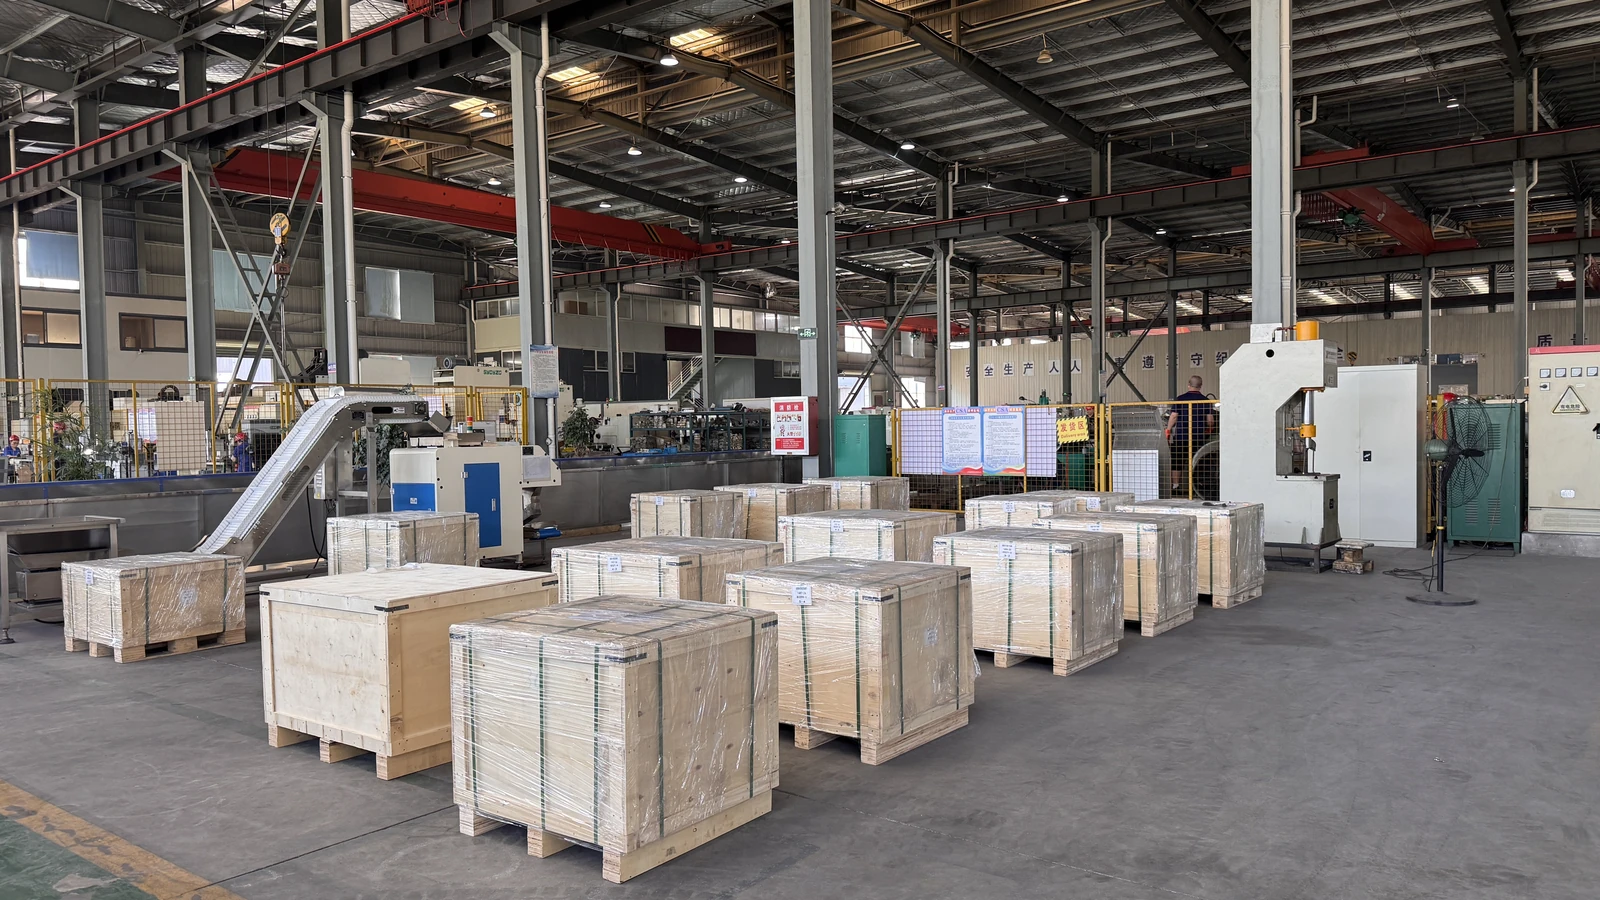
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N07080 · heat number · ordered condition
- Final-part acceptance
- Lot-linked aging record and mechanical acceptance in the final condition.
- Dimensional record
- Head angle & diameter · Socket size & depth · Overall length · Thread gauges
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your Nimonic 80A hex socket countersunk screw enquiry
Questions about Nimonic 80A hex socket countersunk screws
Does a high-strength alloy remove countersunk-head loadability limits?
The conical head and socket still reduce the available section. Head-bearing stress, countersink contact and housing thread engagement need assessment alongside the final alloy strength.