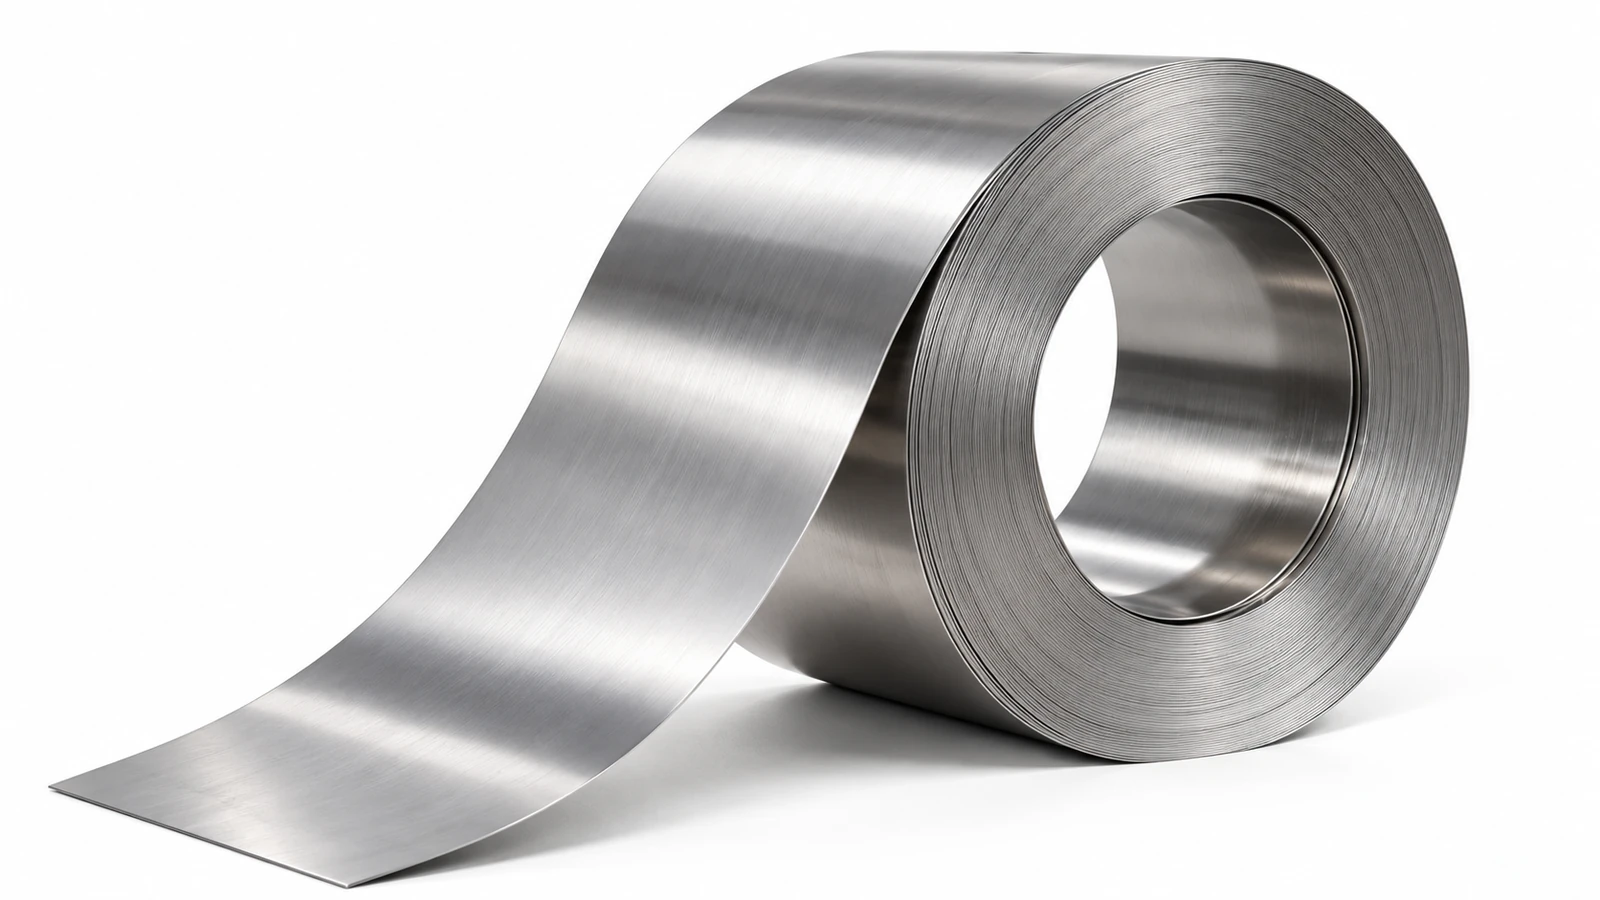
Incoloy 800HT strip
ASTM B409
Incoloy 800HT strip combines tightly controlled carbon and Al + Ti for creep duty with a thin section for clips, shims and formed parts. Edge condition, temper and rolling direction affect both production feeding and the finished bend.
- MOQ
- 100 kg
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed (≥1149°C / 2100°F)
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Heat Treatment
Solution annealedThe specified solution treatment develops the controlled grain structure needed for sustained high-temperature creep duty.
What we can make in Alloy 800HT
Coiled strip
Use for progressive stamping, spring clips and repeated forming. Strip width, thickness and coil dimensions must suit the tool and feed line to maintain consistent component geometry.
Cut lengths
Use for short-run brackets, shims and fabricated pieces when coil handling adds unnecessary setup. Flatness and length tolerance help the blank seat consistently in the tool.
Edge & camber
For narrow stamped or formed parts, control slit-edge burrs to protect tools and contact surfaces. Excess camber pulls the strip away from the intended feed path and affects registration.
- Size
- Thickness × width
- Supply form
- Coils · Cut lengths
- Edges
- Slit · Finished edges
- Condition
- Grade-specific temper
- Final condition
- Solution annealed (≥1149°C / 2100°F)
- Inspection
- Cross-section · Surface · Delivery condition · Heat identity
Supply & preparation
Slitting and cut-length preparation follow the requested width, thickness and edge condition. Rolling direction is retained where the forming drawing needs it.
Material condition
Solution annealing at a minimum of 1149°C (2100°F) establishes the coarse-grain condition used for creep resistance. The heat-treatment record and grain-size result identify this delivery state.
Finished geometry
Thickness variation, edge burr, coil set and surface finish determine suitability for the next stamping or forming step.
Where 800HT fits — and what matters
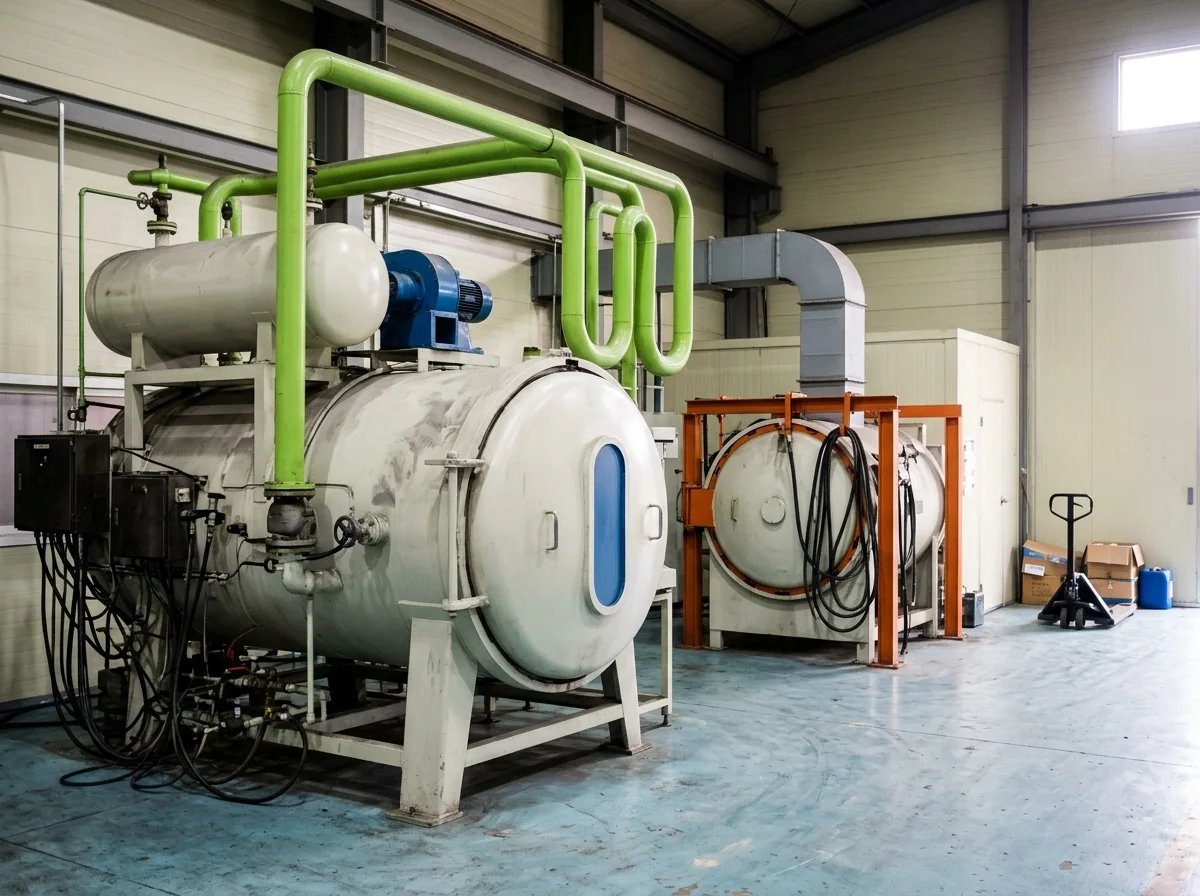
Furnaces & Heat Treatment
Retort and furnace-access coversIncoloy 800HT strip is slit and formed into shims, retaining clips or seal-support pieces around retort and furnace-access covers. Thickness, edge finish and bend direction control the finished fit. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
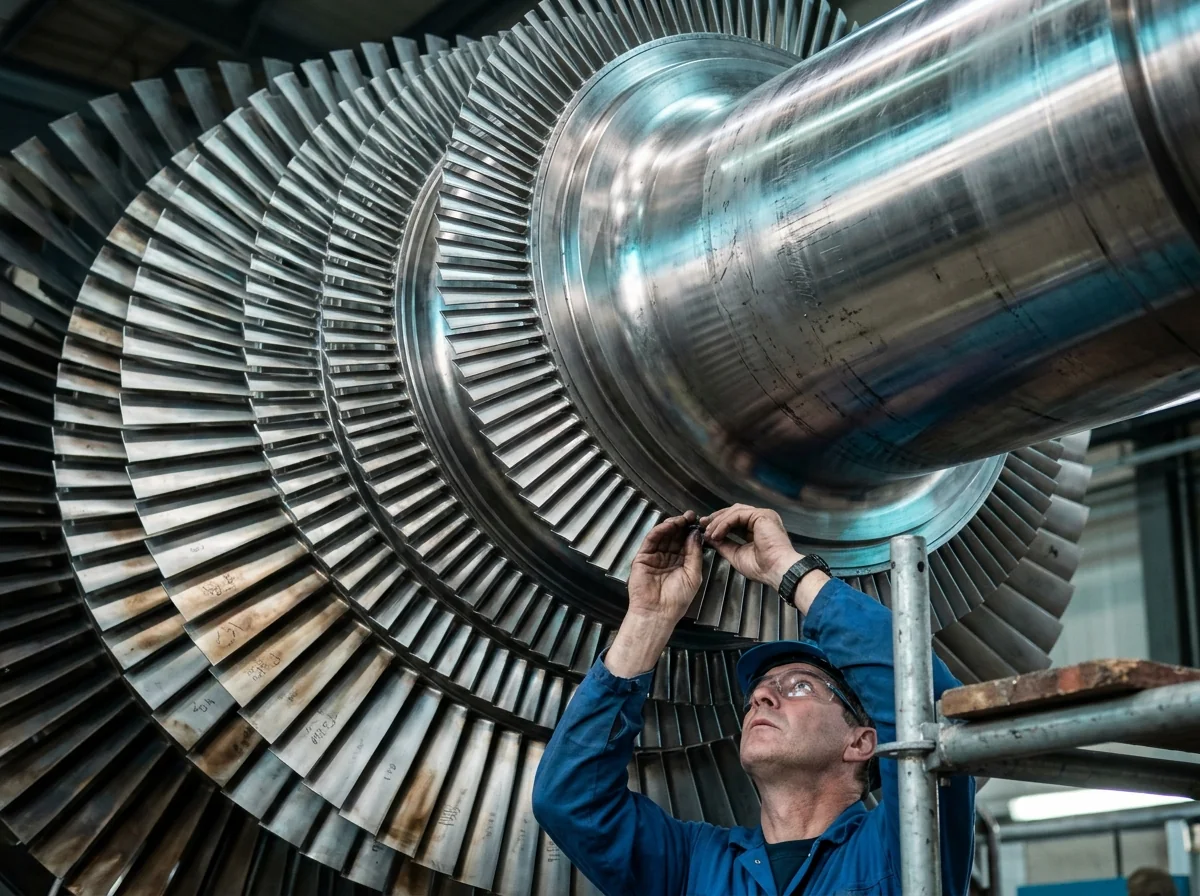
Power & Turbines
Hot-gas access covers and inspection closuresIncoloy 800HT strip is slit and formed into shims, retaining clips or seal-support pieces around hot-gas access covers and inspection closures. Thickness, edge finish and bend direction control the finished fit. Hot dwell and start-stop expansion act on the supported or moving component.
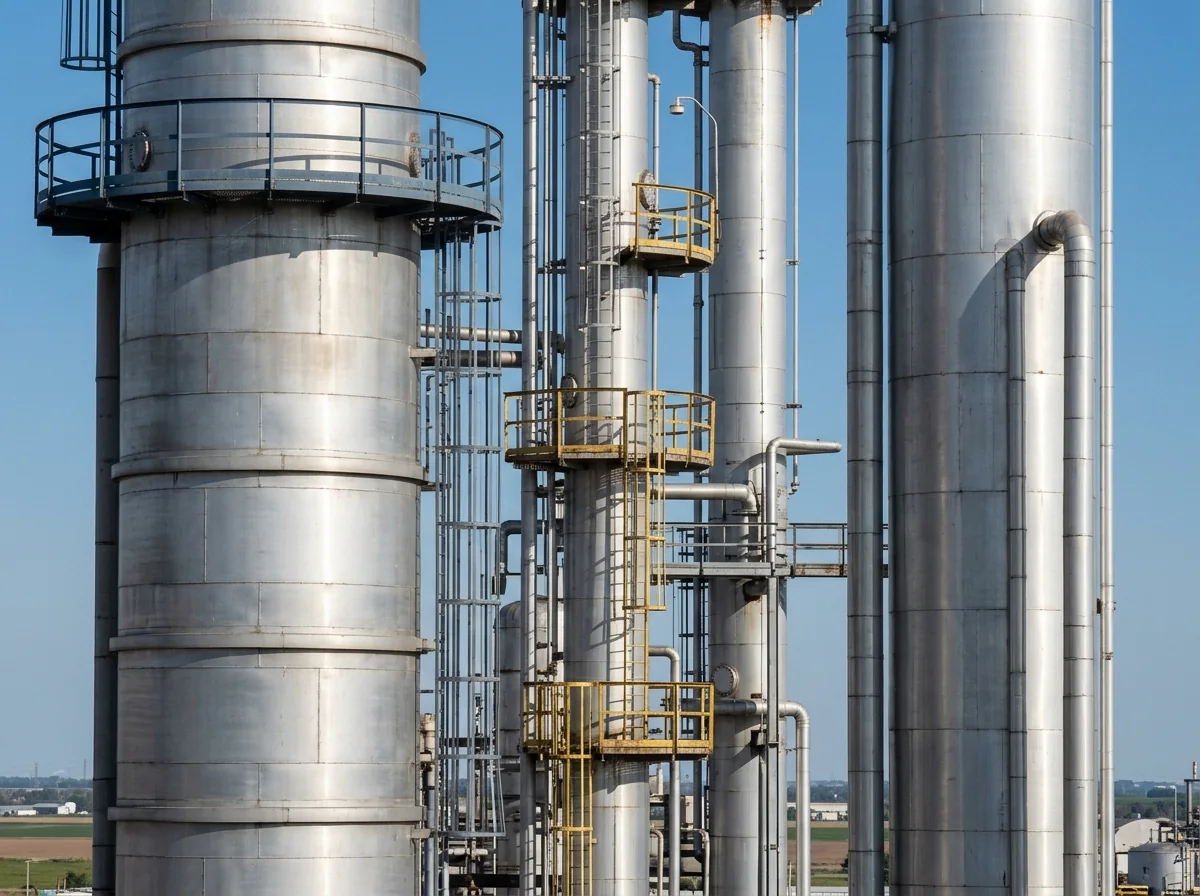
Chemical Processing
Reformer access covers and hot-gas inspection closuresIncoloy 800HT strip is slit and formed into shims, retaining clips or seal-support pieces around reformer access covers and hot-gas inspection closures. Thickness, edge finish and bend direction control the finished fit. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same strip. Different material priorities.
Incoloy 800HT material dataIncoloy 800
UNS N08800- Carbon
- ≤0.10%
- What changes
- General heat and oxidation resistance; no grain-size requirement in the family comparison.
Incoloy 800H
UNS N08810- Carbon
- 0.05–0.10%
- What changes
- Controlled carbon and coarse-grain condition for creep and stress-rupture duty.
Incoloy 800HT
UNS N08811 · Current grade- Carbon
- 0.06–0.10%
- What changes
- Tighter carbon and Al + Ti control (0.85–1.20%), with solution treatment and coarse grain for creep duty.
From drawing to documented delivery
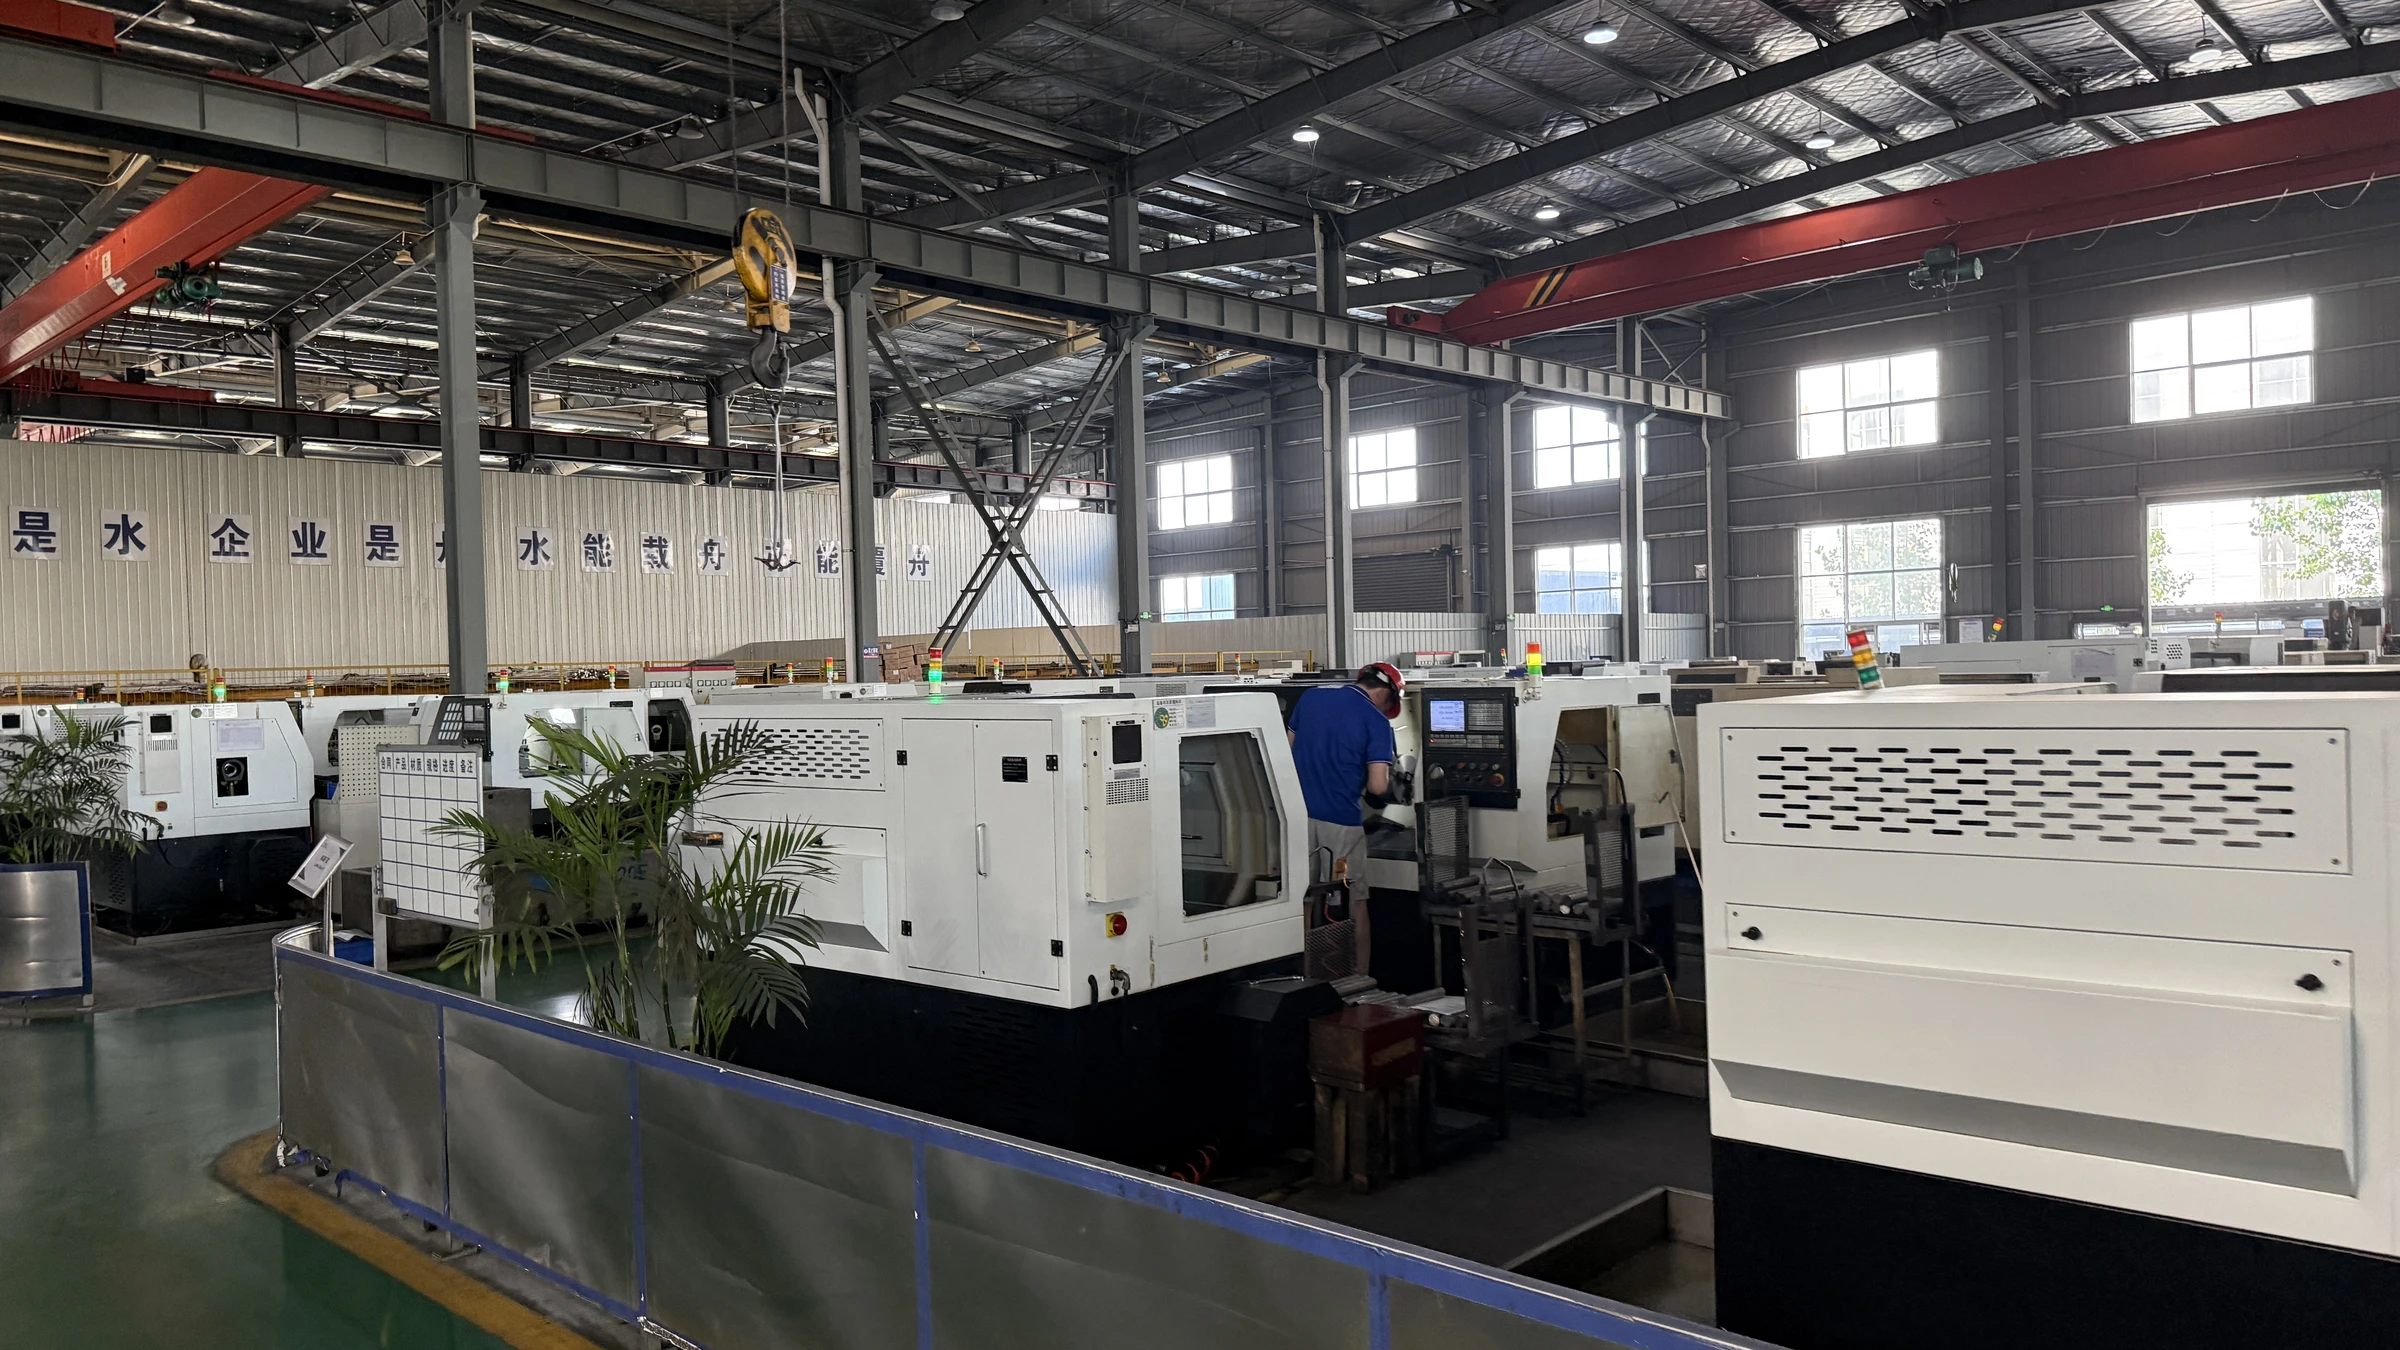
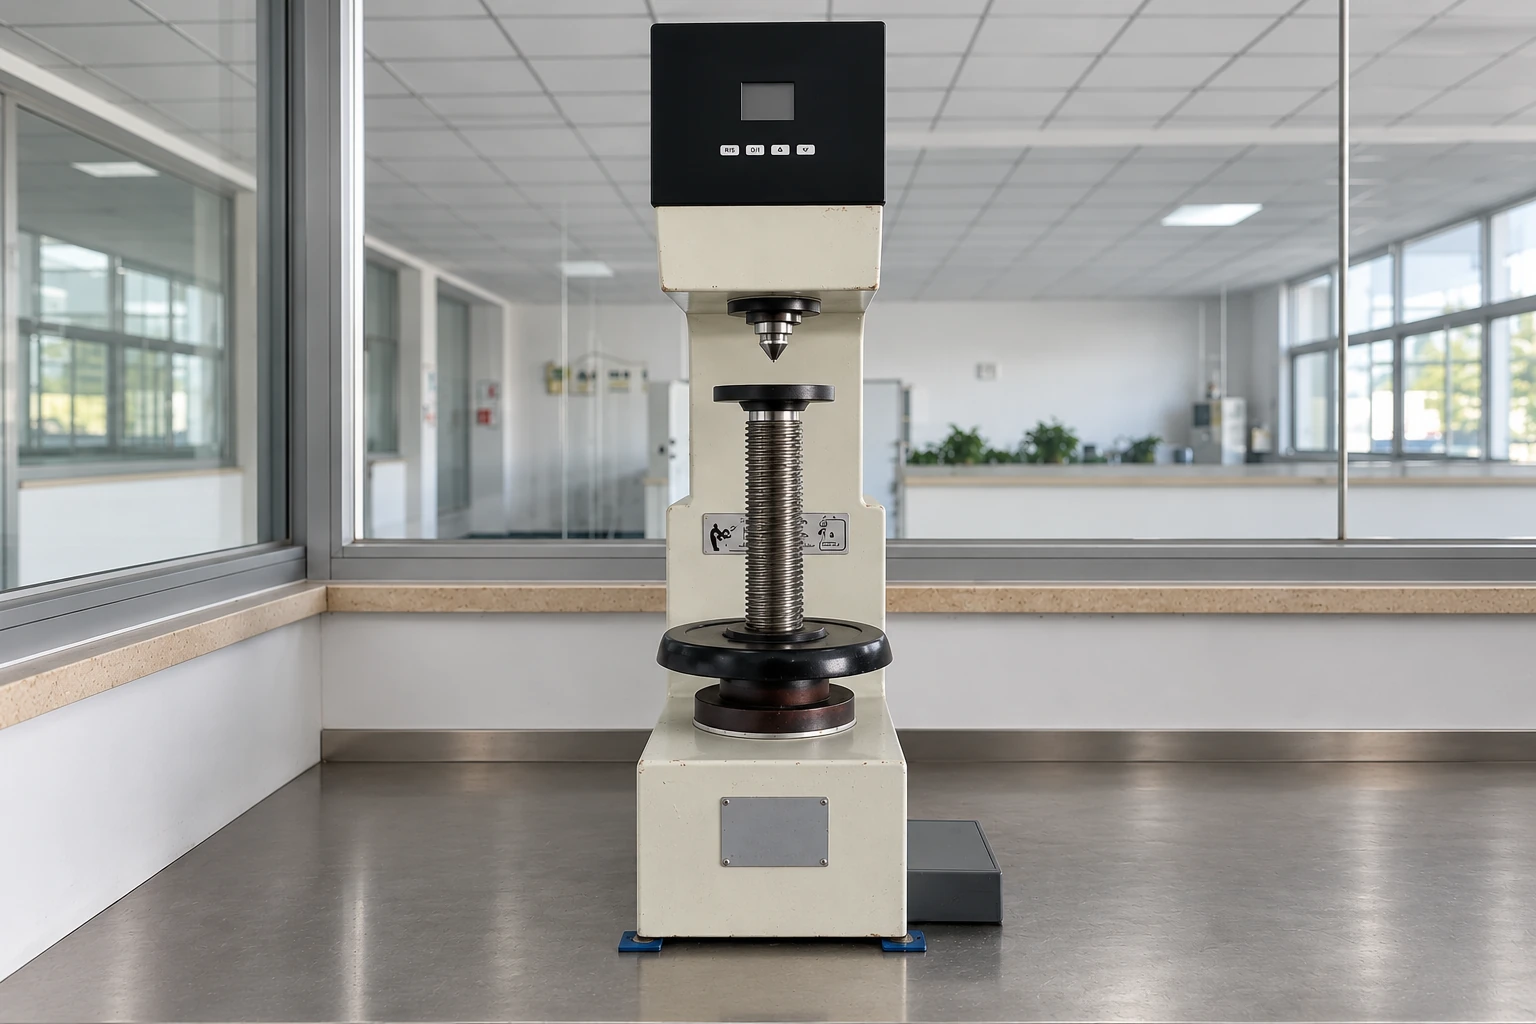
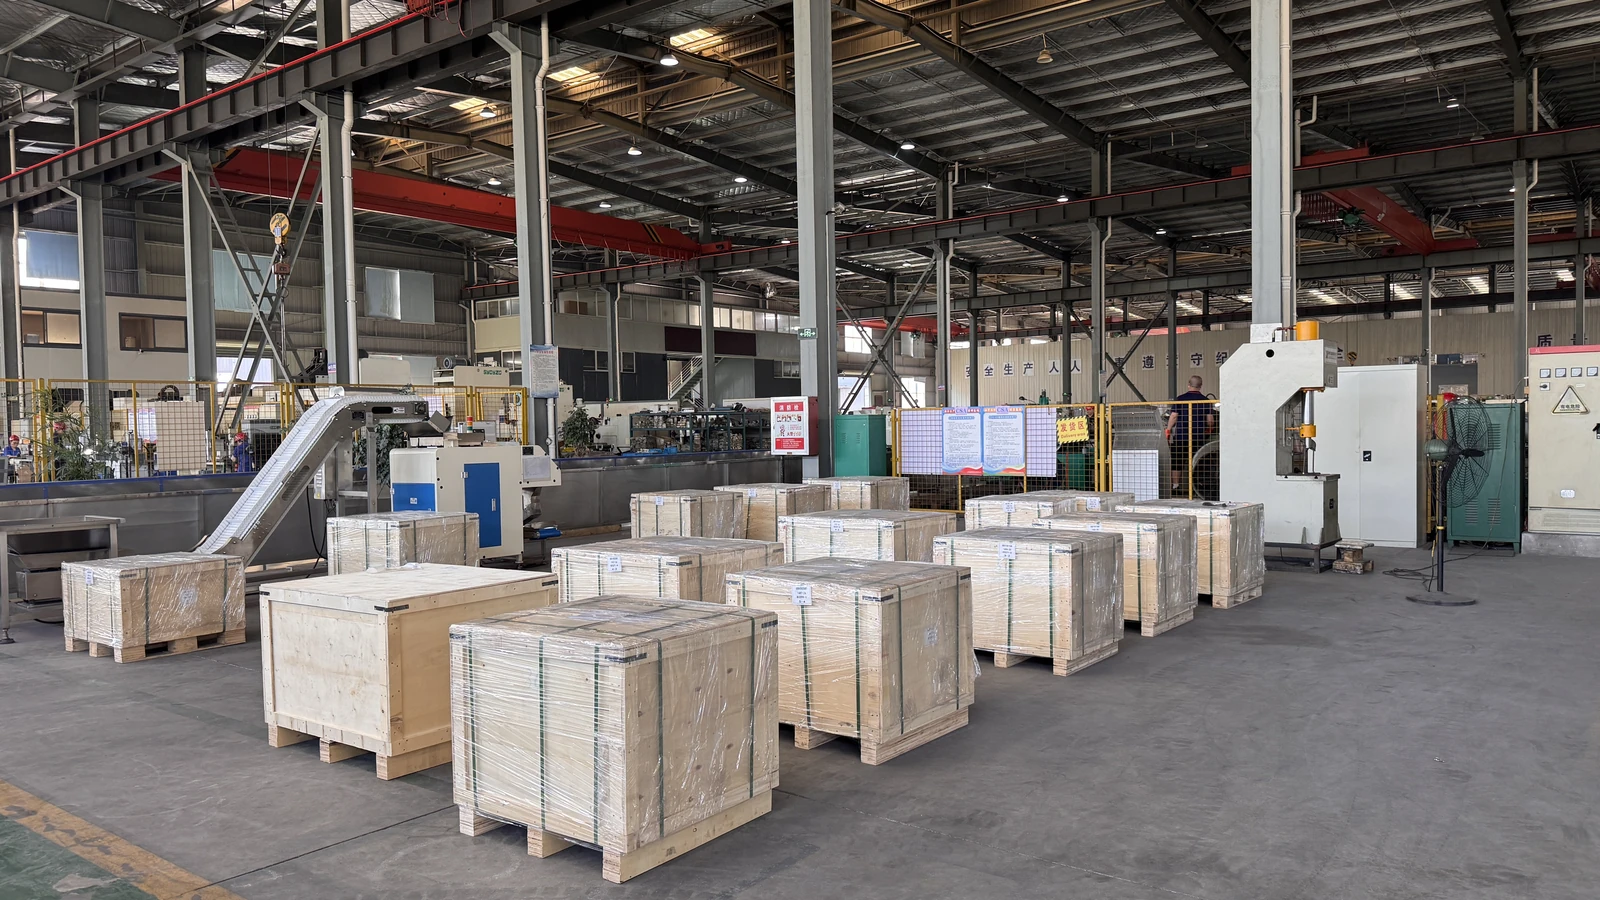
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N08811 · heat number · ordered condition
- Stock acceptance
- UNS grade, carbon and alloy chemistry, solution-treatment record and ordered grain-size evidence.
- Dimensional record
- Cross-section · Surface · Delivery condition · Heat identity
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your 800HT strip enquiry
Questions about 800HT strip
Why does edge condition belong on a strip order?
A slit edge can become the most highly strained edge during forming. Burr direction, edge finish and the chosen bend radius affect the next operation and the finished contact surface.