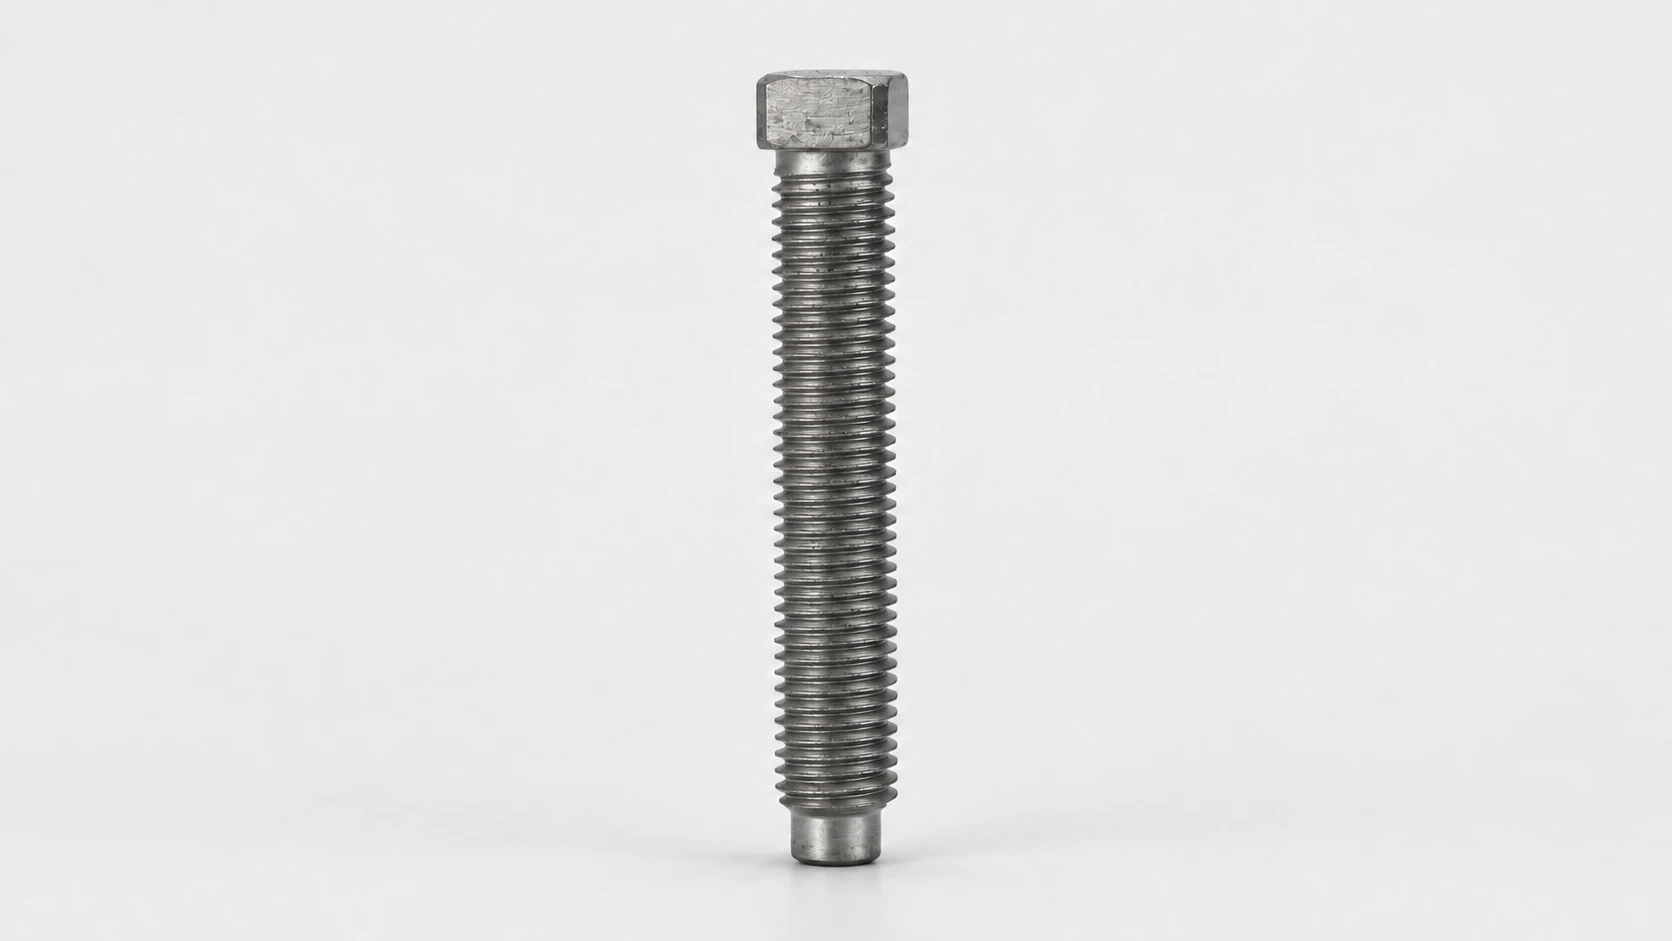
Incoloy 800HT Square-head positioning bolts
ASME B18.2.1ASTM B408
Incoloy 800HT positioning bolts separate anti-rotation at the square head from location at the shoulder. The material’s tightly controlled carbon and Al + Ti for creep duty applies to these loaded contact surfaces as well as the thread.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed (≥1149°C / 2100°F)
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealedThe specified solution treatment develops the controlled grain structure needed for sustained high-temperature creep duty.
What we can make in Alloy 800HT
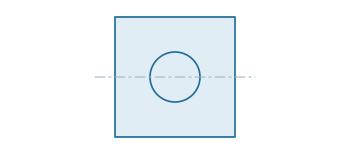
Square head
Capture the square head in a matching slot or pocket to stop rotation while tightening from the nut side. Head width and pocket clearance determine how much turning play remains.
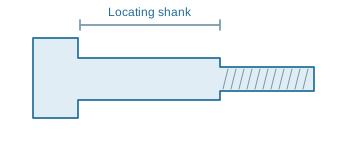
Locating shank
Use a machined step or shank to locate fixture plates and adjustable tooling. Specify its fit to the mating bore when repeatable position matters; thread clearance cannot provide that locating accuracy.
- Drive
- External square
- Interface
- Head flats · Shank steps
- Length basis
- Under head
- Threads
- Metric · Inch
- Final condition
- Solution annealed (≥1149°C / 2100°F)
- Inspection
- Head flats · Locating diameter · Step lengths · Threads
Manufacturing route
CNC machining suits samples and small lots. Cold heading or hot forging is selected for volume production according to alloy formability, head section and size.
Heat treatment & final condition
Solution annealing at a minimum of 1149°C (2100°F) establishes the coarse-grain condition used for creep resistance. The heat-treatment record and grain-size result identify this delivery state.
Finished geometry
Head geometry, bearing face, shank and thread fit are checked after the final machining and thermal operations.
Where 800HT fits — and what matters
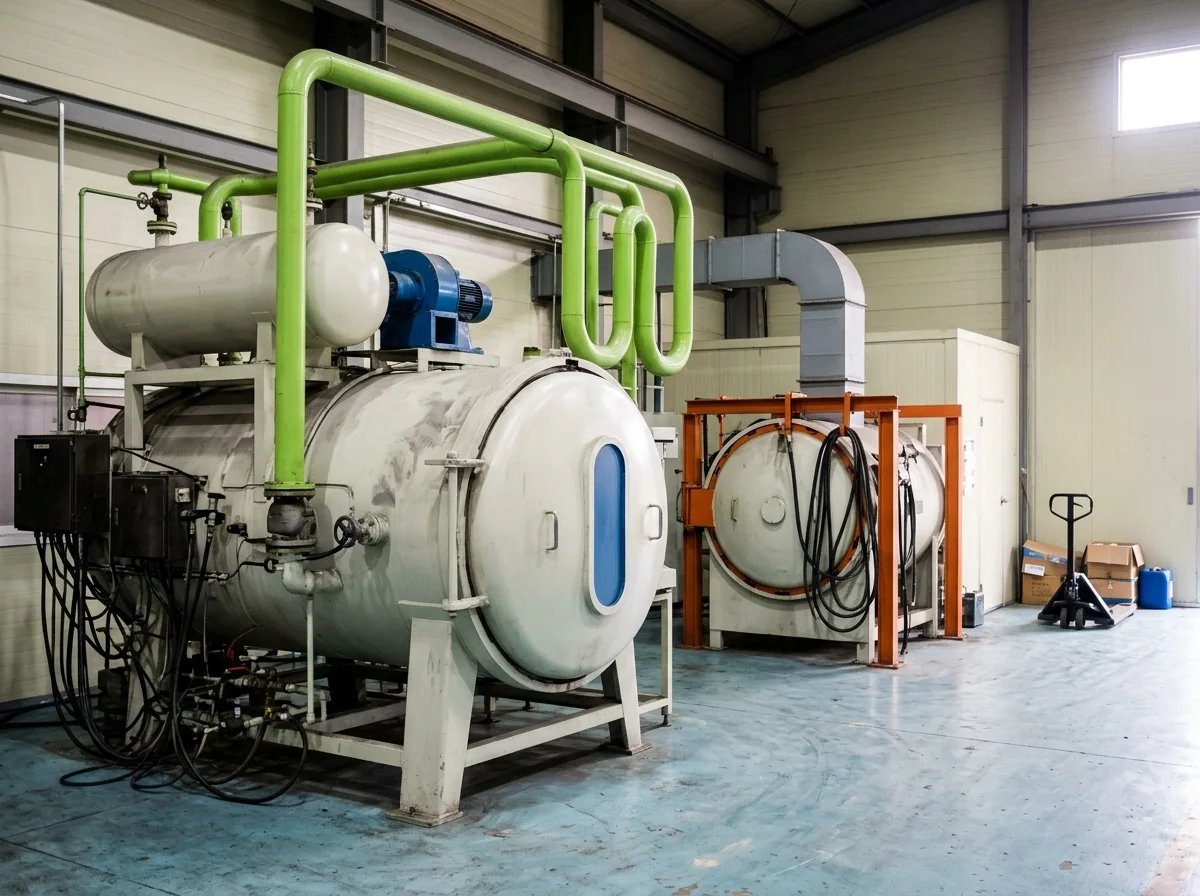
Furnaces & Heat Treatment
Heat-treatment fixturesIncoloy 800HT square-head positioning bolts set stops and clamp positions on heat-treatment fixtures. The square head provides tool purchase while the end face or point bears on the positioned component. Hot dwell, thermal expansion and repeated furnace cycles set the working load.
Power & Turbines
Boiler-duct supports and hot auxiliary bracketsIncoloy 800HT square-head positioning bolts set stops and clamp positions on boiler-duct supports and hot auxiliary brackets. The square head provides tool purchase while the end face or point bears on the positioned component. Hot dwell and start-stop expansion act on the supported or moving component.
Chemical Processing
Reformer tube-support and heater fixturesIncoloy 800HT square-head positioning bolts set stops and clamp positions on reformer tube-support and heater fixtures. The square head provides tool purchase while the end face or point bears on the positioned component. These parts work in the heated equipment zone, where sustained loading and thermal expansion govern their section and clearance.
Same square-head positioning bolt. Different material priorities.
Incoloy 800HT material dataIncoloy 800
UNS N08800- Carbon
- ≤0.10%
- What changes
- General heat and oxidation resistance; no grain-size requirement in the family comparison.
Incoloy 800H
UNS N08810- Carbon
- 0.05–0.10%
- What changes
- Controlled carbon and coarse-grain condition for creep and stress-rupture duty.
Incoloy 800HT
UNS N08811 · Current grade- Carbon
- 0.06–0.10%
- What changes
- Tighter carbon and Al + Ti control (0.85–1.20%), with solution treatment and coarse grain for creep duty.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
- 03Final inspectionGeometry, threads and ordered tests
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS N08811 · heat number · ordered condition
- Final-part acceptance
- UNS grade, carbon and alloy chemistry, solution-treatment record and ordered grain-size evidence.
- Dimensional record
- Head flats · Locating diameter · Step lengths · Threads
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your 800HT square-head positioning bolt enquiry
Questions about 800HT square-head positioning bolts
Which tolerance should locate the component?
Use the specified shoulder or locating diameter, with a matching hole fit. Head clearance serves tool engagement or anti-rotation; it should not silently replace the drawing’s locating datum.