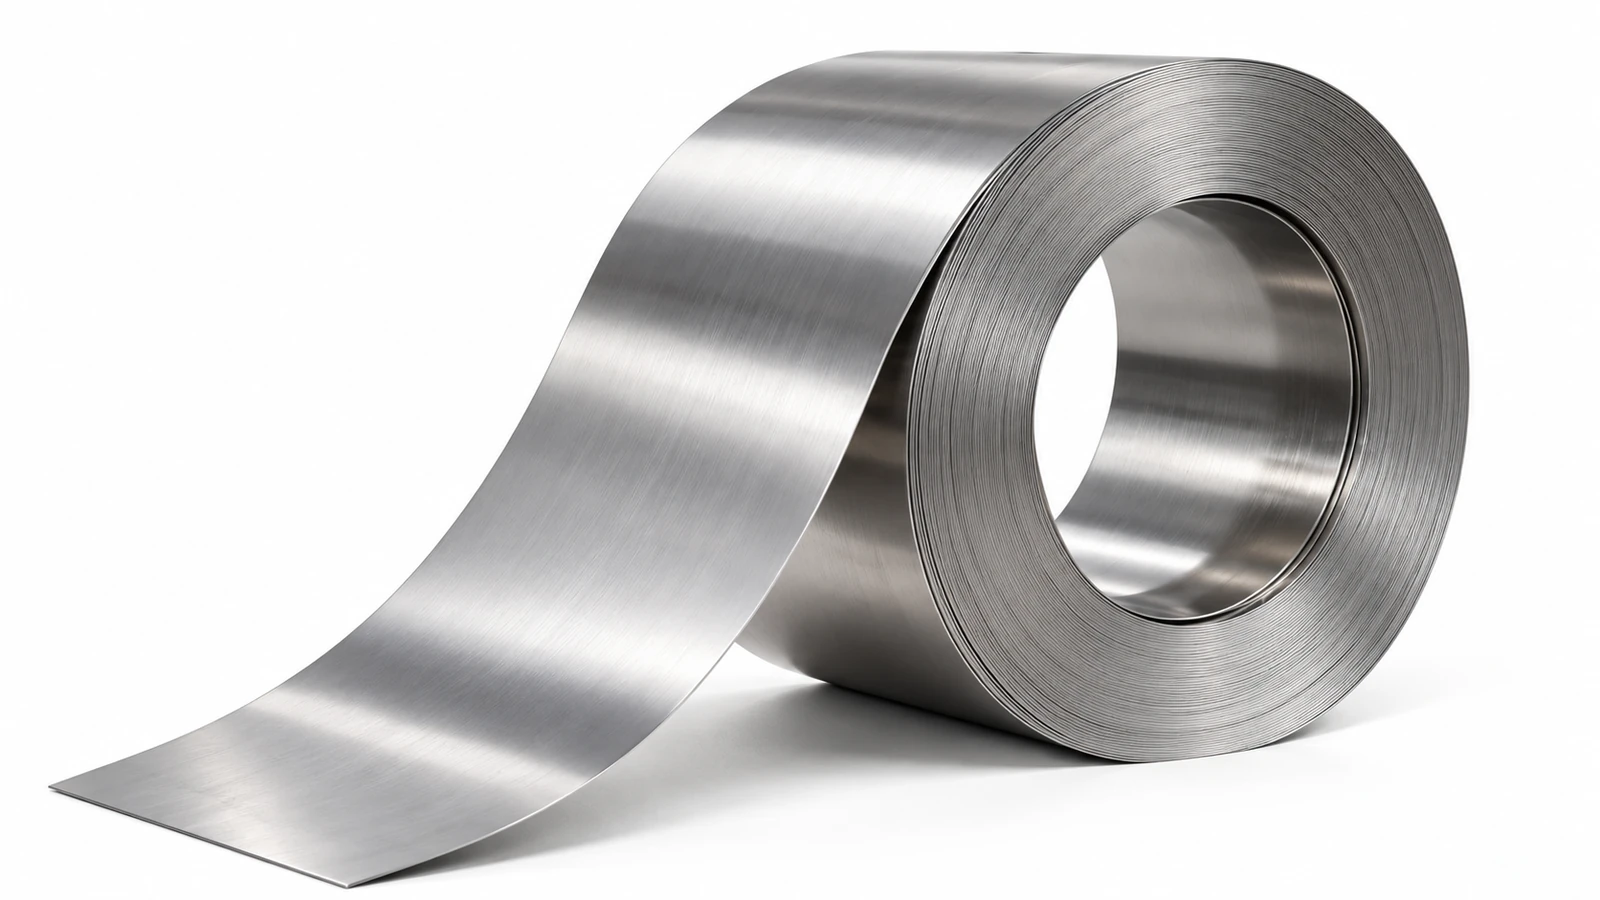
420 strip
EN 10204 3.1
420 strip combines hardness and wear resistance at mechanical contact points with a thin section for clips, shims and formed parts. Edge condition, temper and rolling direction affect both production feeding and the finished bend.
- MOQ
- 100 kg
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Annealed / hardened and tempered
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Heat Treatment
Annealed or hardened and temperedAnnealed stock is easier to machine; hardening followed by tempering establishes the strength and toughness of the ordered final condition.
What we can make in 420
Coiled strip
Use for progressive stamping, spring clips and repeated forming. Strip width, thickness and coil dimensions must suit the tool and feed line to maintain consistent component geometry.
Cut lengths
Use for short-run brackets, shims and fabricated pieces when coil handling adds unnecessary setup. Flatness and length tolerance help the blank seat consistently in the tool.
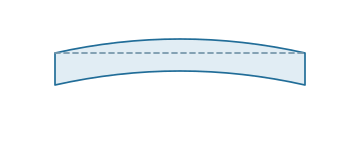
Edge & camber
For narrow stamped or formed parts, control slit-edge burrs to protect tools and contact surfaces. Excess camber pulls the strip away from the intended feed path and affects registration.
- Size
- Thickness × width
- Supply form
- Coils · Cut lengths
- Edges
- Slit · Finished edges
- Condition
- Grade-specific temper
- Final condition
- Annealed · hardened and tempered
- Inspection
- Cross-section · Surface · Delivery condition · Heat identity
Supply & preparation
Slitting and cut-length preparation follow the requested width, thickness and edge condition. Rolling direction is retained where the forming drawing needs it.
Material condition
Hardening and tempering set the final hardness and toughness. Finish dimensions are checked after heat treatment.
Finished geometry
Thickness variation, edge burr, coil set and surface finish determine suitability for the next stamping or forming step.
Where 420 fits — and what matters
Industrial Machinery & Automation
Machine housings and service covers420 strip is slit and formed into shims, retaining clips or seal-support pieces around machine housings and service covers. Thickness, edge finish and bend direction control the finished fit. Alignment, operating cycles and replacement access define the working interface.
Automotive & EV Manufacturing Equipment
Test-equipment housings420 strip is slit and formed into shims, retaining clips or seal-support pieces around test-equipment housings. Thickness, edge finish and bend direction control the finished fit. Repeated tooling changes require consistent seating and repeatable assembly dimensions.
Pumps, Valves & OEM
Pump casings and valve bonnets420 strip is slit and formed into shims, retaining clips or seal-support pieces around pump casings and valve bonnets. Thickness, edge finish and bend direction control the finished fit. Repeated maintenance makes fit, engagement and access part of the component specification.
Same strip. Different material priorities.
420 material data316L
Molybdenum-bearing stainless performance in wet equipment.
- Connection priority
- The stiffness and recovery of the formed strip section
- Washdown and retained cleaner
- Cleaner concentration, rinse quality and deposits determine the exposure in covered joints. The low-carbon designation does not independently establish a fastener strength class. Include liquid retained at slit edges, overlap faces and highly strained bends in the exposure description.
17-4 PH
Aging-controlled strength and hardness.
- Connection priority
- The stiffness and recovery of the formed strip section
- H900 versus H1150
- The aging condition changes the balance of strength, hardness and toughness. A replacement part needs the specified H condition, especially where contact wear and shock load occur together.
Inconel 625
Solid-solution strength and resistance to aggressive process liquids.
- Connection priority
- The stiffness and recovery of the formed strip section
- Annealed or solution-annealed 625
- The delivery condition affects strength and high-temperature response. Keep the specified condition with the component’s mechanical acceptance; 718-style aging is not the strengthening route for 625. Include liquid retained at slit edges, overlap faces and highly strained bends in the exposure description.
From drawing to documented delivery
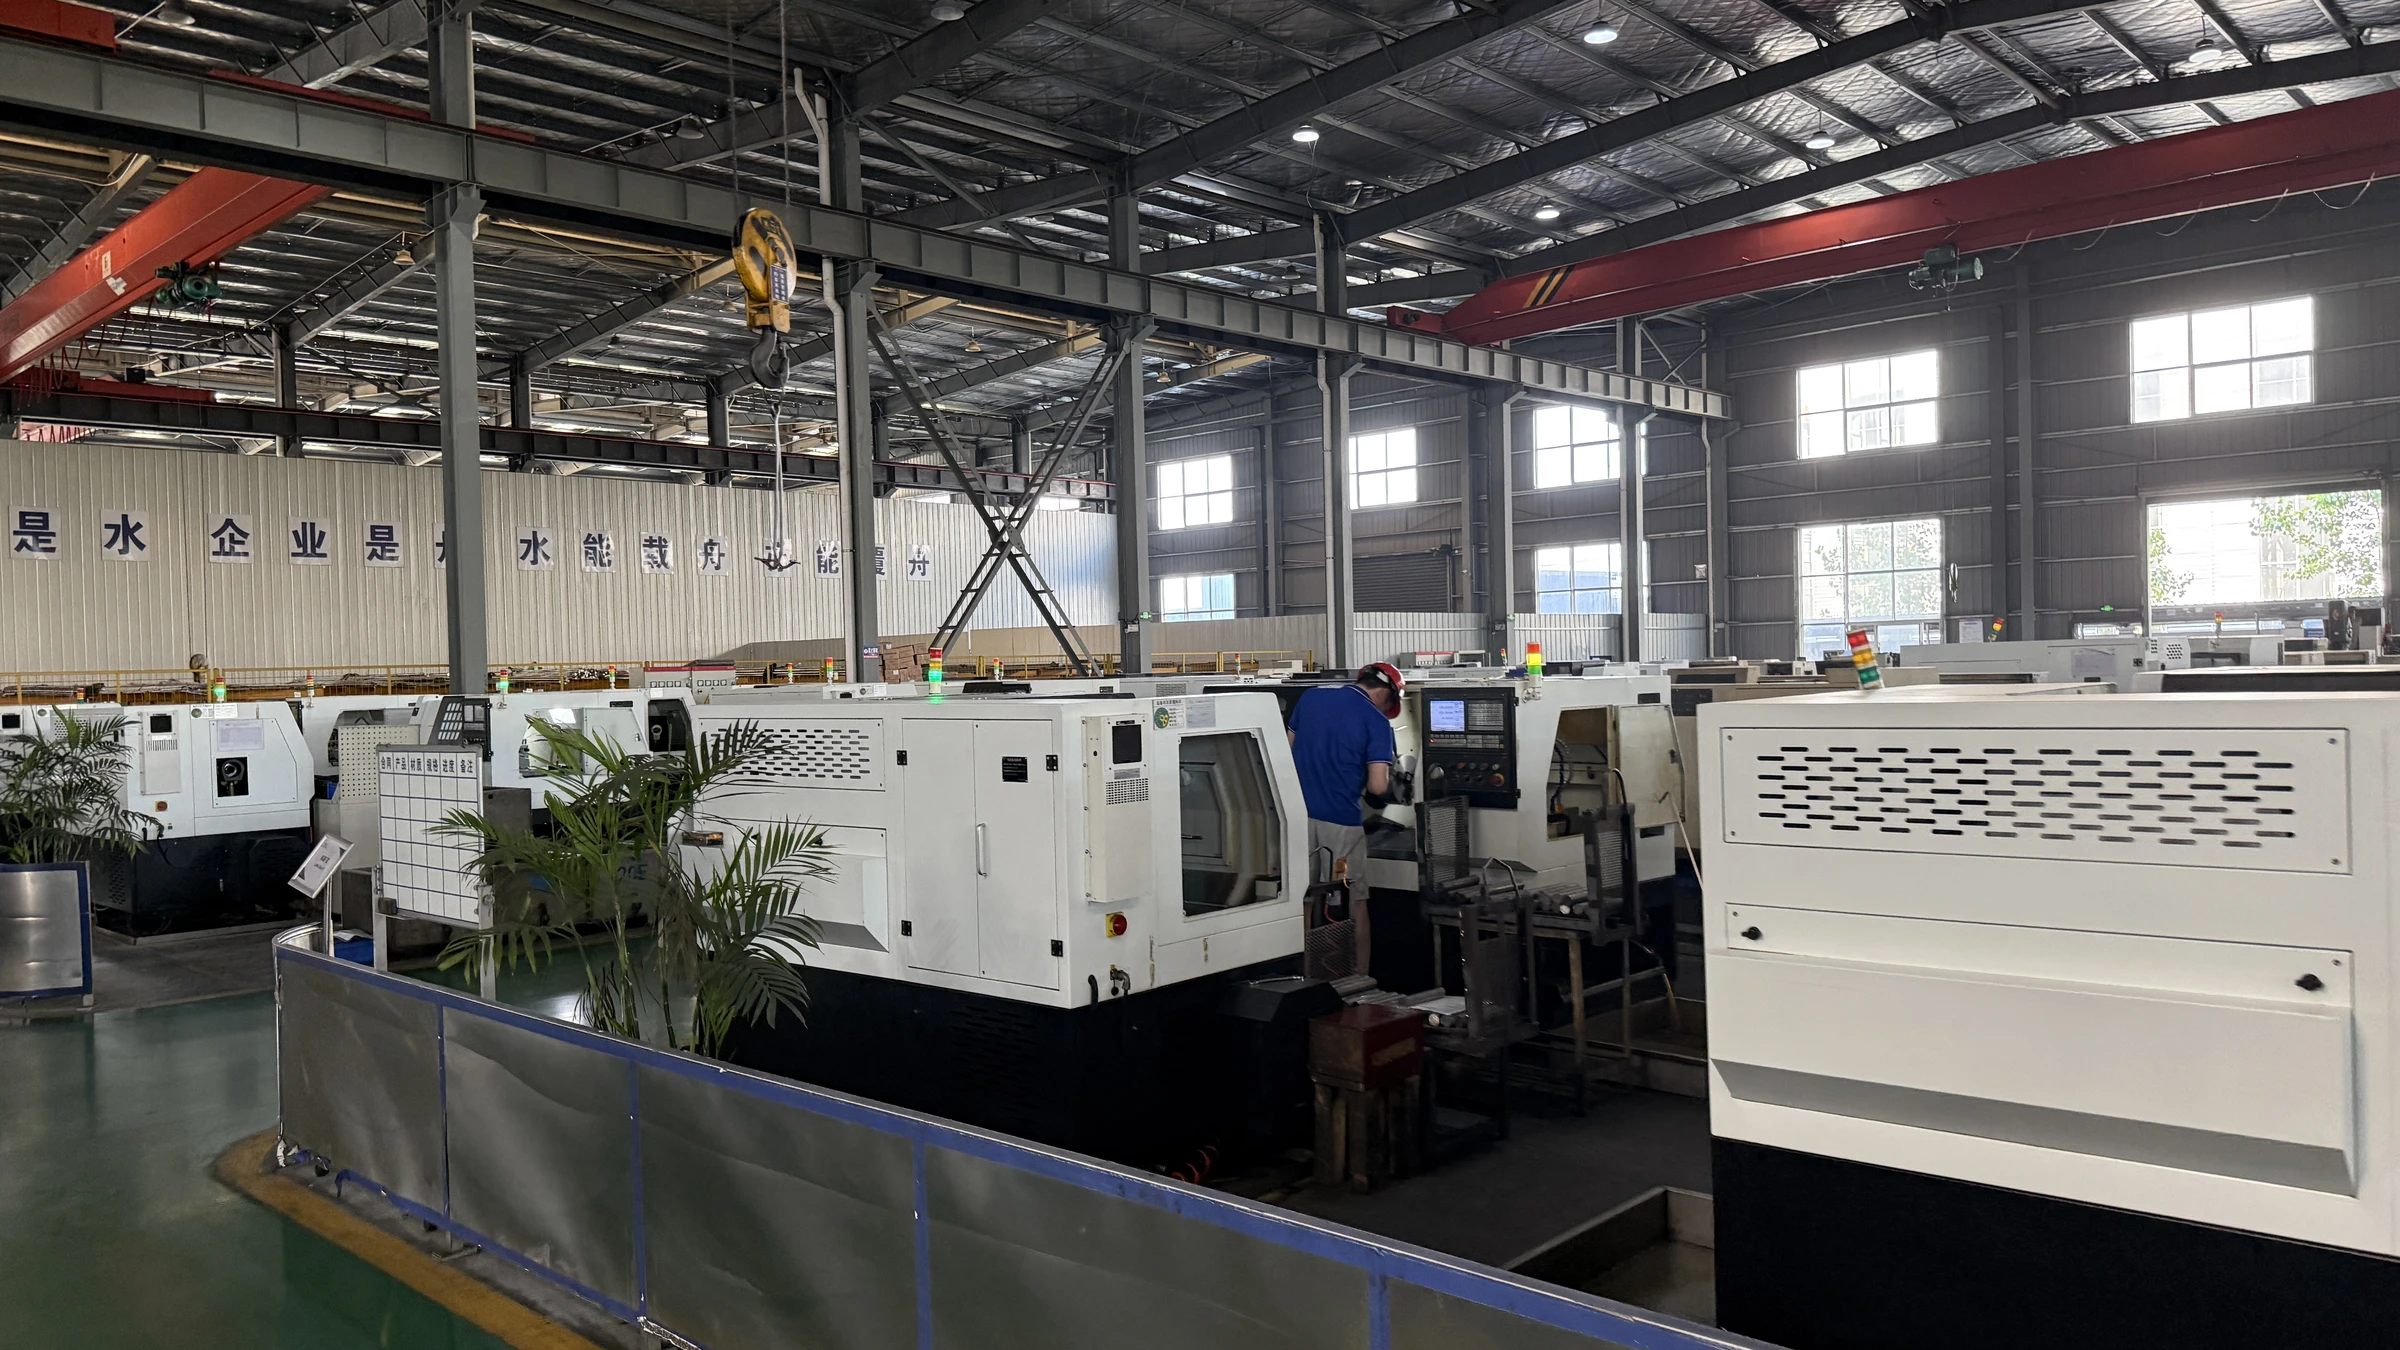
- 01Drawing & BOMForm, dimensions and quantity
- 02Material & formingGrade, heat and manufacturing route
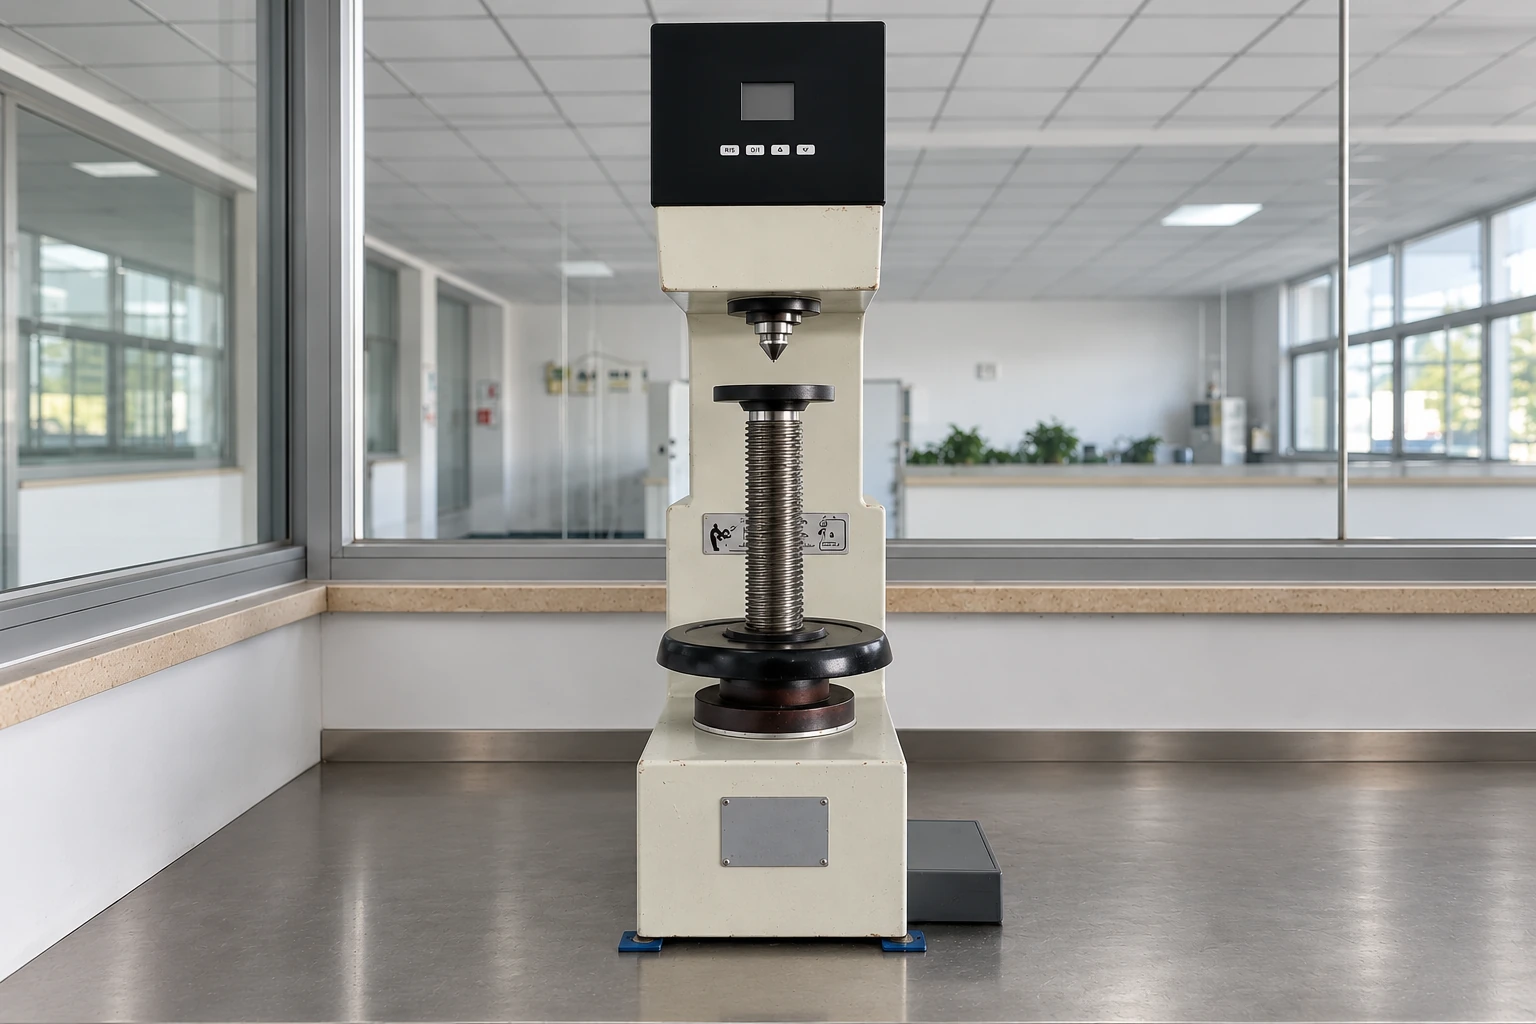
- 03Final inspectionGeometry, threads and ordered tests
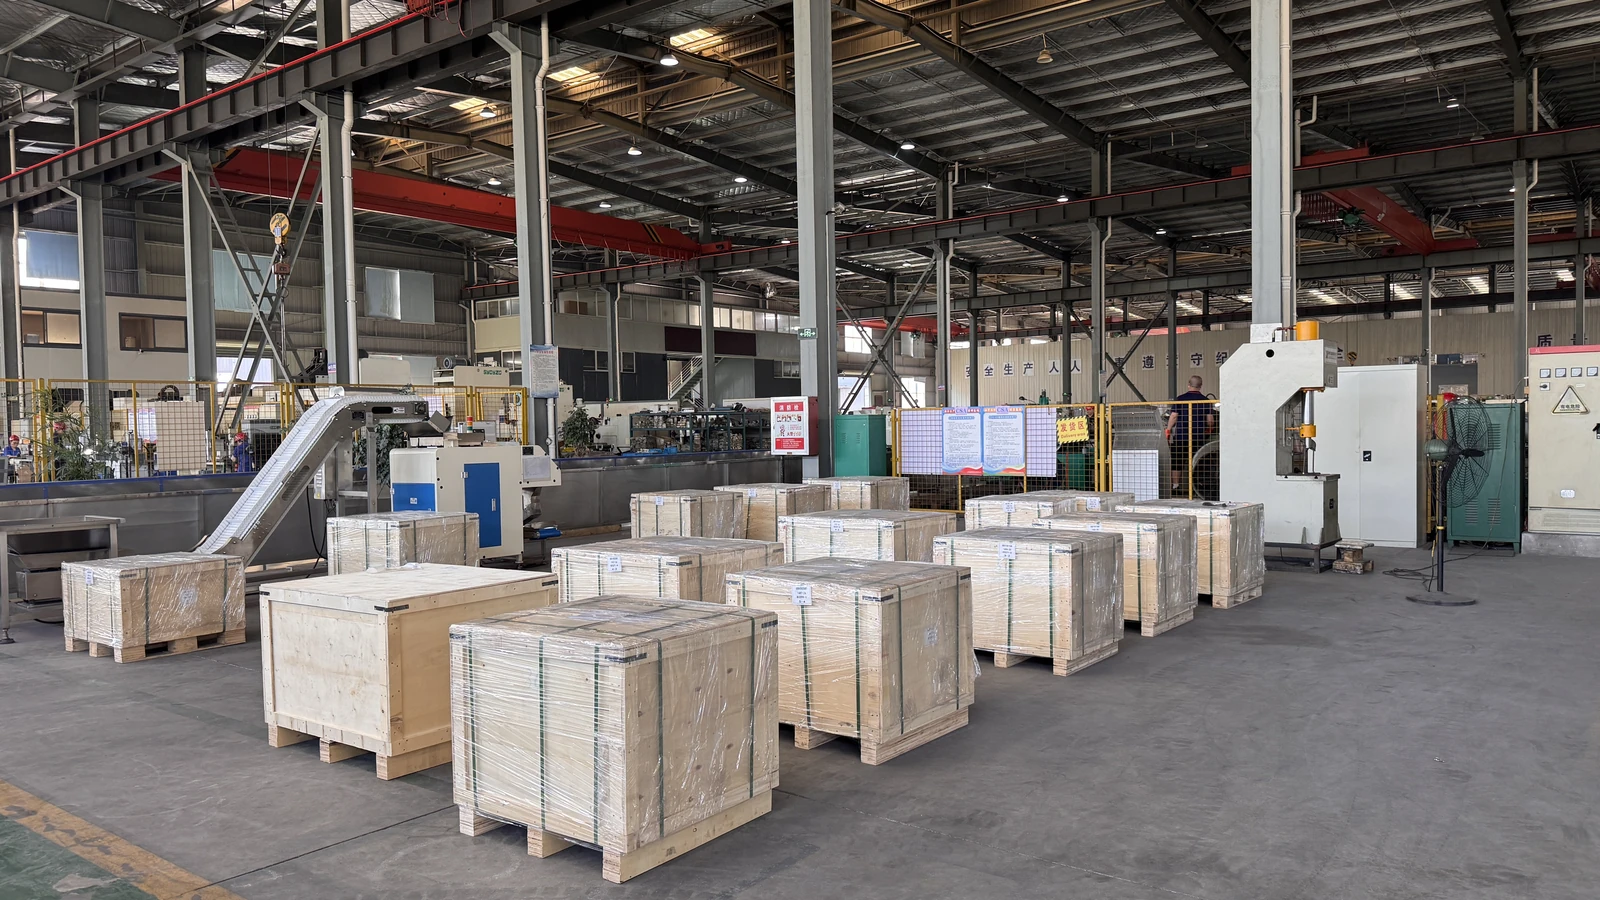
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S42000 · heat number · ordered condition
- Stock acceptance
- Hardness and mechanical acceptance after hardening and tempering.
- Dimensional record
- Cross-section · Surface · Delivery condition · Heat identity
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your 420 strip enquiry
Questions about 420 strip
Why does edge condition belong on a strip order?
A slit edge can become the most highly strained edge during forming. Burr direction, edge finish and the chosen bend radius affect the next operation and the finished contact surface.