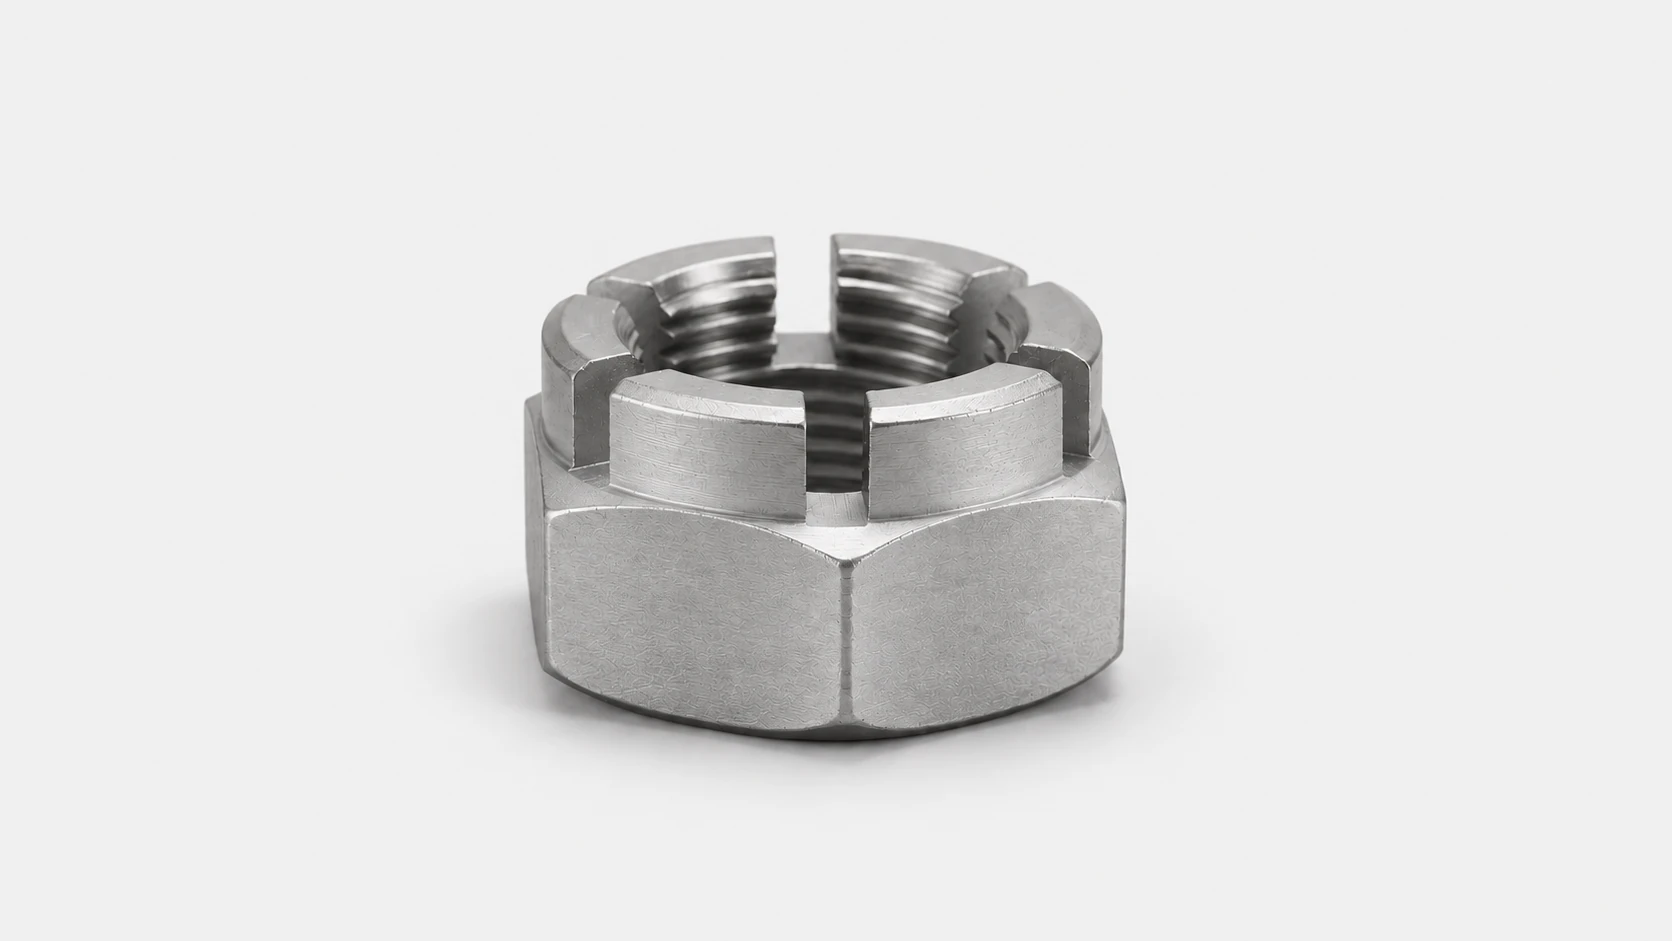
304L Slotted & castle nuts
DIN 935-1ASTM A276
304L castle and slotted nuts combine low-carbon austenitic compatibility with fabricated stainless equipment with visible pin retention. The cross-hole, pin and nut slots complete the system; the nut’s material condition governs its loaded thread.
- MOQ
- 100PCS
- Samples · typical
- ~20 days
- Production · typical
- 25–35 days
- Heat treatment
- Solution annealed
EN 10204 3.1 MTC + heat-number traceability
Which standard is on your order?
Raw Material Specifications
Threads · Metric
Threads · Inch
Dimension Reference
Heat Treatment
Solution annealed; cold worked for strengthened conditionsSolution annealing restores a ductile corrosion-resistant structure, while specified cold work raises strength without precipitation aging.
What we can make in 304L
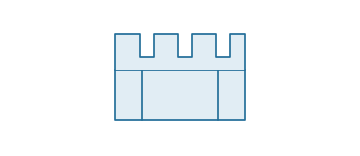
Slotted nut
Use on drilled shafts and pins where a cotter pin retains the nut after adjustment. Slots in the hex body provide a lower axial envelope when the installation has limited clearance.
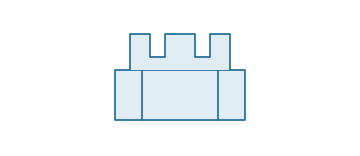
Castle nut
Use the raised slotted crown to position the cotter-pin path above the wrenching body. The crown needs clearance beyond the bearing assembly or linkage end.
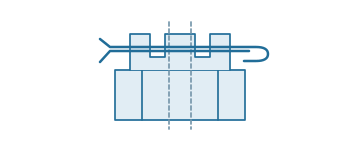
Pin alignment
For wheel, pivot and linkage assemblies, align the slots with the cross-hole using the assembly’s preload or end-play procedure. The pin retains the nut; it does not set the bearing adjustment.
- Retention
- Slots · Split pin
- Mating part
- Cross-drilled bolt or shaft
- Patterns
- Slotted · Castellated
- Threads
- Metric · Inch
- Final condition
- Solution annealed
- Inspection
- Slot width · Crown height · Pin clearance · Threads
Manufacturing route
Small lots use machined blanks. Volume nut blanks use a forming route compatible with the alloy before machining the bore and tapping.
Heat treatment & final condition
The final annealed or specified strengthened condition is linked to the lot; an aging treatment is not assumed for a solid-solution alloy.
Finished geometry
Internal thread gauging, usable engagement and bearing-face alignment are checked after final processing.
Where 304L fits — and what matters
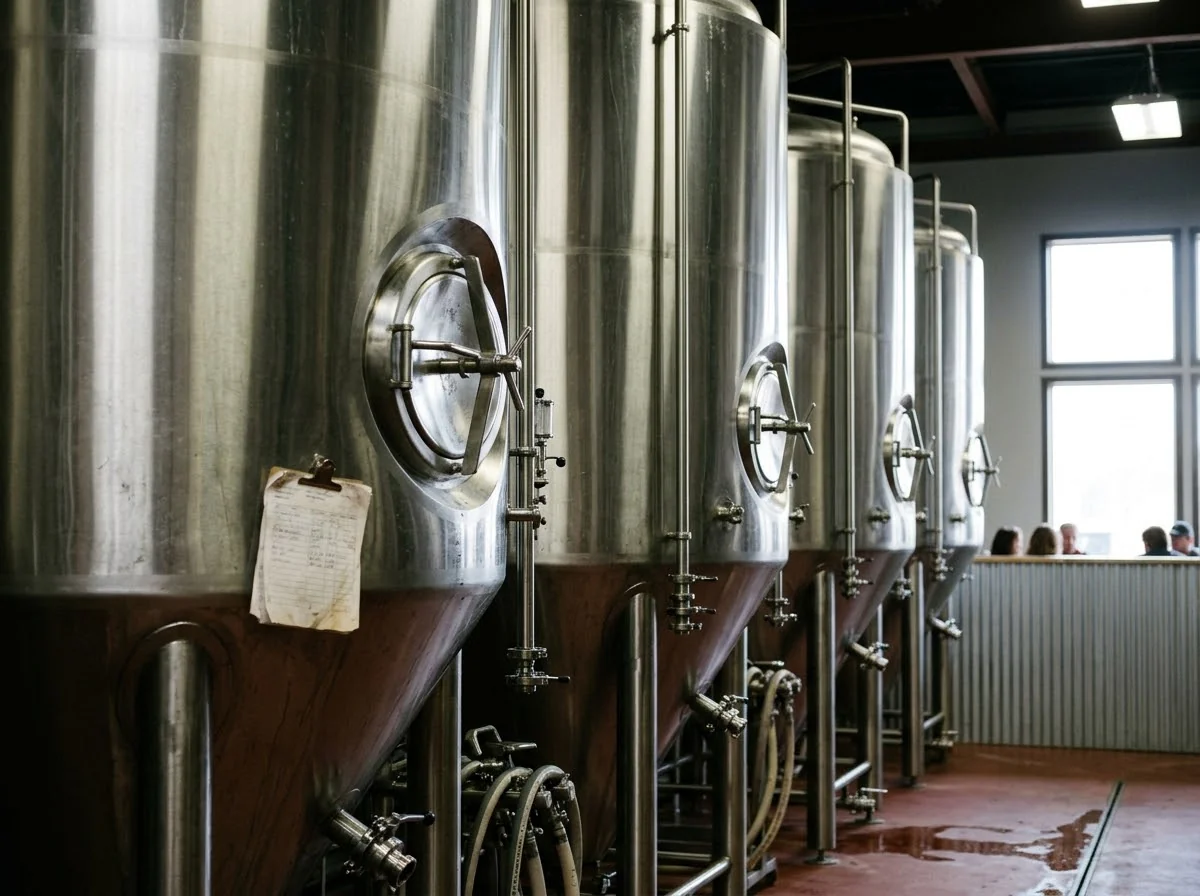
Food & Beverage Equipment
Conveyor shafts and guide components304L slotted & castle nuts retain conveyor shafts and guide components with a split pin through the nut slots and a cross-drilled shaft. Slot alignment establishes the final positive-retention position. Cleaning liquid can remain under the part; exposed finish and access for cleaning matter at the assembled joint.
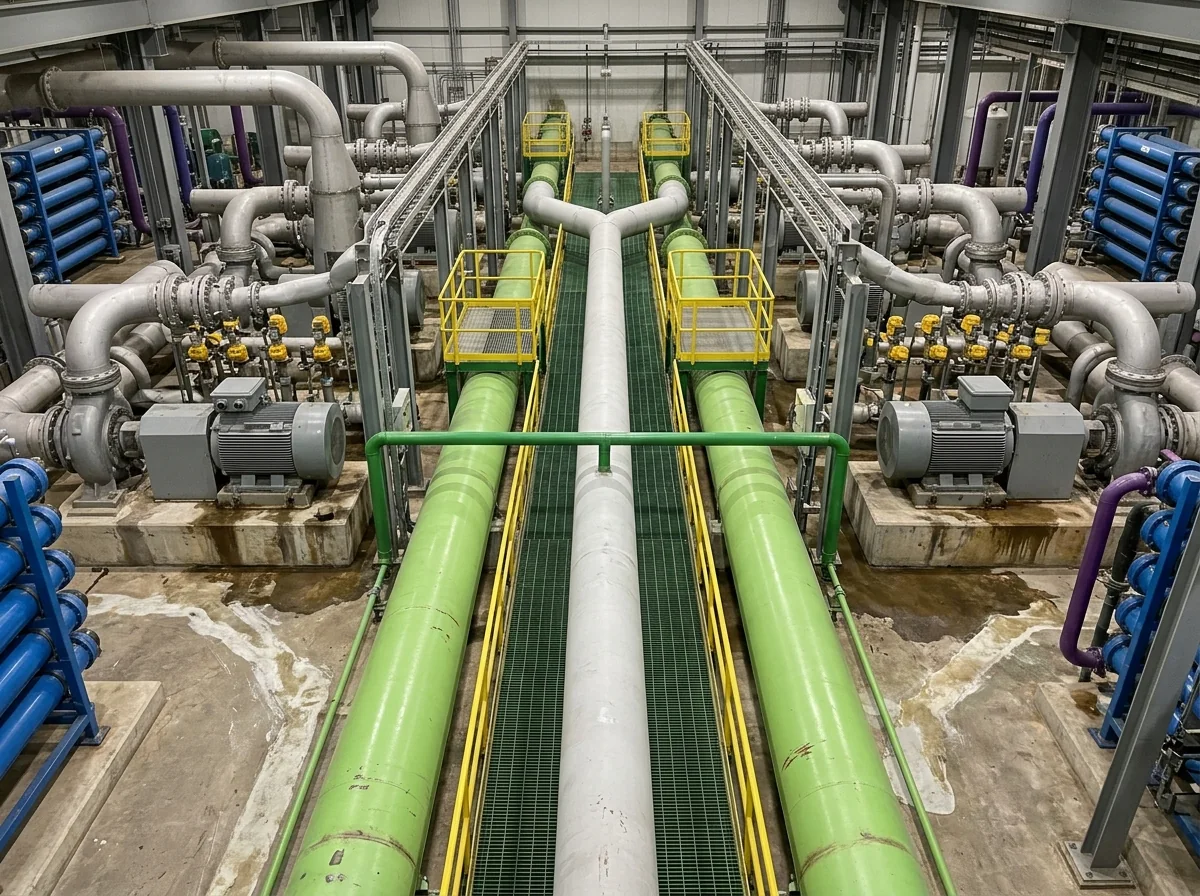
Water Treatment & Desalination
Treatment-pump shafts and actuator parts304L slotted & castle nuts retain treatment-pump shafts and actuator parts with a split pin through the nut slots and a cross-drilled shaft. Slot alignment establishes the final positive-retention position. The water stream, cleaning cycle and retained liquid define exposure at the installed part.
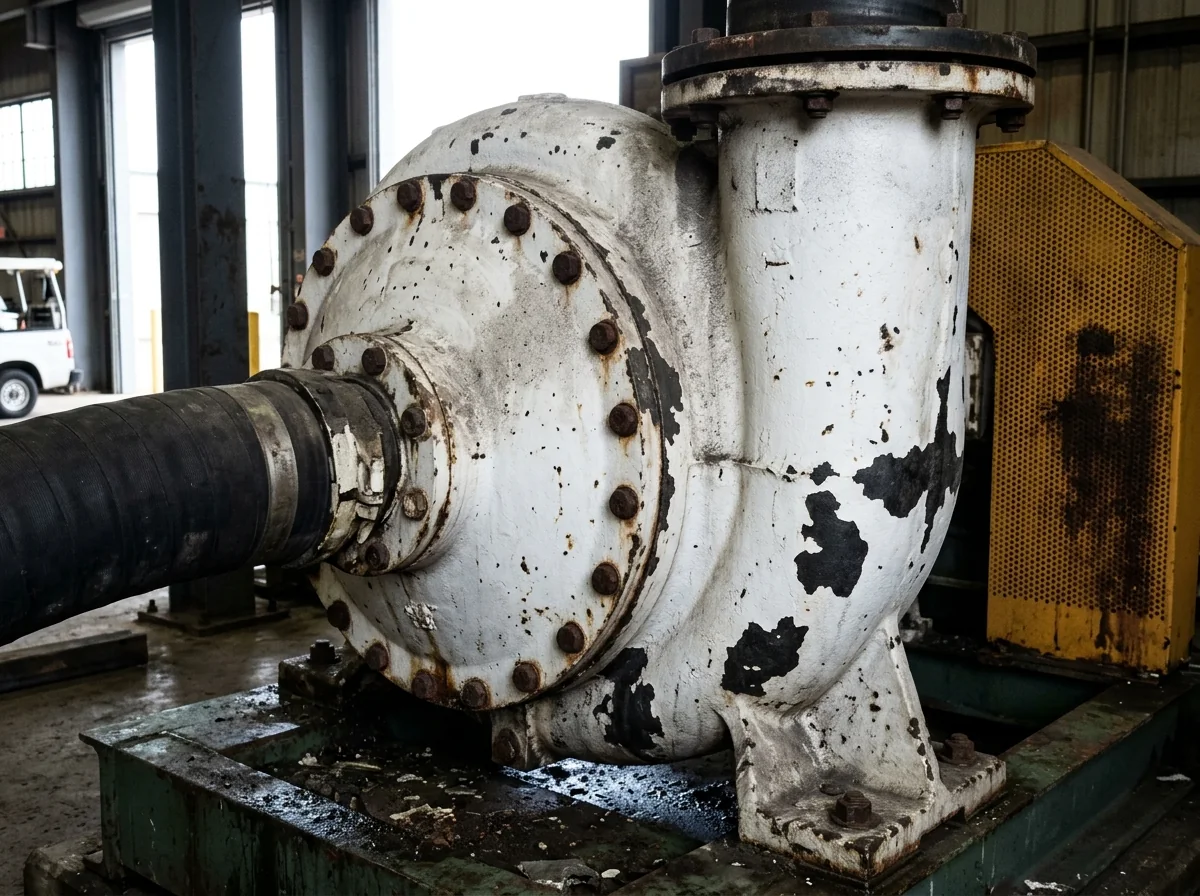
Pumps, Valves & OEM
Valve stems and pump-drive collars304L slotted & castle nuts retain valve stems and pump-drive collars with a split pin through the nut slots and a cross-drilled shaft. Slot alignment establishes the final positive-retention position. Repeated maintenance makes fit, engagement and access part of the component specification.
Same slotted & castle nut. Different material priorities.
304L material data316L
Molybdenum-bearing stainless performance in wet equipment.
- Connection priority
- Nut preload with separate positive pin retention
- Washdown and retained cleaner
- Cleaner concentration, rinse quality and deposits determine the exposure in covered joints. The low-carbon designation does not independently establish a fastener strength class. Include liquid retained at the pin slots, cross-drilled shaft and bearing face in the exposure description.
17-4 PH
Aging-controlled strength and hardness.
- Connection priority
- Nut preload with separate positive pin retention
- H900 versus H1150
- The aging condition changes the balance of strength, hardness and toughness. A replacement part needs the specified H condition, especially where contact wear and shock load occur together.
Inconel 625
Solid-solution strength and resistance to aggressive process liquids.
- Connection priority
- Nut preload with separate positive pin retention
- Annealed or solution-annealed 625
- The delivery condition affects strength and high-temperature response. Keep the specified condition with the component’s mechanical acceptance; 718-style aging is not the strengthening route for 625. Include liquid retained at the pin slots, cross-drilled shaft and bearing face in the exposure description.
From drawing to documented delivery
- 01Drawing & BOMForm, dimensions and quantity
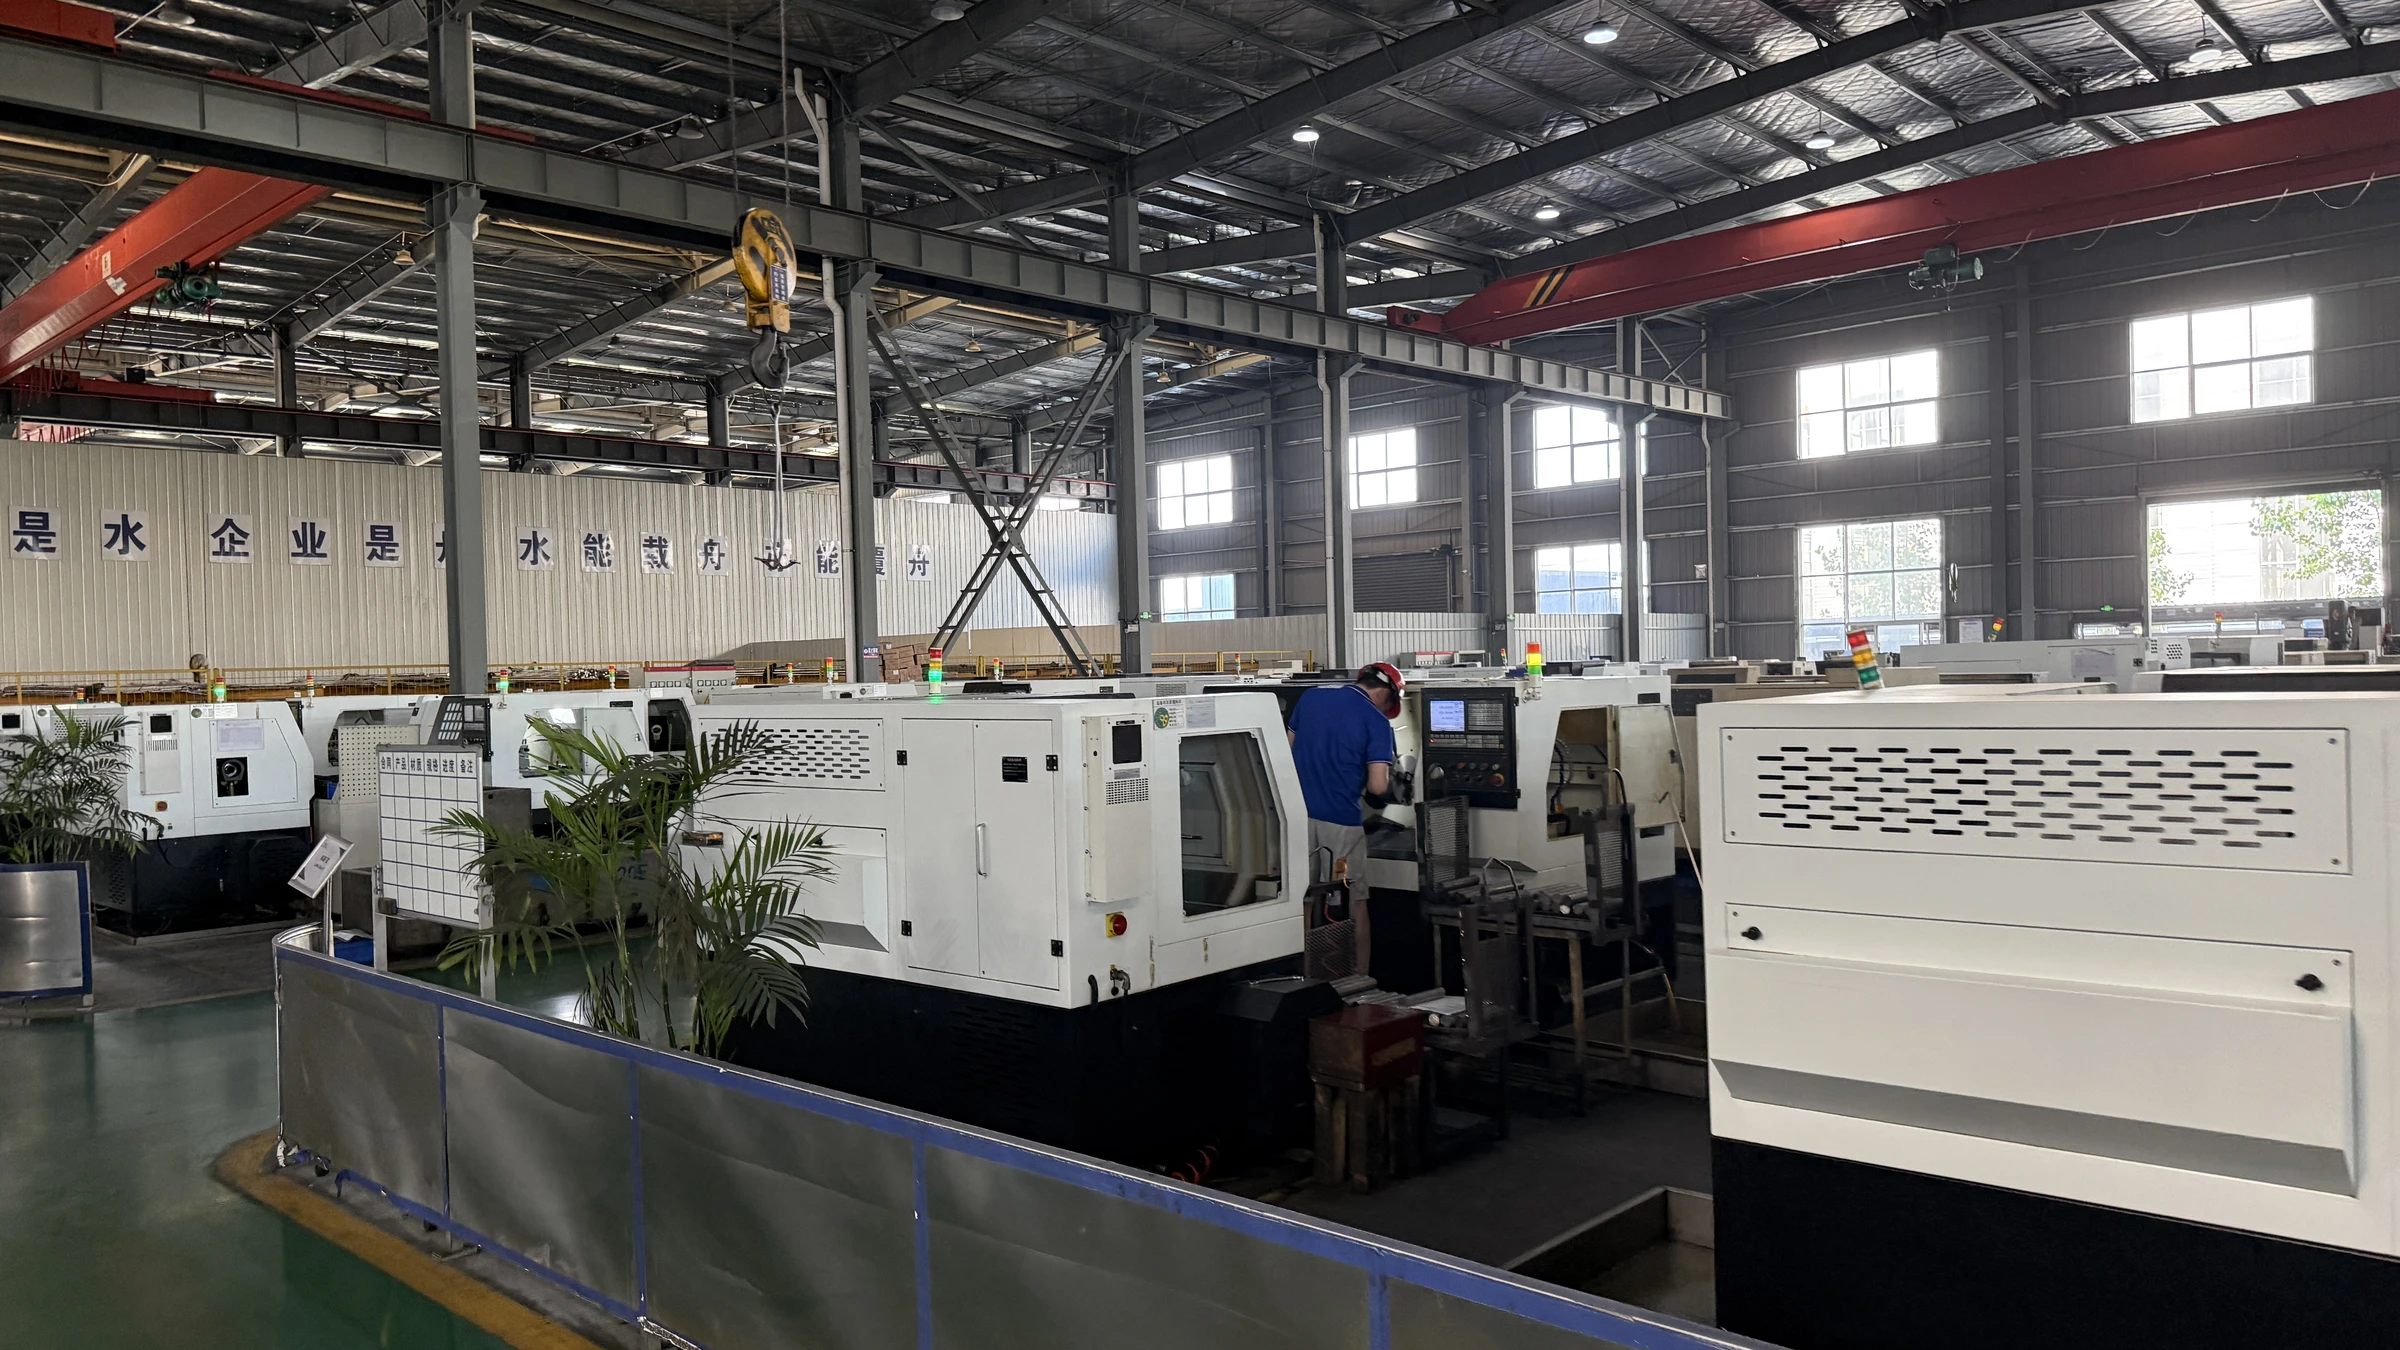
- 02Material & formingGrade, heat and manufacturing route
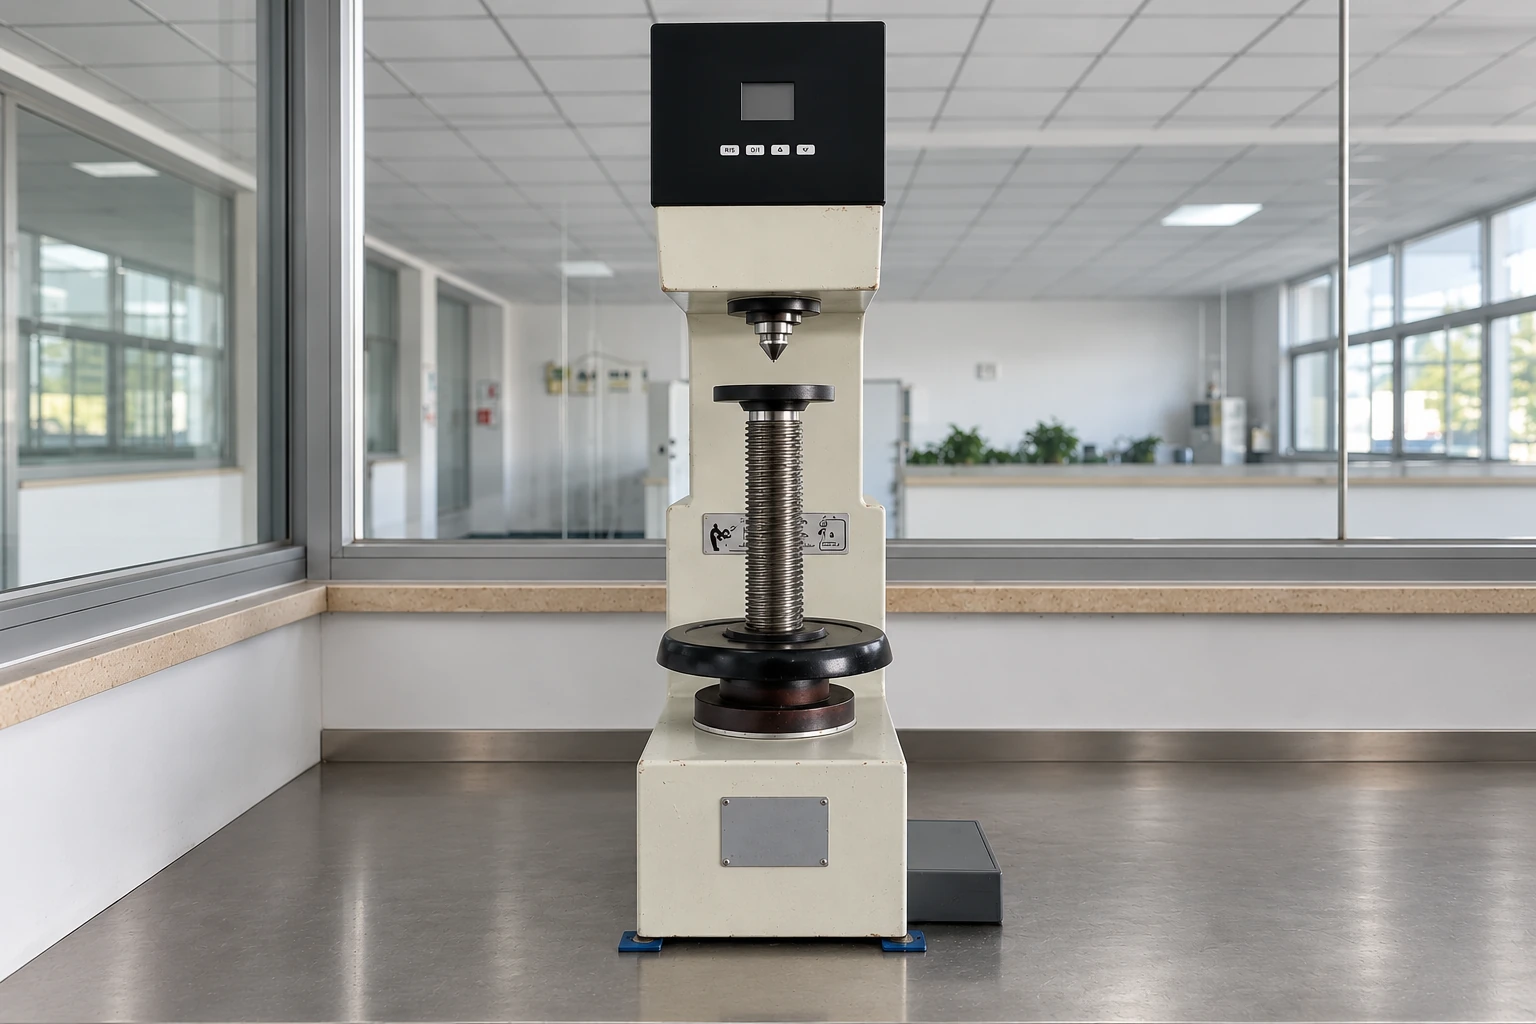
- 03Final inspectionGeometry, threads and ordered tests
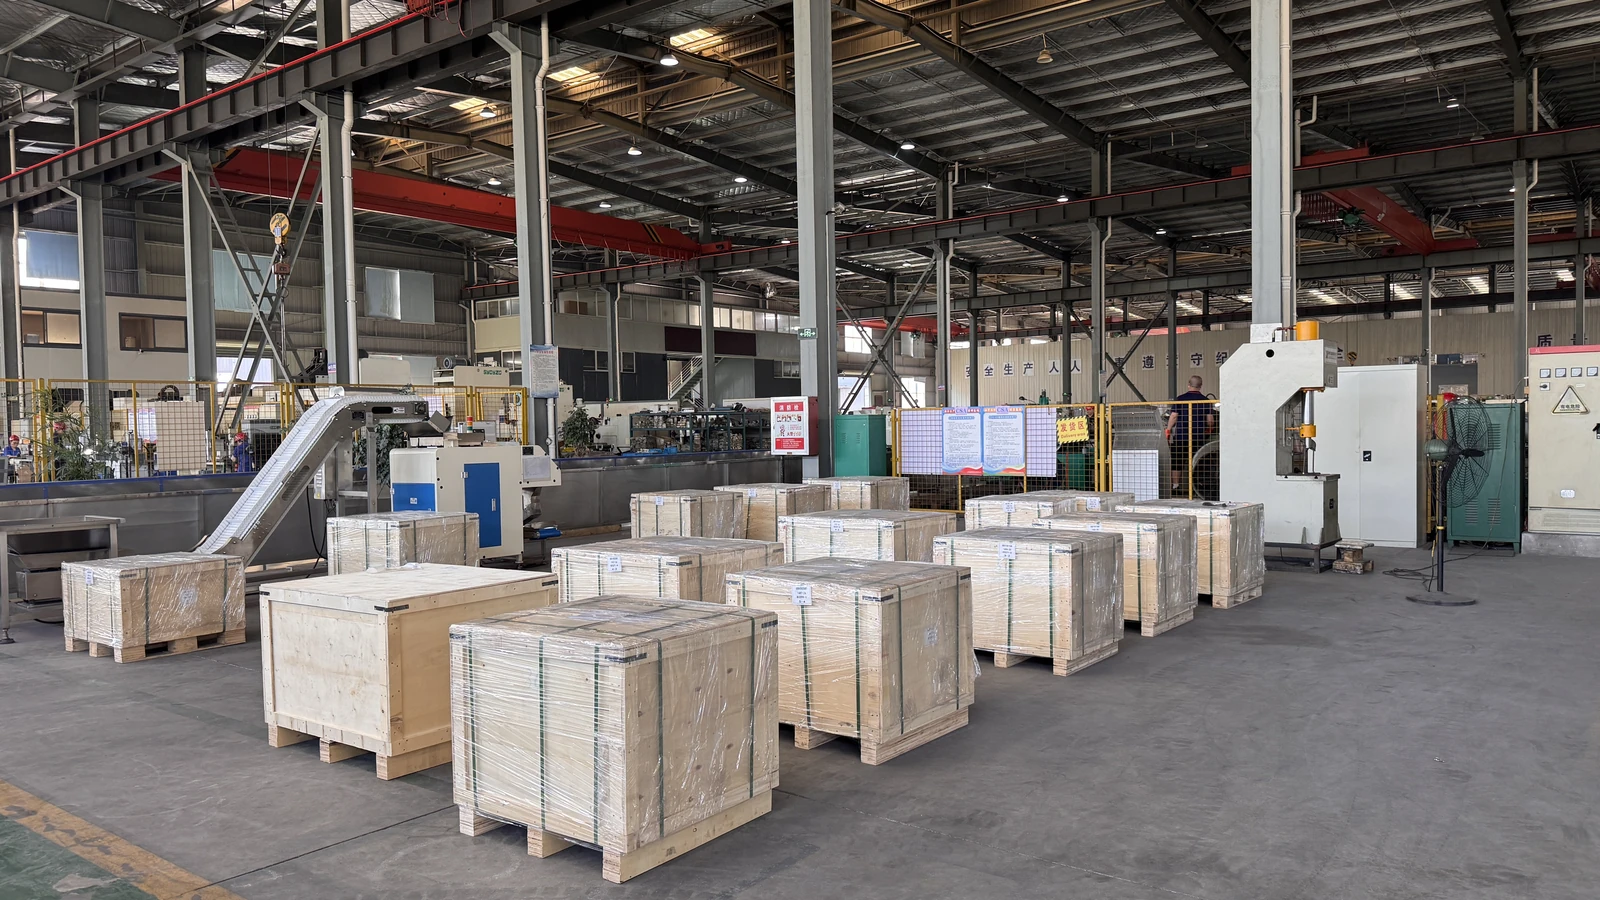
- 04Documents & dispatchLot records and identified packing
Order documents
- Material identity
- UNS S30403 · heat number · ordered condition
- Final-part acceptance
- Grade chemistry, supplied condition and ordered mechanical requirements.
- Dimensional record
- Slot width · Crown height · Pin clearance · Threads
- Traceability
- EN 10204 3.1 material certificate · production lot · identified packing
Build your 304L slotted & castle nut enquiry
Questions about 304L slotted & castle nuts
What must be specified with a castle nut?
The cross-drilled shaft, retaining pin material and slot geometry complete the retention system. Slot alignment follows the assembly tightening procedure; the pin does not generate the joint’s clamp load.