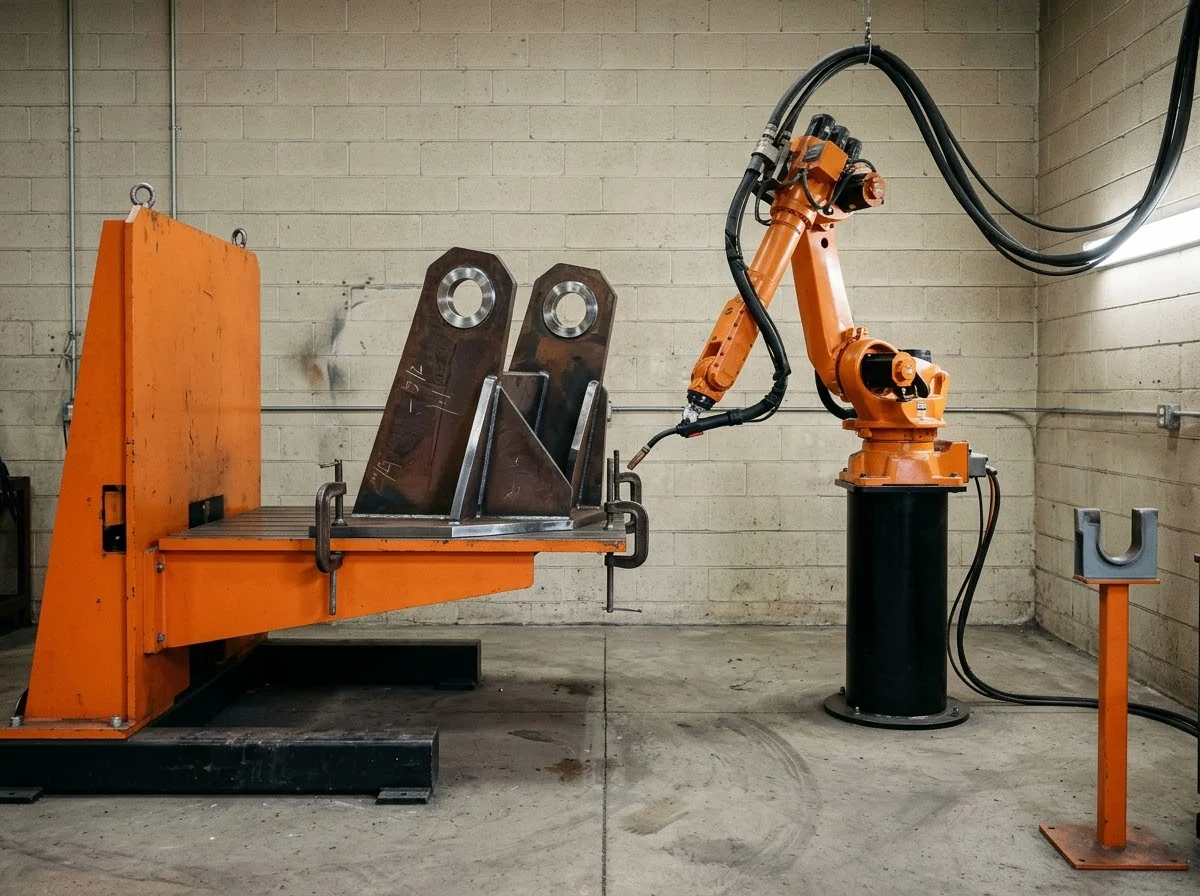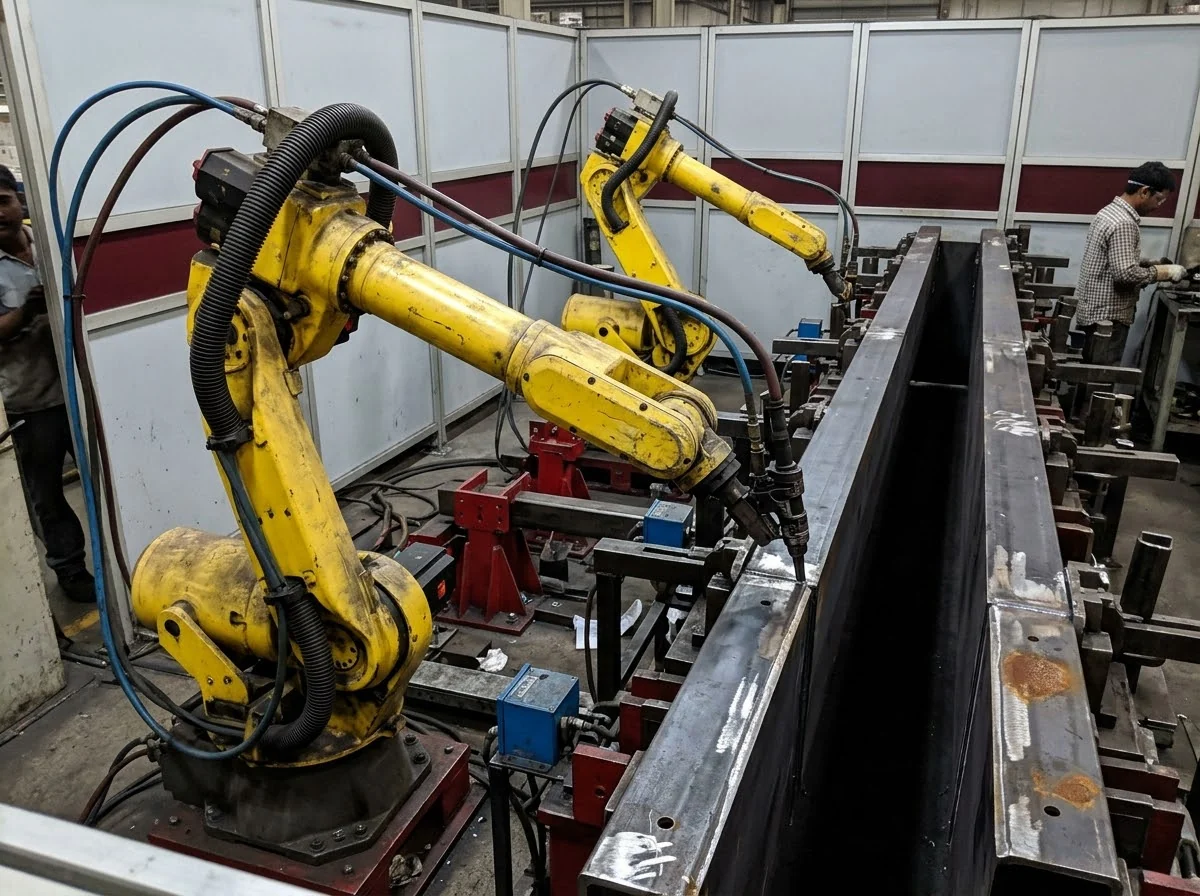
Special alloy fasteners for Automotive & EV Manufacturing Equipment.
Heat-resistant fixture bolts, precision locating hardware and washdown screws for production machinery and test rigs.
Which fasteners fit your production line or test rig?
BYBOLT supplies Inconel 601 hex bolts to resist scaling on heat-treatment fixtures, 17-4 PH positioning bolts for repeatable assembly-tool location and 316L socket head screws for washed production equipment. Inconel 718 stud bolts add high strength to loaded thermal-test rigs. Supply your tooling or equipment drawing to quote the complete fastener set.
Fasteners for EV & automotive equipment.
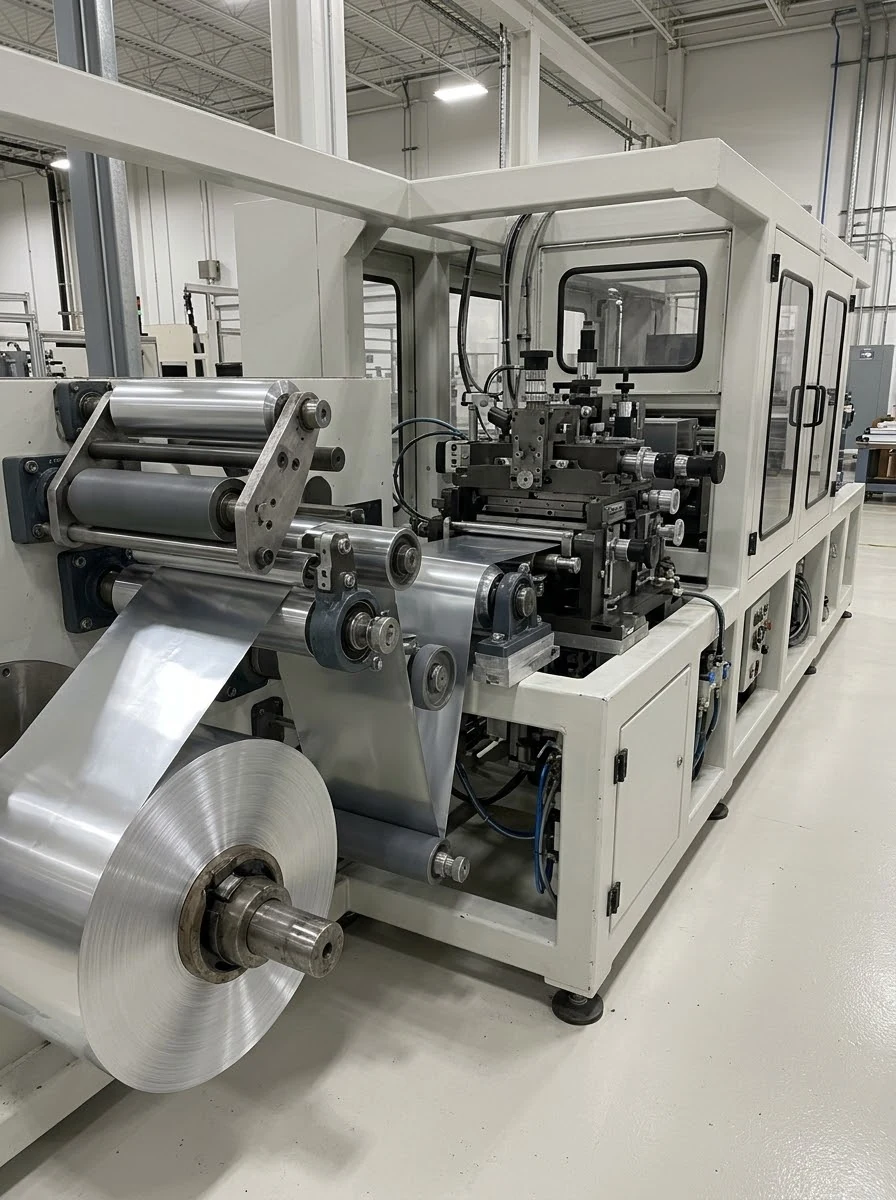
Electrode slurry mixers & coaters
C-276 socket screws offer corrosion resistance for compatible mixer and coater process-contact joints. Select them against the actual slurry and cleaning chemistry; abrasive wear and alignment need separate mechanical design checks.
C-276 cleanroom socket screwsConnection requirements
- Socket recess depth
- Flange face flatness
- Assembly torque sequence
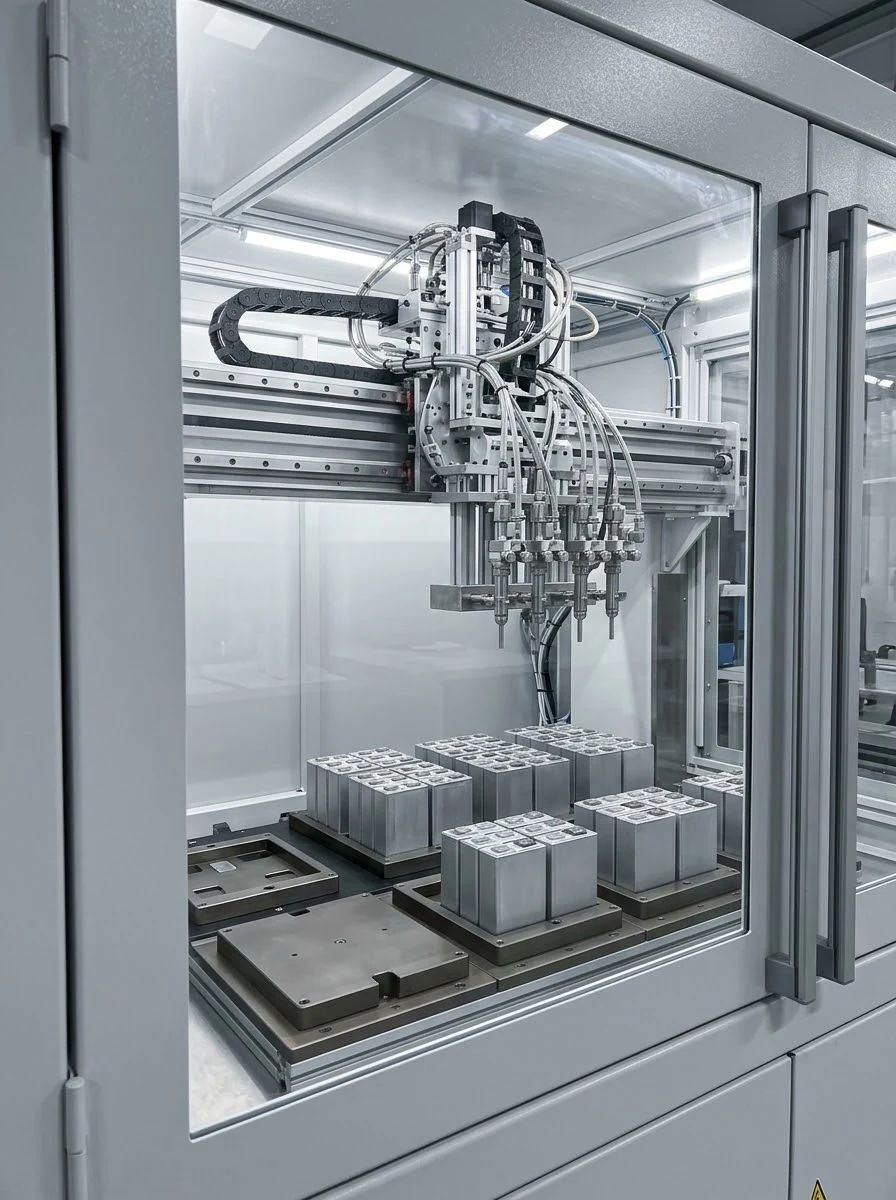
Electrolyte filling & formation stations
Titanium Grade 2 studs can serve compatible external filling-station fixtures where low weight and material cleanliness matter. Keep them out of HF-exposed electrolyte joints; select wetted hardware against the actual electrolyte and fluoride chemistry.
Titanium Gr.2 stud boltsConnection requirements
- Stud thread pitch
- Manifold port alignment
- Seal groove depth
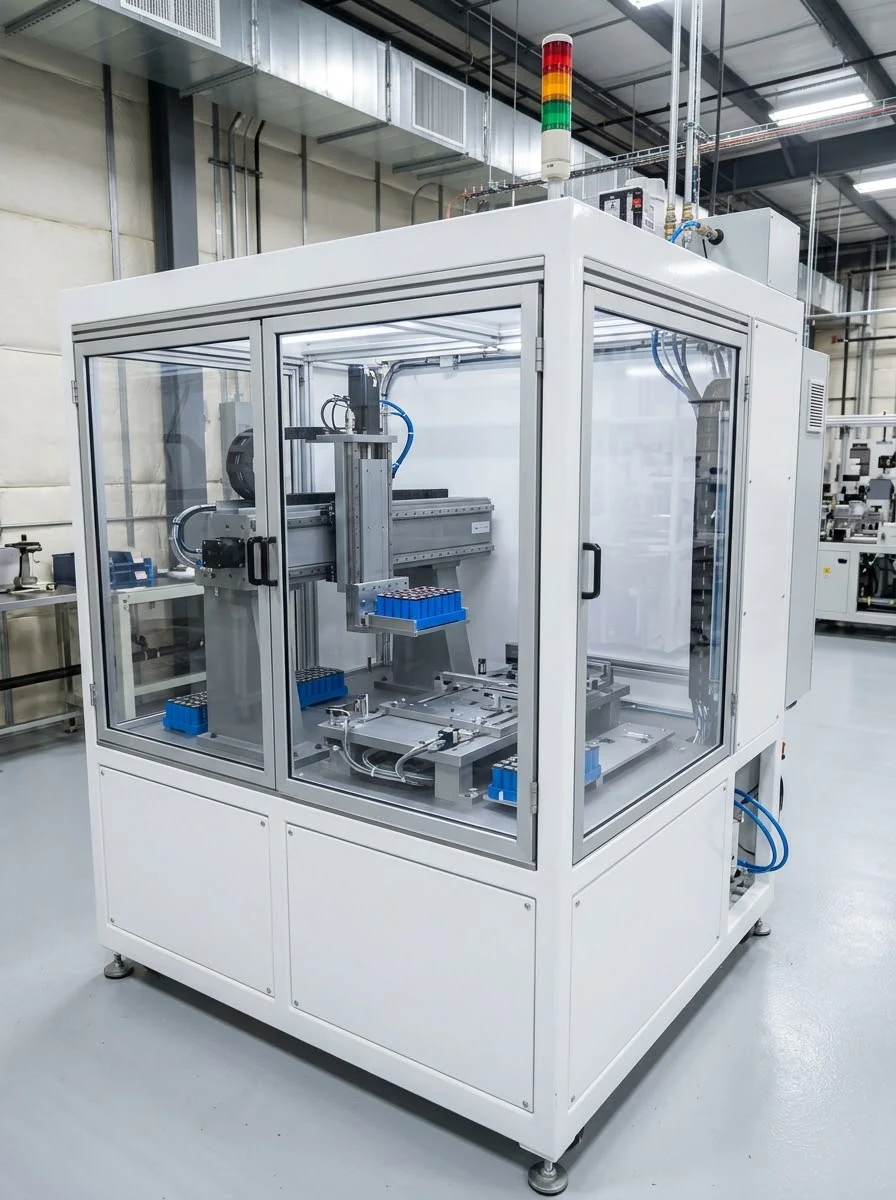
Dry-room cell assembly & handling gantries
Gantry travel and repeated cell handling cycles load fasteners through vibration, start-stop motion, and positional shifting. Cleanroom-bagged 316L socket screws maintain clamped alignment while meeting strict cleanliness rules for dry-room assembly work.
Cleanroom-bagged 316L socket screwsRelated material guides
Connection requirements
- Gantry rail alignment tolerance
- Socket screw engagement length
- Cleanroom bagging specification
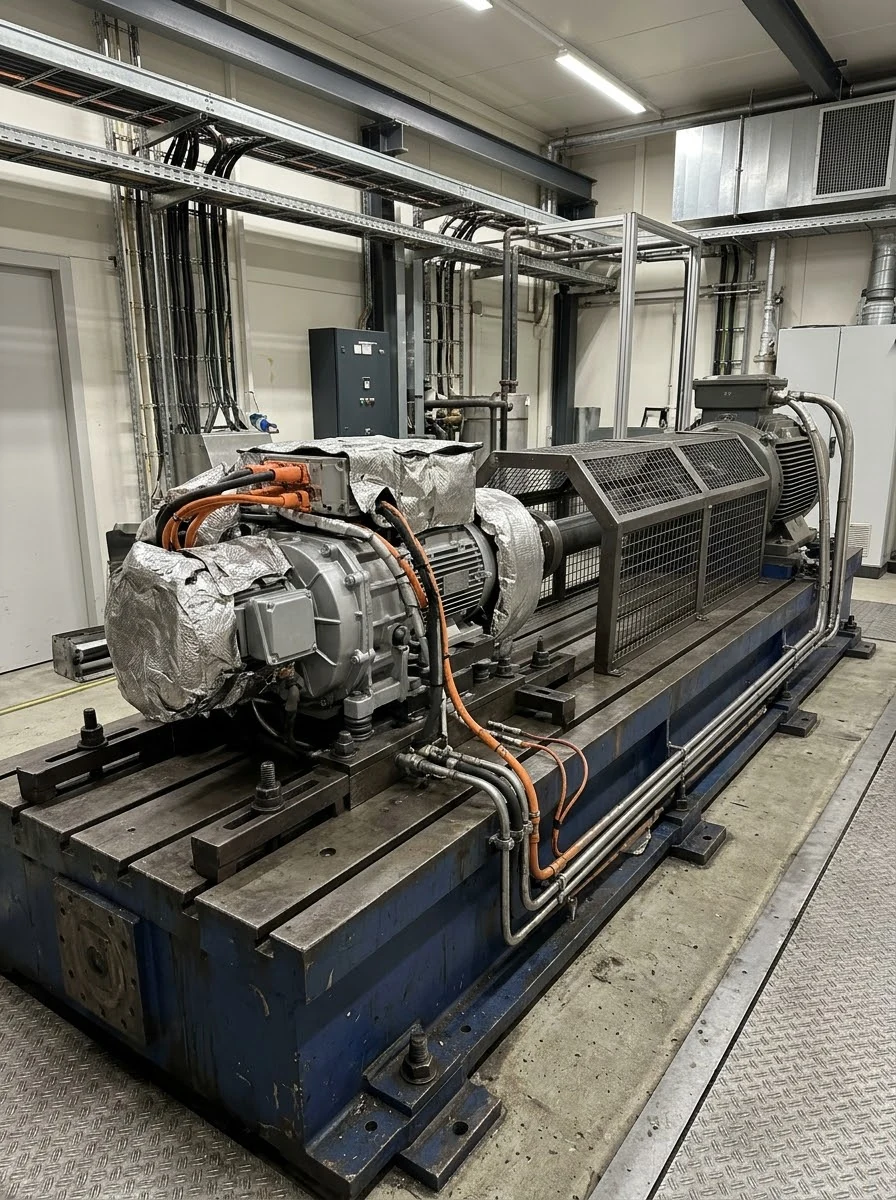
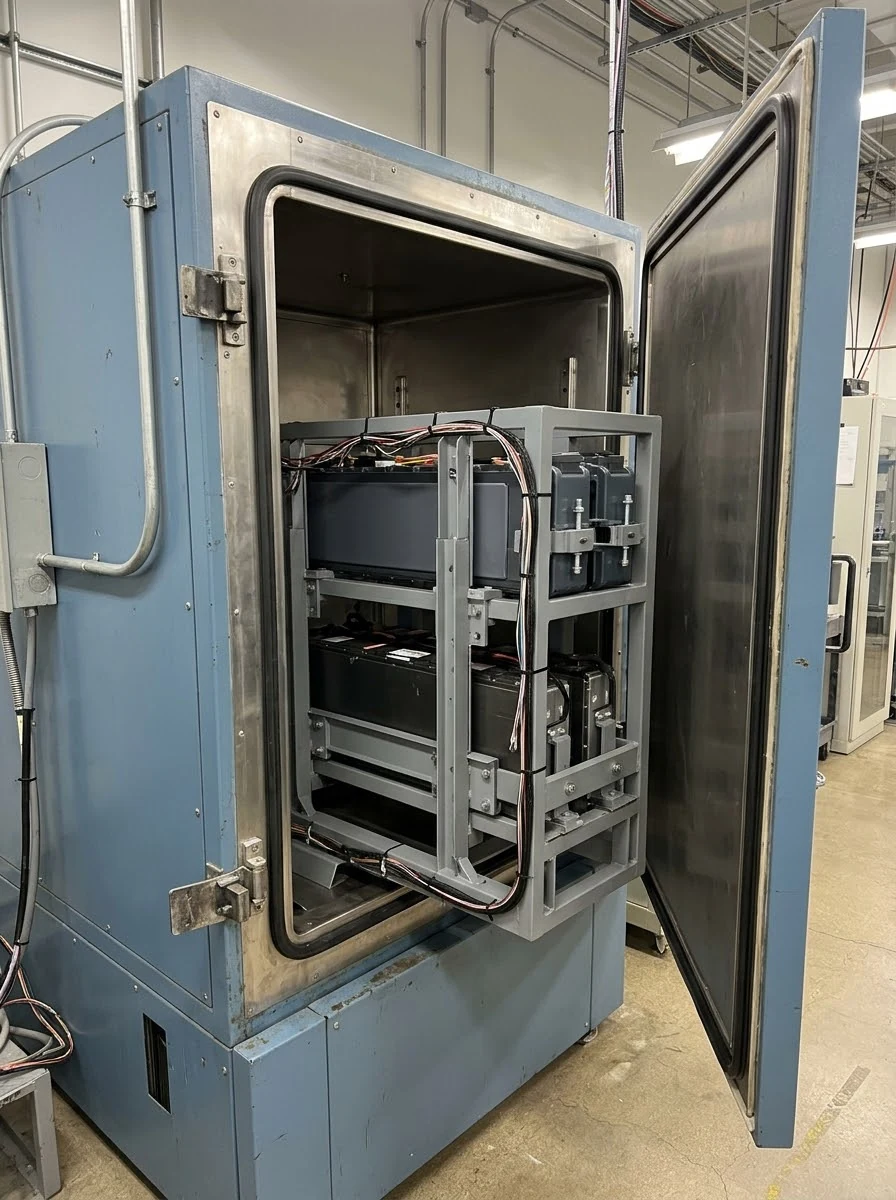
Heated powertrain & battery test rigs
Heated test fixtures expose their mounting screws to both fixture loads and repeated heating cycles. Inconel 718 provides precipitation-hardened strength for these compact joints. The socket head lets technicians reach recessed mounting positions without removing surrounding test hardware, which is often the practical reason to choose this screw form.
Inconel 718 Socket Head Cap ScrewsConnection requirements
- Tapped-hole size, thread form, and effective engagement depth
- Head diameter, head height, and socket depth for drive engagement
- Temperature range, cycling duty, and age-hardened condition certification
Gear & shaft heat-treatment fixtures
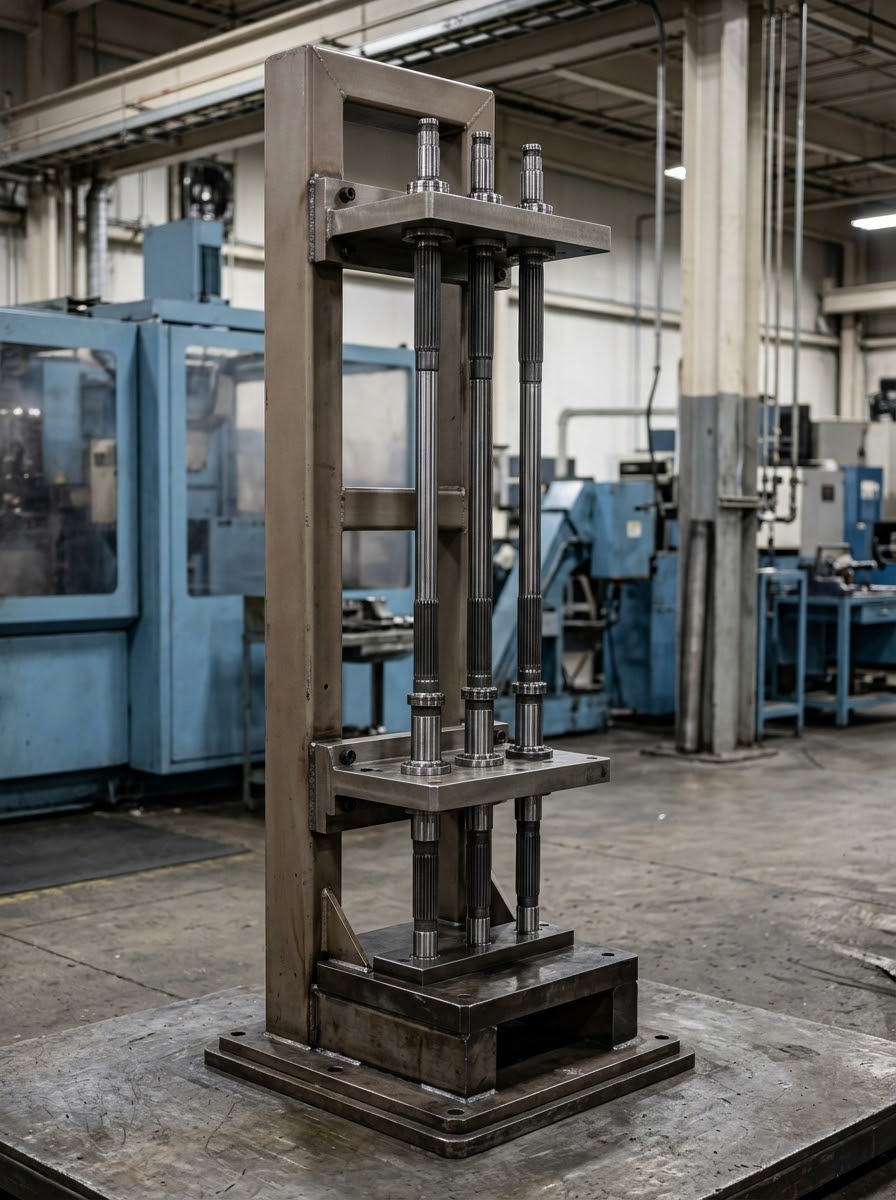
A-286 socket screws can secure fixture blocks and locating hardware where heat-treatment tooling leaves only axial access to the fastener. Their elevated-temperature strength is useful in loaded fixtures. The actual furnace cycle matters, since a fixture repeatedly exposed to a heat-treatment temperature may change the condition of its own fasteners.
A-286 Socket Head Cap ScrewsConnection requirements
- Tapped-hole size, thread form, and effective engagement depth
- Head diameter, head height, and socket depth for drive engagement
- Temperature range, cycling duty, and precipitation-hardened condition certification
E-coat & body surface-treatment lines
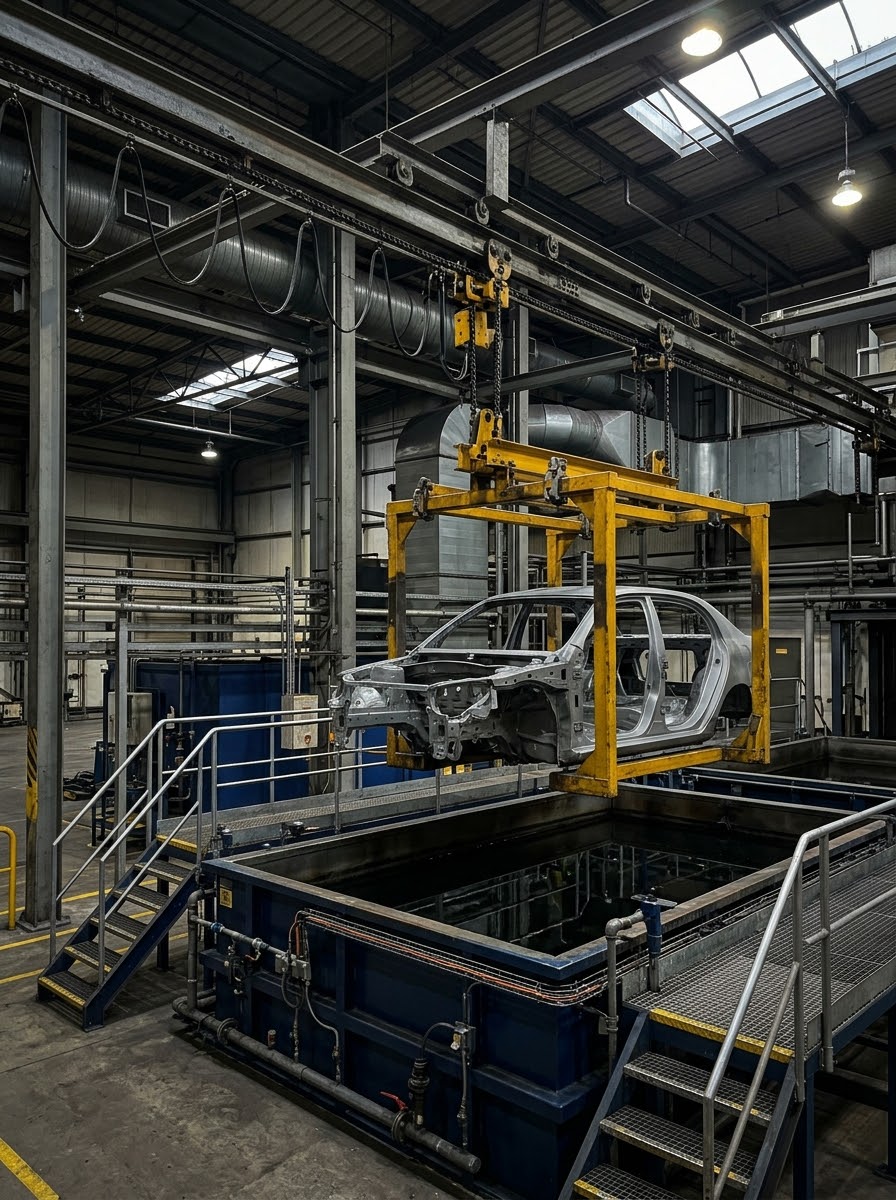
Duplex 2205 hex flange bolts anchor hangers and carriers through e-coat baths and rinse stages. Their strength and corrosion resistance support heavy body panels while resisting process chemicals and repeated immersion cycles.
Duplex 2205 hex flange boltsConnection requirements
- Flange bolt hole spacing
- Carrier hanger load position
- Coating clearance allowance
Abrasion, cleanliness, and heat.
Electrode slurry brings abrasion, while electrolyte moisture can create HF; these are different exposure problems. Select mixer and filling-line hardware against the actual formulation and contact zone. C-276 or duplex names alone do not establish HF compatibility or wear life.
What to specify
- Slurry abrasion rate
- NMP exposure duration
- Trace HF concentration
Battery-line hardware needs particle and residue limits set by the production process. Cleaned 316L and titanium serve different fixture duties; bagging preserves cleanliness but does not prove acceptance. Define restricted contaminants and the inspection method for each contact zone.
What to specify
- Surface cleanliness level
- Particle count per area
- Ionic contamination level
A-286 and 718 provide strength options for heated test-rig joints, selected by bolt temperature, dwell time and relaxation data. RA330 and 601 address furnace-fixture duties where thermal cycling and oxidation govern the fastener choice.
What to specify
- Relaxation rate
- Thermal cycle count
- Operating temperature range
Compare EV & thermal equipment alloys.
| Material grade | Mechanical Duty / Focus | Environment | Relative cost | Popular fastener forms |
|---|---|---|---|---|
| Inconel 601UNS N06601Oxidation resistance |
| Oxidizing production-furnace atmospheres | $$$ | 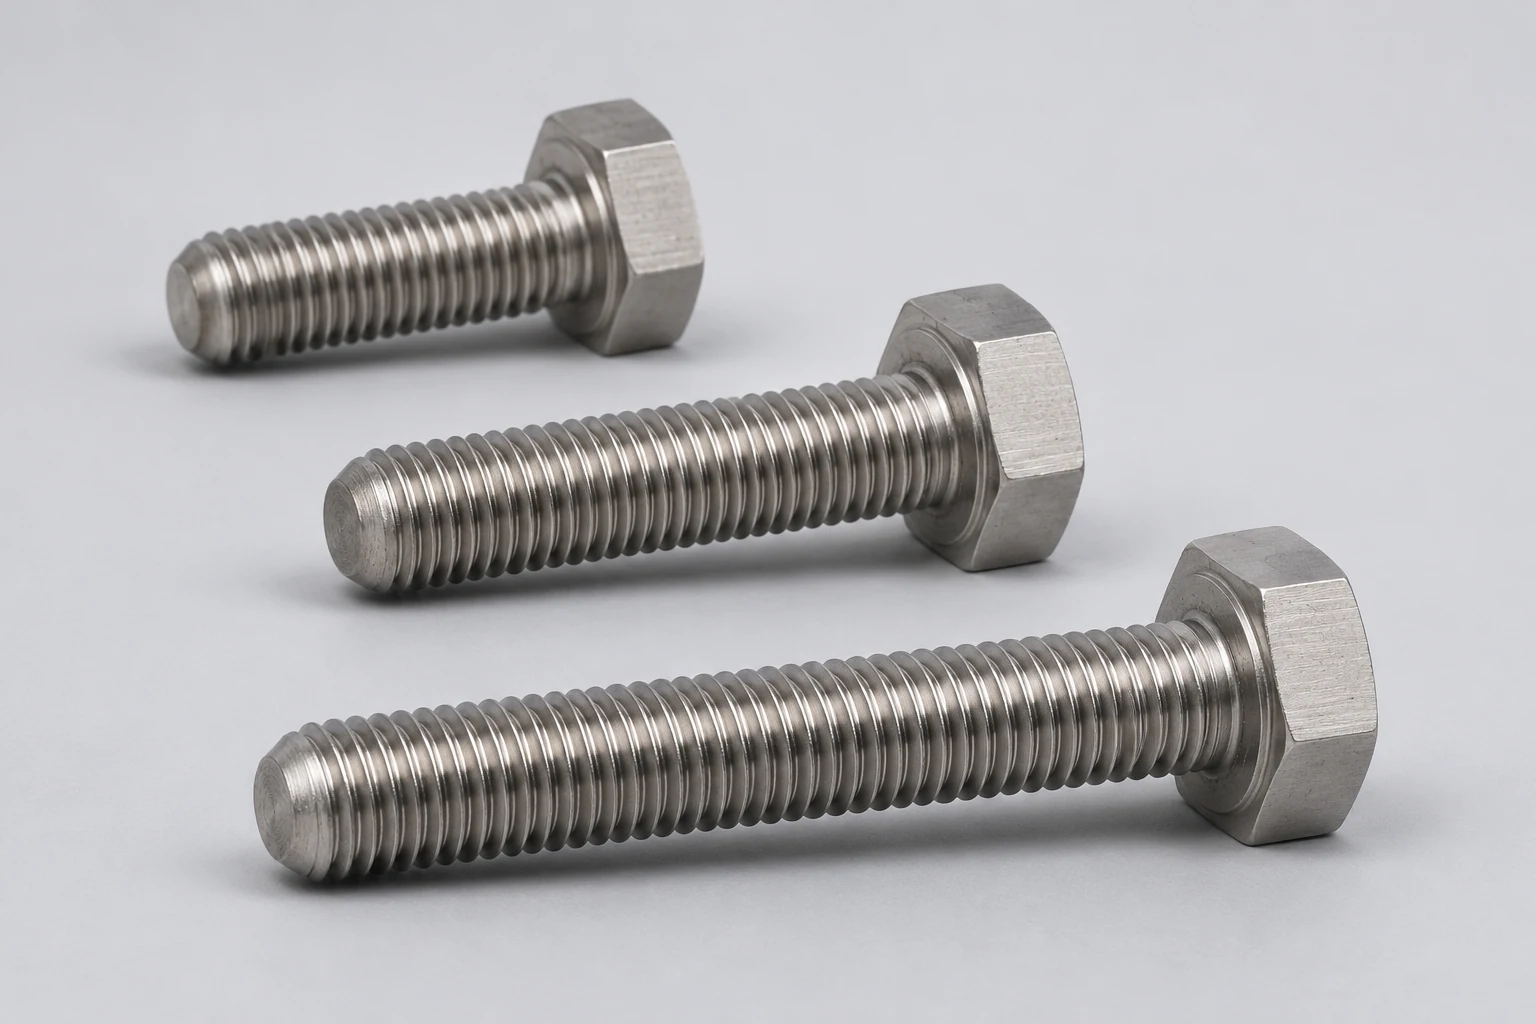 Hex bolts |
| 17-4 PHUNS S17400Precipitation hardened |
| Dry assembly tooling and precision locating interfaces | $$ | 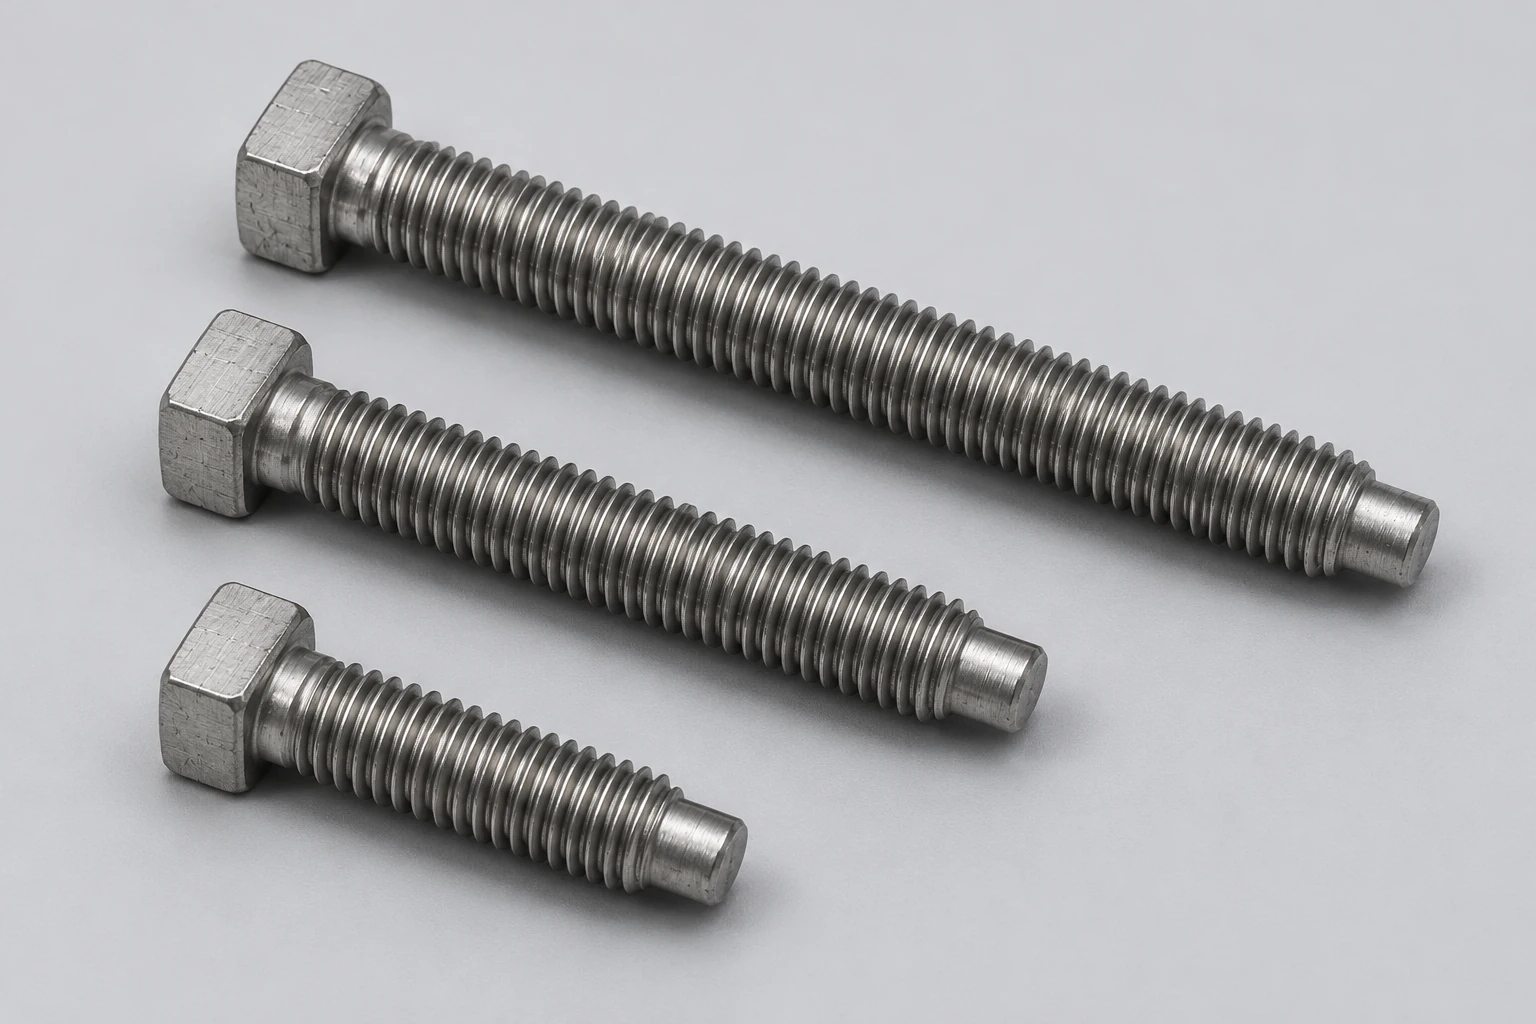 Positioning bolts |
| 316L stainless steelUNS S31603Low-carbon stainless |
| Production-equipment washdown and process auxiliaries | $ | 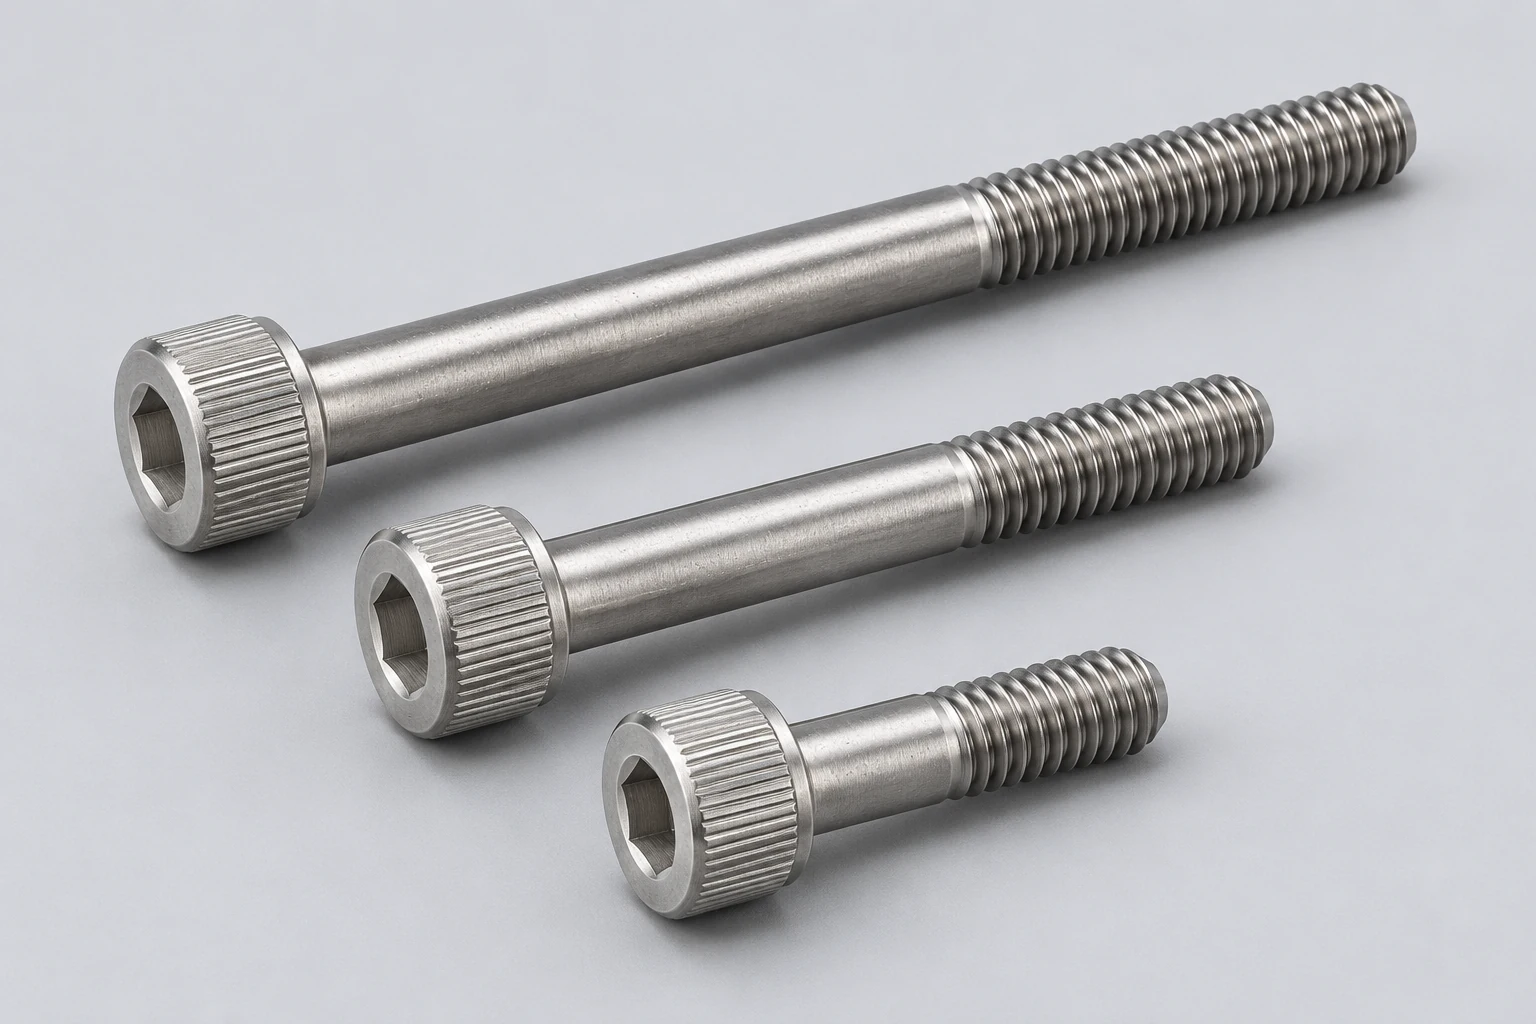 Socket screws |
| Inconel 718UNS N07718Age hardened |
| Loaded thermal-test assemblies with repeated hot cycles | $$$ | 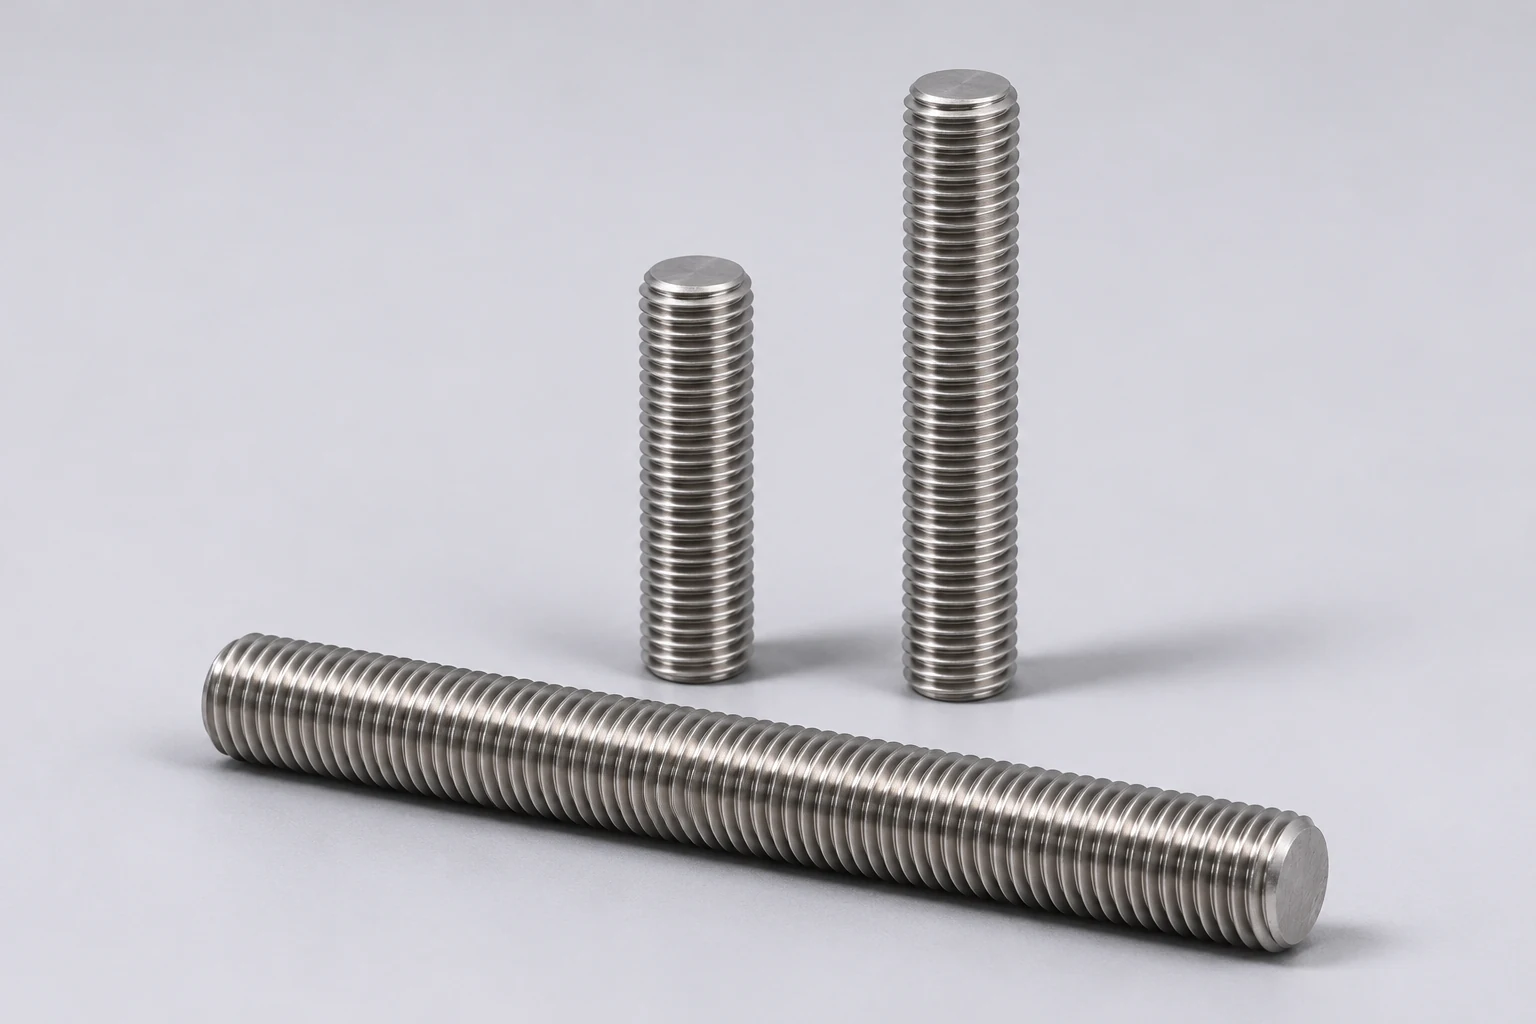 Stud bolts |
Budget guide: $ lower · $$ moderate · $$$ higher · $$$$ premium. Relative raw-material bands; dimensions, quantity, processing and inspection determine the finished-fastener quote.
Material & cost references
- Special Metals — INCONEL alloy 601
- Carpenter Technology — Custom 630 (17-4 PH) material data
- Special Metals — INCONEL alloy 718
- Special Metals — Automotive and heat-treatment applications
- Nickel and specialty-alloy round-bar price comparison
- Stainless-steel supplier price ranges
- 800H round-bar supplier price range
- Alloy 20 round-bar supplier price range
Cost bands group overlapping published supplier ranges for initial budgeting; they are not live BYBOLT prices. Specify the exact UNS and final condition on the order.
Match the fastener to the connection.
Inconel 601 hex bolts
Resist oxidation and scaling on heat-treatment fixtures through repeated production-furnace cycles.
17-4 PH positioning bolts
Keep assembly tooling accurately located with controlled shoulders and high-strength, age-hardened bodies.
316L socket head screws
Secure production-machine covers with compact heads and corrosion resistance for compatible washdown service.
Inconel 718 stud bolts
Provide high-strength clamping at loaded thermal-test assemblies, with grip lengths matched to the rig.
Production-fixture maintenance kits.
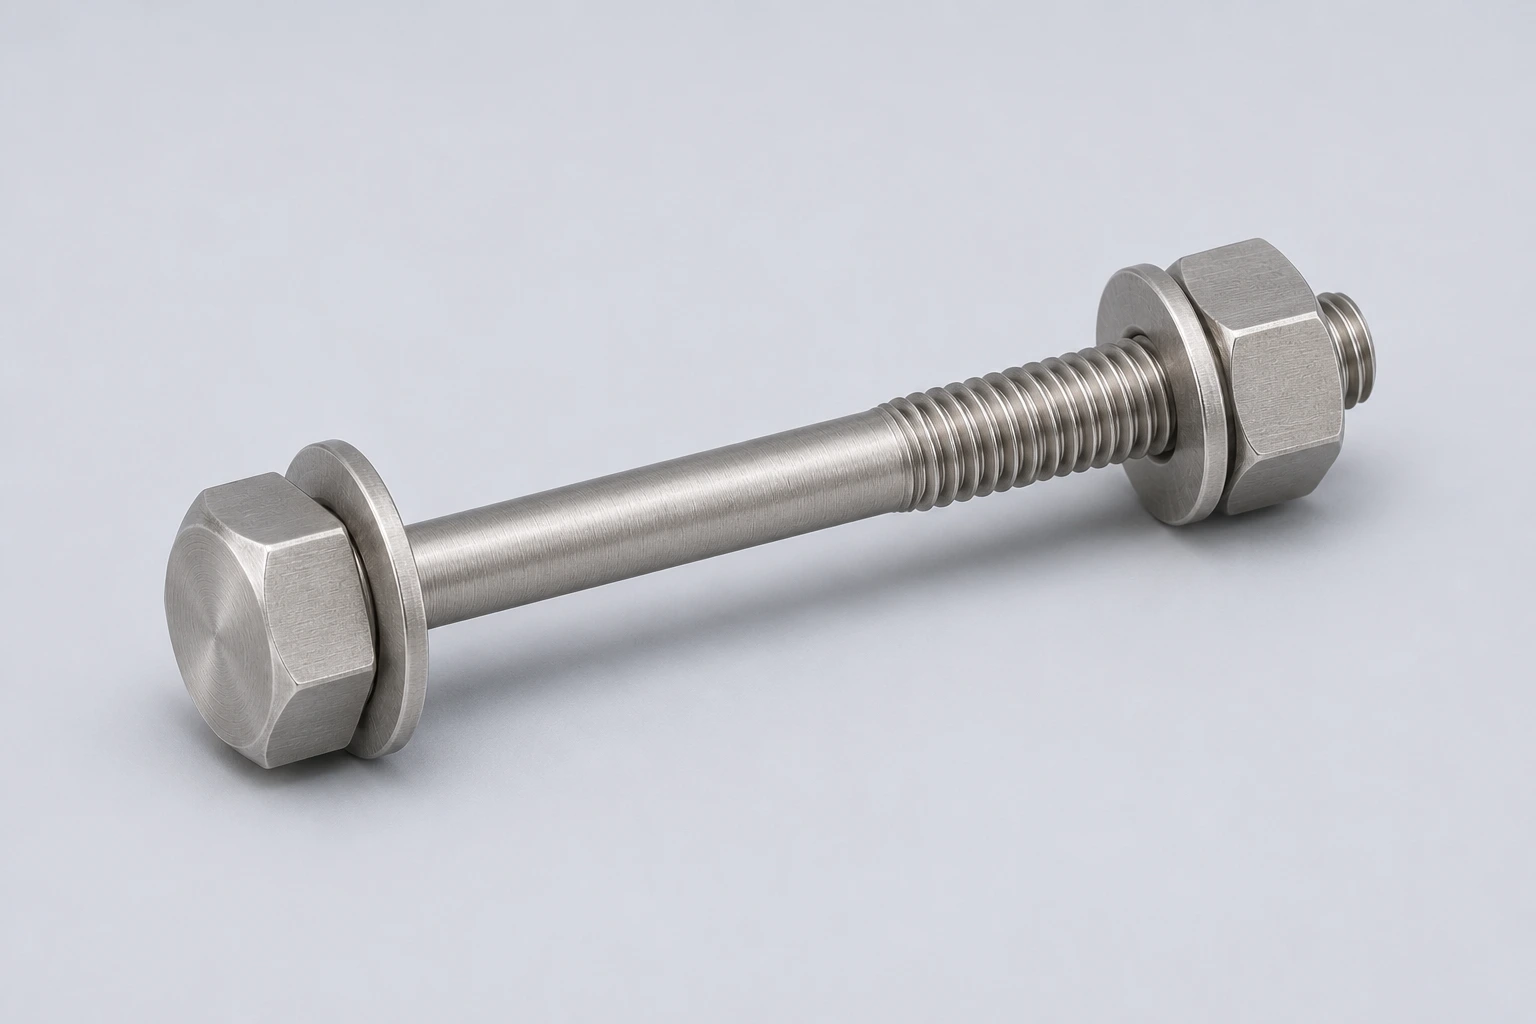
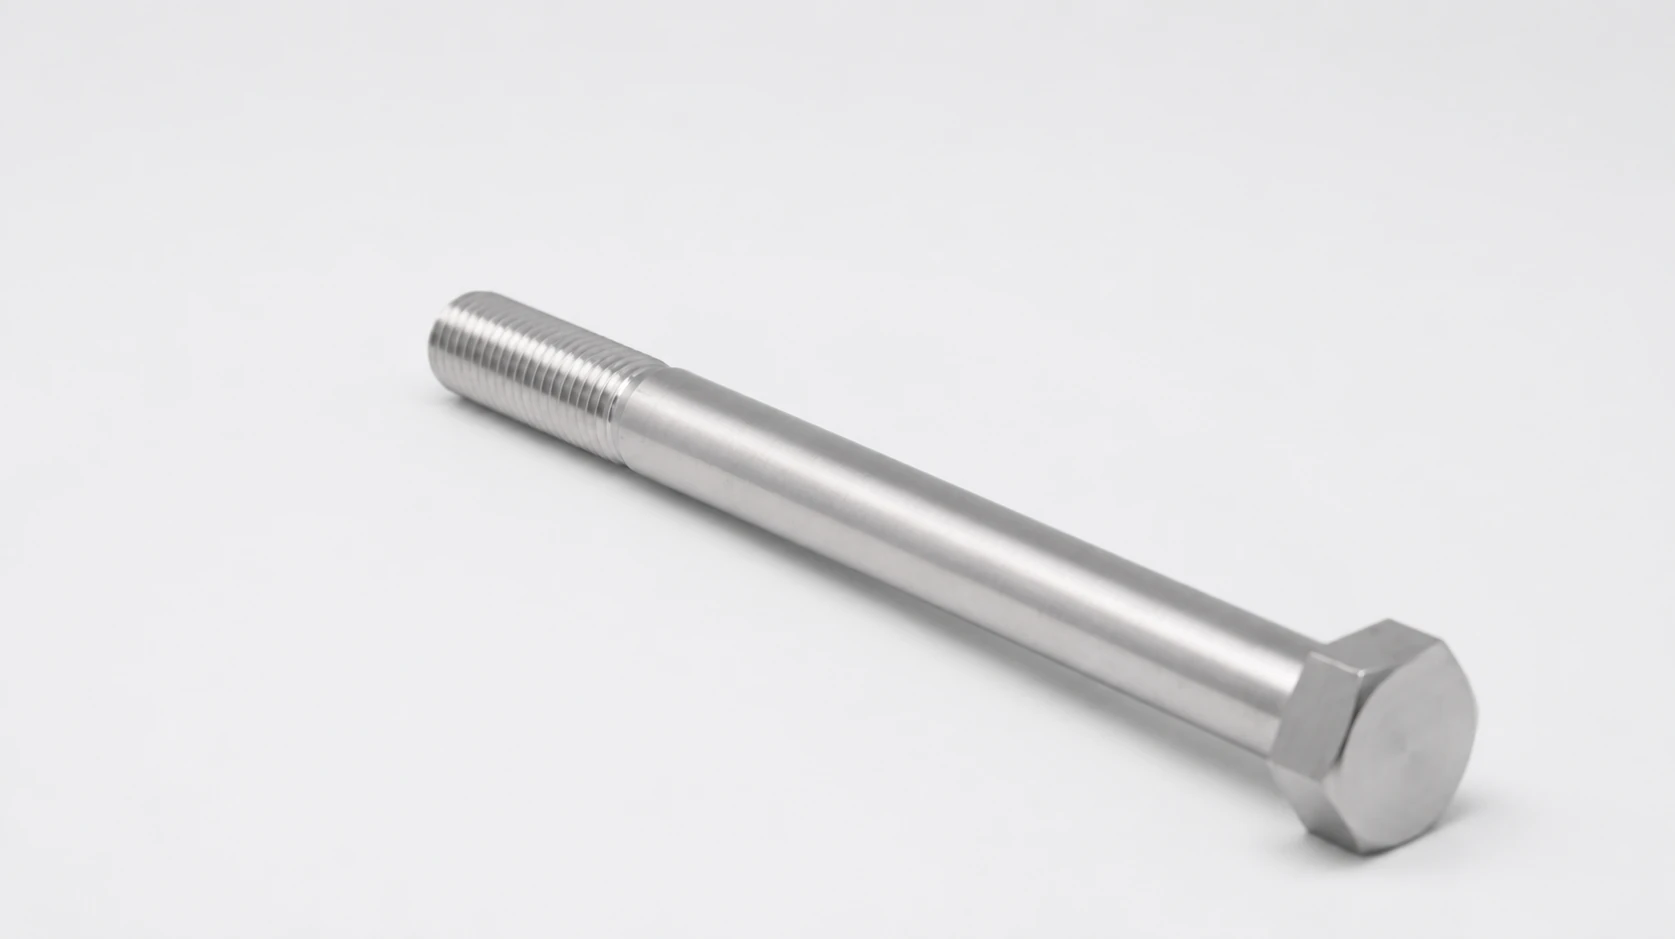
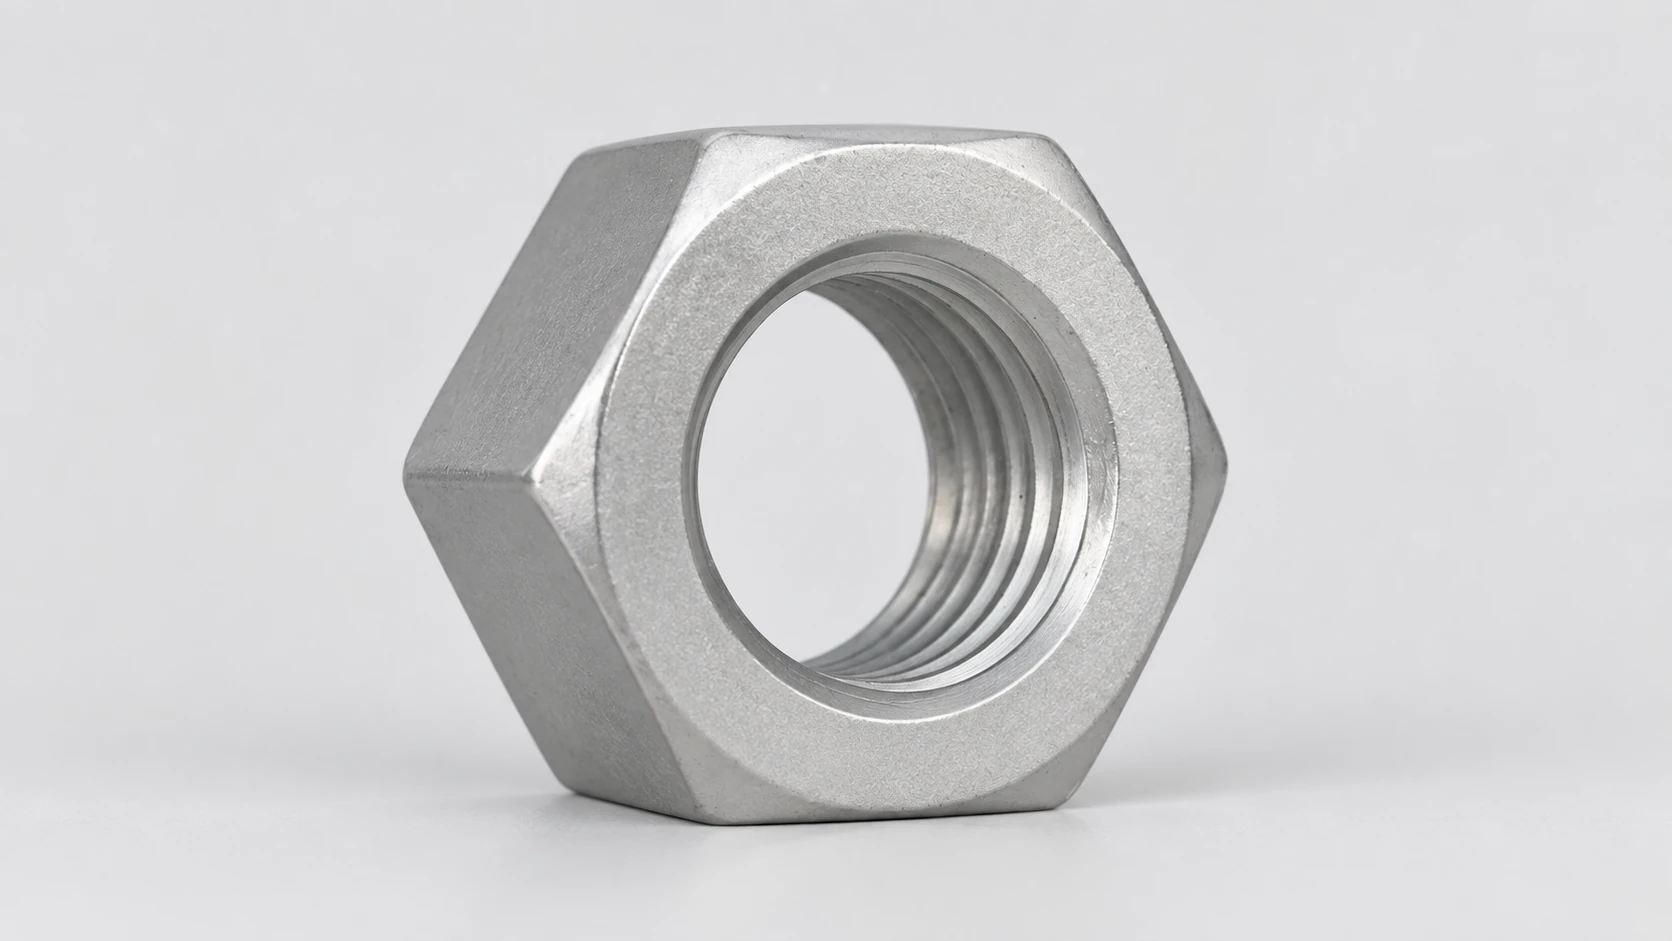
Put the locating, clamping and cover hardware for each production station on one list, with dimensions tied to its tooling drawing.
Trace the material. Inspect equipment fasteners.
EN 10204 3.1 MTC, heat traceability and mechanical test results with each shipment. Add the tests your equipment specification requires.
Material identity
Match the ordered grade and material heat to the certificate, part identification and packing list.
Final condition
Link the specified processing condition and mechanical results to the finished batch; keep separate heat-treatment batches identifiable.
Drawing dimensions
Station/tool number, revision and spare quantities.
Tooling inspection plan
List the critical characteristics, final-condition measurements and customer report format for the production tool.
Before you order equipment fasteners.
Send the drawing and the service details for your connection. We can quote the specified parts, finish and inspection package together.
Get a QuoteAre these fasteners for vehicles or manufacturing equipment?
This range addresses production and test equipment: tooling, furnaces, process machinery and test rigs. Send the equipment drawing and its acceptance requirements with the enquiry.
Can you work to our tooling drawing and inspection plan?
Yes. Provide the controlled revision, material condition, critical characteristics and required report format. Include supplier or process qualification requirements with the enquiry so they are addressed in the quotation.
What information is useful for battery-production equipment?
Identify the part location, any contacting fluid, cleaning process and cleanliness/packing criteria. Add critical dimensions and the required material condition for each part number.
Send your drawing
or parts list.
Upload the drawing or BOM with its revision. We quote the material, dimensions, quantities and inspection requirements for your equipment.
Production station/tool revision, critical dimensions, alloy condition, thermal or fluid exposure, cleanliness and quantities…